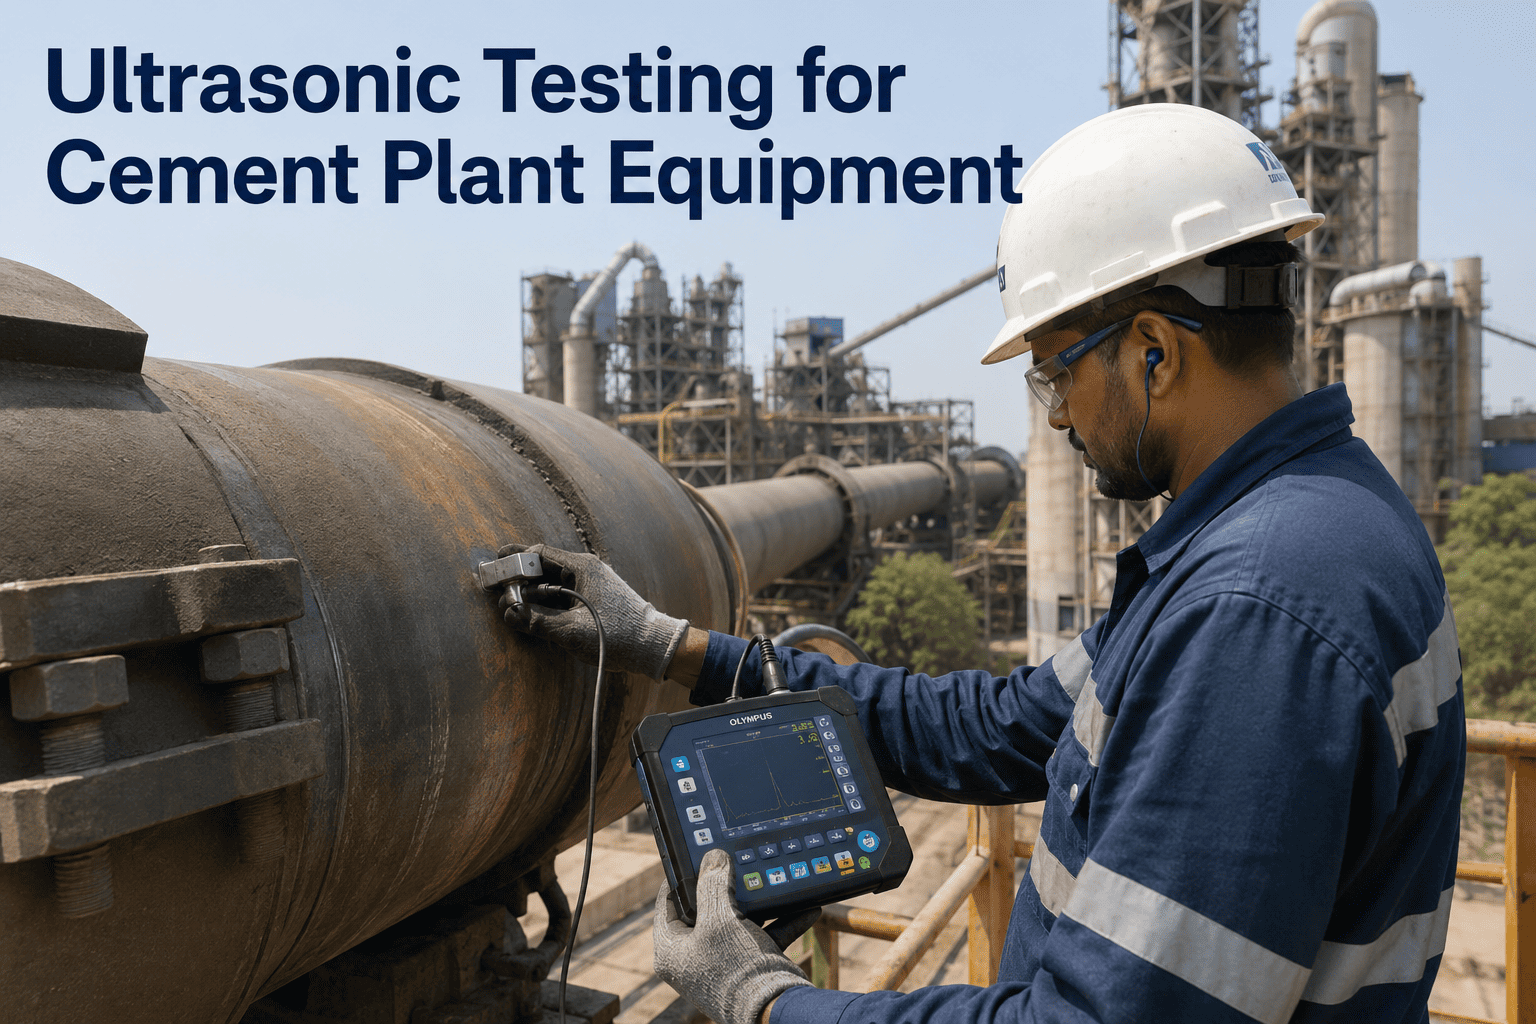
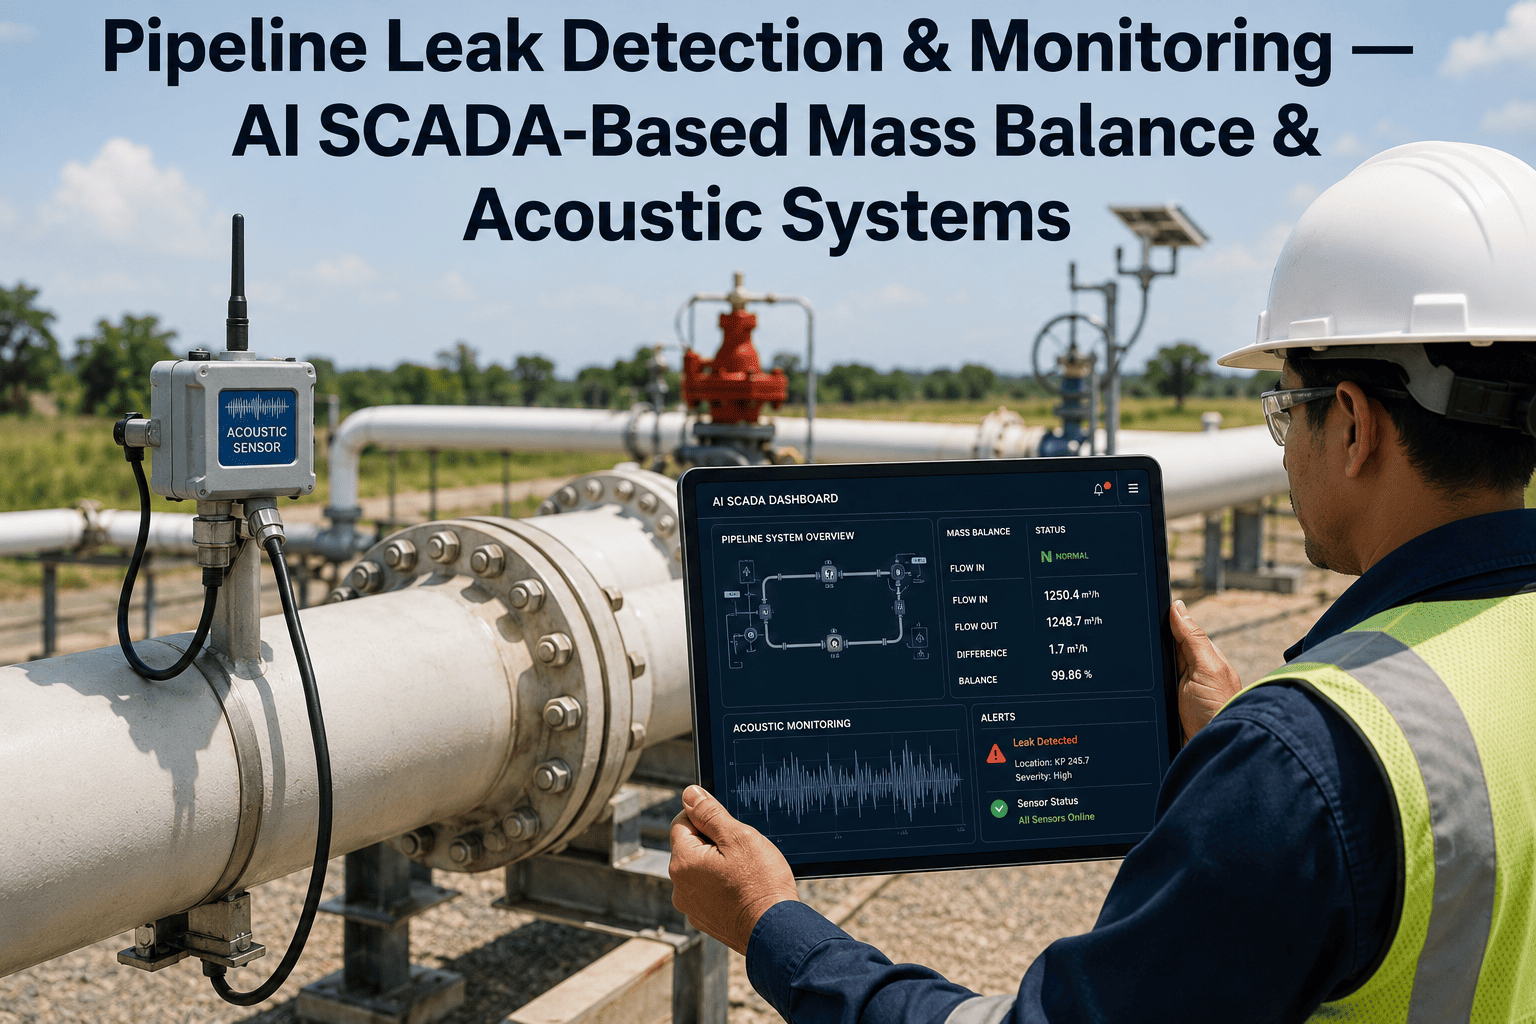
A cement plant loses wall thickness the same way it loses money on unplanned downtime: quietly, in millimeters, until the day a duct wall perforates mid-shift or a compressed air line ruptures near a walkway. Kiln shells, ID fan casings, cooler ducting, and hundreds of meters of process piping erode from dust abrasion and thermal cycling long before any visible sign appears on the outside. Ultrasonic thickness testing is the only practical way to see that loss coming, provided the readings are taken often enough and trended consistently enough to matter. Most plants inspect these assets on a fixed annual schedule regardless of actual wear rate, which means a duct wearing three times faster than average gets checked at the same interval as one barely losing metal at all. See how iFactory turns UT spot readings into continuous wall-thickness trending.
NON-DESTRUCTIVE TESTING · CEMENT · WALL THICKNESS & LEAK MONITORING
Ultrasonic Testing for Cement Plant Equipment — Know Which Wall Fails First, Not Which One Failed Last
iFactory converts scattered ultrasonic thickness readings from ducts, shells, piping, and pressure equipment into a single trended picture of remaining wall life, so replacement decisions happen on a schedule you control instead of one an unplanned leak sets for you.
Nominal Wall
100% of design thickness
Monitor Zone
70–85% remaining
Retirement Zone
Below minimum design thickness
THE COST OF NOT KNOWING
Why Wall Thinning Is the Failure Mode Cement Plants Catch Latest
Wall thinning almost never announces itself. A kiln inlet duct, a fan volute, or a compressed air header can lose more than half of its original wall thickness while looking structurally sound from the outside, because the corrosion and abrasion happen on the internal surface where dust-laden gas or slurry moves continuously across the metal. Unlike a bearing that starts vibrating or a motor that starts running hot, a thinning wall gives almost no operational warning until it perforates. By the time a leak appears — whether that is a visible dust plume from a duct seam or a pressure drop on a compressed air line — the wall has typically already crossed the point where a planned repair was possible, forcing an unplanned outage instead. The scale of the exposure is large because a single production line carries kilometers of ducting, piping, and vessel wall, almost all of it inaccessible during normal operation and most of it never instrumented for continuous monitoring.
60–70%
of unplanned cement plant shutdowns tied to mechanical failure trace back to a wear or corrosion mechanism that a scheduled inspection should have caught earlier.
10+ yrs
is the typical fixed re-inspection interval under API 510 for pressure vessels, far too long for high-abrasion cement duct and piping runs wearing at variable rates.
1 mm/yr
wear rate difference between a normal duct section and a high-turbulence elbow can mean the difference between five years and eighteen months to retirement thickness.
Hours
not weeks, is how quickly an unplanned leak on a hot gas duct or compressed air line can force a full line stoppage once wall perforation actually occurs.
WHERE UT MATTERS MOST
The Equipment Categories Where Wall Loss Actually Drives Risk
Not every asset in a cement plant needs the same UT attention. Coverage should follow where abrasion, corrosion, and pressure combine to create the highest consequence of failure, not simply follow a generic plant-wide checklist applied uniformly regardless of duty.
Kiln Inlet & Riser Ducts
Hot, dust-laden gas moving at high velocity erodes duct walls fastest at elbows, expansion joints, and any point where flow direction changes, making these the highest-priority UT grid locations on the pyroprocessing line.
ID Fan Casings & Volutes
Induced draft fan housings absorb continuous particulate impingement at the volute cutwater and outlet cone, locations that consistently show the fastest wall loss of any rotating equipment enclosure in the plant.
Clinker Cooler Ducting
High-temperature cycling combined with abrasive clinker dust accelerates thinning at cooler vent ducts and transition sections, where thermal expansion stress compounds the erosion mechanism over repeated heating cycles.
Compressed Air & Process Piping
Pneumatic conveying lines, compressed air headers, and cooling water piping thin from internal erosion and external corrosion simultaneously, and a rupture on a pressurized line creates immediate safety exposure beyond production loss.
Baghouse & Cyclone Shells
Dust collection vessel walls face combined abrasive wear from particulate loading and corrosive attack from condensing acid gases whenever operating temperature drops below the dew point during startup or upset conditions.
Storage Tanks & Silo Walls
Fuel oil tanks, water storage vessels, and steel silo shells experience slower but steady corrosion, warranting periodic UT surveys even though the wear rate rarely justifies the monitoring intensity applied to high-abrasion ducting.
FROM SPOT CHECK TO TREND LINE
Turning a Single UT Reading Into a Remaining-Life Forecast
A single ultrasonic thickness reading only tells you the wall is a certain number of millimeters thick on the day it was taken. It says nothing about how fast that wall is thinning or when it will cross the minimum allowable thickness for safe operation. The value comes from comparing successive readings at the same measurement point over time, and that comparison only works if the grid locations, the equipment tag references, and the data format stay consistent across every inspection cycle, which is exactly where manual spreadsheet-based tracking tends to break down.
01
Standardized Grid Mapping
Every component gets a fixed UT grid with numbered measurement points tied to the equipment tag, so the same physical location is measured every time regardless of which technician or contractor performs the survey.
02
Reading Capture & Digitization
Handheld gauge readings, whether logged manually or exported digitally, are captured against the grid reference so each new survey adds to a continuous history instead of starting a fresh, disconnected file.
03
Corrosion Rate Calculation
The platform calculates a wear rate per measurement point from successive readings, automatically flagging points where the rate has accelerated compared to the component's historical average.
04
Remaining Life Projection
Using the calculated wear rate and the minimum allowable thickness for the component, the platform projects a retirement date for every monitored point, ranked so the fastest-wearing locations surface first.
05
Planned Repair Scheduling
Projected retirement dates feed directly into the maintenance planning calendar, converting what would have been an unplanned leak response into a scheduled repair during a planned outage window.
SPREADSHEET VS TRENDED MODEL
What Changes When UT Data Moves Off the Spreadsheet
Most plants already collect the ultrasonic thickness data they need to predict failures. The gap is almost never data collection — it is what happens to that data after the inspection report is filed away.
Every UT Reading You Take Is Already Worth More Than the Spreadsheet You Store It In
iFactory pulls thickness readings from your inspection contractor or handheld gauge into a single trended model per component, so you see remaining life instead of a list of numbers.
READING THE TREND
Four Situations Where Trending Catches What a Single Reading Misses
These are the recurring patterns where a plant with trended UT data made a different maintenance decision than one relying on isolated spot checks, and where that difference determined whether the outcome was a planned repair or an unplanned outage.
SCENARIO 01
An Elbow Wearing Three Times Faster Than Its Neighbors
A kiln riser duct elbow shows a wear rate significantly above the straight-run sections measured on the same grid. Because the trend is visible immediately rather than buried in a report, the plant schedules a targeted repair on that single elbow during the next planned stop instead of waiting for the annual full-duct inspection to catch it.
SCENARIO 02
A Compressed Air Header Approaching Minimum Thickness
Successive readings on a compressed air line show the wall approaching the minimum allowable thickness roughly four months before the next scheduled inspection would have occurred. The projected retirement date gives the planning team enough lead time to source the replacement section and schedule the isolation without an emergency shutdown.
SCENARIO 03
A New Wear Pattern After a Process Change
After a fuel mix change alters gas velocity through a duct section, the wear rate at several grid points begins accelerating in a pattern that would not have been visible without a continuous trend line. Flagging the shift early lets the reliability team investigate the process cause before extensive metal loss occurs.
SCENARIO 04
Justifying a Deferred Repair With Data Instead of Judgment
A component reading close to the monitor threshold, but with a wear rate that has been flat for several survey cycles, gives the reliability team a documented basis to defer replacement to the next major outage rather than an unplanned intervention, saving the cost of an unnecessary early shutdown.
CHOOSING THE RIGHT TECHNIQUE
Conventional Spot UT, Corrosion Mapping, and Permanent Monitoring Compared
Not every component needs the same inspection method, and picking the wrong one for a given asset either wastes budget on unnecessary coverage or leaves a genuinely high-risk location under-inspected. The three approaches below sit on a spectrum from lowest cost and coarsest resolution to highest cost and continuous visibility, and a mature UT program deliberately mixes all three across the plant rather than defaulting to one method everywhere.
Conventional Spot Readings
A handheld contact transducer takes single-point thickness readings at fixed grid locations during a scheduled walk-down. Lowest cost per point and the right default for the majority of piping and duct runs where wear is expected to be relatively uniform across the section.
Corrosion Mapping
A scanning transducer or automated crawler collects a dense grid of readings across a defined area, producing a thickness contour rather than isolated points. Justified on vessel heads, elbows, and other geometries where localized pitting or gouging could hide between conventional spot points.
Permanently Installed Sensors
Wireless ultrasonic transmitters mounted at a fixed point stream continuous thickness data without requiring a technician to physically access the location. Reserved for the highest-consequence points that are difficult to reach safely or that warrant near-real-time wear rate visibility.
Guided Wave Screening
A single transducer ring sends an ultrasonic wave along a length of pipe, screening tens of meters from one access point to flag general areas of wall loss for more detailed follow-up rather than producing a precise thickness value at every location.
MAKING THE ECONOMIC CASE
What a Trended UT Program Actually Saves Over Reactive Repair
Reliability teams rarely struggle to convince plant management that wall thickness matters — the harder conversation is justifying the ongoing cost of a structured inspection and trending program against the alternative of repairing failures as they occur. The comparison is more favorable than it first appears once the full cost of an unplanned leak is counted rather than just the price of the replacement section itself.
A
Planned Repair Cost
A scheduled section replacement during a planned outage typically involves material cost, a few hours of fabrication and welding labor, and no incremental production loss because the work fits inside a stop that was already planned for other reasons.
B
Unplanned Repair Cost
The same repair performed reactively after a perforation typically costs several times more once emergency labor rates, expedited material sourcing, and the production line stoppage required to isolate and access the failed section are all included.
C
Safety & Secondary Damage Exposure
An unplanned leak on a hot gas duct or a pressurized line also carries safety exposure and the risk of secondary damage to adjacent equipment or electrical systems, costs that rarely appear in a maintenance budget line but weigh heavily in any full accounting.
FREQUENTLY ASKED QUESTIONS
What Reliability Teams Ask Before Digitizing UT Data
Do we need to change our existing UT inspection contractor or gauge equipment to use this?
No change is required to your existing inspection provider or handheld ultrasonic gauge equipment. The platform is designed to ingest thickness readings regardless of which contractor or gauge model collected them, matching each reading to the correct equipment tag and grid point based on the survey report format your team already uses. Many plants continue using the same inspection contractor for years after adopting trended digital tracking, since the value comes from what happens to the data after collection rather than from changing how the data is captured in the field.
Contact support to review how your current survey report format maps into the platform.
How is the minimum allowable thickness determined for each component?
Minimum allowable thickness is set per component based on original design thickness, applicable code requirements such as ASME or API standards where relevant, and any engineering assessment specific to that asset's service conditions. The platform stores this limit alongside each component record so every trended projection is measured against the correct threshold rather than a generic plant-wide default. Where a formal engineering assessment has not yet been performed for a given asset, a conservative default consistent with common industry practice is applied until updated.
Book a demo to see how thresholds are configured for your specific equipment list.
Can the platform handle components with irregular or limited historical data?
Yes, though the confidence of any wear rate projection naturally improves as more survey cycles accumulate for a given point. For components with only one or two historical readings, the platform displays the current thickness against the design and minimum values without an aggressive rate projection, and flags the point for closer attention on the next survey cycle to begin building a reliable trend. Once three or more consistent readings exist at a grid point, rate-based forecasting becomes meaningfully more reliable for planning purposes.
How does this integrate with our existing maintenance planning and CMMS system?
Retirement date projections and wear rate alerts are structured to flow directly into standard maintenance planning workflows, generating work order recommendations tied to the specific component and grid location once a projected date falls within your planning horizon. This closes the gap between an inspection finding and a scheduled repair, which is often where value is lost even at plants that already collect good UT data consistently.
Talk to our support team about integration with your specific CMMS platform.
What happens when a UT reading appears anomalous compared to the established trend?
Readings that deviate sharply from the established wear rate at a given point are flagged for review rather than automatically accepted into the trend line, since gauge coupling issues, surface roughness, or measurement error can occasionally produce an outlier reading. The platform distinguishes between a genuine acceleration in wear rate, which warrants immediate attention, and a likely measurement anomaly, which warrants a re-check on the next visit, helping reliability teams avoid both false alarms and missed early warnings.
Book a demo to see anomaly handling applied to a sample dataset from your plant.
The Next Leak Should Show Up on a Trend Line, Not on the Plant Floor
iFactory turns the ultrasonic thickness data your team already collects into a ranked, continuously updated forecast of which component needs attention next — so repairs get scheduled instead of discovered.