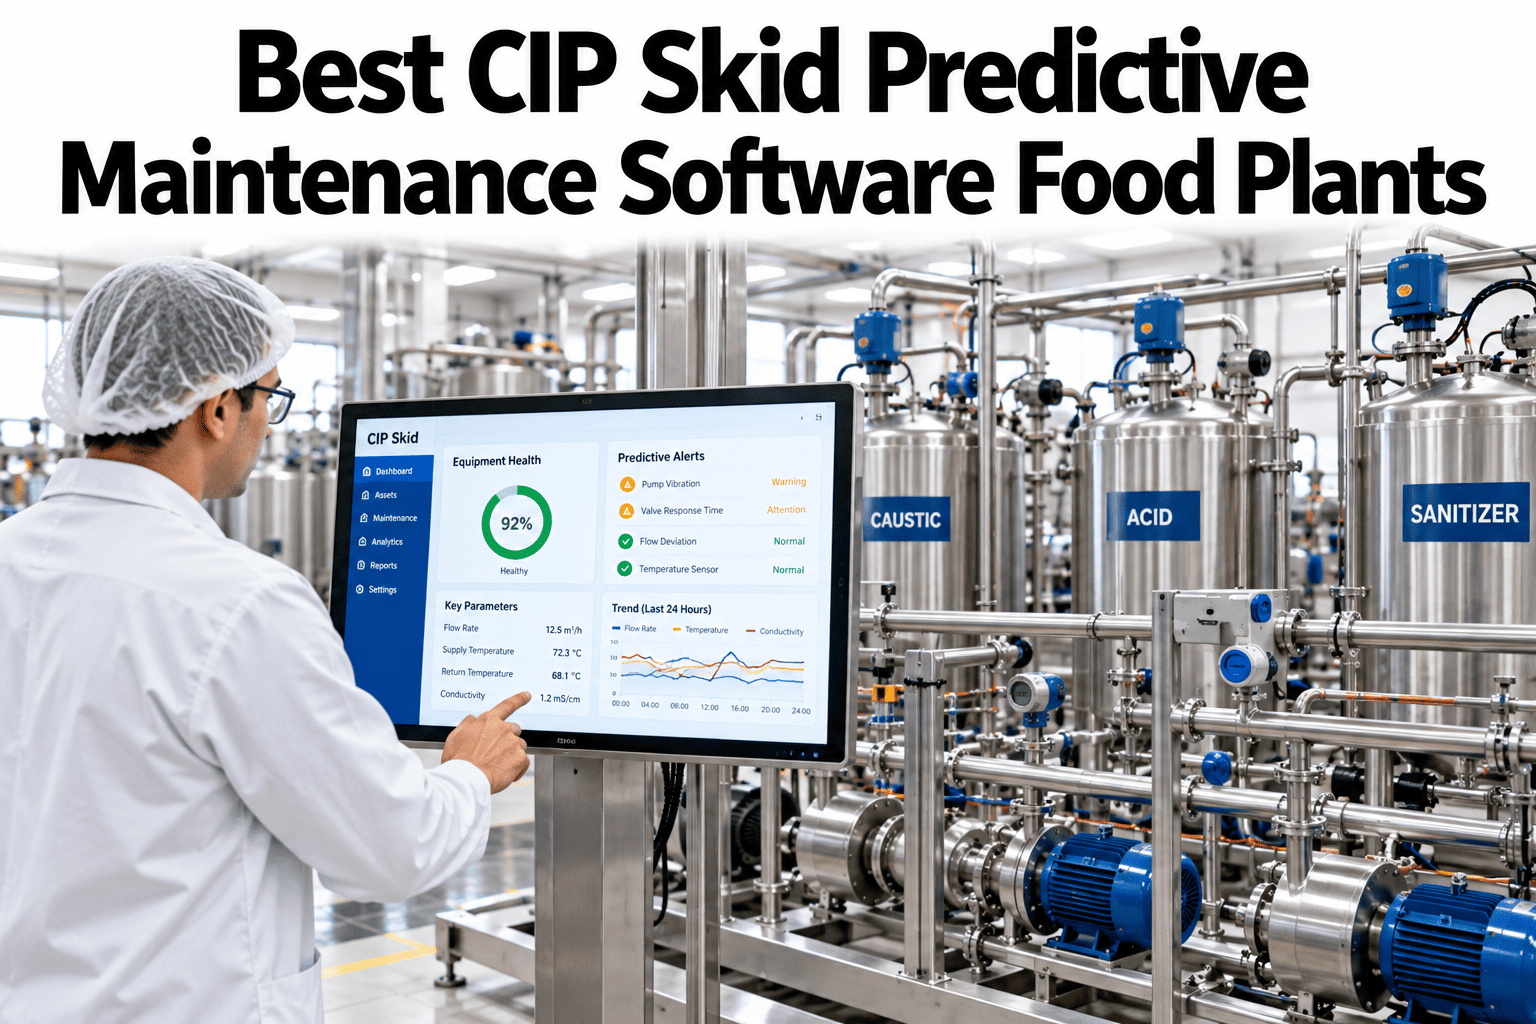
A CIP cycle can finish on time, print a green report and still leave soil in the line. The cause is often the skid itself: a supply pump losing flow, a steam valve drifting, a spray device partly blocked or a sensor reading a little high. Predictive maintenance on the skid catches these before the next sanitation check fails. Food plants weighing software for this job can ask iFactory AI how skid health is tracked.
Best CIP Skid Predictive Maintenance Software for Food Plants: A 2026 Buyer Guide
Know which skid assets are failing before a wash goes out of range. This guide shows what to monitor, what good software must do and how to judge it, with iFactory AI as the plant-wide layer.
Why CIP Skids Fail Quietly
A CIP skid is a small plant inside the plant: tanks, pumps, a heat exchanger, valves, sensors and spray devices. Most of it is hidden behind panels and pipework. Wear shows up not as a stop but as a wash that is slightly weaker than it should be.
Cycle passes, swab fails
The report is green but the hygiene check is not. The cause often sits in flow, temperature or concentration drift that stayed inside loose limits.
Cycles run longer
Operators extend steps to compensate. Time, water and chemical use rise, and nobody records why.
Sudden stop
A pump seizes or a valve sticks mid-cycle, and the line waits for a repair that could have been planned.
The Process Notes guide makes a point worth keeping in mind: sanitiser at the end can mask a problem if the wash steps failed. A skid that is quietly degrading therefore carries risk that the final rinse hides.
What Is on the Skid and What Wears
Predictive maintenance works asset by asset. Start by listing what the skid contains and what fails first on each item.
| Asset | Early Signals | Typical Causes | What to Trend |
|---|---|---|---|
| Supply pump | Rising vibration, falling flow at same speed | Bearing wear, impeller wear, cavitation, seal leak | Vibration, motor current, flow, discharge pressure |
| Spray devices and strainers | Pressure moves from commissioning baseline | Blocked holes, fouled strainer, damaged device | Pressure against flow at each circuit |
| Heat exchanger | Longer heat-up, higher steam valve position | Scale or soil on heat surfaces | Heat-up time, valve position, supply-to-return temperature |
| Steam or temperature valve | Overshoot, hunting, slow response | Worn actuator, stem wear, poor tuning | Setpoint error, valve position, response time |
| Conductivity sensor | Slow drift, reading step after a cleaning | Coating, ageing electrode, temperature compensation fault | Reading against a reference or laboratory check |
| Flow meter | Reading disagrees with pump behaviour | Fouling, air in line, calibration shift | Flow against pump curve and pressure |
| Dosing pumps | Dose time or stroke count changes | Check-valve wear, air lock, diaphragm fatigue | Dose delivered against concentration reached |
Effective Time: What the Report Does Not Show
Cleaning works through four factors: time, action, temperature and concentration. The Process Notes guide points out that elapsed time is not the same as compliant time. If a wash step is out of range for part of its duration, only the in-range part counts.
Many controllers pause the timer on deviation, which is the correct behaviour. The risk is the case where a skid fault keeps conditions just inside the limits, so the timer runs while the cleaning action is weak. Skid health data shows that gap before the swab does.
| Factor | Typical Range in the Source | Skid Asset Behind It |
|---|---|---|
| Temperature | Alkaline 70 to 80 °C, chlorinated alkaline 55 to 65 °C, acid 40 to 70 °C, pre-rinse 35 to 43 °C | Heat exchanger, steam valve, temperature sensor |
| Action | At least 1.5 m/s in the largest pipe, 2.0 m/s as a target | Supply pump, strainers, spray devices, flow meter |
| Concentration | Per chemical supplier, held with a conductivity sensor on the return | Dosing pumps, conductivity sensor |
| Time | Tanks 10 to 20 minutes, line circuits 20 to 30 minutes | Controller and valve sequencing |
Catch Skid Faults Before Swab Day
Book a 30-minute session and iFactory AI will show how pump, valve, sensor and flow data from a CIP skid becomes early warnings and planned jobs.
Supply Pump Health: Vibration Patterns to Watch
The supply pump is the heart of the skid, and vibration is the classic way to watch it. A trade article from MFG Robots describes the usual fault signatures, which condition monitoring software can match automatically.
| Fault | Signature in the Source | Meaning on a CIP Pump |
|---|---|---|
| Imbalance | Vibration at 1 times running speed, mostly radial | Impeller damage or buildup |
| Misalignment | 1 and 2 times running speed, strong 2 times axial for angular | Coupling or base problem after maintenance |
| Bearing defect | Fault frequencies from 5 to 100 times running speed, depending on geometry | Wear that precedes seizure |
| Cavitation | Broad-band high-frequency energy | Starved suction from a low tank level or blocked strainer |
The same source describes the four zones of ISO 10816: A acceptable, B needs closer monitoring, C needs prompt corrective action and D means immediate shutdown. It gives no numeric limits, so take those from the standard and your pump's maker.
Spray Devices and Flow: Spotting a Clog Early
A blocked spray hole or a fouled strainer does not trip an alarm. It simply changes the relationship between pressure and flow. The Process Notes guide says a pressure deviation from the commissioning baseline signals spray device failure or strainer fouling.
The bars show an illustrative 40 mm circuit in cubic metres per hour. The guide's DIN 11851 figures give 6.1 as the minimum at 1.5 m/s and 8.2 at 2.0 m/s for that diameter. The circuit has fallen about 29 percent from its commissioning baseline and now sits only just above the minimum, so a small further loss would put cleaning action out of range.
| Pipe Diameter | Minimum Flow at 1.5 m/s | Flow at 2.0 m/s |
|---|---|---|
| 25 mm | 2.9 m3/h | 3.8 m3/h |
| 40 mm | 6.1 m3/h | 8.2 m3/h |
| 50 mm | 10.6 m3/h | 14.1 m3/h |
| 65 mm | 18.5 m3/h | 24.6 m3/h |
| 80 mm | 27.8 m3/h | 37.1 m3/h |
| 100 mm | 42.4 m3/h | 56.5 m3/h |
The same guide warns about parallel branches. One branch can pass the velocity check while another runs below 1.5 m/s, and both record the same cycle time. Flow per branch, not only total flow, is what software should watch.
Heat Exchanger and Temperature Valve Drift
Temperature is the second big lever of cleaning. A fouled exchanger or a worn steam valve usually shows up in the controls before it shows up in the report.
These patterns are common in practice, but each plant should confirm its own thresholds from trend history. Compare like with like: same program, same product, same season of cooling-water temperature.
Sensors: When the Instrument Is the Problem
Every decision on the skid rests on its sensors. If the conductivity probe reads high, the concentration may be lower than reported. If the flow meter drifts, the velocity check is wrong. Endress+Hauser notes that conventional calibration needs the sensor taken out of the process, and that sensor drift may remain undetected between two calibration intervals.
Cross-check readings
Compare conductivity with dose delivered, and flow with pump speed and pressure. Disagreement points to a sensor or a pump.
Watch for steps
A sudden jump after cleaning or handling is more likely a coating or wiring fault than a real change.
Verify on a schedule
Software flags suspect sensors, and a technician confirms with a reference check on a set interval.
The Endress+Hauser page places the temperature sensor in the CIP return line, where temperatures swing quickly while rinsing and cooling, and quotes a process range of 20 to 70 °C. Both facts matter when judging whether a reading is trustworthy at a given moment.
Three Skid Stories: How an Alert Plays Out
Alerts only matter if they lead to the right action. These short, illustrative cases show the path from signal to repair.
The tired supply pump
Vibration creeps into zone B over three weeks while flow at the same speed slips. The software ranks the pump first, maintenance books a bearing change in the weekend gap and the pump never reaches zone C.
The slow heat-up
Alkaline heat-up takes six minutes longer than last quarter and the steam valve runs wider for the same setpoint. The alert points to the exchanger, and a descale at the next planned stop restores the old curve.
The sensor that lied
Conductivity reads steady, but the dosing pump now takes longer to reach it. Cross-checking shows the probe is coated. A cleaned and checked sensor shows the real strength was lower than reported.
In each case the skid told the team something days or weeks before a cycle failed. The value came from three things together: a baseline to compare against, an alert that said where to look and a job raised with the evidence attached. Remove any one of them and the warning is easy to ignore.
Keep a short log of every alert, what was found and what was done. After a quarter the log shows which signals earn their place and which only add noise, and it becomes the best argument for extending the program to the next skid.
How to Judge the Best Software: A Buyer Scorecard
Skid monitoring tools differ widely. Some are generic vibration systems, some belong to the CIP controller and some are plant-wide analytics platforms. Score each candidate against the same criteria, and weight them to suit your plant. The weights below are a starting point.
| Criterion | What to Ask | Weight |
|---|---|---|
| Signal coverage | Does it read pump, valve, temperature, flow, conductivity and dosing signals, not only vibration? | 20 |
| Phase-aware baselines | Does it compare each cycle phase against its own history, so a hot caustic step is not judged against a rinse? | 20 |
| Alert quality | Are alerts ranked and explained, with a clear next step, or do they flood the team? | 15 |
| Work-order handoff | Does an alert become a job in your maintenance system with the evidence attached? | 15 |
| Audit trail | Can you show what was seen, who acted and when, for an auditor? | 15 |
| Deployment and data access | Can it connect to your controller and historian without a long project? | 10 |
| Cost and support | Is the pricing clear and is there local support? | 5 |
| Total | 100 |
Ask each supplier to run a pilot on one skid with your own data. A demo on clean sample data says little about how a tool handles your noisy signals, and a pilot shows it plainly.
What the Money Looks Like: A Worked Example
Use your own figures, but the method is simple. Count the events the skid causes, price each one and estimate how many can be avoided. The numbers below are illustrative.
| Supply Pump Event | Run to Failure | Planned Repair |
|---|---|---|
| Parts and labour | 6,500 with rush delivery | 2,200 |
| Line downtime | 8 hours at 800 margin, 6,400 | 2 hours at 800 margin, 1,600 |
| Total | 12,900 | 3,800 |
| Difference | 9,100 saved per avoided seizure | |
Add the cost of a failed swab, a held batch or a customer complaint, and the case grows, though those figures vary too much to guess here. Count only what you can document.
Common Mistakes When Monitoring CIP Skids
Programs stall for plain reasons. Each has a plain fix.
A 90-Day Path to Skid Predictive Maintenance
iFactory AI is built as a turnkey server that racks in, plugs in and goes live in roughly 6 to 12 weeks, so a one-skid pilot fits inside a quarter.
What iFactory AI Adds
iFactory AI is smart manufacturing and industrial software. For a CIP skid it brings equipment condition, cycle data and maintenance into one place for food plants.
Plain-Language Glossary
Shared words keep sanitation, maintenance and quality aligned.
Frequently Asked Questions
What does CIP skid predictive maintenance monitor?
The supply and dosing pumps, heat exchanger, temperature valves, spray device pressure, flow meters and conductivity sensors, trended against baselines for each cycle phase.
How is it different from a CIP controller?
A controller runs the recipe and records pass or fail. Predictive maintenance watches the health of the equipment behind it and warns before a cycle goes out of range. Ask support how the two work together on your skid.
Can it spot a clogged spray device?
It can flag a change in pressure and flow against the commissioning baseline, which is a typical sign of clogging or a fouled strainer. A technician confirms the location.
Do we need new sensors?
Often not at first. Start with signals the controller already holds, then add vibration or flow points where gaps show up in the pilot.
How long before we see value?
Baselines build over the first weeks of cycles. A one-skid pilot over 90 days is usually enough to judge alert quality and avoided repeats.
Keep Your CIP Skid Ahead of Failure
iFactory AI joins pump, valve, flow and sensor data to cycle history so your team can fix skid faults before sanitation fails. Book a walkthrough on your own plant data.