A power plant seldom loses output to its fuel handling plant on an ordinary day. The yard holds days of coal, the bunkers hold hours, and a slow rake or a blocked hopper is absorbed without anyone noticing. The loss shows up on the day a buffer is already low: mills starve, load is held back and rakes stand in the siding. Fuel handling cycle time is the number that tells you how much margin you really have. This guide follows a rake from placement to bunker, then looks at gas and fuel oil, and shows where the time can be recovered. To see where your own fuel cycle stands, book a fuel handling review.
Fuel Handling Cycle Time: Find Where the Hours Go Between Rake and Bunker
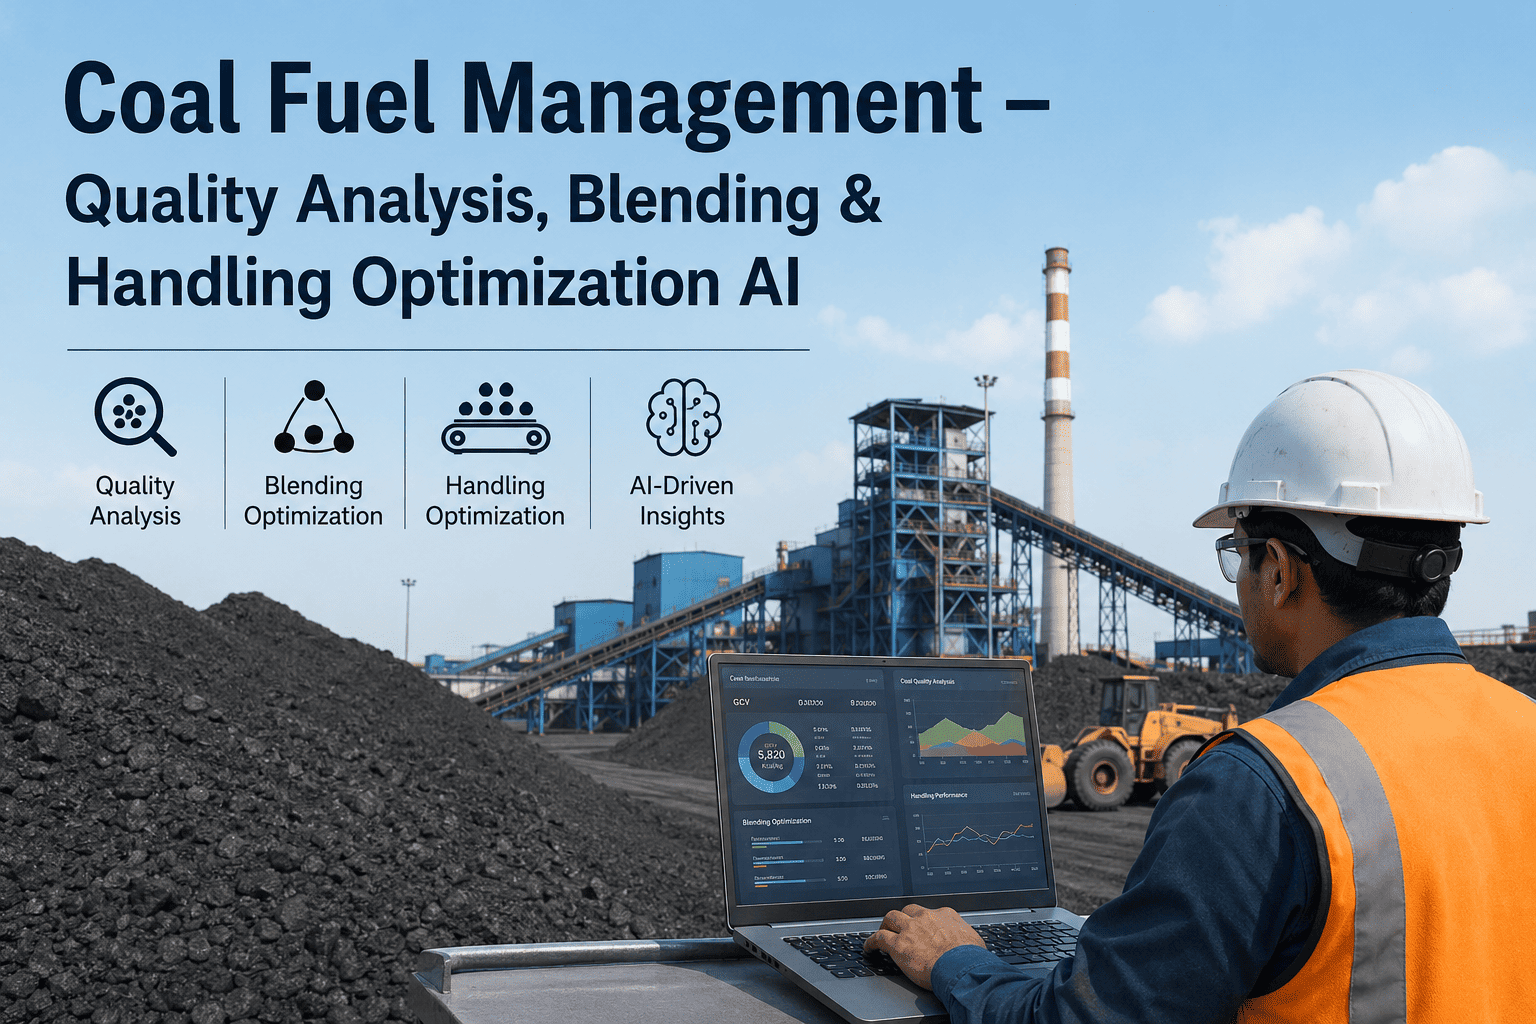
iFactory reads DCS, SCADA and historian signals from the coal handling plant, builds a timeline for every rake, shows which minutes were spent tipping and which were spent waiting, and tells the shift whether the bunkers will last until the next rake. It reads data only and never writes to your control system.
- Rake-by-rake timeline, from placement to release
- Blocked and waiting minutes separated from working minutes
- Bunker run-down compared with the next rake's arrival
Why Fuel Handling Delays Stay Hidden Until They Cost Output
Generation is limited by fuel handling only when the buffers run out, so a slow cycle can go unnoticed for months. A tippler that waits twenty minutes a rake looks like a normal day. The same twenty minutes on a day with a late rake, a wet yard and a bunker at low level decides whether a mill is lost. When the buffer is the only thing standing between the two, the cycle time is worth measuring directly. Our power plant specialists can review a month of your tippler and conveyor signals.
Buffers hide the loss
Yard stock and bunker level absorb slow cycles, so no one sees the delay until both are low at the same time.
Blocked time looks like running time
A tippler waiting on a full hopper or a stopped conveyor is not faulty, so it never raises an alarm. The minutes simply add up.
Interlocked start sequences
Conveyors start one after another, each against the next. After a trip, the restart sequence can take longer than the fault that caused it.
Wet coal and choked chutes
In the monsoon, wet and sticky coal chokes hoppers, feeders and transfer chutes, and each clearance adds minutes to the rake.
Route changes between stacking and bunkering
Switching a stream from bunkers to the stacker, or reclaiming to bunkers, takes time and care. Done late, it leaves a stream idle.
Coordination by radio
The siding, the tippler, the crusher house and the control room each see their own part. No one sees the rake from placement to bunker.
The Coal Cycle, Segment by Segment, for an Illustrative Unit
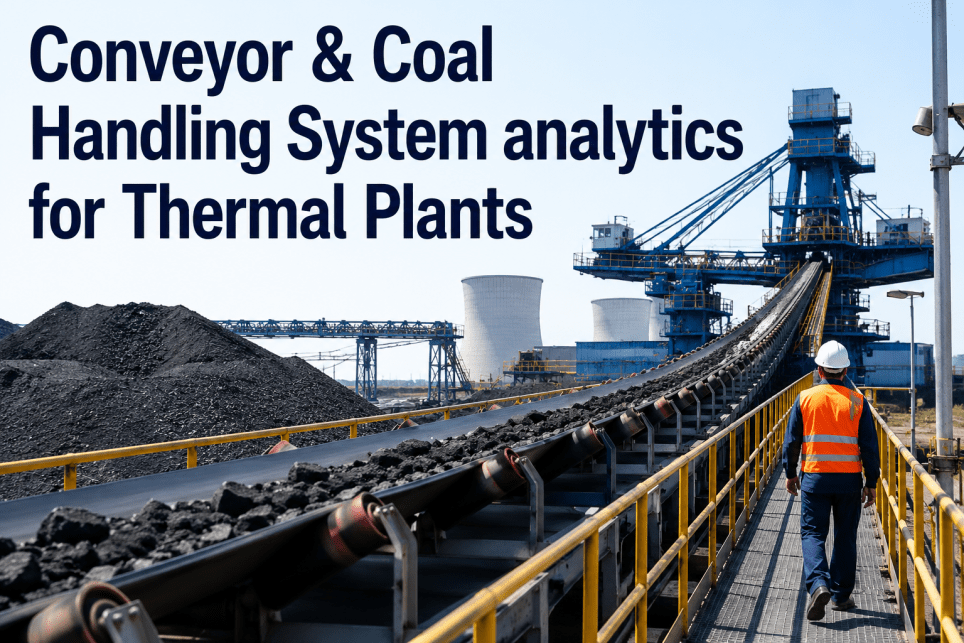
The illustrative plant is two 500 MW coal units burning about 15,600 tonnes a day, supplied by 4.5 rakes a day of about 3,500 tonnes each, through one wagon tippler and a 1,200 tonne per hour conveyor stream to the bunkers. Its figures are not unusual. Tipping a wagon takes about 90 seconds on the machine, yet the effective time from one wagon to the next is far longer once positioning, clamping, clearing and waiting are counted. To build this table from your own signals, book a cycle time session.
Time One Fuel Route End to End in Six Weeks
Choose one unit. We connect its tippler, conveyor and bunker signals, build a timeline for every rake in the last three months, separate working time from waiting time, and show the shift what the fuel margin is each day.
Coal, Gas and Fuel Oil: Three Fuel Cycles With Different Limits
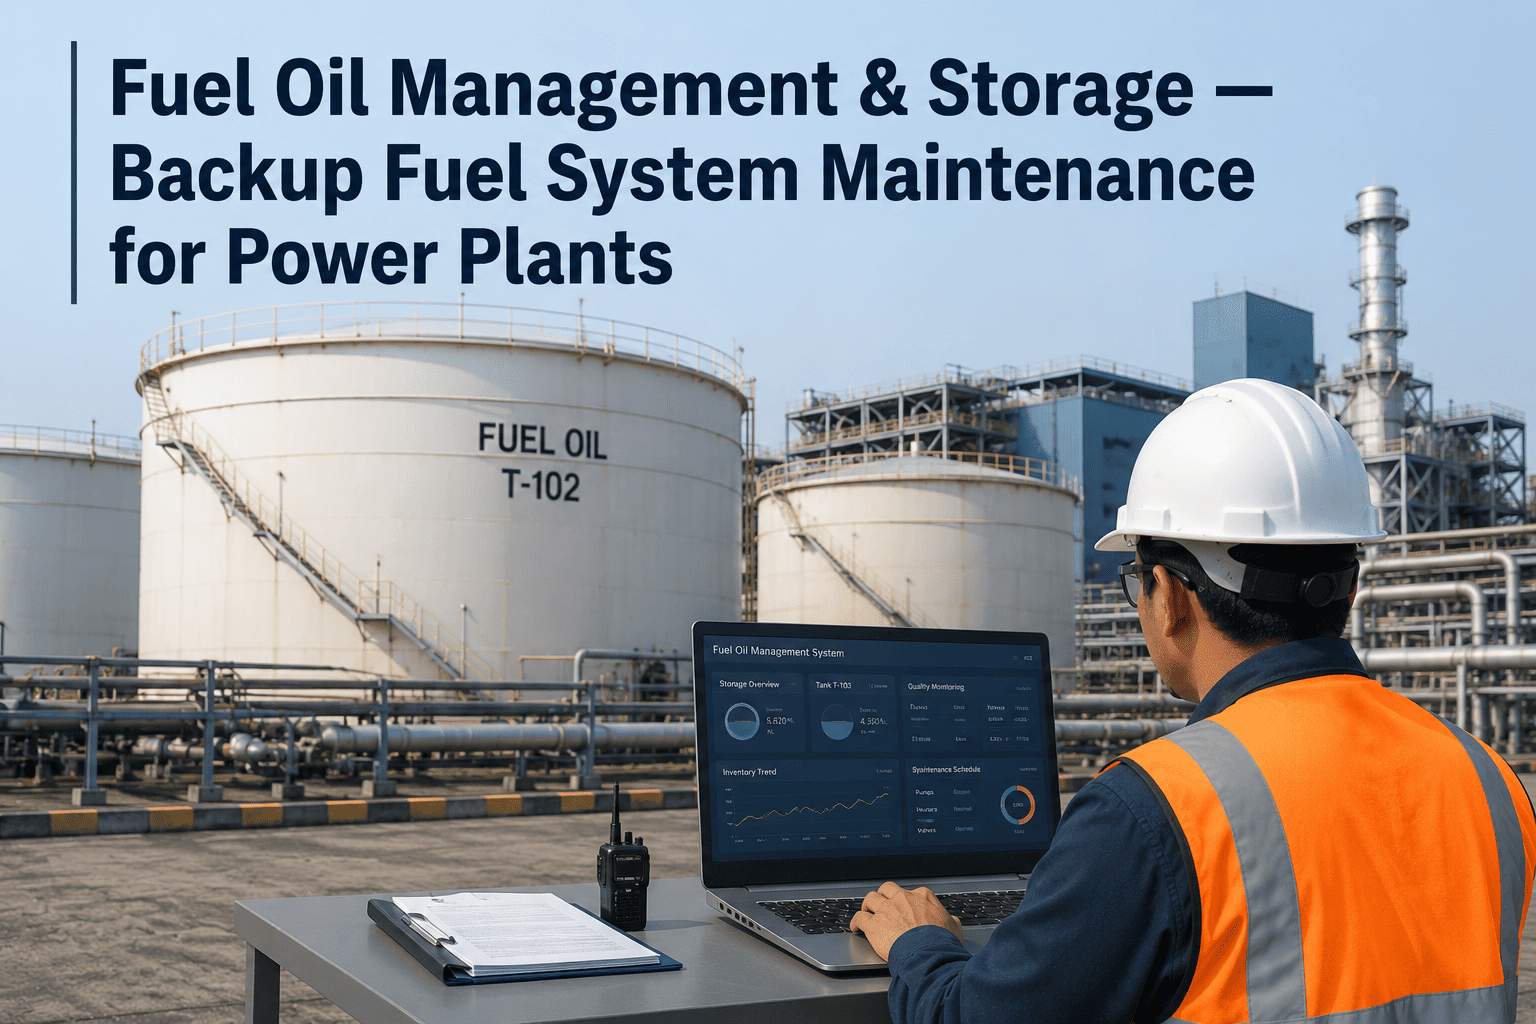
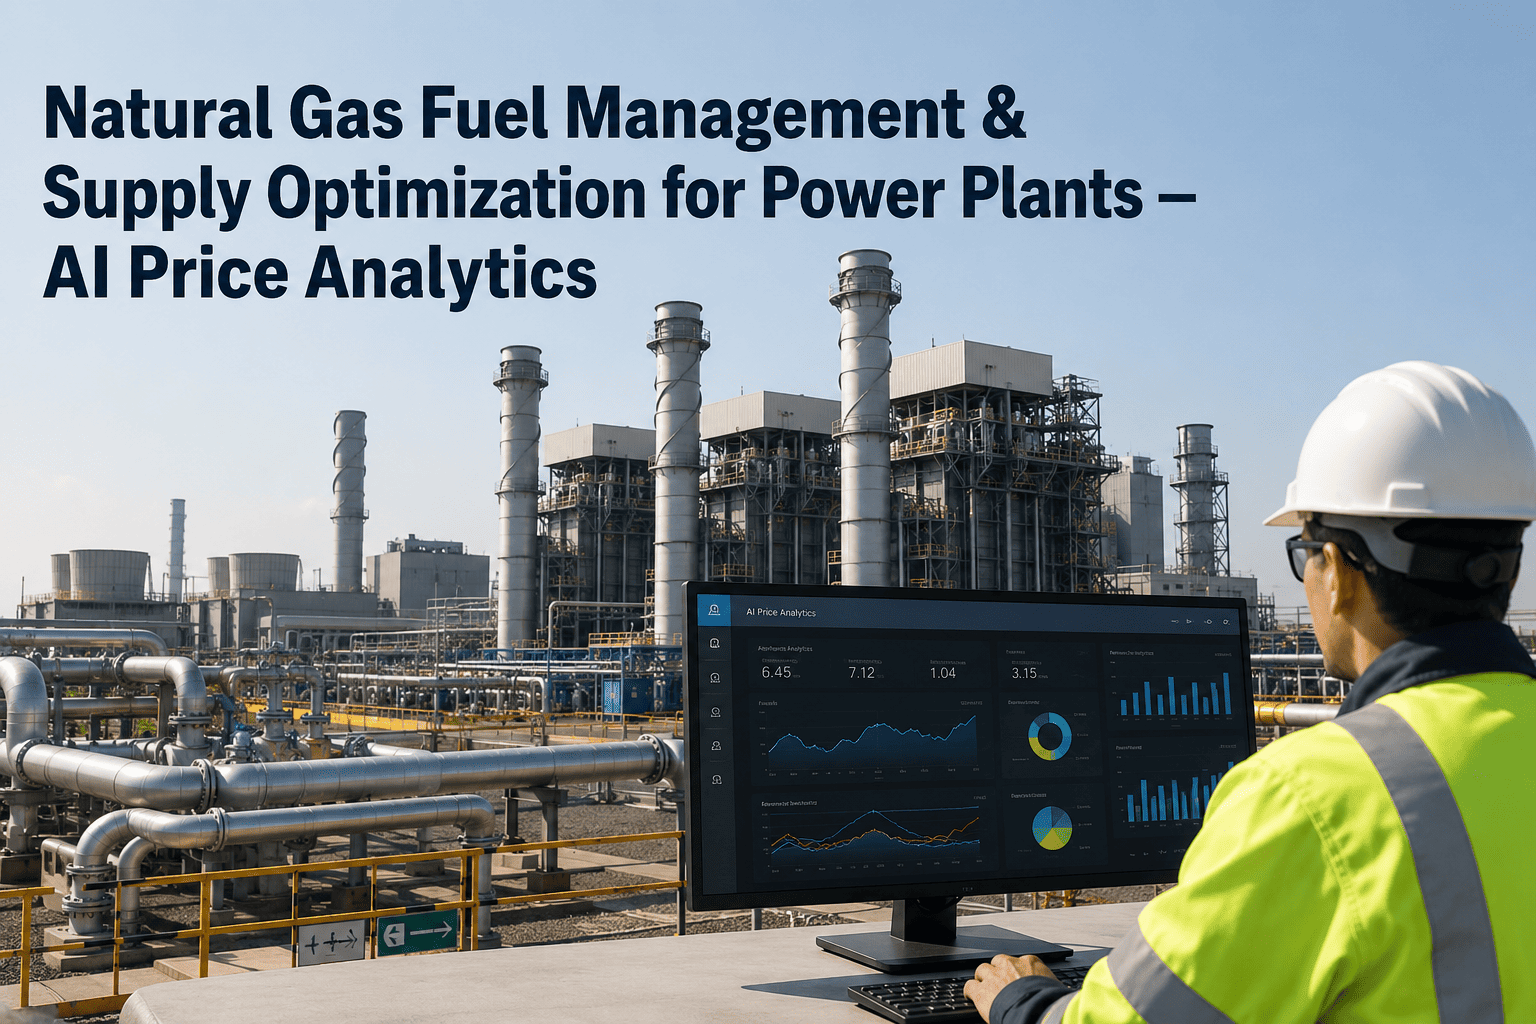
Coal is the longest chain, but it is not the only one. A plant with gas turbines or with fuel oil for start-up and flame support has a fuel cycle for each, and each one limits generation in its own way. The question to ask of each is the same: how long does fuel take to become usable, and what happens when it does not.
Where the Recovered Time Comes From
On the illustrative unit, three steps take a rake from 7 h 50 to 5 h 10. They are listed in the order we would work through them, because each one is easier once the one before it is done. None of them is guaranteed for another plant, and the first benchmark shows which apply to yours.
Remove blocked time: 7 h 50 to 6 h 30
The tippler waits 1 h 20 a rake for a hopper to clear, a feeder to start or a conveyor to be ready. Plotting every wait against its cause usually shows two or three repeat offenders. Hopper level setpoints, feeder sequencing and a clear rule for who restarts a stream after a trip remove most of it.
Run placement checks in parallel: 6 h 30 to 5 h 45
Wagon inspection, sampling, weighing and shunting happen one after another. Preparing the sampling team and the tippler before the rake is placed, and doing inspection while the first wagons are tipping, brings the start forward by 45 minutes.
Tune the tipping cycle: 5 h 45 to 5 h 10
The tip takes 90 seconds, but the effective cycle is 4.3 minutes. Indexing, clamp release, table return and wagon clearance each have a share of the difference. Timing them wagon by wagon shows where it is lost, and tightening that is worth 35 minutes a rake. Beyond this, further gains need layout changes, such as a second tippler or a track hopper with a loop that keeps the locomotive connected.
What the AI Adds for the Fuel Handling Shift
Each of those steps starts from knowing where the time went. iFactory's models run on a GPU server inside the plant and read tippler cycle counts, conveyor run signals, hopper and bunker levels and mill demand together, so nothing leaves the station and nothing is written to the DCS.
- Rake timelines. Every rake is rebuilt from placement to release, with working, waiting and blocked minutes separated.
- Cause ranking. Waiting time is ranked by cause, so the hopper that blocks the tippler every second rake is easy to find.
- Bunker margin. Each bunker's run-down time is compared with the next rake's arrival and its usual time to reach the bunkers.
- Questions in plain language. Operators ask why a rake ran long and get the data, not another report.
Frequently Asked Questions
What is fuel handling cycle time in a power plant?
It is the time fuel takes to move from receipt to the point where the plant can burn it. For coal, that runs from rake placement through tipping, conveying and crushing to the bunkers. For gas it is the conditioning and compression before a turbine can start. For fuel oil it is unloading, heating and transfer to the day tank.
How long does a wagon tippler take to unload a rake?
The tipping operation takes about 90 seconds a wagon, and unloading a whole rake with one tippler in operation typically takes about 4 hours, because positioning, clamping, clearing and waiting add to each tip. A coal rake usually has 55 to 60 wagons. The figure for your siding depends on your tippler, track layout and the state of the downstream plant.
Does fuel handling really limit generation?
Only when the buffers are low, which is why it is easy to miss. Yard stock and bunker level cover slow cycles on normal days. On a day with a late rake, wet coal or a conveyor trip, a slow cycle can leave a mill without coal.
Can cycle time be reduced without new equipment?
Often a good part of it can, because much of the lost time is waiting and sequencing, not machine speed. Removing blocked time and running checks in parallel need no new equipment. Beyond that, a second tippler or a different track layout may be needed, and the timeline shows whether the case for it is real.
Does iFactory change settings in our DCS?
No. It reads signals from your DCS, SCADA and historian, analyses them and proposes changes. Every change to an interlock, setpoint or sequence is made by your engineers in the control system, through your own change process.
How long does deployment take, and what do we need to provide?
A typical unit is live in 6 to 12 weeks. You provide rack space, power, an Ethernet connection, read access to the tippler, conveyor and bunker signals, and an operations contact and a maintenance contact for the pilot. iFactory supplies the pre-configured NVIDIA AI server, software, integration and training. To scope your station, contact our project team.
Know Your Fuel Margin Before the Buffer Runs Out
One turnkey system, with an NVIDIA AI server, fuel cycle analytics, integration and training, delivered and live inside 12 weeks. Start with the unit whose bunkers get low before the next rake arrives.
- 1Hours from rake placement to release
- 2Effective minutes per wagon on the tippler
- 3Minutes the tippler waited, blocked or starved, per rake
- 4Hours of bunker buffer at each shift change
- 5Hours each bunker spent below its low level