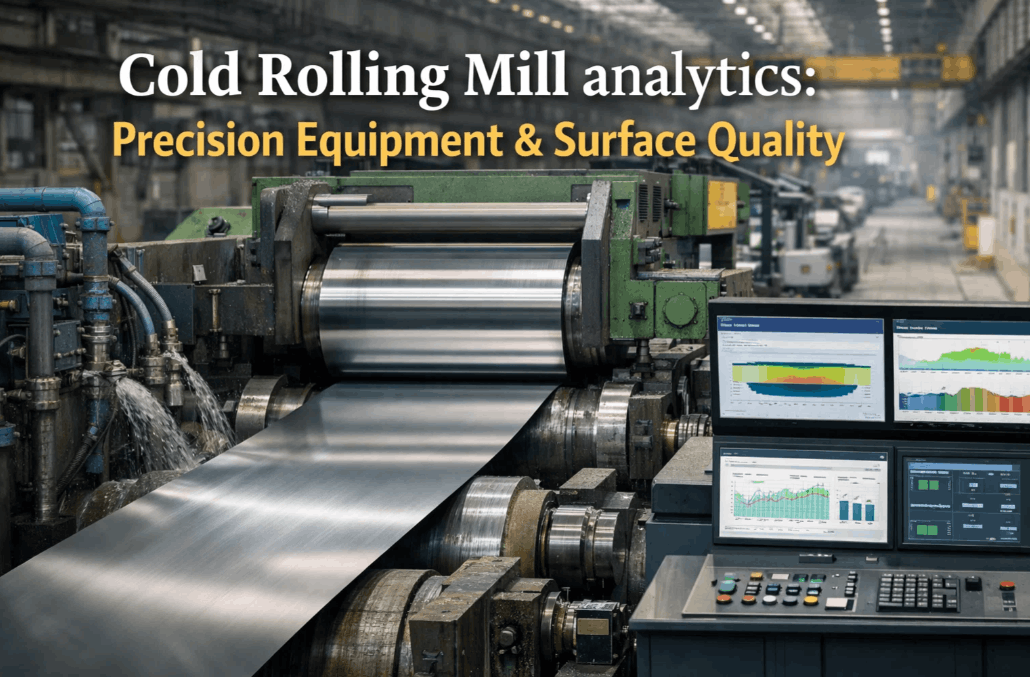
In the ultra-precision world of steel finishing, Cold Rolling Mill (CRM) Analytics represents the final frontier of quality integrity. Unlike hot rolling, where bulk reduction is the goal, cold rolling demands micron-level Thickness Gauge Calibration, intense Inter-stand Tension Control, and flawless Flatness Management (Shape Control). As strip thickness reaches sub-millimeter levels, the margin for error vanishes. A single millisecond of hydraulic instability or a 5% deviation in tension can lead to catastrophic strip breakages or surface chatter marks that render entire coils scrap. For Technical Directors and Quality Managers, transitioning from reactive monitoring to AI-driven predictive analytics is the only way to meet the rigorous surface standards required by the automotive, aerospace, and high-end appliance sectors.
What Are Cold Rolling Mill Analytics?
Cold Rolling Mill Analytics is the high-frequency data framework used to manage the complex interplay between mill speed, hydraulic force, and strip tension. In a Tandem Cold Mill (TCM) or a Reversing Cold Mill (RCM), the physical properties of the steel are transformed through work hardening, necessitating a sophisticated Automatic Gauge Control (AGC) system. Analytics in this context involves the real-time processing of signals from load cells, X-ray thickness gauges, and tensiometer rolls to maintain a steady-state production environment. Every CRM operator must move beyond basic SCADA views to understand the "Digital Signature" of their mill's performance.
The core of CRM excellence lies in Flatness Control—measured in I-units—which ensures the strip is perfectly flat across its entire width. If your facility processes high-strength low-alloy (HSLA) or stainless steels, the roll force required can exceed 2,000 tons, making Hydraulic Gap Analytics a critical safety and quality requirement. Schedule a technical audit to see how AI optimizes your CRM stand settings.
Understanding CRM CTEs: Critical Tracking Events in Cold Finishing
Critical Tracking Events (CTEs) in the cold mill are the high-frequency moments where gauge, tension, and surface data must be synchronized. For mill engineers, the most significant CTEs include:
Entry Coil Threading & Welding
The point where the head-end of the coil enters Stand 1. Analytics must capture weld integrity and entry tension ramping. Improper threading accounts for 30% of head-end scrap; iFactory optimizes the "Thread-to-Run" transition logic.
Active Stand Reduction (AGC)
The real-time adjustment of the work roll gap using hydraulic cylinders. Required data elements include roll force, motor torque, and entry/exit gauge measurements. iFactory's AI tunes the AGC gain parameters to eliminate thickness "flutter."
Inter-stand Tension Management
The maintenance of specific tension levels between stands to ensure strip stability and prevent "folding." Analytics correlate tensiometer roll feedback with mill speed to predict and prevent strip breakages before they occur.
Shape Control & Flatness Sensing
The active monitoring of strip flatness using segmented shape rolls. This CTE is where roll bending and cooling headers are adjusted. iFactory provides real-time "Heat Map" views of strip flatness for the entire coil length.
Exit Reel & Surface Inspection
The final winding and automated surface inspection (ASIS). Data elements include surface defect classification, coil weight, and exit tension. Book a demo to see how exit-end analytics validate the entire mill process.
Key Data Elements (KDEs): What Your CRM Records Must Capture
Key Data Elements in a cold mill are high-velocity streams that must be linked to specific coil segments. The practical challenge is not just capturing the data, but correlating it across multiple stands and passes to identify the root cause of a quality deviation. Book a demo to see how iFactory maps KDE capture to your CRM's PLC and X-ray systems.
| CRM Component | Required Technical KDEs | AI Calibration Available? | Quality Impact |
|---|---|---|---|
| Mill Stand | Roll Force, Hydraulic Gap Pos, Motor Torque, Roll Speed | Yes — AGC Tuning | Thickness Precision |
| Tension Reel | Tension Setpoint, Actual Tension, Coil Build-up Ratio | Yes — Break Prevention | Strip Stability |
| Shape Roll | Segmental Tension, I-Units, Roll Bending Pressure | Yes — Flatness Loop | Strip Flatness |
| Thickness Gauge | X-Ray Intensity, Calibration Offset, Gauge Head Position | Yes — Drift Compensation | Reject Reduction |
| ASIS System | Defect Type, Defect Size, Defect Location (X/Y) | Yes — Defect Prediction | Surface Yield |
The Critical Role of Hydraulic Gap Control & AGC Stability
In a high-speed Tandem Mill, the Automatic Gauge Control (AGC) system must react within milliseconds to compensate for incoming hot-band gauge variations and roll eccentricity. A modern CRM analytics system doesn't just monitor the gap; it uses Feed-forward Analytics to predict the required force adjustment before the strip even enters the next stand. If your mill relies on manual gain tuning, you are likely sacrificing 2-3% of your yield to "Out-of-Gauge" material during speed changes.
The 24-hour audit standard for automotive steel demands that you can produce a "Thickness Map" for any coil delivered. iFactory ensures that every micron of material is documented and searchable, allowing you to prove compliance with the most stringent customer specs. Book a demo to see iFactory's high-speed data archival in action.
A strip breakage in a Cold Rolling Mill (often caused by tension surges or edge cracks) is a high-cost event. Beyond the $25,000 cost of work roll damage, the downtime for mill cleanup can exceed 4 hours. iFactory's tension analytics engine monitors the "Tension Variance Signature" and triggers an emergency mill ramp-down if the breakage risk exceeds 90%, effectively eliminating unplanned mill crashes.
AI-Driven Surface Quality: How Technology Closes the Yield Gap
Manual surface inspection and legacy ASIS systems fail modern finishing on three fronts: they cannot classify complex defects in real-time, they cannot correlate surface marks back to a specific work roll stand, and they cannot predict defect trends across multiple coils. iFactory's AI-driven CRM module addresses these failure points through deep-learning vision and multi-stand correlation.
Real-time AGC Self-Tuning
Integrated with high-speed gauge feedback, AI models automatically adjust AGC gains for different material grades and mill speeds — maintaining ±0.2% precision during acceleration and deceleration phases.
Shape-to-Roll Force Correlation
The platform correlates strip flatness (I-Units) with individual roll bending pressures across all stands — identifying the exact stand responsible for "Wavy Edges" or "Center Buckles" instantly.
Thickness Gauge Calibration Watch
Automated monitoring of X-ray gauge drift ensures your measurements are always valid. The system alerts technicians if calibration constants deviate from historical norms, preventing "Invisible Rejects."
Predictive Surface Defect Identification
By correlating mill vibration and roll history with exit-end surface cameras, iFactory identifies the signature of a "Roll Mark" before it manifests as a rejected coil, allowing for an immediate roll change.
Cold Rolling Performance Gaps: Where Mills Are Most at Risk
Based on industry analysis of CRM technical readiness, the following performance gaps appear most frequently in facilities approaching their digital modernization deadline.
Customer Testimonial: Cold Mill Transformation
"Since deploying iFactory CRM Analytics, our strip breakage rate has dropped by 80%. The ability to see tension stability and AGC precision in real-time has fundamentally changed how we run our tandem mill. We're now producing automotive-grade material at speeds we never thought possible."
Building a CRM Digital Roadmap: A Step-by-Step Approach for Technical Directors
For CRM engineers leading their organization's digitalization, the roadmap has five operational phases. Each phase provides a foundation for the next, moving from basic data capture to fully autonomous mill control.
Data Backbone Integration (PLC & Gauge)
Connect all mill stand PLCs, X-ray thickness gauges, and tensiometer rolls to a high-frequency data historian (100Hz+). Ensure data is time-stamped and synchronized across all stands. Output: a unified CRM data stream.
AGC & Tension Gap Analysis
Compare your current gauge and tension variability against global benchmarks. Identify stands with high eccentricity or slow hydraulic response times. Output: a prioritized hydraulic and control system upgrade register.
Real-time Thickness Mapping
Deploy automated thickness and flatness "Genealogy" tools that link gauge data to specific coil IDs. Enable instant search for out-of-spec segments. Output: a searchable coil quality digital library.
AI Predictive Model Training
Train deep-learning models on historical strip breakage and surface defect data. Deploy "Early Warning" alerts for tension surges and roll marks. Output: a predictive quality and safety layer.
Autonomous Control & Optimization
Implement closed-loop AI control for AGC gains and roll bending pressure. Allow the system to optimize mill speed for maximum yield vs. risk. Output: a fully autonomous, audit-ready Cold Rolling Mill.
Frequently Asked Questions: Cold Rolling Mill Analytics
What is the difference between Tandem and Reversing Mill analytics?
Tandem mill analytics focus on inter-stand synchronization and high-speed gauge control, whereas Reversing Mill (RCM) analytics prioritize pass-by-pass reduction schedules and tension ramping during direction changes. iFactory supports both architectures with specialized models.
How does AI improve Thickness Gauge Calibration?
AI monitors the "Detector Drift" of X-ray gauges by comparing results with known sample standards and downstream physical measurements. It identifies calibration decay before it causes rejects, a process we call "Predictive Calibration."
Can CRM analytics prevent all strip breakages?
While no system can prevent 100% of breakages, AI can eliminate those caused by tension surges, improper mill ramping, and edge-crack propagation—which typically account for 85% of total CRM breakages.
What is "I-Units" in flatness measurement?
An I-Unit is a dimensionless measure of strip flatness (10^-5 strain). High-end automotive steel usually requires flatness < 5 I-U. iFactory's analytics track this live to ensure every coil meets the shape target.
Does iFactory integrate with existing ASIS (Surface Inspection) systems?
Yes. We ingest the raw defect logs from legacy inspection systems and use AI to correlate those defects with mill parameters like roll force and lubricant concentration to find the root cause.
How does mill speed impact gauge precision?
At higher speeds, hydraulic response and lubrication dynamics change. iFactory's AI-driven AGC adjusts parameters dynamically based on mill speed, ensuring thickness remains stable even at 1,800 mpm.
What is "Hydraulic Gap Hysteresis" and how is it managed?
Hysteresis is the lag in hydraulic response during roll gap changes. iFactory's analytics model this behavior and use "Anticipatory Logic" to send gap commands that compensate for the mechanical lag.
How long does it take to implement CRM Analytics?
A standard CRM deployment takes 10–16 weeks, including high-speed data integration, AGC baseline modeling, and training of the surface defect correlation engine.