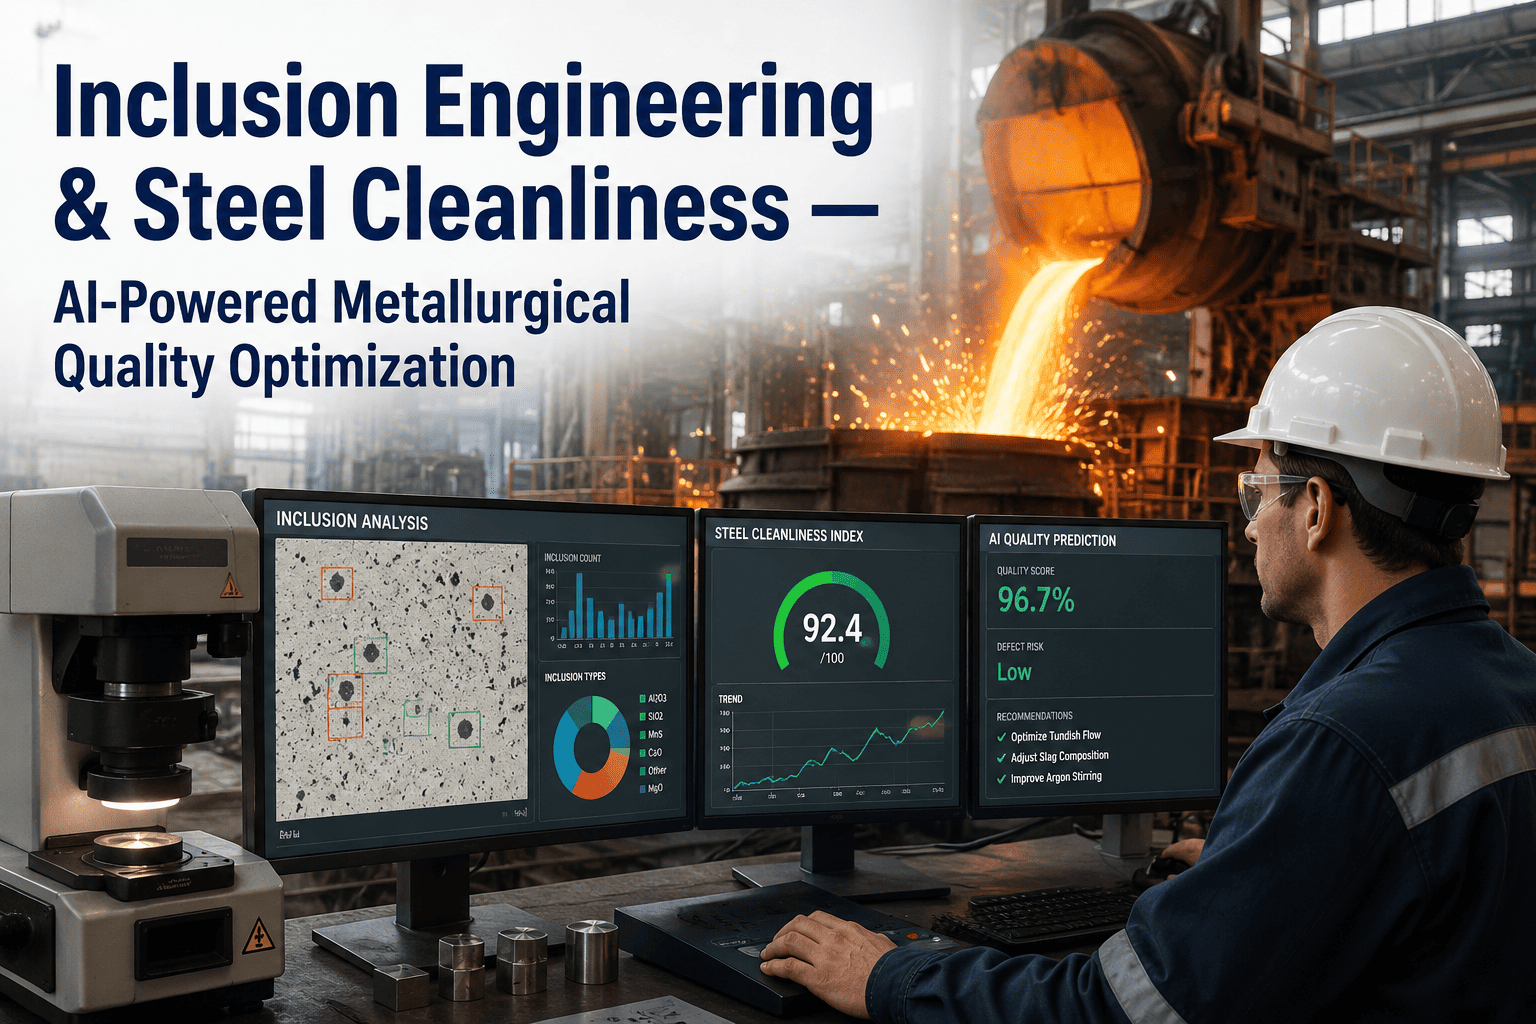
A bearing steel heat can pass every chemistry check on the ladle analysis and still fail a customer's rotary fatigue test months later, because the failure wasn't caused by what element was present but by what shape and size the non-metallic inclusions took as the steel solidified. Inclusion engineering — the deliberate control of inclusion type, morphology, and size distribution rather than simply their total volume — is one of the few areas of steelmaking where getting the chemistry right isn't the same as getting the product right. This piece covers how inclusion control actually works across secondary metallurgy and casting, why bulk oxygen content alone is a poor proxy for cleanliness, and how a demo can walk through inclusion trend data against your current customer rejection history.
Why Total Oxygen Content Is an Incomplete Cleanliness Measure
Total oxygen content has been used as a cleanliness proxy for decades because it's relatively simple to measure and correlates loosely with overall inclusion volume, but two heats with identical total oxygen readings can behave completely differently in a fatigue-critical application depending on whether their inclusions are small, well-dispersed, and globular, or larger, clustered, and angular. Angular alumina-type inclusions concentrate stress in a way that globular calcium-aluminate inclusions of similar size generally don't, which means morphology control — not just volume reduction — is what actually determines whether a bearing or automotive-grade steel performs in service.
This is exactly where inclusion engineering diverges from simple cleanliness control: the goal isn't zero inclusions, which isn't achievable in conventional steelmaking, but rather steering inclusion chemistry through calcium treatment and slag design so that whatever inclusions remain are the least harmful type and shape for the specific application the steel is destined for.
Where Inclusion Control Actually Happens
Inclusion engineering isn't a single-step process — it's a sequence of decisions made across secondary metallurgy and casting, each of which shapes the final inclusion population differently. Deoxidation practice sets the initial inclusion type formed. Calcium treatment modifies alumina inclusions toward the softer, more globular calcium-aluminate form that's generally less harmful to fatigue performance. Slag composition and ladle stirring practice govern how effectively inclusions that do form are able to float out before casting. And tundish and mold flow control during casting determine how many of the remaining inclusions get entrained back into the solidifying steel rather than removed.
| Process Stage | Primary Inclusion Control Lever |
|---|---|
| Deoxidation | Determines initial inclusion type (alumina, silica, or complex oxides) formed |
| Calcium treatment | Modifies alumina inclusions toward less harmful calcium-aluminate morphology |
| Ladle stirring / slag design | Governs float-out efficiency of inclusions before casting begins |
| Tundish and mold flow control | Determines re-entrainment risk of remaining inclusions during casting |
Why Removal Efficiency Is Harder to Track Than It Sounds
Inclusion removal efficiency — the share of inclusions formed during deoxidation that successfully float out before casting rather than remaining trapped in the final product — is influenced by stirring energy, ladle residence time, and slag viscosity in ways that interact rather than acting independently. Increasing stirring energy improves float-out up to a point, but excessive stirring can also re-entrain slag into the steel or damage refractory in ways that introduce new inclusion sources, which means removal efficiency isn't simply a matter of stirring harder or longer.
Connecting Process Data to Customer-Facing Quality Outcomes
The practical challenge most process engineers face isn't a lack of process data — most secondary metallurgy and casting operations already log stirring parameters, calcium treatment additions, and slag composition — it's connecting that process data back to actual inclusion outcomes at the level of an individual heat, and then connecting those outcomes forward to which customer applications each heat is best suited for. Without that connection, inclusion control decisions get made against general best practice rather than against what's actually happening heat to heat, and a heat with borderline morphology can end up allocated to a fatigue-critical order it was never well suited for.
What This Means for a Process Engineer's Daily Decisions
In practice, this shifts inclusion control from a set of fixed recipes applied uniformly across grades toward a decision made per heat, informed by how that heat's actual measured or predicted inclusion characteristics compare against the requirements of the specific order it's destined for. A heat trending toward slightly higher inclusion count but excellent morphology might still be well suited for a bearing-grade order, while a heat with lower total count but poor morphology control might need to be reallocated to a less demanding application instead of risking a customer rejection.
It also strengthens the case a process engineer can make when a customer disputes a cleanliness-related rejection. Rather than relying on aggregate chemistry data that doesn't speak to morphology, having the actual inclusion characterization data for that specific heat available gives a defensible, specific answer about what happened and why.