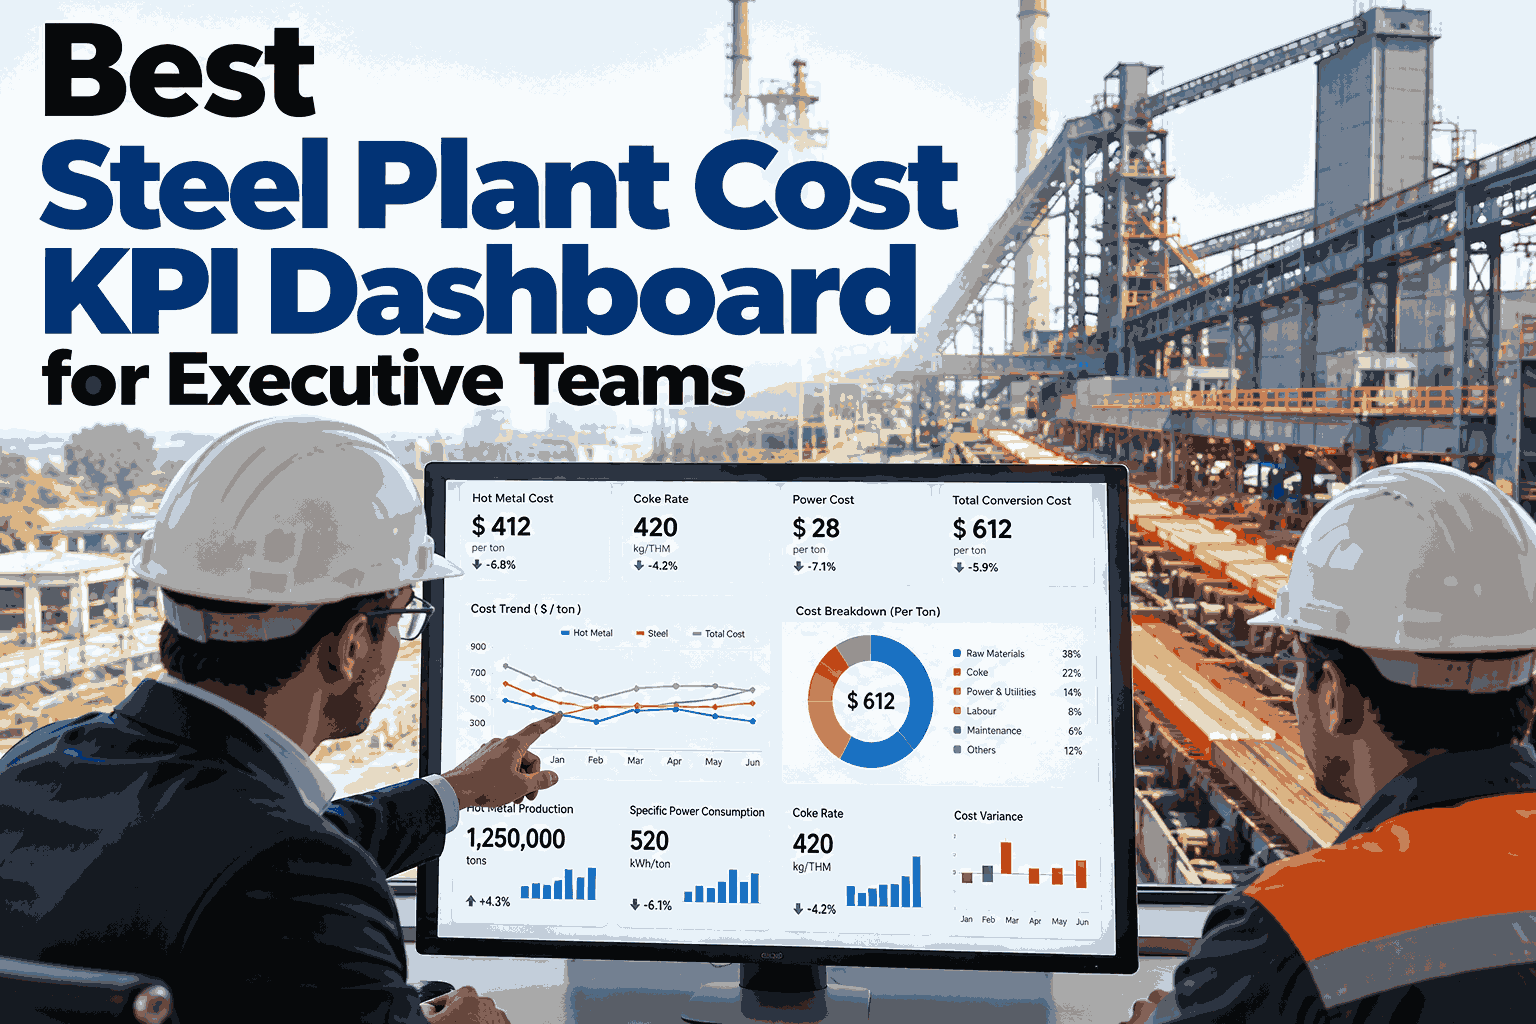
Every works manager has sat in a review where cost per tonne moved and nobody could say why. The total is easy to read, but the reasons sit across hot metal, refractory, electrodes, alloys and utilities, each owned by a different team and reported on a different day. Cost driver analysis breaks the single number into buckets and follows each bucket down to the heat, shift or asset behind it. Plants that want that view without a month-end scramble can ask the iFactory AI team to review their cost data before the next budget cycle.
Find Out Why Cost Per Tonne Moved, Not Just That It Did
iFactory AI splits steel plant cost into hot metal, refractory, electrode, alloy and utility buckets, then drills each one down to the root cause a works manager can act on.
What Sits Inside One Tonne of Steel
Cost per tonne is a stack, not a single figure. The chart below shows an illustrative mix for a mid-sized plant, and every site will look different, but the shape is familiar: a few buckets carry most of the weight.
The Five Buckets a Works Manager Owns
Each bucket has its own physics and its own usual suspects. Knowing them in advance is what makes a drill-down fast.
Hot Metal and Ferrous Charge
Driven by hot metal ratio, scrap mix, yield and metallic loss. A slightly worse charge mix or a slag carry-over shows up here first.
Refractory
Tracks lining life per heat, gunning frequency and early relines. Cost per tonne climbs when campaign life quietly shortens.
Electrodes
In electric arc shops, graphite consumption per tonne follows power-on time, breakage events and furnace practice.
Alloys
Depends on grade mix, recovery and overshoot against aim chemistry. Over-alloying is cheap to fix once it is visible.
Utilities
Power, oxygen, nitrogen, argon, gas and water, each with its own consumption pattern and idle loss.
The Drill-Down Ladder
A variance is only useful when it ends at something a person can change. The ladder below shows the four steps every driver should climb.
See Your Own Cost Buckets Drilled to Root Cause
Book a 30-minute session and bring one month of cost and heat data. iFactory AI will show where the variance actually came from.
Drivers, Signals and First Actions
Use this table as a quick reference when a bucket moves. It pairs the common driver with the signal to check and the first move to make.
| Bucket | Typical Driver | Signal to Check | First Action |
|---|---|---|---|
| Hot metal | Charge mix drift | Yield and metallic loss per heat | Compare charge recipe against aim |
| Refractory | Shorter lining life | Heats per campaign, gunning count | Review slag practice and tap temperature |
| Electrodes | Breakage or long power-on | Kg per tonne by furnace and crew | Inspect handling and column practice |
| Alloys | Overshoot on chemistry | Added versus aim by grade | Tighten addition model and recovery figures |
| Utilities | Idle and off-peak losses | Consumption per tonne by shift | Trace idle draw between heats |
Two Views of the Same Month
Most plants report cost by department. A driver view reports it by cause. The difference decides how quickly a manager can respond.
A Composite Scenario: The Month Nobody Could Explain
A mid-sized electric arc plant saw cost per tonne rise against budget for two months running. Finance blamed raw material prices, while operations blamed grade mix, and neither explanation matched the heat records.
A Review Rhythm That Keeps Costs Honest
Analysis only pays when it becomes routine. This cadence gives every bucket an owner and a deadline.
Where iFactory AI Fits
Building this by hand means chasing spreadsheets from five departments. iFactory AI pulls the data together and keeps the drill-down current.
Live Cost Per Tonne
Cost is rebuilt as heats close, so the number a manager sees is never a month old.
One-Click Drill-Down
Move from total variance to bucket, unit, shift and heat without opening another report.
Driver Ranking
Buckets are ranked by their contribution to the gap, so attention goes where it matters.
Shared Across Teams
Operations, maintenance and finance read the same figures and stop arguing over versions.
Frequently Asked Questions
Which cost bucket should we analyze first?
Start with the bucket that contributed most to last quarter's variance, not the one with the largest share of total cost. Large buckets like hot metal or ferrous charge tend to be stable, while smaller ones such as alloys, electrodes and refractory swing far more from month to month. Ranking buckets by their contribution to the gap tells you where one hour of review pays back the most. It also stops the team from spending weeks on a bucket that was never the problem. iFactory AI's team can rank your buckets from a sample of your heat and cost data.
Do we need new sensors to run driver analysis?
Usually not. Most plants already hold heat records, consumption logs and cost data in ERP, MES or Level 2 systems, and the real work is joining them so a cost line links back to the heat behind it. Metering gaps do exist, especially for utilities like compressed air or water by section. The sensible approach is to run the first drill-downs on existing data, see which gaps actually block a root-cause answer, and add metering only where it changes a decision.
How is this different from our monthly cost report?
A monthly report tells you what was spent, and it arrives after the period has closed. By then the furnace practice, crew or grade mix that caused the variance has often changed. Driver analysis explains why a number moved and refreshes as heats complete, so a manager can correct course during the month instead of explaining it afterwards. Finance and operations also read the same figures, which removes the version arguments. See a live comparison in a short walkthrough using your own figures.
Does it work for both integrated and electric arc plants?
Yes, although the buckets weigh differently. Integrated plants lean on hot metal, coke, blast furnace practice and converter refractory, while electric arc shops lean on scrap mix, electrodes and power. The drill-down ladder from total variance to bucket, unit and root cause stays the same in both. Bucket definitions, cost centers and heat identifiers are mapped during configuration so the views match your route, your product mix and the way your teams already talk about cost.
Who should own each bucket?
Assign one owner per bucket, ideally the person who controls the practice behind it, such as the melt shop lead for electrodes, the maintenance head for refractory and the energy manager for utilities. Finance supports with the numbers but should not own the explanation. Each owner then brings one variance and one agreed action to the weekly review, which keeps accountability visible. Support can share a sample ownership matrix that plants adapt to their own structure.
Turn Cost Per Tonne Into Something You Can Act On
iFactory AI shows which bucket moved, on which shift, and why. Book a walkthrough to see it against your own heat and cost data.