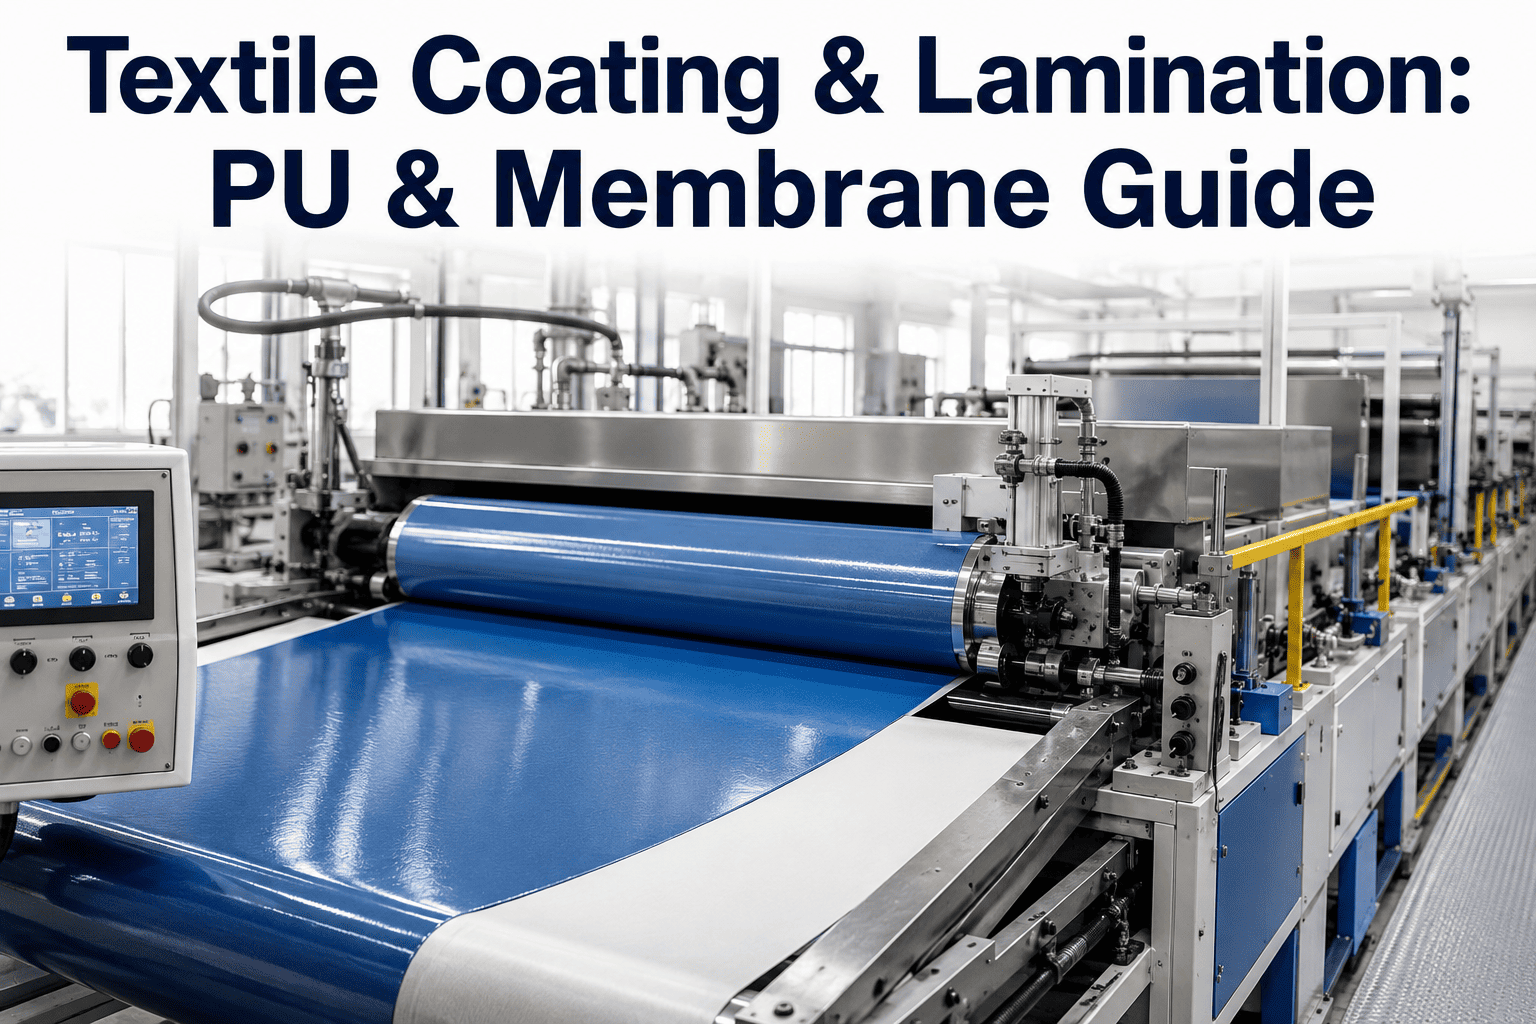
A waterproof jacket that leaks at the seams or a tent fabric that traps condensation instead of breathing usually isn't a design failure, it's a coating weight or lamination bond that drifted somewhere on the line and nobody caught it before the roll shipped. PU coating, PVC lamination, and PTFE membrane bonding all depend on precise, consistent control of thickness, temperature, and bond pressure across the full fabric width, and a variance of even a few grams per square meter can be the difference between a garment that performs in the rain and one that doesn't. AI-monitored coating and lamination lines catch that variance across the width in real time rather than relying on a spot check every few hundred meters. Process teams can Book a Demo to see width-wise coating weight tracked live against target.
Catch a Coating Weight Drift Before the Roll Ships.
iFactory tracks coating weight and lamination bond quality across the full fabric width, flagging drift before it reaches a finished order.
Why Coating Weight Drifts Across a Fabric's Width
A knife-over-roll or gravure coating head is set once at a target thickness, but the actual deposit varies across the width for reasons that have nothing to do with the initial setting. Roller wear, uneven fabric tension across the width, and viscosity changes in the coating compound as a batch ages all shift the amount of material actually reaching the fabric surface.
A spot check taken at one point across the width, once every few hundred meters, simply cannot catch a gradual edge-to-center variance that develops slowly across a production run. By the time a lab sample flags an out-of-spec coating weight, an entire order may already be rolled, cut, and partly sewn into finished garments before anyone knows the waterproof rating is compromised.
What Each Layer of a Functional Fabric Actually Does
A finished waterproof-breathable fabric is rarely a single material. It's a bonded stack where each layer contributes a specific property, and a defect in any one layer compromises the whole garment's performance.
Provides abrasion resistance, appearance, and the surface the coating or membrane bonds to.
Bonds the membrane to the face fabric without blocking the membrane's breathability.
Delivers the actual waterproof and breathable barrier through microporous or hydrophilic structure.
Protects the membrane from abrasion on the inside face and improves garment drape.
PU Coating vs. PVC Lamination vs. PTFE Membrane Bonding
| Factor | PU Coating | PVC Lamination | PTFE Membrane |
|---|---|---|---|
| Breathability | Moderate to high | Low | Very high |
| Typical application | Rainwear, bags | Tarpaulin, tents | Outdoor apparel |
| Bond method | Direct coating | Heat/pressure laminate | Adhesive dot lamination |
| Key control variable | Coating weight (gsm) | Roll temperature & pressure | Adhesive dot coverage |
Tracking Weight and Bond Quality Across the Full Width
Rather than relying on periodic manual sampling, continuous monitoring builds a live map of coating weight and bond quality across the entire fabric width as it runs.
Width-Wise Weight Sensing
Sensors positioned across the fabric width continuously measure coating weight rather than relying on a single center-line reading.
Thermal & Pressure Tracking
Roll temperature and nip pressure are logged continuously for lamination processes, correlating directly with bond strength results.
Vision-Based Bond Inspection
Camera inspection flags delamination, bubbling, or adhesive dot gaps that a manual spot check would likely miss.
Real-Time Alerting
Operators are alerted the moment a width position drifts outside the target range, before further meters run out of spec.
What Finishing Lines Report After Rollout
Reduction in rolls flagged for out-of-spec coating weight or bond strength after continuous monitoring is deployed.
Typical reduction in coating compound usage once over-application on out-of-spec sections is eliminated.
Of the fabric width tracked continuously instead of a single center-line spot check.
Adding Monitoring to an Existing Coating or Lamination Line
Sensors and cameras are added to the existing coating head or laminator without requiring a line rebuild. Baseline data is collected across normal production for a few weeks to establish what a good run actually looks like for each product recipe, and alert thresholds are then tuned against those baselines before full-width tracking goes live. Most lines are fully monitored within four to six weeks from installation.
Textile Coating & Lamination Monitoring — Common Questions
Can the same sensors work across PU coating and PVC lamination processes?
Yes, though the specific parameters tracked differ between the two. PU coating monitoring focuses primarily on coating weight and viscosity-related deposit variation, while PVC lamination adds roll temperature and nip pressure as key variables that directly affect bond strength. Both can run on the same monitoring platform with process-specific configurations.
How is coating weight actually measured without contacting the wet coating?
Non-contact sensing methods measure the coating layer's thickness or mass per area without touching the still-wet compound, which avoids disturbing the coating or introducing a contamination risk. This allows continuous measurement across the full width while the coating head is running at normal line speed.
Does width-wise monitoring catch problems a center-line-only check would miss?
Yes, edge-to-center variance is one of the most common coating defects and is exactly what a single center-line reading is structurally unable to detect. Full-width sensing is what actually surfaces this pattern, since the variance often shows up gradually at the edges long before the center-line reading shows any deviation at all.
What happens when a bond quality issue is detected mid-run?
The system flags the affected roll length and width position immediately so the section can be marked for downstream inspection or rework rather than being discovered only after cutting and sewing. Teams can review integration options with existing quality systems through iFactory Support.
How long does a pilot deployment take on one coating line?
A pilot typically runs for four to six weeks, covering sensor installation, baseline collection across the normal product recipe mix, and validation of at least one real drift catch against lab results. Teams ready to scope a pilot can Book a Demo to review a comparable line's rollout.
Bring Your Coating Line Under Continuous Watch.
Talk to iFactory about tracking coating weight and bond quality across your finishing floor, edge to edge.