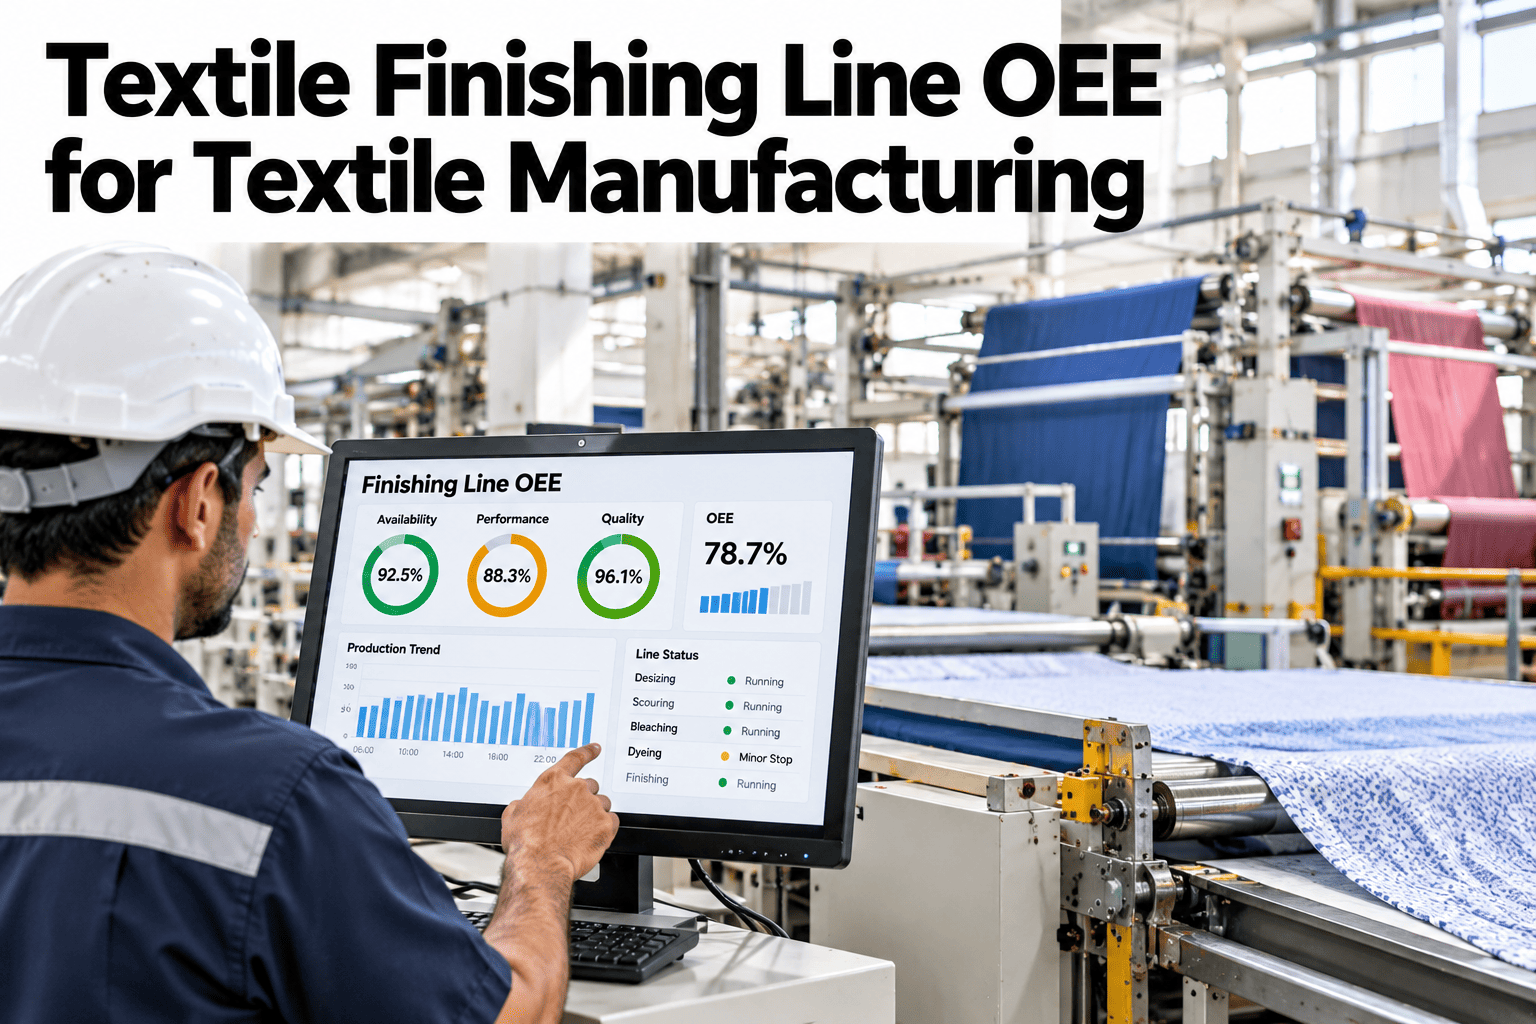
A finishing line running at a comfortable-looking speed can still be losing a third of its potential output, and the reason rarely shows up in a single number. OEE on a finishing line breaks down into three distinct losses: time lost to stops, speed lost running below rated capacity, and output lost to quality rejects, and a mill tracking only one of the three gets a misleading picture of where the real opportunity sits. A line with excellent uptime but chronic underspeed looks fine on a stop report while quietly losing more output than a line with occasional stops running at full rated speed. Breaking OEE into its three components, tracked continuously, shows exactly where the loss is and what to fix first. Finishing teams rethinking this view can see their own finishing line OEE broken into speed, stops and quality live before the next improvement cycle.
Textile Finishing Line OEE for Textile Manufacturing
Speed, stops and quality losses broken out individually, not blended into one misleading number.
Why One OEE Number Hides the Real Problem
A blended OEE figure can look acceptable while one of its three components quietly drags it down.
A line can have strong uptime and quality while chronically running below rated speed.
Teams often chase visible stops while a bigger speed or quality loss goes unaddressed.
Without the breakdown, it is unclear which of the three losses to tackle first.
Breaking the number into availability, performance and quality shows exactly where the opportunity actually sits.
Reading the Three Components
Each component answers a specific question about where output is being lost.
| Component | What It Measures | Common Cause on a Finishing Line |
|---|---|---|
| Availability | Time running versus time scheduled | Changeovers, mechanical stops, material waits |
| Performance | Actual speed versus rated speed | Running below rated speed for fabric type or width |
| Quality | Good output versus total output | Rejects from shade, width or finish defects |
Break Your Own Line's OEE Into Its Three Parts
Book a 30-minute session and bring your current OEE data. iFactory AI will break it into availability, performance and quality live.
Prioritizing the Fix
Once the breakdown is visible, prioritizing improvement effort follows a consistent approach.
What iFactory AI Supports
All three components are tracked continuously and broken down together, not calculated separately after the fact.
Three-Component Breakdown
Availability, performance and quality are tracked and displayed separately, not blended.
Continuous Tracking
All three update continuously as the line runs, not from a periodic manual calculation.
Fabric and Shift Breakdown
Each component can be filtered by fabric type and shift to find where the gap concentrates.
Priority-Ranked Gaps
The component with the largest opportunity is surfaced automatically for the team to act on.
iFactory AI connects to existing finishing line data sources. Scope covers data integration, OEE model setup, team training and ongoing support.
Expert Review
Performance loss is the component finishing teams most consistently underestimate. Mills tend to track stops closely because they are visible and disruptive, while a line quietly running ten or fifteen percent below rated speed for a given fabric type goes unaddressed because nothing visibly stopped.
Filtering the breakdown by fabric type and shift, rather than looking only at the line-wide average, is usually what reveals where the real opportunity sits. A gap that looks modest on average can be significant concentrated on one shift or one difficult fabric.
Frequently Asked Questions
How is rated speed determined for different fabric types?
Rated speed is typically set per fabric type and construction based on established process parameters, since a heavier or more delicate fabric runs at a different speed than a standard fabric. The performance calculation uses the correct rated speed for whatever fabric is currently running. See rated speed configuration in a live session.
Does this require new sensors on the finishing line?
Most finishing lines already have speed and stop data available from the line controller, which is usually sufficient for the availability and performance components. Quality data typically comes from existing inspection records. Ask support about your current data sources.
How often should the OEE breakdown be reviewed with the team?
A weekly review is common for tracking whether improvement effort on the prioritized component is actually closing the gap, with a daily glance useful for catching sudden shifts. Request a sample review cadence for your production meeting.
Can this breakdown be compared across multiple finishing lines?
Yes, each component can be compared across lines to see whether one line consistently underperforms in a specific component, which often points to a line-specific equipment or setup issue rather than a general process problem. Contact support about multi-line comparison.
How long before the breakdown is accurate enough to act on?
Most lines have a reliable breakdown within five to eight weeks of connecting data, enough time to validate rated speed settings and quality categorization against known history. Book a session to estimate your own timeline.
Find Out Which of the Three Is Actually Costing You Output
iFactory AI breaks finishing line OEE into availability, performance and quality, tracked live. Book a walkthrough.