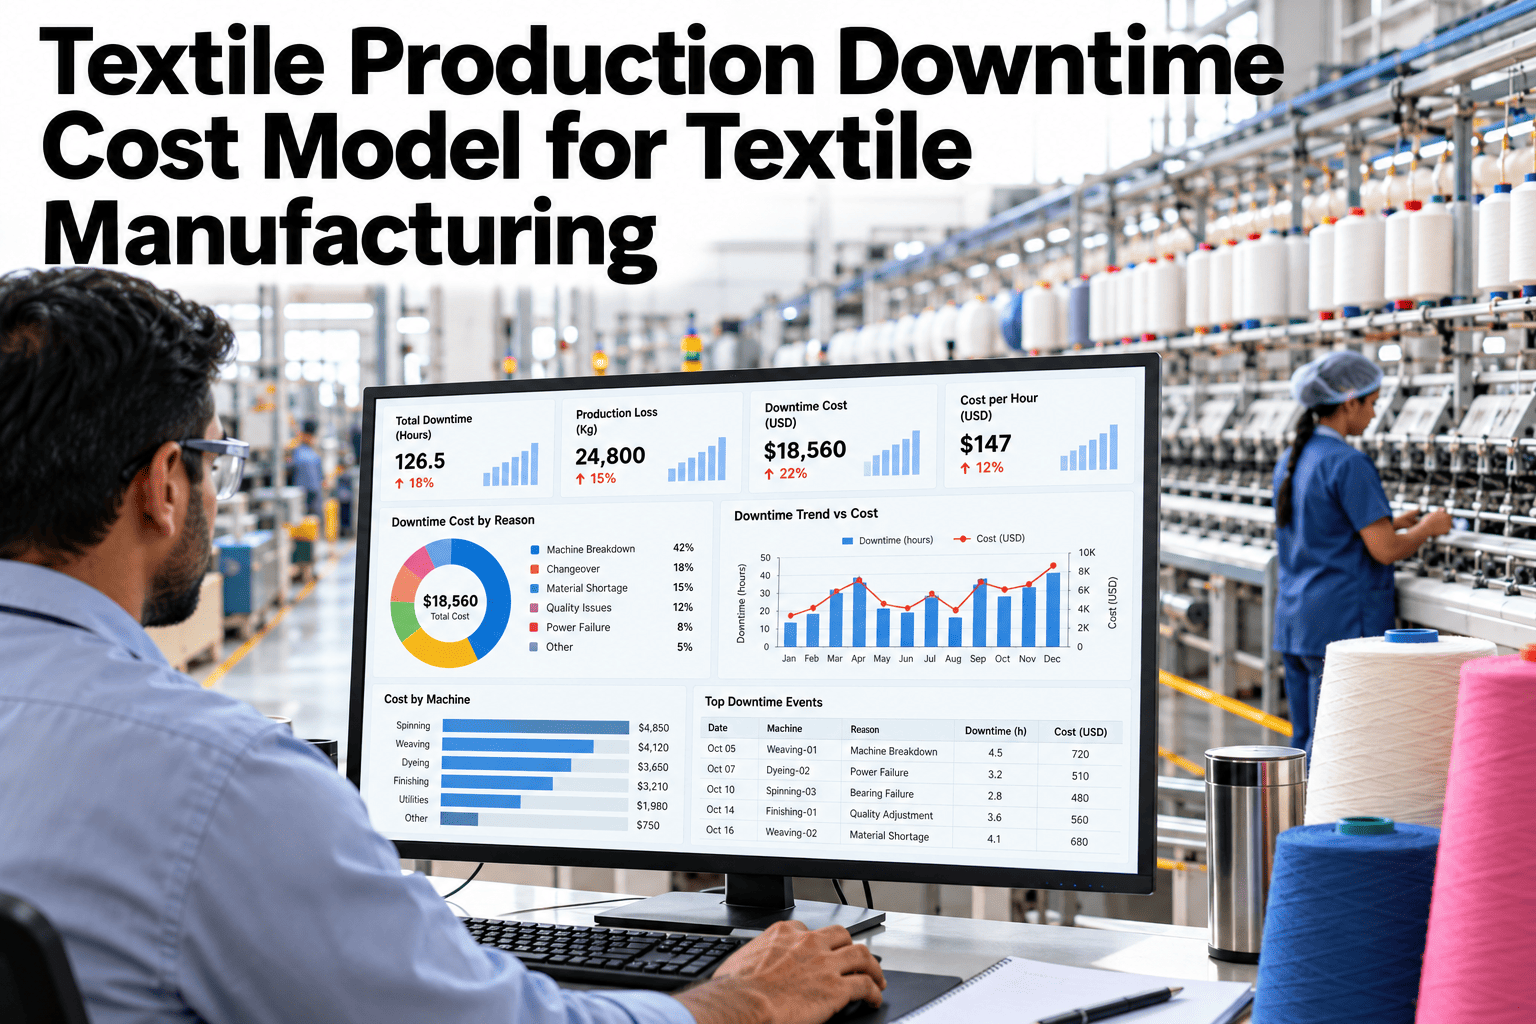
Ask a textile plant what an hour of downtime costs and you will often get a shrug or a single number applied everywhere. In reality the cost depends on where the stop happens, because a bottleneck department stops the whole route while a department with spare capacity barely feels it. A downtime cost model by department turns that shrug into a figure that guides maintenance priorities, spare parts and investment. Textile teams can ask iFactory AI how downtime is costed by department and machine group.
Put a Real Price on Downtime in Every Textile Department
iFactory AI links stop time to lost output, idle labour, restart losses and delivery risk by department, so maintenance and investment follow the true cost of a stop.
What Goes Into the Cost of a Stop
A stop costs more than the missing output. Five components explain most of the bill.
Lost contribution
The margin on output that cannot be recovered later in the schedule.
Idle labour and overhead
People and fixed costs that continue while the machine stands.
Restart losses
Waste, rework and off-quality output as the process restarts.
Energy and utilities
Steam, power and air consumed while production stands still.
Delivery risk
Late order penalties, expediting and customer goodwill.
A Worked Example: Two Hours at a Dyeing Machine
This is illustrative arithmetic in generic currency units, not real plant data. A dye machine stops for two hours.
| Component | Basis | Illustrative Cost |
|---|---|---|
| Lost contribution | 1,200 kg of output at 0.5 per kg margin | 600 |
| Idle labour | 4 people for 2 hours at 3 per hour | 24 |
| Restart and re-dye risk | Allowance for one affected lot | 150 |
| Idle energy and utilities | Steam and power while standing | 40 |
| Total for the stop | Sum of the four items above | About 814 |
Why the Bottleneck Changes Everything
An hour lost at the bottleneck is an hour lost for the whole route. The chart shows an illustrative cost per stop hour across a route.
What Drives Cost in Each Department
Each department loses money differently. The matrix, shown as an illustration, ranks typical cost drivers.
| Department | Lost Output | Restart Waste | Delivery Risk |
|---|---|---|---|
| Spinning | Moderate | Moderate | Moderate |
| Weaving | High | Moderate | Moderate |
| Knitting | High | Moderate | Moderate |
| Dyeing | High | High | High |
| Finishing | High | Moderate | High |
Find Out What Your Most Expensive Hour Really Is
Book a 30-minute session and iFactory AI will review your routes, stop records and margins to show which departments cost the most when they stop.
From Stop Records to a Cost Figure in Five Steps
A cost model needs only a few inputs. These steps work in most textile plants.
Capture every stop with start, end and reason.
Mark each machine group on the route and note the bottleneck.
Set margin, labour, utilities and restart allowances per department.
Multiply stop hours by the cost per hour of each department.
Rank reasons and machines by total cost, not by hours alone.
Hours Lost or Cost Lost
Counting hours treats every stop equally. Counting cost does not.
Using the Model to Make Decisions
A cost per hour is only useful if it guides choices. These are the most common uses.
Rank maintenance work
Fix the machines whose stops cost the most first.
Size spare parts stock
Hold more for critical, high-cost machines.
Justify improvement projects
Compare project cost with annual downtime cost saved.
Plan the schedule
Protect the bottleneck from avoidable stops.
Downtime Cost Model Checklist
Use this list when building or reviewing your model. Each box should be answerable from records.
A Composite Scenario: The Quiet Stop That Cost Most
This is a composite example, not a named plant. It shows how costing reorders priorities.
What iFactory AI Adds to Downtime Costing
iFactory AI is smart manufacturing and industrial software for textile operations. Explore downtime costing in a live product tour on realistic plant data.
A 30-Day Plan to Start
A month is enough to cost downtime for one route.
Review of Downtime Cost Modelling
A practical review of what makes a downtime cost model useful, written as editorial guidance rather than a named expert quote.
Find the bottleneck first
A cost per hour means little until you know which department limits output.
Count all five components
Repair cost alone understates the real price of a stop.
Write down the assumptions
A model finance has agreed is far more likely to be used.
Frequently Asked Questions
How do I calculate the cost of downtime in a textile plant?
Add lost contribution, idle labour and overhead, restart losses, energy and any delivery penalties for the stop. See a cost calculated on a live stop in a short demo. Use your own margins and rates, and agree them with finance.
Why does the department matter?
A stop at the bottleneck loses output for the whole route, while a stop where spare capacity exists may lose very little. Costing by department shows where stops really hurt. Maintenance should follow that ranking.
Do we need exact figures to start?
No. Reasonable estimates agreed with finance are enough to rank priorities, and they can be refined later. Ask support how assumptions are stored and updated in the model. The ranking matters more than the decimals.
Does this replace OEE?
No. OEE measures how well a machine uses its time, while a cost model shows what lost time is worth. Used together they point to the stops worth fixing first.
How quickly can we build a model?
Many plants build a first model for one route within a month. Book time to scope a downtime costing pilot with your finance and maintenance leads. A first ranking usually changes priorities immediately.
Fix the Stops That Actually Cost You Money
iFactory AI turns stop records into a cost ranking by department so maintenance and investment follow the true price of downtime. Book a walkthrough to see it on your own plant.