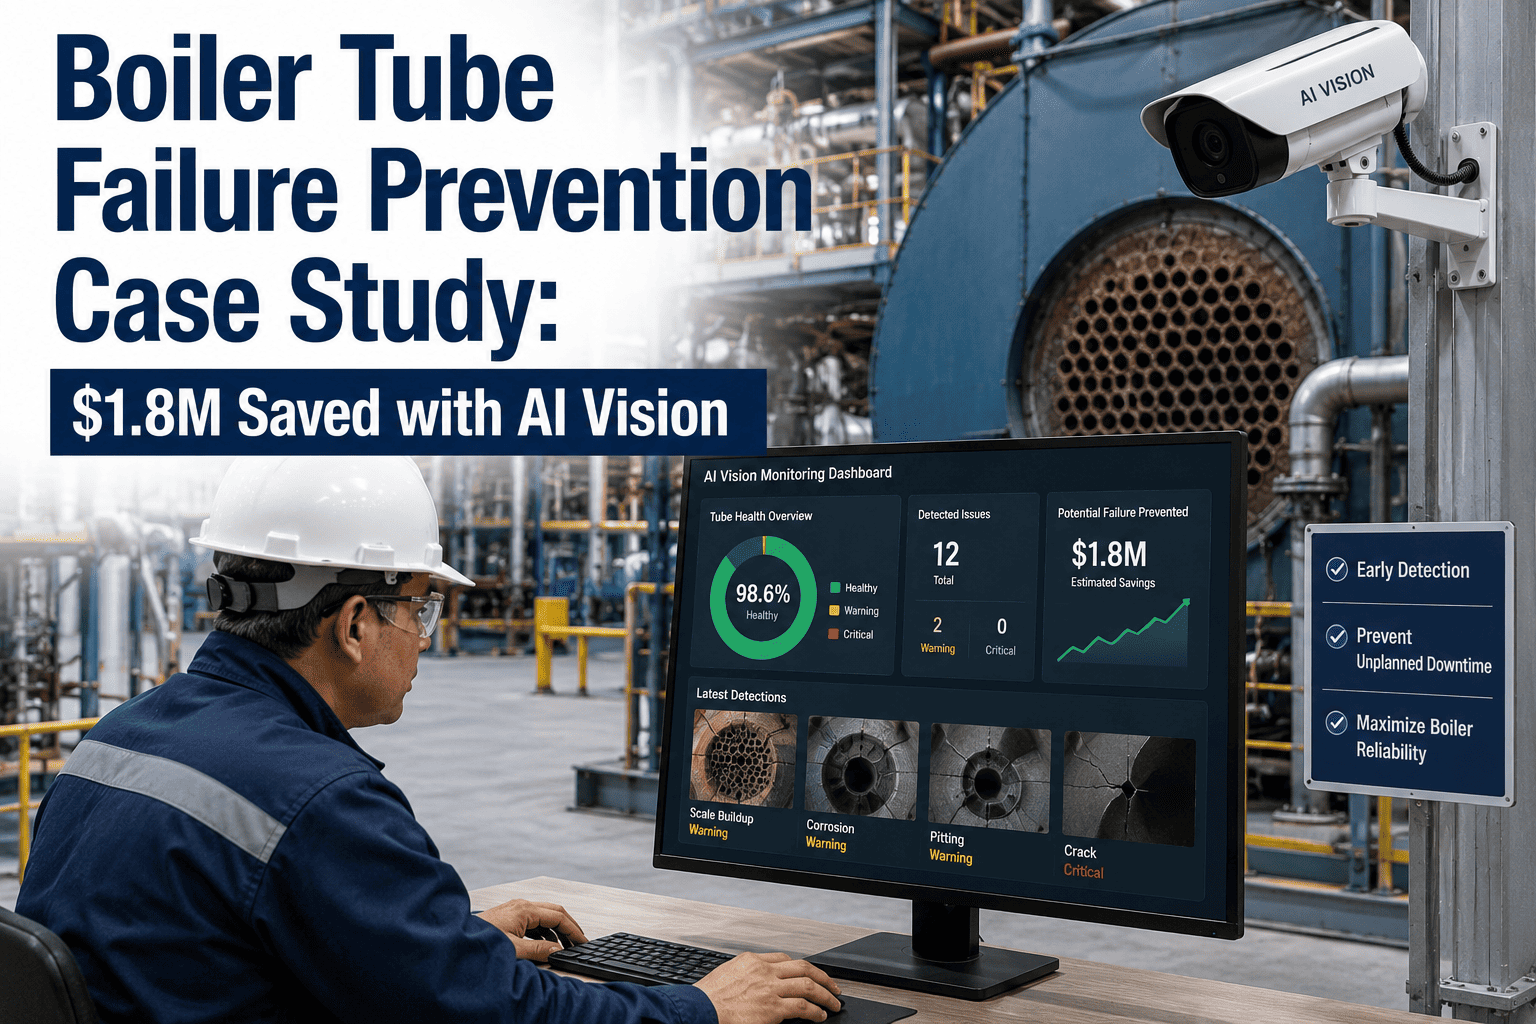
A single unplanned boiler tube failure at a coal or gas-fired thermal plant does not just cost the price of a replacement tube — it costs the forced outage itself, the lost generation revenue for every hour the unit is down, the emergency labor called in at overtime rates, and the downstream damage when a ruptured tube sprays high-pressure steam across adjacent tubing and refractory. This case study walks through how one thermal power plant used AI-assisted borescope inspection to catch seven tubes running below minimum safe wall thickness before any of them failed, and what that early detection was actually worth across three planning cycles. Full inspection methodology is available through iFactory's support team.
iFactory Case Study — Power Generation
7 Tubes Flagged Before Failure — $1.8M in Avoided Forced Outage Costs
AI-assisted borescope inspection caught wall-thickness degradation on seven boiler tubes during a scheduled outage, allowing planned replacement instead of reactive emergency repair after rupture.
$1.8M
estimated total value of avoided forced outages across the review period
7 Tubes
Flagged below threshold
3 Outages
Estimated avoided
1 Outage
Planned replacement window
100%
Baseline comparison coverage
The Situation Going Into the Outage
The plant had been running a conventional borescope inspection program for years — a technician physically walking the boiler during scheduled outages, capturing still images at predetermined access ports, and writing up findings based on visual judgment against reference photographs from prior cycles. The program was not negligent; it was simply working at the limit of what manual visual review can reliably catch. Wall-thinning from erosion, fireside corrosion, and creep damage develops gradually, and the difference between a tube at 85% of nominal wall thickness and one at 68% is often not visually obvious to the eye, particularly across different lighting conditions, camera angles, and technicians rotating through inspection duty over multiple outage cycles.
What Changed With AI-Assisted Inspection
Going into this outage cycle, the plant introduced AI-assisted analysis on top of the existing borescope hardware. Every image captured during the walkdown was processed against a trained model that measured apparent wall condition, flagged deviation from the prior-cycle baseline image at the same access point, and scored each tube segment on a standardized severity scale rather than a technician's subjective read. The same borescope, the same access ports, the same walkdown route — the difference was what happened to the images after capture.
How the Inspection Cycle Ran
1
Pre-Outage Prep
Historical baseline images for every access port pulled and loaded into the comparison model ahead of the outage window.
2
Borescope Walkdown
Standard walkdown route completed by the existing inspection technician team, no change to physical access procedure.
3
AI Wall-Condition Scoring
Each captured image scored against baseline and against a trained degradation model, with severity flags attached automatically.
4
Engineering Review
Flagged segments routed to the plant's reliability engineers for confirmation and repair-versus-monitor decisions.
5
Outage Work Scope Update
Confirmed tubes added to the active outage work scope for planned replacement before startup.
What the Findings Looked Like
Of the several hundred tube segments imaged during the walkdown, seven were flagged by the model as showing wall-condition deviation significant enough to warrant engineering review, and all seven were confirmed on secondary ultrasonic thickness measurement as running below the plant's minimum safe wall-thickness threshold. None of the seven had been flagged as a concern in the prior inspection cycle's manual review — the degradation was real but had been within the range that a technician working from memory and reference photos across many similar-looking images was reasonably likely to pass over.
| Tube Location |
Prior Cycle Status |
AI Flag Severity |
Confirmed Wall Loss |
Action Taken |
| Waterwall, Zone 3 | No concern noted | High | 34% below nominal | Replaced this outage |
| Superheater bank 2 | No concern noted | High | 29% below nominal | Replaced this outage |
| Reheater inlet | Minor note, no action | Medium-High | 26% below nominal | Replaced this outage |
| Waterwall, Zone 7 | No concern noted | Medium-High | 25% below nominal | Replaced this outage |
| Economizer bank 1 | No concern noted | Medium | 22% below nominal | Replaced this outage |
| Superheater bank 4 | No concern noted | Medium | 21% below nominal | Replaced this outage |
| Waterwall, Zone 11 | No concern noted | Medium | 19% below nominal | Replaced this outage |
Want to see how this scoring model performs against your own borescope archive? Send a sample image set to our team for a no-cost comparison run.
How the $1.8M Estimate Was Built
The plant's reliability engineering team built the avoided-cost estimate using the three tubes with the most advanced wall loss — the ones judged most likely to have progressed to failure before the next scheduled outage if left unaddressed. Each of those three was modeled as an independent forced-outage event using the plant's own historical cost data for comparable prior tube failures, rather than industry-average figures, which is why the number is treated internally as a defensible planning estimate rather than a marketing claim.
45%
Lost Generation Revenue
Modeled hours of forced outage per event multiplied by the unit's generation capacity and prevailing market power price at time of estimate.
25%
Emergency Repair Premium
Overtime labor, expedited parts freight, and contractor mobilization costs typical of an unplanned repair versus a scoped outage task.
20%
Collateral Damage Risk
Estimated probability-weighted cost of adjacent tube and refractory damage typical when a tube ruptures under pressure rather than being replaced proactively.
10%
Extended Outage Duration
Additional days a forced outage typically runs beyond a planned outage window due to unscoped diagnostic and repair sequencing time.
Results Beyond the Immediate Outage
7 of 7
Flags Confirmed on Secondary Testing
Every tube flagged by the model was independently confirmed below threshold on ultrasonic thickness testing, with zero false positives requiring unnecessary replacement.
0
Tube Failures in the Following Operating Cycle
No unplanned tube failures occurred in the operating period following the outage, compared to an average of two to three forced events per cycle in prior years.
Consistent
Scoring Across Technician Rotation
The severity model applied the same criteria regardless of which technician performed the physical walkdown, removing rater-to-rater variability from the review.
Baseline Set
For Every Future Cycle
This cycle's images now serve as the comparison baseline for the next outage, making degradation trends visible cycle over cycle rather than reset each time.
Why Gradual Wall Loss Is Hard to Catch by Eye
Wall thinning inside a boiler tube almost never happens as a single dramatic event. It accumulates cycle over cycle from a combination of fireside erosion where ash particles abrade the tube surface, localized corrosion where water chemistry or flue gas composition attacks the metal at a specific point, and creep damage where sustained high temperature and pressure slowly deform the tube wall. Each of these mechanisms produces a visual signature that is subtle in any single image and only becomes obviously alarming once the tube is already close to failure. A technician looking at one outage's images in isolation has no reliable way to know whether a given patch of discoloration or surface texture represents this cycle's normal condition or a meaningful step down from where that same tube stood two cycles ago.
This is compounded by the sheer volume of images a single outage walkdown produces. A boiler with hundreds of access ports and multiple tube rows per port generates a stack of images that no single person can hold in working memory across an eight-hour or longer inspection shift, let alone compare with precision against a stack from a prior outage months or years earlier. Reference photo binders help, but flipping between a current image and a printed or digital reference photo taken under different lighting, at a slightly different angle, is still an approximate comparison rather than a precise one. The gap between what a careful technician can reasonably catch and what true pixel-level, angle-matched comparison can catch is exactly where these seven tubes sat before this outage.
Turning a One-Time Catch Into a Standing Monitoring Program
The real value of this case study is not the single outage where seven tubes were caught — it is what the plant did afterward to make sure the next set of developing issues gets caught just as reliably. A one-time AI-assisted pass that is not repeated the following cycle loses most of its value, since the comparison model depends on having a growing, consistent image history to compare against. The plant treated this outage as the starting point for a standing program rather than a one-off audit.
Every Cycle
Baseline Set Refreshed
Each outage's image set becomes the new baseline for the next cycle, so degradation trends stay visible rather than resetting to a fresh comparison each time.
Standing Scope
Same Access Points Every Time
The plant locked in a fixed set of access ports and capture angles for every future outage, since consistent capture is what makes precise comparison possible at all.
Documented
Review and Sign-Off Process
Every flagged tube now goes through a documented repair-versus-monitor decision with the reliability engineering team, rather than an informal judgment call by whoever reviews the images.
Trend Record
Tracked Per Tube Segment
Any tube segment with a repeat medium-severity flag across two or more cycles is now automatically escalated for closer engineering review rather than waiting for a high-severity flag to appear.
Frequently Asked Questions
Does this replace ultrasonic thickness testing?
No, and it is not designed to. The AI vision layer works as a screening and prioritization step on top of the existing borescope program, identifying which tube segments warrant secondary ultrasonic confirmation rather than replacing that confirmation step entirely. In this case study, all seven flagged segments were still independently verified with ultrasonic testing before any repair decision was finalized. The value is in directing limited testing time and engineering attention to the segments most likely to need it, instead of spreading confirmation testing evenly or missing segments a technician's visual review passed over.
Talk to our team about how the two methods fit together on your outage program.
What kind of borescope hardware does this require?
The model is built to work with the digital borescope equipment most thermal plants already use for outage inspections, since the analysis runs on the captured images rather than requiring a hardware swap. Image resolution and lighting consistency matter more than a specific brand or model of borescope, and our deployment team reviews sample images from your current equipment during the onboarding assessment to confirm compatibility. Where equipment upgrades would meaningfully improve image quality, that gets flagged early rather than discovered mid-deployment.
Book a walkthrough to review your current hardware against the requirements.
How long does it take to build a reliable baseline?
A usable baseline can often be built from a single prior outage cycle's image archive if that archive is organized by access point and reasonably consistent in capture method, which is common for plants that have run a structured borescope program for several cycles already. Where historical images are sparse or inconsistent, the first live cycle itself becomes the baseline for future comparison, and severity scoring in that first cycle relies more heavily on absolute degradation models than on cycle-to-cycle comparison. Either path gets a plant to full baseline-comparison scoring within one to two outage cycles.
Share a sample of your inspection archive and we will assess baseline readiness before you commit.
Can this be extended to turbine and pressure vessel inspection?
Yes, the same underlying approach — image-based comparison against baseline plus trained defect classification — applies to turbine blade borescope inspection, pressure vessel internal inspection, and other visually-inspected assets across a thermal plant, though each asset class uses its own trained model tuned to the specific degradation modes relevant to that equipment. Plants that start with boiler tube inspection commonly extend the same platform to turbine inspection in a subsequent phase once the workflow is proven.
Book a demo to see the turbine inspection module alongside the boiler tube workflow.
What does a typical deployment cost relative to the avoided-cost estimate shown here?
Deployment cost scales with the number of access points, image volume per outage, and the number of asset classes covered, so a precise figure depends on your plant's specific inspection scope rather than a single published price. What plants running this comparison consistently find is that avoiding even a single forced outage event, using the same conservative modeling approach applied in this case study, typically covers the platform cost for several outage cycles. Our team builds a scoped estimate specific to your unit configuration during the initial assessment call.
Request a scoped estimate from our deployment team.
Catch It Before It Ruptures.
See What Your Own Borescope Archive Would Have Flagged
Bring image sets from your last two outage cycles. We will run the comparison model against them and show you exactly what would have been flagged, at no cost and with no commitment.
$1.8M
Estimated avoided cost
7 of 7
Flags confirmed accurate
1-2 Cycles
To full baseline coverage