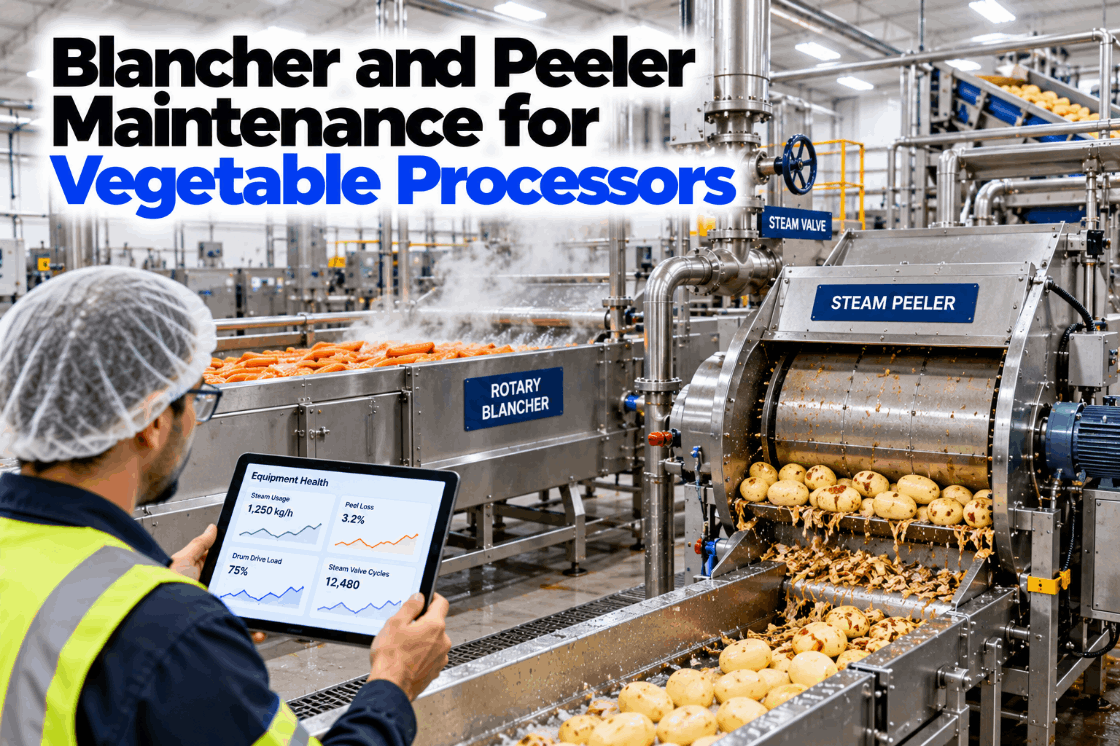
Blancher and Peeler Maintenance for Vegetable Processors

By James C on October 24, 2026

blancher-peeler-maintenance-vegetable-processors

For a frozen or canned vegetable plant, the pack season leaves no room for a blancher or peeler to fail. A steam peeler cycles its exhaust valve thousands of times a day, a drum blancher turns its auger through hot water for weeks on end, and every steam valve on the line wears while it works. When those parts slip, peel loss and steam use climb before anything breaks. Blancher and peeler maintenance works best when that early drift sets the service date. See how iFactory tracks steam valve cycles and drum loads in a short blancher and peeler demo.

PREDICTIVE AI · PRODUCE PROCESSING

Service Peelers and Blanchers Before Peel Loss Climbs

iFactory trends steam valve cycles and drum drive loads, links rising peel loss to the wear behind it, and fits PMs around your seasonal pack schedule so overhauls land before the first load arrives.

Steam peeler 2 · Potato linePack day 41
Batch cycle trend · last 24 hours
Exhaust valve cyclesSince overhaul, counted
Exhaust timeLonger than baseline
Peel lossUp three days running
Blancher drum driveLoad normal
Voice log · 06:15"Peeler 2, lid seal checked, light wear." Logged. Seal wear noted with exhaust trend.
PM suggested · exhaust valve inspection at Sunday wash-down
ROTARY BLANCHER, BELT AND WATER BLANCHERS

Three Blancher Designs, Three Sets of Wear Points

A rotary drum blancher turns a perforated drum, partly submerged in hot water or fed with steam, while internal flights or a helical auger carry product from end to end. A belt blancher carries product on a moving belt through a heated zone, and the belt speed sets the time. Water blanchers give even treatment at slightly lower temperatures, while steam suits cut and small pieces. Each design puts its wear in a different place. Map your own blanchers with our process team.

Blancher type
How heat reaches product
Parts that wear
PM focus
Signal to trend
Rotary drum
Drum turns in hot water, heated by steam injection or a heat exchanger
Drum drive, trunnions or bearings, auger flights, perforated screens, seals
Drive chain and gearbox, flight wear, screen damage, seal leaks
Drum drive load
Belt, steam
Steam fills a hood over a moving belt
Belt and sprockets, steam manifolds, hood seals
Belt tracking, nozzle blockage, hood seal condition
Steam flow against zone temperature
Belt or flume, water
Product moves through recirculated hot water
Pumps, heat exchanger, belt, spray headers
Pump seals, exchanger fouling, header blockage
Water temperature recovery
All types
Steam supply controls the heat
Control valves, steam traps, temperature probes
Valve seats and actuators, trap tests, probe checks
Valve position and cycles
STEAM PEELER

A Pressure Vessel That Cycles All Day

A steam peeler is a batch pressure vessel. It closes on a load, fills with steam for a short time, then releases the pressure in a flash so the skin lifts off. Thelen, for example, describes steam at up to 16 bar for roughly 30 to 60 seconds, depending on the product. Equipment makers quoted by FreshPlaza call steam time the single biggest factor in peel loss. A slow exhaust valve or a leaking lid seal therefore costs product on every batch. Review your peeler cycle data with our peeling specialists.

1
Vessel, lid and lockingLid seals, locking parts and any interlock that stops opening under pressure
2
Quick-release exhaust valveSeats, seals and actuator. Slower exhaust means a less sharp release and more steam time
3
Steam inlet and rotationInlet valve seats, pressure sensors and the drive that turns the vessel
Pressure vessel inspection is set by your jurisdiction

Steam peelers are usually built to ASME Section VIII. In-service inspection intervals and who may inspect are set by the state, province or local jurisdiction where the vessel sits. Repairs to a code vessel normally follow the National Board Inspection Code. Confirm the rules for your site with your inspector and insurer.

PEEL LOSS

Signals That Move Before Peel Loss Rises

Peel loss is the yield number everyone watches, but it moves late. The equipment signals behind it move first. Steam takes longer to reach pressure when an inlet valve wears, exhaust slows as a valve seat erodes, and operators add steam time to make up for both. Tracking these signals per batch shows which part is drifting. Check which signals your peeler controls already record with our integration team.

Pressure rise timeSeconds from steam on to target pressure, per batch
Exhaust timeSeconds to vent. A slower release points to the exhaust valve
Steam time settingOperator changes that may be covering for wear
Valve cycle countCycles since the last rebuild for each inlet and exhaust valve
Peel loss by shiftYield from weigh points, matched to the batches behind it
Steam per tonneSteam used per tonne peeled, which rises with leaks and slow cycles

Ask Why Peel Loss Went Up This Week

iFactory reads peeler cycle data, valve counts and blancher drive loads together, so a yield change points to the part most likely behind it. Crews log seal and valve checks by voice, and those notes appear with the trend.

Potato line · Maintenance lead and iFactory
LeadWhy is peel loss up on Peeler 2?
iFactoryExhaust time has grown over three days, and steam time was raised twice to keep the peel clean. The exhaust valve is near its usual rebuild count.
LeadCan it wait for Sunday?
iFactoryThe trend is gradual, so Sunday's wash-down fits. I've added an exhaust valve inspection to that PM.
ABRASIVE PEELERS AND AUGER MAINTENANCE

Rollers, Screws and the Seals Around Them

Abrasive peelers rub the skin off with grit-coated rollers, while a conveyor screw sets how long the product stays in contact. Herbort, for example, describes carborundum rollers with quick-change mounts and notes that a faster screw means a shorter peel. Augers and screw conveyors also move product through drum blanchers and between machines, and their bearings and shaft seals sit in hot, wet conditions all season. Plan roller and auger PMs with our maintenance planners.

Abrasive rollers
Grit wear sets peel qualityWorn grit leaves skin on, so operators slow the screw. Track roller hours and swap sets on a plan.
Augers and screws
Flights, shafts and hanger bearingsWorn flights carry product unevenly and change residence time. Measure flight edges each overhaul.
Seals and bearings
Shaft seals in hot waterA leaking seal lets water reach bearings. Drive current and bearing temperature show it early.
STEAM VALVE WEAR

Valves and Traps That Decide Blancher Temperature

Blanchers and peelers depend on steam valves that open and close many times an hour. Seats erode and actuators slow, so the valve reaches its position later or leaks when shut. Steam traps on the blancher supply matter too. Emerson notes that a trap failed shut lets condensate collect, cutting heat transfer and making temperature hard to control. Grade each valve and trap so work is planned before it fails. Ask our support team how to set grades.

Healthy
Reaches position on time, holds shut, cycle count well below rebuild level
Watch
Response slowing or cycle count nearing the usual rebuild point
Plan
Seat leak or slow temperature recovery. Book work at the next wash-down
Act now
Valve sticking, trap failed shut or water hammer. Fix before the next run
BLANCH ADEQUACY

The Peroxidase Test Belongs to QA, the Conditions to Maintenance

Blanching stops enzymes that would spoil colour and flavour in storage. QA teams commonly check it with an enzyme indicator such as peroxidase, and some use lipoxygenase for certain products. That test is a quality check. Its result depends on equipment holding the right temperature for the right time, which is where maintenance comes in. Line up QA and maintenance checks with our food safety team.

WHAT QA CHECKS
  • Enzyme indicator test on blanched samples, such as peroxidase
  • Colour, texture and over-blanching
  • Sampling plan by line, product and shift
  • Holds and releases when a result fails
WHAT MAINTENANCE CONTROLS
  • Temperature probes checked and calibrated
  • Steam valves and traps that hold temperature steady
  • Drum speed, auger flights and belt speed that set time
  • Even water or steam spread from clear headers and nozzles
BLANCHER PEELER MAINTENANCE TEMPLATE

Pre-Season Overhaul and Post-Season Layup

Seasonal plants live by the pack calendar. Most heavy work happens in the off-season, and how the line is laid up decides how much work the next overhaul needs. Use this list as a starting point and add your machine makers' own steps. Ask our support team for a version built on your assets.

01Pre-season overhaulBefore pack
02Post-season layupAfter pack
BLANCHER PEELER MAINTENANCE BEST PRACTICES

Six Habits That Protect the Pack

These habits come up again and again in seasonal produce plants. None needs new equipment, only steady records and planned stops. Talk them through with our produce specialists.

01
Count valve cyclesRebuild by cycles run, not calendar weeks
02
Watch steam time changesEvery increase may be hiding wear
03
Use wash-downsPlan short PMs into the cleaning windows
04
Log wear at layupMeasurements made in autumn set the spring parts list
05
Keep critical sparesValve kits, seals and probes on the shelf before pack starts
06
Share yield dataGive maintenance the peel loss figures QA and production see
BLANCHER PEELER MAINTENANCE IMPLEMENTATION GUIDE

Five Steps From First Signal to a Pack-Ready Line

Start in the off-season with the peeler or blancher that cost you the most in the last pack. Most of the data already sits in the machine controls. Plan your first asset with our implementation team.

1ConnectPeeler cycle data, valve positions, drum drive loads and probes
2BaselineLearn normal pressure rise and exhaust times per product
3LinkMatch peel loss and steam use to the signals behind them
4AlignPMs set around the pack calendar and wash-down windows
5LogSeal, valve and wear checks recorded by voice
BLANCHER PEELER MAINTENANCE COST AND ROI

Put Your Own Figures Into Peel Loss

Peel loss is where small changes add up across a season. Every input below is an assumption made to show the arithmetic only, so replace each with your own numbers before drawing a conclusion. Our team can build the case with your yield data.

Raw product through the peeler10 tonnes per hour, assumed
Peeling hours per season1,500, assumed
Raw product per season10 × 1,500 = 15,000 tonnes
Peel loss avoided by planned valve and seal work0.5 percentage points, assumed
Product kept per season15,000 × 0.005 = 75 tonnes

Add steam saved and fewer in-season breakdowns only where your own meter and work order records support them.

TURNKEY AI DEPLOYMENT

Predictive Models and AI Server, Ready Before Pack

iFactory is delivered as a turnkey bundle. A pre-configured NVIDIA AI server ships racked and ready with the peeler, blancher and steam valve models loaded, and connects to your line controls on site. You rack it, plug in power and Ethernet, and the AI is live. Get a scope for your plant from our deployment team.

What's Included
  • Pre-configured NVIDIA AI server, racked and ready
  • Connectors for peeler, blancher and steam controls
  • Steam valve cycle and drum drive load models
  • Peel loss linked to equipment wear
  • PM plans aligned to the seasonal pack calendar
  • Voice logging for seal, valve and wear checks
  • 24×7 remote monitoring of models and hardware
Live in 6–12 weeks
Wk 1–4
Connect and Map

Server installed, peeler and blancher signals linked, pack calendar loaded.

Wk 5–8
Baseline and Shadow

Normal cycle times learned, alerts checked by maintenance.

Wk 9–12
Go-Live and Training

Alerts switched on, voice logging rolled out, planners trained.

HOW iFACTORY FITS

Blancher Peeler Maintenance for Plant Managers

iFactory is built for seasonal lines where every pack day counts and the off-season is the only long window for work. Our specialists can show it on your own equipment.

1
Counts steam valve cycles. Inlet and exhaust valves tracked from rebuild to rebuild.
2
Trends drum drive loads. Blancher drives and augers watched for rising load.
3
Links peel loss to wear. Yield changes matched to the part most likely behind them.
4
Plans around the pack. PMs aligned to seasonal schedules and wash-down windows.
1000+
Industrial clients running iFactory
99.9%
Platform uptime through the pack season
6-12 wks
From racked server to live line alerts
FREQUENTLY ASKED QUESTIONS

What Plant Managers Ask About Blancher and Peeler Maintenance

What wears most on a steam peeler?
The parts that cycle with every batch: the quick-release exhaust valve, the steam inlet valve, the lid seals and locking parts, and the drive that turns the vessel. Wear in the exhaust and inlet valves often shows up first as longer cycle times and more steam time.
How does equipment wear raise peel loss?
Equipment makers describe steam time as the biggest single driver of peel loss. When valves slow or seals leak, the release is less sharp, and operators often add steam time to keep peeling clean. That extra time takes more flesh with the skin.
Who inspects a steam peeler pressure vessel?
Rules depend on the jurisdiction where the vessel is installed. Peelers are usually built to ASME Section VIII, and the state, province or local authority sets in-service inspection intervals and who may carry them out. Repairs normally follow the National Board Inspection Code.
What is the difference between rotary drum and belt blanchers for maintenance?
A rotary drum blancher puts its wear in the drum drive, bearings, auger flights, screens and seals. A belt blancher wears its belt, sprockets, steam manifolds and hood seals. Both depend on steam valves, traps and temperature probes to hold temperature.
Does the peroxidase test tell maintenance anything?
Indirectly. It is a QA check that blanching stopped the enzymes. A failing result can point to low temperature or short time, which leads back to steam valves, traps, probes, drum speed or belt speed. Linking QA results to equipment data shortens the search.
When should we start?
In the off-season, ideally right after layup. Connect the peeler and blancher that cost you most last pack, load the pack calendar and record the wear you measured at layup. Our support team can plan that first step with you.

Start the Next Pack With a Line That Is Ready

Count steam valve cycles, trend drum drive loads and link peel loss to the wear behind it, with PMs planned around your pack calendar. The full system is delivered turnkey and goes live in 6 to 12 weeks.
Example pack summary · Potato line
Peelers watchedCycle, exhaust and rise times
BlanchersDrum drive loads and temperature
Steam valvesCycles counted, graded
PM planAligned to the pack calendar
Every overhaul planned before pack starts

Share This Story, Choose Your Platform!