Every 1% of comber noil is real cotton walking out of the machine as waste, and combing is the process where the mill decides how much of that waste is justified. Most mills book the noil percent from an ERP setpoint that hasn’t been reconciled against weighed noil in months — which means the cost accounting is running on a number the shop floor knows is wrong. Head-to-head variation, shift-to-shift drift, and slow settings decay all hide inside a single monthly average. The raw-material yield loss shows up in monthly cost review as a variance the ERP can’t explain, and the specific comber head that caused it is invisible.
iFactory / Comber noil percent reconciliation
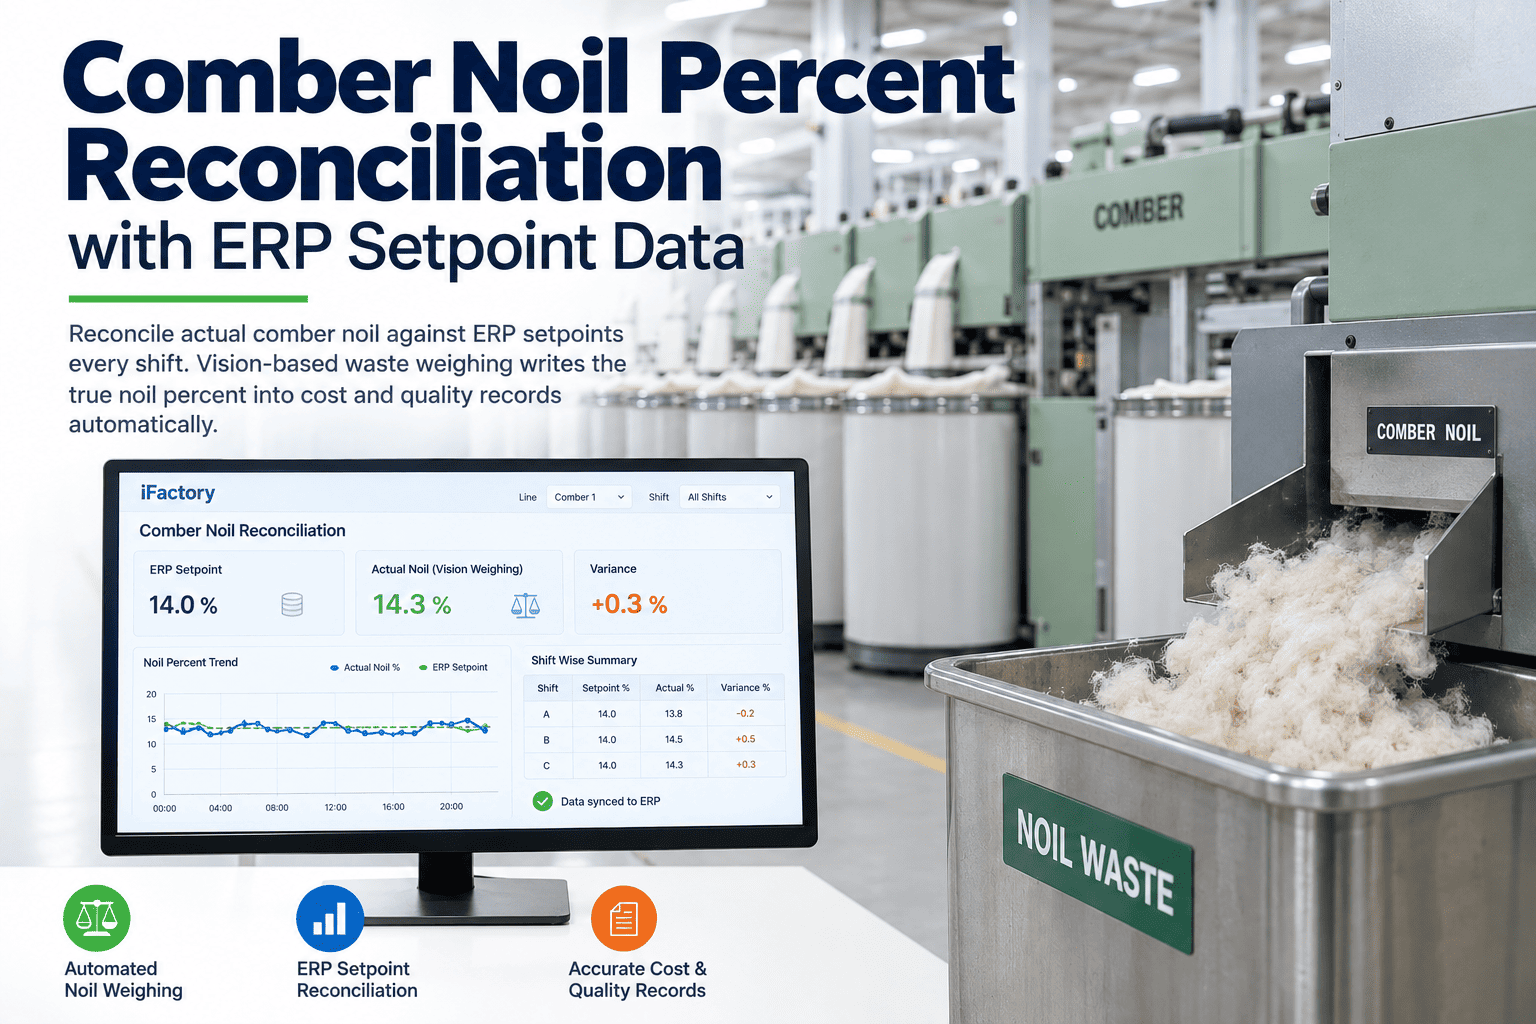
Reconcile Actual Comber Noil Against ERP Setpoint Every Shift
Vision-based waste weighing at each comber captures the true noil percent per head, per shift, per mix — and writes the reconciliation into the cost accounting and quality records automatically, so the number the ERP shows matches the number the floor produced.
+2.4%
unaccounted raw material walking out as waste
$1.43
/ 0.1% / 1000 kg Ne30
2–3%
Turkish mill trial reduction
The Problem on the Line
A comber deliberately wastes cotton — that’s the point. The noil percent, typically 15–22%, is the balance between removing enough short fibre and neps for combed-count yarn, and not throwing away raw material the mill has paid for. Uster mill trials on 50,000 spindles running Ne30 at $1.43/kg show every 0.1% of noil deviation is worth about $1.43 per 1000 kg of yarn produced. Yet in most mills the noil percent booked in cost accounting is an ERP setpoint that is rarely reconciled against noil actually weighed at the head. When actual runs above setpoint for weeks, the mill pays for raw material the ERP says it isn’t using.
What Escapes Into the System of Record Today
The gap between setpoint noil and actual noil is a data problem, not a physics problem. In most mills, the actual weighed noil is captured once and then rebuilt from tally sheets that nobody trusts.
Paper
Noil weighed at a periodic waste audit, entered on a paper log, typed into the ERP as a monthly adjustment that averages away the head-level and shift-level variation.
WhatsApp
Combing supervisor and cost accountant exchange messages about a suspected noil overrun. Neither has a per-head, per-shift record to point at.
Winder-only data
The elevated raw-material yield loss shows up in monthly cost review as a variance the ERP can't explain. Neither the head, nor the shift, nor the mix that caused it is identifiable.
Nowhere at all
Head-to-head variation — one comber running 20.4% noil while another runs 17.8% on the same mix — is invisible without weighed-noil data per head. The mill averages it away, misses the specific comber that needs setting review, and pays raw material cost blind.
What the Camera or Agent Actually Sees
A vision-based weighing station at the noil-collection chute of each comber captures the actual noil weight produced per head, per shift interval. Combined with the delivered-sliver weight (already in the MES), the true noil percent is reconciled against the setpoint automatically.
Noil Volume
Vision on the noil chute or the collection bin measures the volume of noil produced per head over a shift interval — with density calibrated per fibre type.
Read: noil volume per head
Bin Weigh
Load-cell or vision-verified weigh at bin change gives the periodic weight ground-truth that calibrates the vision volume-to-mass estimate.
Read: bin weight ground truth
Delivered Sliver
Sliver delivery mass per head over the same interval read from the MES production record — the denominator for the noil percent calculation.
Read: from MES delivery
Reconciliation
Actual noil percent per head per shift computed as noil-mass ÷ (noil-mass + sliver-mass), reconciled against the ERP setpoint for the mix.
Compute: actual vs setpoint
What Gets Written Back
Weighing noil is not the point. Writing the true noil percent back into cost accounting and quality records — automatically, per head, per shift — is what changes how the mill sees raw-material yield.
Actual Noil %
ERP Cost Accounting
Actual noil percent per head per shift written into the mix's raw-material cost record, replacing the standing setpoint entry with weighed truth.
Yield Variance
ERP Materials
Raw-material yield variance calculated on actual noil, not setpoint noil — the monthly cost variance stops being a surprise line.
Comber Head Trend
Spinning MES
Noil percent trend per comber head over shifts — a drifting head or a machine needing setting review surfaces against the fleet.
Quality Correlation
Spinning MES / SPC
Noil percent joined to the same-shift AFIS or Uster Tester lab sample — the quality-cost balance visible on one chart, not two.
Take last quarter's cost review. If the raw-material yield variance for combing showed up as unexplained, that variance is a noil-reconciliation gap. Book a cost reconciliation review — we'll audit one month's ERP setpoints against weighed noil.
12-Week Pilot Shape on One Station
One comber, one mix, one month. The pilot is scoped to prove the ERP write-back — that when the actual noil percent overrides the setpoint in cost accounting, the monthly variance closes and the mill sees noil discipline as a controllable number, not a monthly surprise.
Weeks 1–2
Baseline & Weigh
Vision on the noil chute of one comber head. Two weeks of continuous volume capture, calibrated against periodic bin weighs. Baseline: actual noil % per head per shift vs ERP setpoint.
Weeks 3–4
Calibration Lock
Volume-to-mass model calibrated to the fibre type and comber-specific chute geometry. Reconciliation error targeted below 0.2% noil against bin-weigh ground truth.
Weeks 5–8
ERP Write-Back Live
Actual noil percent writing into ERP cost accounting per head per shift. Comber head trend visible in the MES. Yield variance calculated on actual.
Weeks 9–12
Cost-Variance Match
First month closes with actual-noil cost variance. Combing supervisor uses head-level data to adjust settings on the drifting head. Monthly cost review presents a variance the shop floor can defend.
Who Owns the KPI
Noil reconciliation crosses production, quality, and finance. Each function needs its own number on the KPI board or the discipline is one person's spreadsheet.
Combing Sup.
Actual noil % per head per shift
Owns the machine-level noil trend and the setting adjustment decision — Uster trials show mills reduced noil 2–3% with no quality loss when they saw head-level data.
Quality Head
Noil % vs AFIS / Uster Tester
Owns the quality-cost balance — validates that noil reductions do not degrade CVm or nep count; approves setting changes based on the joint chart.
Cost Accountant
Raw-material yield variance to actual noil
Owns the ERP write-back and the monthly variance — the cost record now reflects weighed truth, not standing setpoints from last year.
Materials / GM
Raw-material yield $ per bale processed
Owns the yield number that goes to the operations review — every 0.1% of noil recovered on 50k spindles at Ne30 is roughly $1.43 per 1000 kg of yarn.
FAQ
Isn't the noil percent already known from the mix planning?
The setpoint is known — the mix planning specifies target noil for the count and end use. What isn't known is what the comber actually delivered on any given shift. Uster mill trials found real noil can sit two to three percentage points above the setpoint on some heads for weeks at a time, invisible to the ERP. On 50,000 spindles at Ne30 that's tens of thousands of dollars per year per head. The setpoint is aspiration; the reconciliation is truth.
Why vision on the chute — why not just a scale on the bin?
A scale on the bin gives you excellent ground truth once per bin change, which is typically once or twice per shift. Vision on the chute gives you continuous volume — which reveals the intra-shift variation (start-of-shift settings, doff cycles, end-of-lot behaviour) that a bin-average completely hides. The right architecture uses both: vision for the continuous trend, bin weighs as the periodic calibration check. Every plant that's taken the trouble to do this discovers that the intra-shift variation is where the setting decisions actually live.
What noil reduction is realistic without hurting yarn quality?
Uster's published mill trials show CVm improvement flattens out above about 18% noil — extra noil above that point buys almost no additional evenness or nep reduction and is essentially wasted cotton. A Turkish mill referenced in the same trials reduced noil by 2–3% with no yarn-quality loss once they saw the head-level and shift-level data continuously. The realistic recovery on any specific mill depends on where its current noil sits and what its quality customers demand — the reconciliation is what makes the trade-off visible.
Stop paying for noil the ERP doesn't know you produced.
Reconcile One Month of Comber Noil Against ERP Setpoints
Bring one comber, one mix, and last month's ERP setpoints for combing. We'll set up vision capture on the noil chute, calibrate against bin weighs, and show the actual-vs-setpoint reconciliation on a per-shift chart.