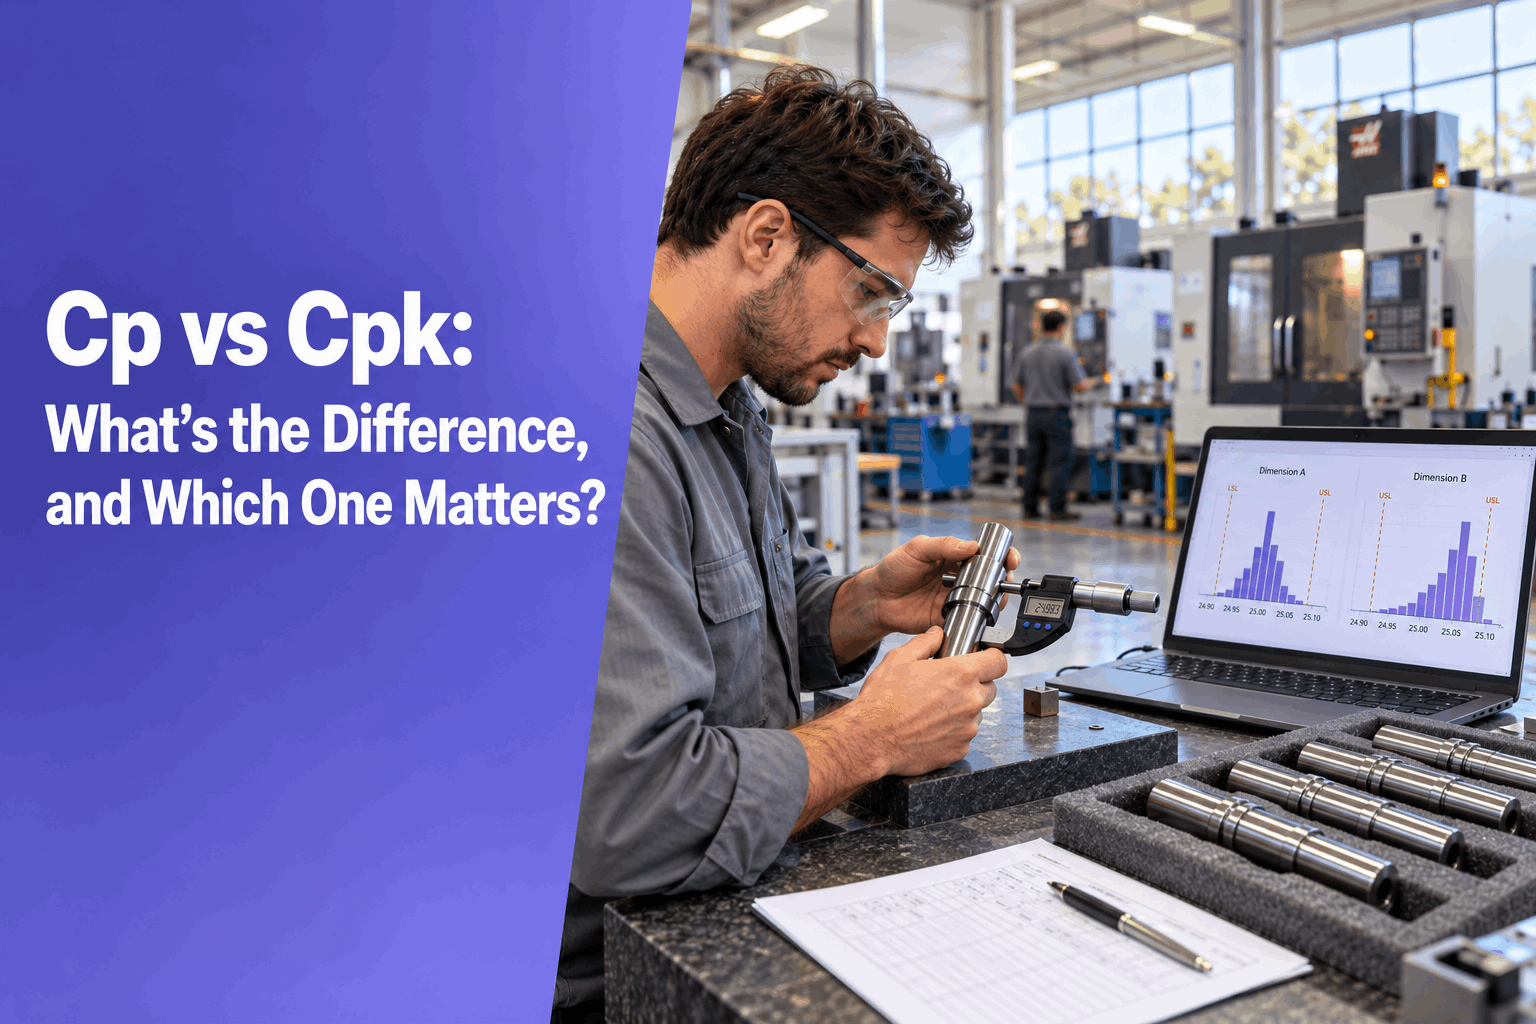
Every capability study asks one question: does the process vary less than the drawing allows? Two numbers do most of the work, and the Cp vs Cpk question is where many engineers get stuck. Cp tells you if the spread fits the tolerance. Cpk tells you if it fits where the process actually runs. For the step-by-step math, see how to calculate Cpk.
Same spread, different answer
A shaft diameter can have a tight, healthy spread and still run close to the upper limit. That gap is what separates the two indices. Below: both formulas, one worked example, and what to fix first when the numbers disagree.
What Cp measures
Cp is the simplest process capability index. It compares the width of the tolerance with the natural width of the process. That natural width is six standard deviations: three on each side of the mean.
What the number tells you
Cp is a ratio. At 1.00, the process spread exactly fills the tolerance, with nothing to spare. Above 1.00, the spread is narrower than the tolerance and there is room left over. Below 1.00, the spread is wider than the tolerance, so some parts will land outside the limits no matter where you aim.
What it assumes
Cp never looks at the mean. It assumes the process sits dead center between the limits. Slide the whole distribution up against one limit and Cp stays exactly the same. Think of Cp as potential: what the process could do if it were perfectly centered.
What Cpk measures
Cpk closes that blind spot. It measures the distance from the mean to each spec limit in units of three standard deviations, then keeps the worse of the two sides.
Why the smaller side wins
Parts fail on the side closest to a limit. A process with lots of room on the low side and very little on the high side will make high-side rejects, and the extra room on the low side does nothing to stop them. Taking the minimum makes Cpk report the side that will hurt you.
Spread and position in one number
Because Cpk uses both sigma and the mean, it reacts to two different problems: too much variation, and an aim point that has moved off target. That is useful and limiting at the same time. A low Cpk on its own cannot tell you which problem you have. You need Cp next to it.
Cp vs Cpk side by side
Here is the difference between Cp and Cpk in one view.
The last row is the one to remember. A low Cp points to one cause. A low Cpk can point to two. That is why a capability report should show both numbers, not just the one your customer asks for.
A worked example
Take a turned shaft diameter with a nominal of 10.00 and a tolerance of ±0.06. The study gives a within-subgroup sigma of 0.01.
Calculate Cp
The spread uses only half of the tolerance. On spread alone, this process is very capable.
Calculate Cpk at mean 10.03
The high side has three sigma of room. The low side has nine. The high side sets the score.
Re-center at 10.00
Nothing about the variation changed. Only the aim moved.
Same spread, but the off-center mean halves the capability. In the shop, a shift like this often traces back to a setup target on the high side of nominal, a tool offset or a wear allowance. Those are adjustments, not projects. That is the main lesson here: before you spend money on reducing variation, check where the process is aimed.
Get Cp, Cpk, Pp and Ppk from your own data: paste your measurements and get a one-page capability report. 14-day free trial, no card needed.
Reading Cp and Cpk together
Once you have both numbers, compare them before you touch the process. The gap between them tells you what kind of problem you have and where to start.
The process is centered
The mean sits at the midpoint of the tolerance, so aim is not the issue. If both values are high, leave the process alone and keep charting it. If both are low, see the third pattern.
The spread is fine, the aim is off
The distribution fits inside the tolerance, but the mean has moved toward one limit. Re-centering is usually the quickest fix, exactly as in the worked example above.
The variation is too wide
Re-centering will not save this one. Even perfectly aimed, the spread is too wide for the tolerance. Illustrative: with the same ±0.06 spec and a sigma of 0.03, Cp = 0.12 / 0.18 = 0.67.
The mean is outside a limit
A negative Cpk means the average part is out of spec, so more than half of the output is outside that limit. Illustrative: a mean of 10.07 gives Cpu = (10.06 − 10.07) / 0.03 = −0.33.
How high is high enough depends on the characteristic and on what your customer requires. For the usual targets, see what a good Cpk value is.
One-sided specifications
Some characteristics only have one limit. A burr height has a maximum but no minimum. A pull-off force has a minimum but no maximum. With only one limit there is no tolerance width, so Cp cannot be calculated at all.
Use it for maximums such as burr height, runout or surface roughness.
Use it for minimums such as pull-off force, minimum wall thickness or minimum hardness.
Do not invent a missing limit, such as a lower limit of zero, just to get a Cp value. A made-up limit gives a made-up number. Report Cpu or Cpl as the Cpk, and state clearly which side it covers.
Before you trust either number
Cp and Cpk are only as good as the data behind them. Check these four conditions before you share the numbers with anyone. The AIAG SPC manual covers each one in more depth, and the AIAG PPAP manual explains where capability studies fit in a part submission.
The process is stable
Capability only predicts future output if the process is in statistical control. Run a control chart first. Points out of control mean you are measuring a moving target, and the index will not hold.
The data is roughly normal
The formulas assume a bell-shaped distribution. Check a histogram and a normal probability plot. Characteristics bounded at zero, like flatness or runout, are often skewed and may need a different method.
There is enough data
Aim for about 25 subgroups or 100 individual values. With small samples, the sigma estimate is rough and Cpk can swing noticeably from one study to the next.
The gauge can see the tolerance
If the measurement system uses up a large share of the tolerance, part of your process spread is really gauge noise. Run a gauge R&R study before you blame the machine.
One more detail: Cp and Cpk use the within-subgroup sigma, typically estimated from the average range or standard deviation of your control chart subgroups. That choice matters in the next section.
Where Cpk vs Ppk fits in
Pp and Ppk use the same formulas as Cp and Cpk, but swap in the overall standard deviation of all the data. That overall spread includes shifts between subgroups, such as setup changes, material lots and shift-to-shift drift. When Ppk sits well below Cpk, the process looks tight inside each subgroup but moves around over time. The full comparison is in Cpk vs Ppk.
Get both numbers from your own data
You do not need to work the Cp vs Cpk math by hand for every characteristic on a control plan. Paste your measurements and spec limits into the Cp/Cpk Report Generator and you get Cp and Cpk side by side, a histogram drawn against your spec limits, and centering advice when Cpk sits well below Cp. Treat the result as an estimate to review, and still check stability and your gauge first. If you would rather check the math yourself, you can calculate Cpk in Excel and compare the two.
Get Cp, Cpk, Pp and Ppk from your own data: paste your measurements and get a one-page capability report. 14-day free trial, no card needed.
Frequently asked questions
What is the main difference between Cp and Cpk?
Cp compares the tolerance width with the process spread and ignores where the process is centered. Cpk compares the distance from the mean to the nearest spec limit with half the process spread. Cp shows what the process could do if centered, while Cpk shows what it actually does at its current aim.
Can Cpk be higher than Cp?
No. Cpk equals Cp only when the mean sits exactly at the midpoint between the spec limits. Any shift away from the midpoint lowers Cpk while Cp stays the same. If a report shows Cpk above Cp, check the inputs, especially the spec limits, the sigma estimate and how the mean was calculated.
Which matters more in the Cp vs Cpk comparison?
Cpk matters more for judging current output, because it reflects both spread and position. Cp still earns its place, since comparing it with Cpk tells you whether a low score comes from aim or from variation. Report both, then decide whether to re-center the process or work on reducing its variation.
Why can't I calculate Cp with a one-sided specification?
Cp needs a tolerance width, which is the upper limit minus the lower limit. With only an upper or only a lower limit, there is no width to compare against. Use Cpu for a maximum-only characteristic or Cpl for a minimum-only characteristic, and report that value as the Cpk for the study.
How much data do I need for a Cp and Cpk study?
A practical guide is about 25 subgroups or 100 individual values from a stable process. Check a control chart first, look at the histogram for a roughly normal shape, and confirm your gauge is good enough with a gauge R&R study. Smaller samples give a rougher estimate of sigma and a less reliable index.