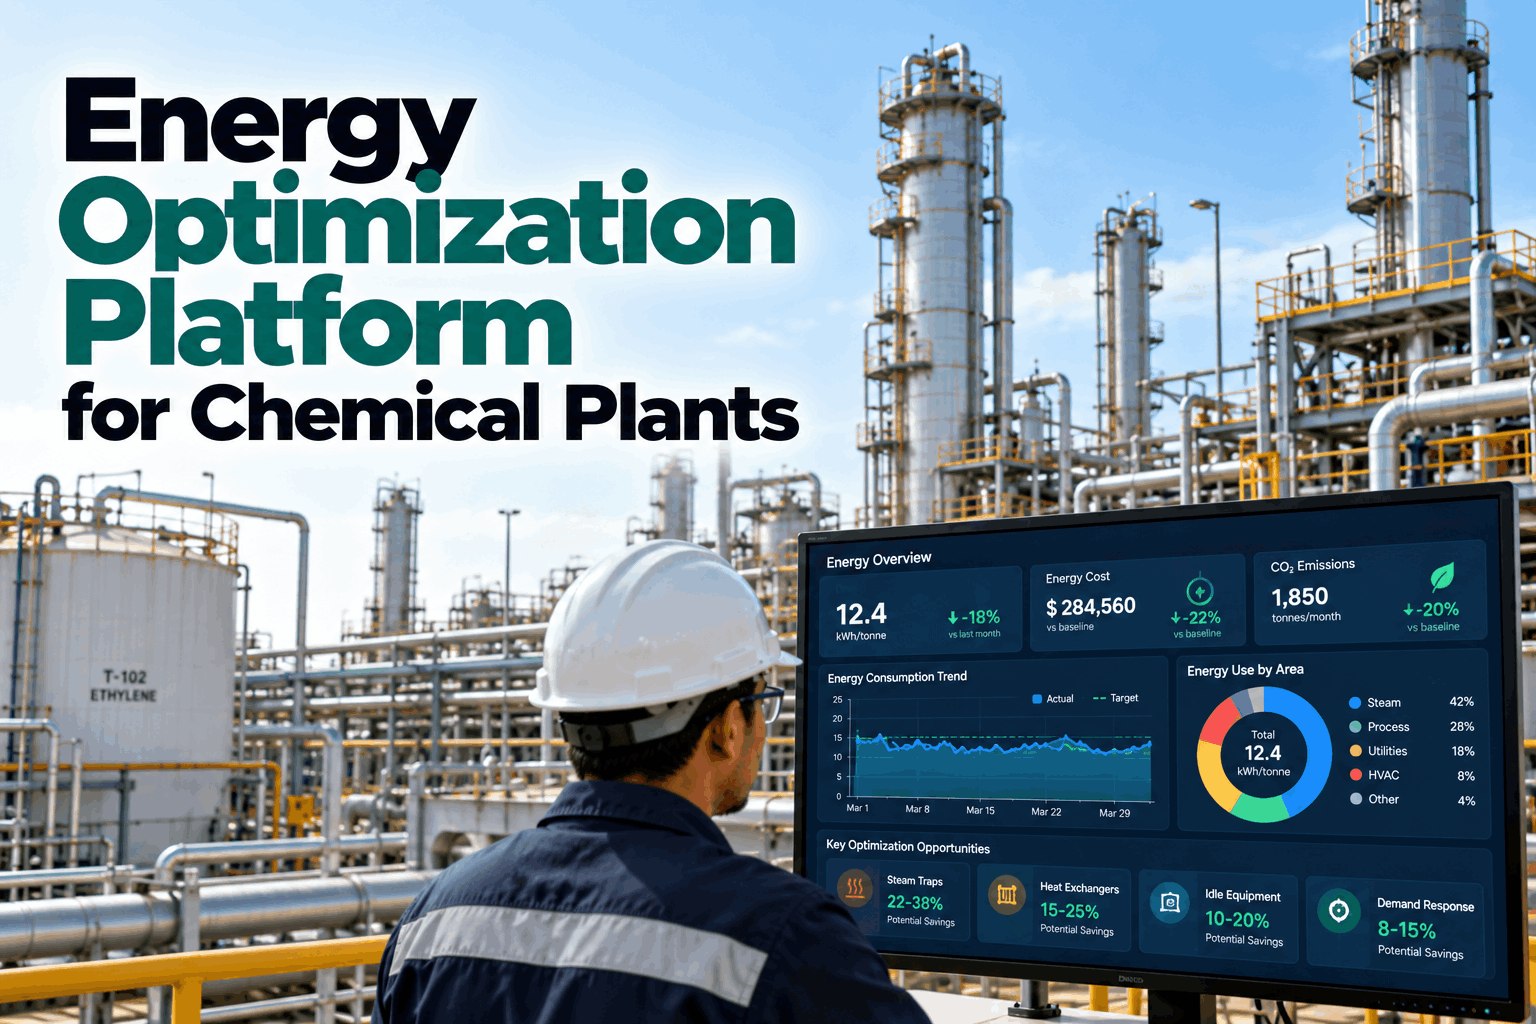
A chemical plant's energy bill has two parts. One is the energy the chemistry needs. The other is energy that buys nothing: steam blowing through a failed trap, extra heat pushed through a fouled exchanger, a chiller running between batches, a demand charge set by one bad half hour. The second part is hard to see because it is mixed into the first. iFactory's Energy Optimization Suite separates them. It works out what your plant should have used for the tonnes it made, compares that with what it did use, and names the equipment behind the gap. To see it on your own data, book an energy session.
Energy Optimization Platform for Chemical Plants
Find the energy your plant uses but does not need: failed steam traps, fouled exchangers, idle equipment and avoidable demand peaks. Delivered turnkey, and run on your own site.
- A baseline that shows expected against actual, every day
- Four kinds of hidden waste, traced to named equipment
- EnPIs and records ready for ISO 50001
Hidden Waste Is a Gap, Not a Guess
Expected energy on one side. Actual energy on the other. The difference is what you hunt.
Energy use in a chemical plant rises and falls with production, product mix and weather. That makes a monthly bill almost useless for spotting waste. The platform builds a baseline instead: a model of what the plant should use for what it made that day. Any day that lands above the baseline has energy with no production reason behind it. Our support team can show how a baseline is built from your own meters.
One dot for each day
Illustrative. The ringed dot is yesterday: 150 tonnes made, 498 MWh used.
Three terms, one example
- Baseline. What the plant should use. Here: 180 MWh a day of base load, plus 1.9 MWh for each tonne. For 150 tonnes, that is 465 MWh.
- EnPI. An energy performance indicator. Here: actual against baseline. 498 against 465 is 7.1% over.
- SEC. Specific energy consumption, or energy for each tonne. 498 ÷ 150 is 3,320 kWh per tonne, against 3,100 expected.
All energy, fuel and power together, expressed in one unit.
On a 75 tonne day the same plant, with no waste at all, would use about 4,300 kWh per tonne. The base load is simply spread over fewer tonnes. Judge a slow day by SEC alone and it looks wasteful when it is not. A baseline that separates base load from load that follows production avoids that trap.
Four Kinds of Waste the Platform Looks For
Each one hides in a different place, and gives itself away through a different signal.
A gap above baseline is only useful if you know what caused it. The Energy Optimization Suite looks for four common causes, using signals your control system mostly already records. To check which of the four are likely on your site, book a site walk-through.
What published sources say about each
Steam traps
The share that may have failed in a steam system left three to five years without maintenance, per US DOE guidance.
Fouling
The share of GDP that exchanger fouling is estimated to cost industrialised countries, in a widely cited academic review.
Idle running
We found no reliable average. It is simple to measure: compare running hours with production hours.
Flexible loads
The cost saving reported in one scheduling study, as cited in the trade journal Chemical Processing.
Figures from the sources named. None is a promise for your site. The pilot measures what is true for your plant.
Nearly half the energy used in chemical manufacturing is steam, so that is where the largest gaps tend to sit. The same US Department of Energy assessment found that single steam improvements each saved between 0.6% and 5.2% of fuel, and that most paid back in under 24 months. Small fixes, repeated across a site, add up.
One Day, Explained
The platform does not stop at "you were over". It splits the gap by cause, and says plainly how much it cannot yet account for.
Demand Response Without Risking the Batch
Move the loads that can move. Leave the chemistry alone.
Much of an electricity bill is set by when power is used, not only how much. Shifting a flexible load by an hour can cut a demand charge or earn a payment from the grid. In a chemical plant the hard part is knowing which loads are truly flexible. The platform forecasts site demand and suggests what could move. Your operators decide. Our utilities specialists can help map your loads.
Loads that can often move
- Batch start times and cleaning cycles
- Drying and milling campaigns
- Pre-cooling by refrigeration plant
- Electrolysis and air separation
- Utilities that are not critical to the process
Limits that do not move
- Product quality and delivery dates
- Catalysts that dislike sudden changes
- Minimum run lengths
- Tank space to buffer product
- Safety margins and interlocks
Both lists follow an article in Chemical Processing by a Schneider Electric author.
Map each large load
For every big user, write down what it needs, how fast it can ramp and what it must never do.
Run a shadow schedule
For four to eight weeks, let the platform plan the shifts on paper only, and count what they would have saved.
Then decide
Join a grid programme or change the schedule only if the shadow results justify it.
Built for ISO 50001: Baselines, EnPIs and Evidence
The standard asks you to prove improvement. The platform keeps the proof.
An energy management system under ISO 50001 needs an energy review, a baseline, performance indicators and records that show performance getting better. Most plants assemble these by hand before each audit. The platform produces them as a by-product of running every day. It supports your EnMS. It does not replace it, and it does not certify you. To see the reports, book a report review.
For most chemical sites, the quickest route to lower emissions is to stop wasting fuel and power. The platform converts each saving into tonnes of CO2 using the emission factors you supply, so the energy work feeds straight into your decarbonization reporting.
From Yearly Audit to Daily Answer
An audit is a photograph. A plant needs a film.
An energy audit is valuable, but it describes the week the auditor was on site. Traps fail, exchangers foul and schedules change the week after. The platform keeps looking. It also runs on a server inside your own network, which matters to plants that will not send process data outside. Our integration team can confirm what your systems already record.
An energy audit gives you
- A snapshot of one period
- A list of projects, with estimated savings
- Expert eyes on the whole site
- No way to see what changed afterwards
The platform adds
- A check every day, against a baseline
- New waste flagged as it appears
- Savings measured after each fix, not assumed
- Data and models that stay on your own site
How a finding becomes a saving
Detect
A day, a unit or a utility lands above its baseline.
Explain
The gap is matched to a cause and to named equipment.
Size
The loss is given in MWh and in money for each day it continues.
Assign
The finding goes to an owner, with the evidence attached.
Fix
Your team repairs, cleans or changes the routine.
Verify
The saving is measured against the baseline, and kept on record.
One set of data, three views
- Energy manager. The daily gap, split by cause, with EnPIs and reports.
- Utilities operator. Suspect traps, fouling trends and the next demand peak.
- Plant manager. Energy and cost per tonne, by unit and by product.
iFactory advises. It does not change set-points or schedules on its own.
Turnkey AI: Delivered, Connected and Live in 6–12 Weeks
You do not build this. It arrives ready.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready, with the software pre-loaded. Rack it, plug in power and Ethernet, and the AI is live on your network.
Our team handles cabling, network setup, PLC and SCADA integration, operator training and 24×7 remote monitoring. The server sits inside your own network, so energy and process data stay on site. For a scope matched to your site, request a turnkey quote.
Ship, network and data
Server installed. Energy meters, control system tags and the production record connected. Meter gaps listed.
Model training and pilot
Baseline built from your own history. First gaps explained and checked on the plant by your engineers.
Go-live and training
Daily reports and EnPIs live. Energy, utilities and operations staff trained. 24×7 remote monitoring begins.
Frequently Asked Questions
What does an energy optimization platform do?
It compares the energy a plant used with the energy it should have used for what it made, every day. When the two differ, it traces the gap to causes such as failed steam traps, fouled exchangers, idle equipment or demand peaks, and tracks the saving once each is fixed.
How much hidden waste can it find?
That depends on the site, and any range quoted in advance is an estimate. As one reference point, a US Department of Energy assessment found 12.4% potential fuel savings in chemical industry steam systems alone. A pilot on your own data gives the real figure.
Do we need new sensors?
Often not to begin. Baselines, fouling trends and idle running use meters and control system tags most plants already have. Pinpointing individual steam traps is the exception. That works best with trap sensors, and without them the platform narrows the loss down to a header.
Does it change set-points or schedules?
No. It advises. It shows the gap, the likely cause and the cost of waiting, and your engineers and operators decide what to do. Any change to plant settings goes through your normal approval route.
How does it support ISO 50001?
It provides the measurement side of an energy management system: an energy baseline, EnPIs, continuous monitoring and a record of each improvement with its measured saving. Policy, targets, action and certification stay with your organisation and your certification body.
Why run it on-premise?
Energy data reveals production rates, recipes and schedules. Many chemical sites prefer not to send that outside. The server sits inside your network, the data and models stay on site, and the platform keeps working if the outside connection is lost.
How long does it take to go live?
Six to twelve weeks from delivery. We need a place for the server with power and Ethernet, read access to energy meters and control system tags, and a year of production history if you have it. To check your set-up first, contact our team.
Bring One Month of Energy Data
In thirty minutes we plot your own days against tonnes made, draw a first baseline and show which days sit above it. You keep the chart whether or not you go further with iFactory.
- 1Daily energy use by utility, for one month
- 2Daily tonnes made, by product
- 3A list of your largest energy users
- 4Your last steam trap survey
- 5Your electricity tariff, with the demand charge