The four-point system is the most widely used way to grade fabric rolls, and most mills still run it on paper. An inspector watches cloth pass over a lit frame, judges the length of each flaw, writes points on a sheet and adds them up at the end of the roll. The rules are simple. Applying them the same way on every roll, every shift and every inspector is not. This checklist explains the ASTM D5430 scoring rules, shows the math with a worked example, and sets out how digital scoring and AI vision make four-point results consistent enough to trust, audit and share with buyers. If you want to see a roll scored live, a short walkthrough shows the full flow.
Four-Point Fabric Inspection Software: Digital Scoring That Grades Every Roll the Same Way
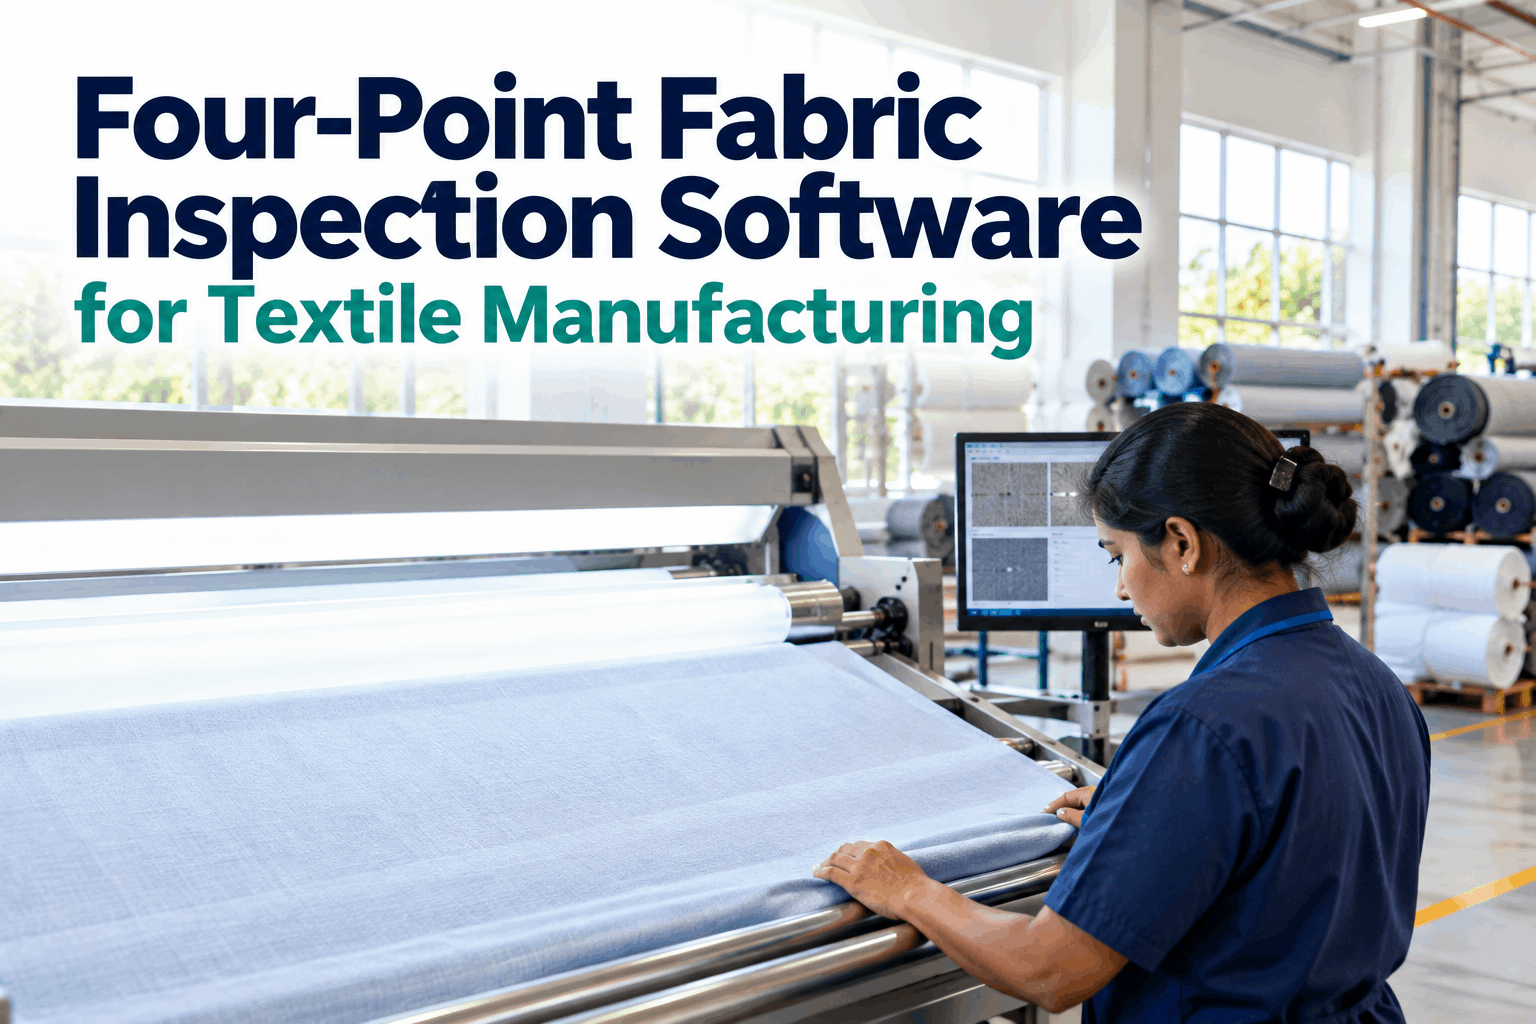
Defects found, sized and scored against ASTM D5430 rules as the fabric runs, with points per 100 square yards calculated automatically for every roll.
Why Paper Four-Point Scoring Breaks Down
The four-point system looks objective. A defect is measured, a number of points is assigned and the roll either passes or fails. In practice, the measurement happens by eye at inspection speed, and small differences add up. One inspector calls a slub 3 inches and gives it 1 point. Another calls it 4 inches and gives it 2. One counts a continuous streak yard by yard, another counts it once. Across a 120-yard roll those judgments can move the final score by enough to change a pass into a fail.
The paper sheet also hides what matters most after the roll is graded. Nobody can easily see where in the roll the defects sat, whether the same flaw repeats every few yards, or which loom produced the worst rolls this week. The score is recorded, but the pattern behind it is lost. That is a problem because fabric quality drives garment quality: a widely cited textile research survey notes that fabric defects account for about 85% of the defects found in the garment industry, and that second-quality fabric sells for 45–65% less than first quality.
Digital scoring fixes the consistency problem first, then turns every scored roll into data your team can act on. You can review how that works on your own fabrics with our QC team.
The ASTM D5430 Four-Point Rules in Plain Terms
ASTM D5430 sets out the test methods for visually inspecting and grading fabrics, and the four-point system is the scoring option most buyers name in their quality manuals. The core rules fit on one card, but each has a detail that trips up manual inspection.
The formula is simple: points per 100 square yards equals total points multiplied by 3,600, divided by the cuttable width in inches multiplied by the yards inspected. Many factories treat 40 points per 100 square yards as the acceptance limit, but buyers set their own levels by fabric type. Our engineers can map your buyer rules into the scoring logic.
Scoring One Roll From Start to Finish
Here is how a single roll moves from individual defects to a pass or fail decision. The numbers are an example, but the method is exactly what the standard describes and what digital scoring automates.
The per-yard cap applies before the total is added. If two of the short defects had fallen in the same yard as a long one, that yard would still be capped at 4 points.
Two details matter in the example. First, the width in the formula should be the cuttable width, not the full width including selvage. Using the wrong width shifts every score in the lot. Second, the per-yard cap has to be applied to the right yard, which means the position of every defect must be known. On paper, position is rarely recorded. In digital scoring, every defect carries its yard position, so the cap is applied correctly every time.
A roll that scores 18.6 on paper might score 22 or 15 with a different inspector. The math is not the issue; the inputs are. That is why consistent defect sizing is the real goal of any scoring tool.
The Four-Point Inspection Checklist
Use this checklist to run four-point inspection the same way on every frame and every shift. It works for manual, digital and AI-assisted inspection alike, because the rules stay the same; only the way defects are found and sized changes.
Printing the checklist is a start. Building it into the software, so a roll cannot be closed without width, position and cap checks, is what makes it stick. Ask our support team for a template matched to your buyers.
What Changes When Scoring Goes Digital
Digital four-point scoring does not change the standard. It changes how reliably the standard is applied and how much you learn from each roll.
- Defect length judged by eye at speed
- Yard position rarely recorded
- Per-yard cap applied inconsistently
- Math done by hand at the end of the roll
- Results filed, seldom analyzed
- Buyer disputes settled by memory
- Defect length measured from the image
- Every defect tagged with its yard position
- Cap applied automatically per yard
- Score calculated live as the roll runs
- Points trended by loom, lot and shift
- Buyer receives the defect map with the roll
The biggest gain is not speed. It is agreement. When two frames score the same roll the same way, the grade means something, and the conversations with buyers and weaving rooms move from arguing about the number to fixing the cause.
Most mills start by digitizing the sheet on a tablet, then add cameras once the data habits are in place. That path is covered in a short demo.
How AI Vision Finds, Sizes and Scores Defects
AI vision takes the most error-prone step, spotting and sizing each defect, and makes it repeatable. Line-scan cameras image the full width of the fabric as it runs. A trained model flags anything that looks like a flaw, classifies it, measures it and passes the result to the scoring engine.
Cameras image the full width under steady lighting at inspection speed.
The model flags slubs, floats, holes, stains, broken ends and more.
Each defect is sized on its longest dimension in inches.
Points are assigned, yard caps applied and the roll total recalculated.
The roll is passed, held or failed against the buyer limit.
The inspector stays in charge. Borderline calls are queued for a human to confirm, and every confirmation teaches the model more about your fabrics. Over time, the share of defects that need a human decision falls, and the inspector spends their time on the hard cases rather than on every slub.
Detection quality depends on lighting, fabric type and defect library. Our engineers run a trial on your own rolls before anything is committed.
Where Four-Point Scoring Usually Goes Wrong
Most scoring disputes come from a handful of repeat mistakes. Each one is easy to prevent once it is named.
A 3.2 in defect scored as 1 point instead of 2. Boundary calls are where inspectors disagree most.
Several defects in one yard added without the 4-point cap, inflating the roll score.
A broken end running 12 yards charged once instead of 4 points per affected yard.
Including selvage in the formula lowers every score and hides problem rolls.
Shade variation is judged separately; folding it into points confuses both results.
Without yard positions, nobody can check the cap or plan cutting around defects.
Digital scoring blocks most of these by design: sizes come from the image, caps are automatic and a roll cannot close without position data. See the rules engine in a live session.
How iFactory Delivers Four-Point Scoring
Cameras and lighting fitted to your existing inspection frames.
ASTM D5430 rules with your buyer limits built in.
Every defect stored with yard position, size and image.
Borderline calls routed to a human for confirmation.
Pass, hold or fail tagged live with the score.
Repeat defects sent to weaving, knitting or dyeing the same shift.
It works alongside your ERP and roll labels rather than replacing them. Share your buyer manual and we will show the rules running in a scoring demo.
Score Your Own Rolls the Same Way Every Time
Run a pilot on one inspection frame. We fit cameras, load your buyer limits and score your rolls side by side with your inspectors, so you can compare results roll by roll.
Three slubs and one 7 in float scored in the first 60 yards. The roll is trending toward the buyer limit.
What a Scored Roll Looks Like on the Floor
Here is a typical exchange between a QC supervisor and iFactory at the start of a shift, showing how scores turn into decisions rather than paperwork.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the fabric defect and four-point scoring models loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our scope covers cameras and lighting on inspection frames, PLC/SCADA and ERP integration, cabling and network setup, operator and QC team training, and 24×7 remote monitoring.
Server installed, cameras and lighting mounted, historical inspection and defect records loaded.
Models trained on your own fabrics and styles, then piloted on one line with your QC team reviewing every call.
Rollout to the agreed lines, inspector and supervisor training, ERP hand-off and 24×7 remote monitoring in place.
Hardware, software and integration come as one package. For pricing on your frame count, contact our sales team.
Frequently Asked Questions
It is a method under ASTM D5430 for grading fabric rolls by assigning 1 to 4 penalty points to each defect based on its size, with holes scored at 2 or 4 points. Points are capped at 4 per linear yard and converted to points per 100 square yards so rolls can be compared.
Multiply total points by 3,600, then divide by the cuttable width in inches multiplied by the yards inspected. For example, 36 points on a 120-yard roll with 58 inches of cuttable width gives about 18.6 points per 100 square yards.
Many factories use 40 points per 100 square yards as the acceptance limit, but there is no single rule. Buyers set their own limits by fabric type and end use, so the software should hold a limit per buyer and article.
AI takes over the repetitive work of finding and sizing defects, but inspectors stay in charge of borderline calls, shade judgments and final decisions. Most mills use AI to make scoring consistent and to free inspectors for the hard cases.
Usually not. Cameras and lighting can be fitted to existing inspection frames, and the scoring runs on a server on your network. Frame condition, speed control and lighting are checked during the site survey.
A typical rollout takes 6–12 weeks: installation and data setup first, then model training and a pilot on one frame, then go-live and training. You can plan the scope with our team.
Make Every Roll Grade Mean the Same Thing
iFactory finds, sizes and scores every defect against ASTM D5430 rules and your buyer limits, and hands each roll a grade with the defect map to prove it.
Longer bars mean more points. Roll 4472 is over a 40-point limit and goes on hold with its defect map.