Every OEE figure rests on one number that almost nobody checks: the ideal cycle time, or its twin, the ideal run rate. It is the speed your line is measured against. Set it too slow and every shift looks better than it was. On most food and beverage lines it was typed into a spreadsheet years ago, copied from a budget, and never looked at again. This guide shows how to set it properly: start from the OEM design speed, apply only the correction factors that are real, and check the result against what the line has actually done. It also shows how iFactory keeps the standard honest for every product. To review yours with us, book a speed review.
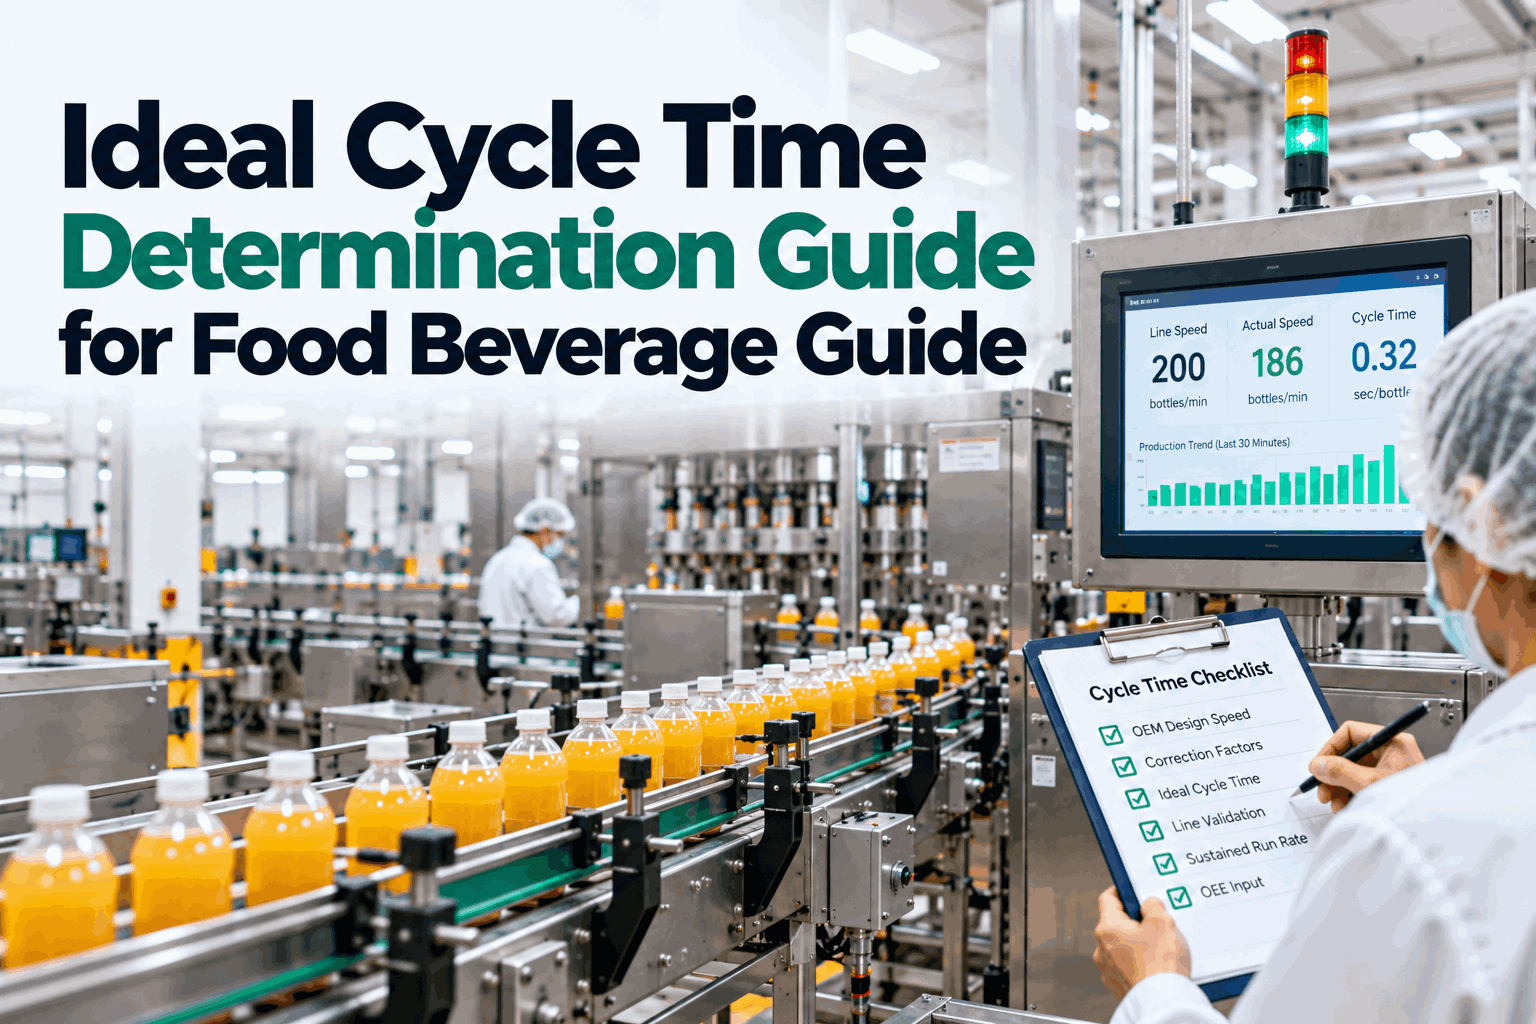
Ideal Cycle Time Determination Guide for Food and Beverage Lines
Set the speed standard from the machine's design speed and real correction factors, not from a guess, a budget or last year's average.
- A three-step method anyone can follow
- Which correction factors are real, and which are excuses
- A worked example for four products on one line
For the machine that limits the line.
Physical limits only, each with a reason.
If the line has beaten it, it is too low.
One for each product on each line.
What Ideal Cycle Time Is, and Why It Moves Your OEE
It is the fastest the line can make one good unit of this product. Everything slower is a loss you want to see.
Ideal cycle time is the time for one unit at the theoretical top speed. Ideal run rate is the same thing turned over: units a minute. The performance part of OEE compares what you made with what the ideal rate says you could have made, so the lower you set the ideal, the better you look. Our support team can check which standard your reports use.
The line ran at 500 a minute in all three cases. Performance changes by 13 points because of the number it is divided by.
Four speeds people confuse
- Ideal rate. The fastest the process can support. Used for OEE.
- Budget or standard rate. What finance plans on. Slower, on purpose.
- Takt. How fast you need to make to meet demand. Nothing to do with capability.
- Average rate. What you usually get, losses included.
Only the first belongs in an OEE calculation.
Step 1: Start From the OEM Design Speed
The builder has already told you how fast the machine was designed to run. Begin there, not with an opinion.
The design speed is written down in more places than most plants realise. Find it for the machine that limits the line, in the units you count in, for a named base product. That gives you a starting figure that came from engineering, with a document behind it. To trace the design speeds for your own lines, book a working session.
The nameplate
The rated output on the machine itself, and in its manual.
The OEM speed chart
Rated speed for each container size and product type.
The acceptance test
What the machine actually proved at hand-over, on your products.
The contract
The output the supplier guaranteed, and under what conditions.
Lines are built so that machines either side of the filler run faster than it does. The filler is the heartbeat, so its design speed is the line's ideal rate.
Three things to pin down
- The machine. Use the one that limits the line, not the fastest or the newest.
- The unit. Bottles, packs or cases. Count and standard must use the same one.
- The base product. Design speed is always quoted for a particular size and product. Write down which.
A European standard, EN 415-11, sets out how efficiency and acceptance tests for packaging lines should be defined. It is a useful reference when the documents disagree.
Step 2: Apply Only Real Correction Factors
A real factor is a limit of physics or of the product. Anything else is a loss wearing a disguise.
Design speed is quoted for one base product. A larger bottle fills more slowly. A fizzy drink foams. These are real, and the builder's own charts usually give the figure. What is not real is a factor for an old machine, a short crew or frequent jams. Those are the very losses OEE exists to show. Ask our line specialists to review your factors.
Real: limits of the product
- Container size. A bigger fill volume takes longer.
- Product behaviour. Foaming, thickness, particles, fill temperature.
- Pack design. A light bottle or thin film that cannot be handled faster.
- Process rules. A heat hold time or fill accuracy that sets a ceiling.
Each should come from the OEM chart, an acceptance test or a recorded trial.
Not real: losses in disguise
- "The machine is old." Wear is a speed loss to measure.
- "We are short of people." A staffing loss, not a machine limit.
- "It jams above that speed." A fault to fix.
- "That is what we normally run." An average, with every loss inside it.
- "That is the budget rate." A planning number.
Would this factor still apply if the line were in perfect condition, with a full skilled crew and materials in specification? If yes, it is real. If no, it is a loss, and it stays out of the standard.
Worked example: four products on one filler
Illustrative figures. One rate for all four products would be wrong for at least three of them.
A factor with no source is a guess that happens to have a decimal point. Beside every factor, record where it came from: the page of the OEM chart, the acceptance test, or the date and result of a trial. When someone asks in two years why the standard is 540, the answer should take ten seconds to find.
What a Soft Standard Hides
A standard set 10% too low does not look like a problem. It looks like a good shift. This is what it conceals on one product.
Step 3: Check It Against What the Line Has Done
A standard the line has beaten is not a standard. A standard the line never gets near needs a second look too.
Now test the paper figure against history. Find the best steady run for each product: a full hour with no stops and product in specification. Then compare. The rule is simple: the ideal rate is the faster of the corrected design speed and the best run the line has truly sustained. To run this check on your own data, book a validation session.
Illustrative. Two standards hold, one is proven too low, and one shows a gap that is either a hidden limit or a long-standing speed loss.
Never beaten
If any steady hour beats the standard, raise the standard to that hour.
Never far away
If the best hour is well short of the standard, look for a real limit or a chronic loss.
Never left alone
Check again after any new format, material, machine change or overhaul.
Nameplate or best run: which wins?
Practitioners disagree. Some trust the nameplate. Others say nameplates are cautious and prefer the best run on record.
You do not have to choose. Work out both and take the faster. If the nameplate is higher, the gap is a speed loss to chase. If the line has run faster, the nameplate was cautious and the line has shown what it can do.
What counts as a best run
- At least a full hour, not a lucky five minutes
- No stops inside it, long or short
- Product inside specification throughout
- Normal materials and a normal crew
If the line cannot hold any steady hour at all, fix the stops first. Speed comes after.
Keep the Standard Honest
A speed standard is a measuring stick. Somebody has to own it, and it must not bend when results are poor.
Once set, the standards belong in a short register: one row for each product on each line, with the source of every figure. Changes go through engineering, not through whoever is having a bad month. iFactory keeps that register live, and flags any product that beats its standard or never gets near it. Our integration team can confirm what your lines already record.
Six traps to avoid
- One rate for every product. Wrong for most of them.
- A machine's rate used for a line. The line runs at its slowest machine.
- Mixed units. A standard in cases against a count in packs.
- Lowering it after a bad quarter. The stick has been cut to fit.
- Never raising it. Improvements vanish into a figure above 100%.
- No owner. Nobody can say who set it, or why.
What the register holds
- Line, limiting machine and counting point
- Product and format
- Design speed and its source
- Each factor, its reason and its source
- Ideal run rate and ideal cycle time
- Best steady hour, and the date
- Who approved it, and when it is next due
One set of data, three views
- Operator. Today's rate against the ideal for the product now running.
- Engineer. Every standard, its sources, and the products due for review.
- Plant manager. Performance that means the same thing on every line.
iFactory proposes changes to a standard. An engineer approves them.
Turnkey AI: Delivered, Connected and Live in 6–12 Weeks
You do not build this. It arrives ready.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready, with the software pre-loaded. Rack it, plug in power and Ethernet, and the AI is live on your network.
Our team handles cabling, network setup, PLC and SCADA integration, operator training and 24×7 remote monitoring. The server sits inside your own network, so production data stays on site. For a scope matched to your lines, request a turnkey quote.
Ship, network and data
Server installed. Counters, line states and product codes connected for one line. Design speeds and their documents gathered.
Model training and pilot
Best steady runs found for each product from live and past data. A draft register reviewed with your engineers.
Go-live and training
Approved standards go live in the OEE figures. Operators and engineers trained. 24×7 remote monitoring begins.
Frequently Asked Questions
What is ideal cycle time?
The shortest time in which the process can make one unit of a given product, in theory, with nothing going wrong. Its mirror image is the ideal run rate in units a minute. It is the yardstick for the performance part of OEE, so it has to be the true top speed, not a typical one.
How is it different from a standard or budget rate?
A budget rate is what the business plans to achieve, with normal losses built in. It is the right number for costing and scheduling. It is the wrong number for OEE, because it hides those same losses. Keep both, and never use one in place of the other.
Should we use the nameplate or the best run on record?
Work out both and take the faster. The corrected design speed tells you what the builder says is possible. The best steady hour tells you what the line has proved. Whichever is higher is the ideal. The other tells you something useful about the gap.
Which correction factors are legitimate?
Those that would still apply to a line in perfect condition: container size, how the product behaves when filled, the limits of the pack, and process rules such as a heat hold. Age, staffing, jams and habit are not factors. They are losses, and they belong in the OEE figure.
What should we do when performance goes above 100%?
Treat it as a finding, not a triumph. The line has shown it can run faster than the standard says. Confirm that the run was steady and in specification, raise the standard for that product, and record the date and the evidence.
How often should the standard be reviewed?
Whenever something physical changes: a new format, a new material, a machine modification or an overhaul. Also whenever a product beats its standard. Beyond that, a yearly look at the whole register is enough for most plants.
How long does it take to go live?
Six to twelve weeks from delivery for a first line. We need a place for the server with power and Ethernet, read access to counters and product codes, and whatever OEM documents you can find. To check your set-up first, contact our team.
Bring One Line and Its Speed Standards
In thirty minutes we take one line, look at the rates your OEE uses today, and mark which have a source and which do not. You keep the marked-up list whether or not you go further with iFactory.
- 1The standard rates in your OEE sheet
- 2The filler's nameplate or manual
- 3Any OEM speed chart or acceptance report
- 4Your main products and formats
- 5A shift where performance read over 100%