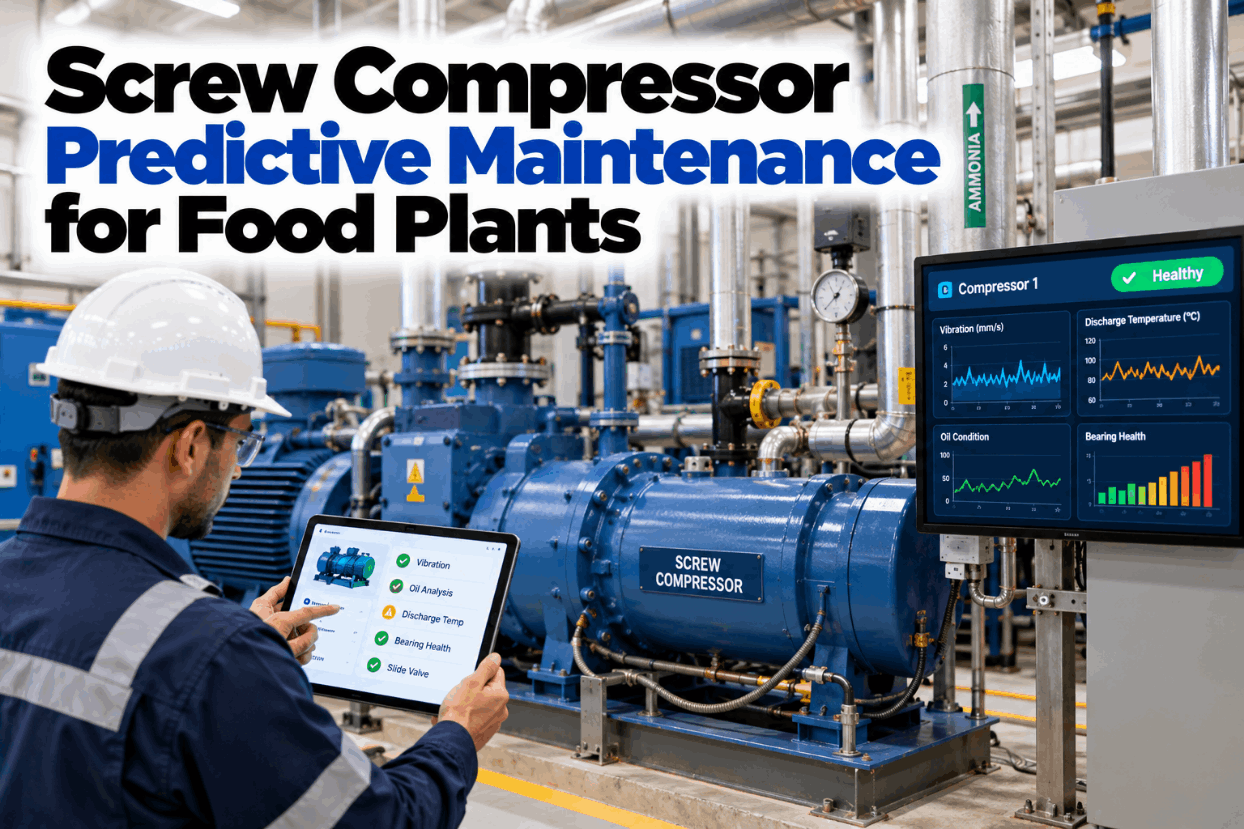
Screw Compressor Predictive Maintenance for Food Plants

By James C on October 22, 2026

screw-compressor-predictive-maintenance-food-plants

In most food plants, the ammonia screw compressors are the machines nobody thinks about until a cold room starts to warm up. They run for years with little fuss, then a thrust bearing or slide valve fails in the one week when every evaporator is calling for capacity. The early warning is almost always there, in vibration, oil and discharge temperature, weeks before the failure. This guide shows where to look and how to turn it into planned work. See it on real engine room data in a short compressor PdM demo.

PREDICTIVE AI · AMMONIA ENGINE ROOM

Fix the Screw Compressor in Spring, Not in the Heatwave

iFactory builds a vibration and oil model for each compressor, adds the readings your operators log by voice, and schedules the work order before peak cooling demand arrives. Repairs land in a month with spare capacity, not in the hottest week.

Compressor C-3 · ammonia screwWatch
Engine room 1 · slide valve 100% · 6,240 h since overhaul
Thrust bearing envelopeRising 4 weeks
Oil water, last sampleUp vs baseline
Discharge tempNormal for load
Amps at 100% slideNormal
Voice log · 06:10"C-3 oil filter diff up a little, oil level fine."
WO proposed: thrust bearing check · before 1 June
INSIDE THE MACHINE

Where an Ammonia Screw Compressor Wears

An oil-injected screw compressor squeezes gas between a male and a female rotor. Oil is injected to seal the rotor clearances, cool the gas and lubricate the bearings. A slide valve under the rotors sets capacity. Radial bearings carry the rotors, and thrust bearings at the discharge end take the axial load from discharge pressure. Each of these parts wears in its own way and leaves its own signal. Our refrigeration specialists can help you map your machines.

1
Suction-end radial bearingsSpall and wear under load. Show as bearing tones and rising envelope readings.
2
Male and female rotorsClearance grows with wear or contact. Lobe pass vibration and efficiency change.
3
Slide valve and Vi controlSticking, worn seals or a drifting position indicator. Capacity and amps stop agreeing.
4
Discharge-end thrust bearingsCarry the axial load. A frequent source of serious failures, and costly if missed.
5
Oil injection and coolingFilter, pump, cooler and separator. Problems show in oil pressure, oil temperature and discharge temperature.
REFRIGERATION COMPRESSOR FAILURE MODES

Each Fault, Its First Signal and How to Catch It

No single sensor sees every fault. Vibration finds bearing and rotor problems. Oil analysis finds contamination and wear inside the machine. Process data from the compressor panel finds slide valve, cooling and efficiency problems. Combining them is what turns a vague "it sounds different" into a dated work order. Walk through your compressor list in a failure mode review.

Component
Failure mode
First signal to look for
Best source
Thrust bearings
Spalling, cage wear, loss of preload
Bearing tones and envelope rise, axial vibration change, iron in oil
Vibration + oil
Radial bearings
Fatigue spalling, wear from dirty oil
Non-synchronous peaks, rising high-frequency energy
Vibration
Rotors
Clearance growth, rotor contact
Lobe pass amplitude change, higher discharge temp for the same load
Vibration + process
Slide valve
Sticking, worn seals, indicator drift
Slide position and motor amps no longer match baseline
Panel data
Oil system
Filter loading, cooler fouling, water ingress
Filter differential up, oil temp up, water in sample
Panel + oil lab
Shaft seal
Face wear, leakage
Rising seal leak rate, oil at the seal drain
Operator rounds
Coupling and alignment
Misalignment, element wear
2× running speed and axial vibration at the motor end
Vibration
AMMONIA COMPRESSOR VIBRATION

Reading the Spectrum: Running Speed, Lobe Pass and Bearings

A screw compressor has a few frequencies you can predict from its design. Each rotor turns at its own speed, and every time a lobe passes the discharge port it sends out a pulse, called the lobe pass frequency. Bearing defects make their own tones, set by bearing geometry, and are often clearest in an envelope or demodulated spectrum. Knowing where each one should sit lets the model tell normal machine sound from new damage. Our vibration team can work out the frequencies for your models.

Worked example · assumed design
Motor and male rotor speed3,550 rpm ÷ 60 = 59.17 Hz
Lobes, male : female4 : 6
Female rotor speed3,550 × 4 ÷ 6 = 2,366.7 rpm = 39.44 Hz
Lobe pass frequency4 × 59.17 = 236.7 Hz (same as 6 × 39.44)
Second harmonic2 × 236.67 = 473.3 Hz
COMPRESSOR OIL ANALYSIS

Four Oil Results That Tell You What Is Happening Inside

Oil is the compressor's blood test. Take samples from the same point, with the machine running, at a steady interval, so each result compares with the last. The lab sets limits for your oil type, but the trend matters more than any single number. Mixing the wrong oil also shows up. Additive elements such as zinc, phosphorus or calcium that your ammonia oil doesn't contain point to contamination. See oil trends beside vibration in a combined model demo.

ViscosityTrend
Thickening suggests oxidation or the wrong oil. Thinning points to dilution or a separator problem. Refrigerant in the sample can skew it, so labs degas first.
WaterAct early
Water in an ammonia system brings rust and iron wear. A rising trend means checking purgers, oil pots and how oil is stored and added.
Wear metalsTrend
Iron from bearings and rotors, plus other metals from cages and bushings. A sharp rise in iron with a bearing tone is a strong pair.
Acid or base numberTrend
Tracks oil breakdown. Some labs run base number instead of acid number for ammonia systems. Ask yours which it reports.
SLIDE VALVE AND DISCHARGE TEMPERATURE

When Discharge Temperature Climbs, Where to Look First

Discharge temperature only means something when compared with the same load and pressures. A reading that is normal at 50% slide valve may be high at 100%. The slide valve also changes the built-in volume ratio, or Vi, on many machines. If Vi doesn't match the system pressure ratio, the gas is over- or under-compressed, which wastes power and adds heat. The tree below is a starting point for diagnosis, not a replacement for the maker's manual. Our support team can share the full version.

Discharge temperature above baseline for the same load and pressures
Is oil temperature leaving the cooler also higher?
If yes
Oil cooling problemFouled oil cooler, starved thermosyphon feed, or high condensing conditions. Check liquid feed and cooler approach.
If no
Check injection and compressionLow oil injection flow from a loaded filter, wrong Vi for the pressure ratio, or growing rotor clearances. Compare filter differential and amps.

Engine Room Readings Spoken, Not Scribbled

Operators already walk the engine room every shift. With voice logging, each reading is spoken, checked against that compressor's normal range and added to its model. Odd values get a question back on the spot.

Engine room 1 · Operator and iFactory
OperatorC-3 discharge 180, oil out 135, slide one hundred, sounds normal.
iFactoryLogged in °F for C-3. Both in range for this load. Thrust bearing trend is still rising on vibration. Want me to book the oil sample early?
OperatorYes, pull it this week.
iFactorySample task raised for Thursday. Result will be added to the C-3 model.
ENGINE ROOM RELIABILITY

Daily Logs That Do Double Duty for IIAR 6 and PdM

IIAR 6 covers inspection, testing and maintenance of closed-circuit ammonia systems. Its compressor tasks include daily checks of suction and discharge pressure, oil pressure and temperature, discharge temperature, oil level, oil filter differential and abnormal noise or vibration, plus annual tests of safety cutouts. Where a plant holds 10,000 lb or more of ammonia, OSHA's process safety management standard, 29 CFR 1910.119, also applies, including mechanical integrity. Confirm the exact tasks against the edition your plant follows. See how daily logs feed the model in a logbook walkthrough.

Daily log · C-3Captured by voice 06:10
Suction pressureLogged
Discharge pressureLogged
Oil pressure and temperatureLogged
Discharge temperatureLogged
Oil level and filter differentialLogged · diff up
Noise or vibrationNormal by ear
Motor amps and alarmsPulled from panel
DailyOperator readings and checksFeed the trend model every shift
MonthlyUnloader and capacity control checksConfirm the slide valve responds
Planned intervalsOil samples and vibration routesOr continuous sensors on key machines
AnnualSafety cutout tests and alignmentRecords kept for PSM and audits
COOLING CAPACITY

Time the Work Before the Load Peaks

A compressor repair is easy in a month when the other machines can carry the load and hard in a month when they can't. Look at your own load profile, not the calendar. Many plants peak in summer, but seasonal products and blast-freezing campaigns can move it. The aim is to finish any planned repair while you still have spare capacity. The heat map below is an illustration for one plant. Plan your windows with our planning team.

Jan
Feb
MarWO window
AprWO window
May
Jun
JulPeak
AugPeak
Sep
Oct
NovWO window
Dec
Low loadMediumPeakPlanned work window
SCREW COMPRESSOR PREDICTIVE MAINTENANCE EXAMPLES

Three Patterns and What They Led To

These are illustrations of typical patterns, not customer case studies. Each shows how two signals together give enough confidence to plan the work. Talk through your own history in a data review.

Pattern A
Thrust bearing
SeenEnvelope readings rising for a month, iron up in the next oil sample
DoneBearing change planned in the spring window
Pattern B
Slide valve
SeenSlide shows 100% but amps match 80% of the usual full-load draw
DoneIndicator and valve checked on a low-load day
Pattern C
Oil cooler
SeenOil and discharge temps creeping up at the same load and pressures
DoneCooler cleaned and thermosyphon feed checked
SCREW COMPRESSOR PREDICTIVE MAINTENANCE COST AND ROI

Size the Value of Moving One Repair

The clearest value of compressor PdM is turning an emergency repair in peak season into a planned one in a quiet month. Every input below is assumed. Replace them with your own figures. Our team can help you build the case.

Unplanned, in peak season
Days out of service, assumed6
Rental cooling per day, assumed$2,000
Rental cost6 × $2,000 = $12,000
Overtime, assumed 40 h × $60$2,400
Event cost$14,400
Planned, in a low-load month
Days out of service, assumed4
Rental cooling neededNone, spare capacity
Rental cost$0
Overtime$0, normal hours
Avoided per event$14,400

Parts and labour are similar in both cases, so they cancel out. Product loss, if a cold room warms up, is left out on purpose. Add it only if your own records support a figure.

SCREW COMPRESSOR PREDICTIVE MAINTENANCE BEST PRACTICES

What Works and What Wastes Effort

Most compressor PdM programmes that stall do so for simple reasons: too few baselines, samples taken inconsistently, or alerts nobody owns. Compare notes with our reliability engineers.

AVOID
  • Judging readings without load and pressure context
  • Oil samples from different points or after shutdown
  • One alarm level for every compressor
  • Alerts that reach an inbox but no planner
DO
  • Baseline each machine at several slide valve positions
  • Sample oil at the same point, running, at fixed intervals
  • Pair vibration and oil before calling a bearing fault
  • Give every alert an owner and a target date
SCREW COMPRESSOR PREDICTIVE MAINTENANCE IMPLEMENTATION GUIDE

Five Steps From First Machine to Whole Engine Room

Start small and prove the signals on the machines that matter most at peak load. Each step below produces something the next one needs, so skipping one usually shows up later as noisy alerts. Plan the pilot with our reliability team.

1Pick the machinesTwo or three compressors you can least afford to lose in summer
2Gather historyPast oil results, overhaul dates, panel trends and alarm logs
3Add vibrationSensors or routes on rotor bearings, thrust end and motor
4Name the ownersWho acts on each alert, and by when
5Review and extendMonthly review of alerts, then add the rest of the fleet
TURNKEY AI DEPLOYMENT

Sensors, Models and AI Server for the Engine Room

iFactory delivers compressor PdM as a turnkey bundle. A pre-configured NVIDIA AI server ships racked and ready with the vibration, oil and process models pre-loaded, and connects to your compressor panels and existing sensors. You rack it, plug in power and Ethernet, and the AI is live. To scope it for your engine room, request a turnkey quote.

What's Included
  • Pre-configured NVIDIA AI edge server, racked and ready
  • Vibration sensors for compressor and motor bearings
  • Panel connection for pressures, temperatures, slide valve and amps
  • Oil lab result import with per-machine trends
  • Voice engine room logging for operator rounds
  • Work orders timed against your cooling load profile
  • 24×7 remote monitoring of models and hardware
Live in 6–12 weeks
Wk 1–4
Connect and Baseline

Server installed, sensors fitted, panels linked, past oil results loaded.

Wk 5–8
Tune per Machine

Normal ranges learned at each slide valve position, voice rounds started.

Wk 9–12
Alerts and Planning

Risk scores live, work orders timed to low-load windows, team trained.

HOW iFACTORY FITS

Compressor PdM Built Around Your Cooling Season

iFactory joins machine data, oil results and operator knowledge into one view per compressor. Our support team can walk you through a pilot plan.

1
A model per compressor. Vibration and oil trends judged against that machine's own normal.
2
Voice engine room logs. Operators speak readings, and odd values get a question back.
3
Load-aware context. Slide valve, pressures and amps keep readings in context.
4
WOs before the peak. Repairs are planned into windows when spare capacity exists.
1000+
Industrial clients running iFactory
99.9%
Platform uptime for round-the-clock cooling
6-12 wks
From racked server to live risk scores
FREQUENTLY ASKED QUESTIONS

What Engineers Ask About Screw Compressor PdM

What fails first on an ammonia screw compressor?
It varies with design, duty and oil condition, but bearings, especially the thrust bearings at the discharge end, are a common source of serious failures. Slide valve problems and oil system issues such as loaded filters or a fouled cooler are frequent too, though they are usually less costly if caught early.
How often should we sample compressor oil?
Follow the compressor maker's and your lab's guidance. Many plants sample on a fixed run-hour or calendar interval and shorten it when a trend starts to move. Consistency matters most: same point, machine running, clean bottle.
Do we need permanent vibration sensors?
Not always. Route-based readings work for many machines. Permanent sensors make sense on the compressors you can least afford to lose, or where load changes too often for monthly readings to compare well.
Why does slide valve position matter for the readings?
Vibration, discharge temperature and amps all change with load. A reading at 60% slide valve can't be judged against a baseline taken at 100%. The model learns normal behaviour at each position, so a real change stands out.
Does PdM replace IIAR 6 or PSM tasks?
No. Daily checks, cutout tests and mechanical integrity duties still apply. PdM adds earlier warning on top of them, and the voice logs can serve as the record of the daily checks.
How do we start?
Pick the two or three compressors you rely on most at peak load, gather their past oil results and panel data, and add vibration readings. Baselines form within weeks. Our support team can plan the pilot with you.

Know Which Compressor Needs Work Before Summer

Combine vibration, oil and engine room logs into one risk score per machine, and plan repairs while spare capacity exists. The full system is delivered turnkey and goes live in 6 to 12 weeks.
Example engine room summary
Compressors modelled5 ammonia screws
Watch listC-3 thrust bearing
Next oil samplesC-3 this week, others on cycle
Planned workBooked before peak load
Every repair timed to spare capacity

Share This Story, Choose Your Platform!