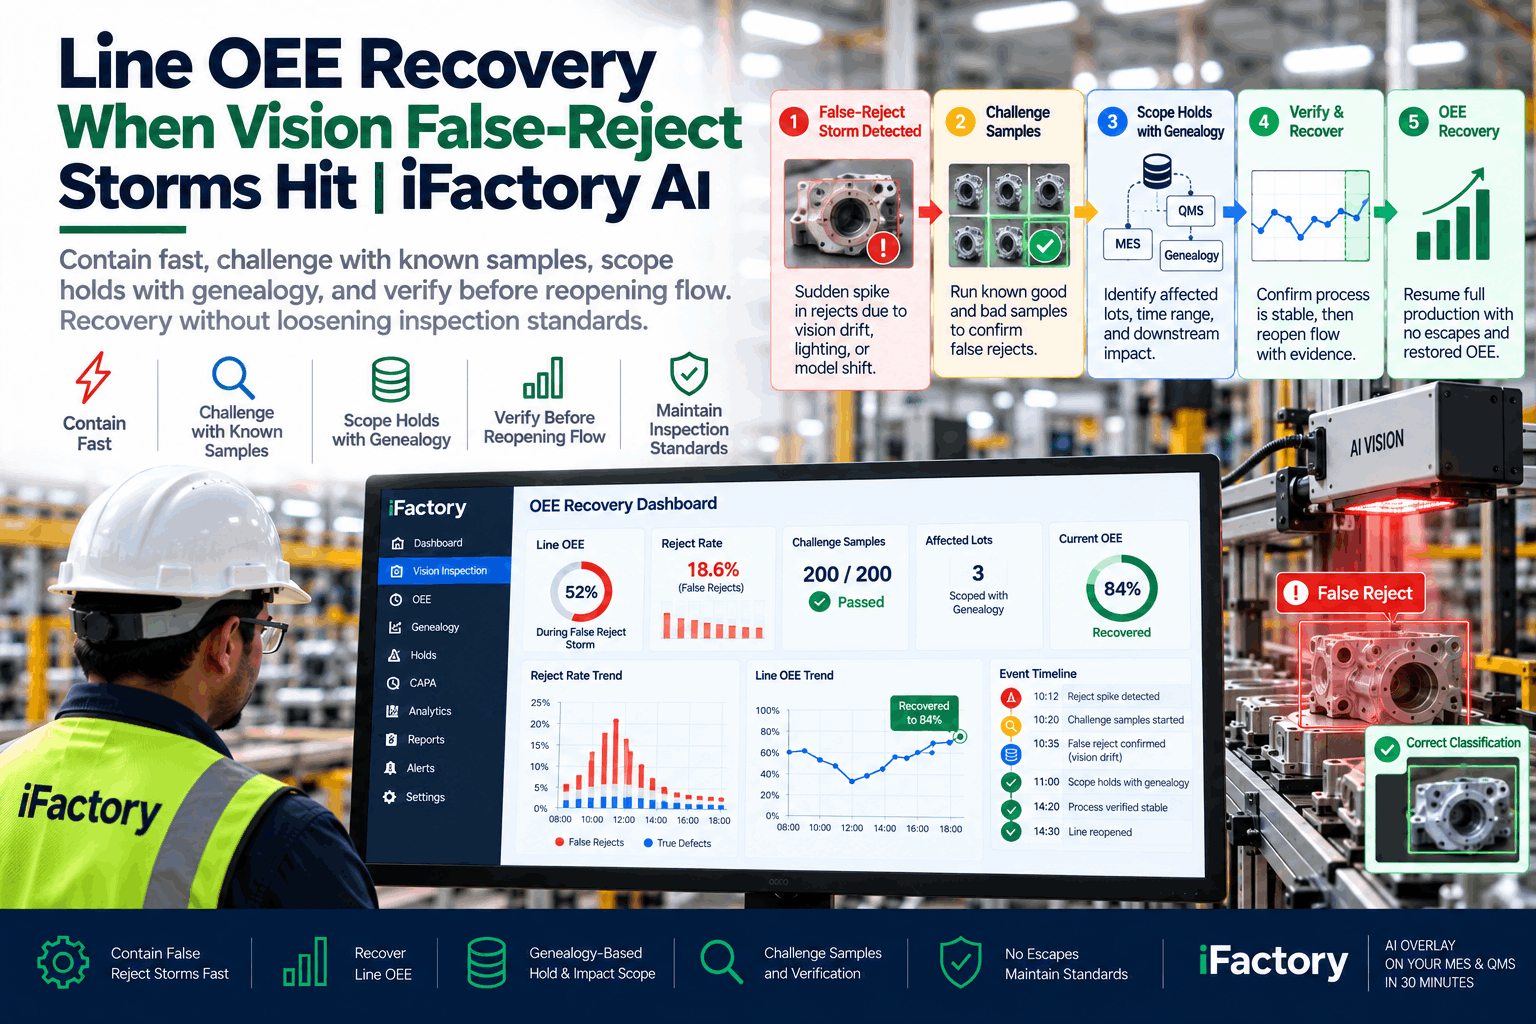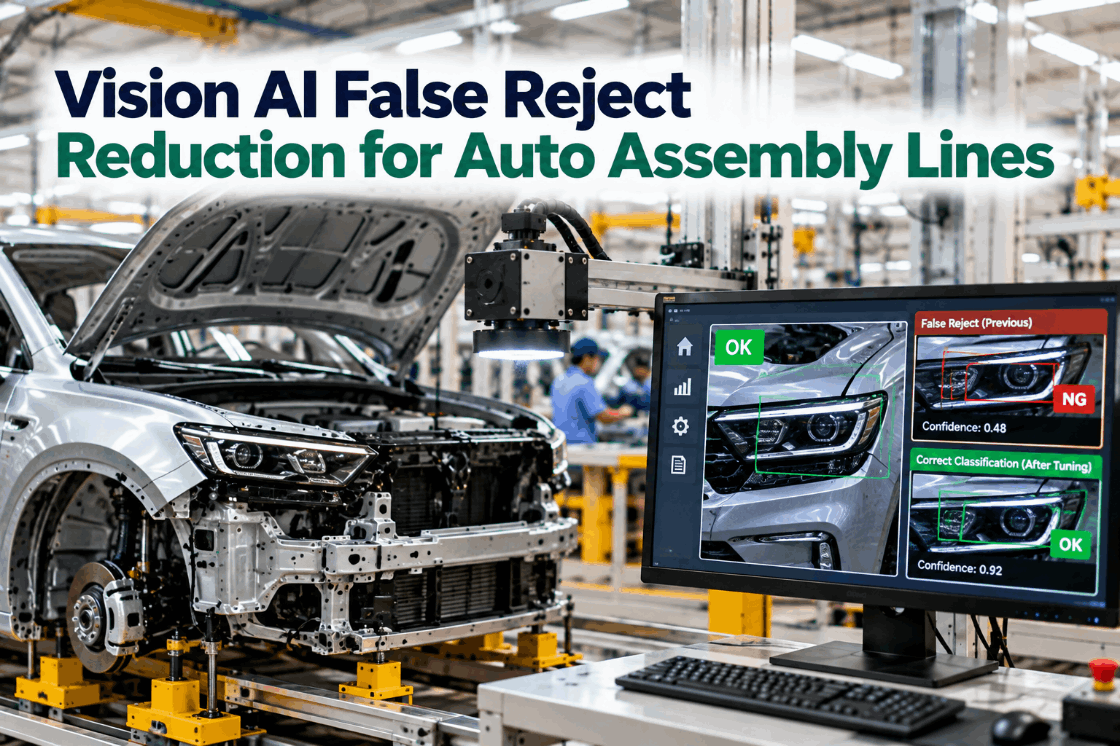
A vision system that rejects good parts does more damage than its reject count suggests. Every false reject sends a good part or vehicle into a repair loop, costs operator time and, worst of all, teaches the line to ignore the system. Once operators start overriding calls by habit, real defects slip through with them. Reducing false rejects is therefore about trust as much as efficiency. This guide explains how to measure false rejects properly, where they come from on automotive assembly lines, and the three levers that reduce them without letting misses creep up: confidence tuning, region-based sensitivity and human-in-the-loop feedback. To see those levers on your own stations, book a short walkthrough.
Vision AI False Reject Reduction for Auto Assembly Lines: Fewer Alarms, No Extra Misses
Confidence tuned by defect class, sensitivity set by region and every operator correction fed back into training, with misses tracked beside every change.
Why False Rejects Undermine the Whole System
False rejects look like a small cost: a good part is checked again and sent on. On an assembly line the cost compounds. Each false reject pulls a vehicle or part into repair or re-inspection, takes an operator away from the line and adds noise to quality data. When false rejects are frequent, operators learn that most alarms are wrong and begin to override them. At that point the system is still running but no longer protecting anything.
Human inspection has the same problem, which is often forgotten when AI vision is judged. A Sandia National Laboratories study of trained inspectors found they rejected 35% of acceptable parts while still missing some defective ones. People lean toward rejecting when unsure, and so do poorly tuned models. The aim is not zero false rejects at any cost; it is a false alarm rate low enough to keep trust, with misses held where they are.
Vendors sometimes promise large percentage cuts in false rejects. The honest answer is that the reduction depends on where your false rejects come from, which is what the rest of this guide helps you find. We can review your current reject data on a call.
How to Measure False Rejects Properly
You cannot reduce what you do not measure consistently. False rejects need a clear definition, a denominator and a partner metric that shows misses.
Record the cause of each false reject once it is known, too. After a few weeks, a simple count by cause, such as glare, texture or positioning, usually shows that one or two causes explain most of the problem.
Measure by station and by defect class, not only for the plant. A plant-wide false alarm rate of 3% can hide one station at 12% that operators have stopped believing. Per-station views are standard in our dashboards.
Where False Rejects Come From on Assembly Lines
Most false rejects trace back to a handful of causes. Each has a different fix, which is why diagnosis comes before tuning.
A single confidence threshold is too strict for some defect types and too loose for others.
Inspection regions that include edges, labels or textured areas invite harmless features to be flagged.
Reflections on paint or chrome and shadows from fixtures can look like scratches or dents.
New suppliers, colours or textures appear as defects until the model learns them.
If similar parts were labelled differently during training, the model learns the confusion.
Fixture wear or conveyor drift moves parts, so normal features fall into inspection regions.
Review a sample of false rejects by image before changing anything. The images usually point straight at the cause. Our engineers run this review in the first week of every tuning project.
Tuning Confidence Thresholds Without Trading Away Misses
Every deep learning call comes with a confidence score. The threshold decides where a score becomes a reject. Raising it cuts false rejects but can let real defects pass; lowering it does the opposite. The skill is in moving thresholds by defect class, with data on both sides.
| Threshold on scratch class | False alarm rate | Miss rate | Decision |
|---|---|---|---|
| 0.50 | 8.4% | 0.6% | Too many false alarms |
| 0.60 | 4.9% | 0.8% | Inside both limits |
| 0.70 | 2.7% | 1.6% | Inside limits, tighter margin on misses |
| 0.80 | 1.2% | 3.9% | Misses outside limit, reject |
In this illustrative example, 0.60 and 0.70 both meet the AIAG limits of under 5% false alarms and under 2% misses. Which to choose depends on the consequence of a miss for that defect class. For safety-related or customer-visible defects, the lower threshold is safer. For minor cosmetic classes, the higher one may be acceptable.
Two rules keep threshold tuning honest. Always evaluate on a validation set the model did not train on, including real defects at the edge of the specification. And never change a threshold without recording the new miss rate beside the new false alarm rate.
Threshold changes are process changes. They should be versioned and approved like any model release, which is built into our release workflow.
Region-Based Sensitivity: Strict Where It Matters
Not every part of a panel matters equally. A scratch on a visible door skin is a defect; the same mark on a flange hidden by trim is not. Region-based sensitivity lets the system be strict where customers look and relaxed where they do not.
Divide the part into regions using drawings and the customer’s appearance zones.
Set visibility classes, such as class A visible, class B partly visible, class C hidden.
Assign thresholds per region and defect class, strictest on class A.
Exclude labels, edges and features that should never be judged.
Check false alarms and misses by region on the master set.
Many OEMs already define appearance zones for paint and trim. Using the same zones in the vision system keeps inspection aligned with the customer’s own judgment and makes decisions easier to defend.
Regions are defined per body style, so the same logic follows each model on a mixed line. Region set-up is covered in a short demo.
Using Operator Feedback to Keep Improving
Operators see every reject, and they know which ones are wrong. Capturing that knowledge turns each false reject into training data rather than a frustration.
At the station, the operator marks each reject as confirmed or false with one touch.
Quality engineers review overrules daily, because operators can be wrong too.
Confirmed false rejects join the training set as good examples with clear labels.
The next model version is trained and checked on the master set for both misses and false alarms.
The version is approved and released, and the station’s false alarm rate is watched.
The review step matters. If every operator overrule went straight into training, a busy operator waving through real defects could teach the model to miss them. Engineering review keeps the feedback loop honest.
Over time, the share of rejects that need human review falls, and operators see the system learning from them, which rebuilds trust. The loop is shown on a live station view.
False Reject Reduction Checklist
Work through this checklist in order. Skipping straight to threshold changes is the most common mistake.
Most plants find that lighting, regions and missing good samples explain more false rejects than thresholds do. Our team can help with the first diagnosis.
How iFactory Reduces False Rejects
Confidence set by defect class with miss data alongside.
Strict on visible zones, relaxed or masked elsewhere.
Glare and shadows removed at the source.
One-touch confirm or overrule at the station.
Disputed calls checked before they enter training.
False alarms and misses reported together by station.
It works with your existing stations and quality systems. Share a week of reject data and we will show where your false rejects come from in a session.
Find and Fix the Sources of Your False Rejects
Choose the station operators trust least. We review its rejects, fix lighting and regions, tune by class and report false alarms and misses side by side for the pilot period.
False rejects on the grained door trim rose after a supplier texture change. The texture reads as fine scratches.
A False Reject Problem Traced to Its Cause
This exchange shows how a quality engineer might work through a false reject problem with iFactory.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the defect detection and false reject control models loaded. Rack it, plug in power and Ethernet, and the AI is live on your network. Our scope covers cameras and lighting at inspection stations and cells, PLC/SCADA and MES integration, cabling and network setup, operator and quality team training, and 24×7 remote monitoring.
Server installed, cameras and lighting mounted, PLC and MES links live, existing defect images and records loaded.
Models trained on your own parts, paint and variants, then run in shadow on one line with your quality team reviewing every call.
Rollout to the agreed stations under your change control, team training and 24×7 remote monitoring in place.
Hardware, software and integration come as one package. For pricing on your stations, contact our sales team.
Frequently Asked Questions
A false reject, or false alarm, is a good part or vehicle that the system flags as defective. The AIAG MSA manual measures it as false rejects divided by the number of good parts inspected.
The AIAG MSA attribute criteria treat a false alarm rate under 5% as acceptable, 5–10% as marginal and above 10% as unacceptable. Many plants set tighter internal targets for high-volume stations.
Fix causes first: lighting, inspection regions, positioning and missing good samples. Then tune thresholds by defect class, always measuring the miss rate beside the false alarm rate on a validation set.
It sets different sensitivity for different areas of a part, strict on visible appearance zones and relaxed or masked on hidden areas, often using the OEM’s own appearance classes.
No. Operators can be wrong, especially under pressure. Disputed calls should be reviewed by quality engineers before they are added to training data.
Diagnosis usually takes days. Fixes and retraining typically fit within a 6–12 week rollout, with changes run in shadow before release. Plan it with our engineers.
Make Every Alarm Worth Checking
iFactory cuts false rejects at their source and tracks misses beside every change, so operators trust the system and real defects never ride through with the noise.
Station 6 is over a 5% false alarm limit and has an open tuning action. Misses are tracked beside every change.