CNC predictive maintenance watches the parts of a machine tool that fail most often, such as the spindle, tool changer and ball screws, and warns before they stop a machining line. For automotive suppliers that matters twice over: a dead spindle halts deliveries, and a worn one drifts parts out of tolerance long before it fails. This guide explains what fails on CNC machines, which signals show it early, and how to turn a warning into a planned repair. To see predictive maintenance on your own machine data, book a short walkthrough.
CNC Machine Tool Predictive Maintenance for Auto Suppliers: Protect Spindles, Tool Life and Cycle Time
Spindle, tool changer and axis health tracked from signals your CNC already has, so repairs are planned weeks ahead and parts stay in tolerance.
Hydraulics, tool magazines, electrics and spindles lead the published failure studies.
Spindle load, servo load, alarms and tool-change times can be read without new sensors.
A new spindle can take months to arrive; a planned repair takes weeks.
Tracking machine health protects tolerance and cycle time, not just uptime.
Why CNC Failures Hurt Automotive Suppliers
Machining lines for engine, transmission, chassis and e-drive parts run close to capacity, so one stopped machine can hold up a customer.
- Tight delivery windows. Just-in-time supply leaves little buffer for a week-long repair.
- Long part lead times. Spindles and ball screws are not always on the shelf.
- Quality risk. A worn spindle or loose axis shows up as scrap and rework first.
- Shared bottlenecks. One machining center often feeds a whole assembly cell.
The Siemens figure is for large plants and is not a supplier average, but the direction is the same everywhere: unplanned stops cost far more than planned ones.
Knowing weeks ahead changes an emergency into a scheduled job. We can review your machine list on a call.
What Actually Fails on a CNC Machine
Field studies show failures spread across several subsystems, not just the spindle.
From a field study of twelve machining centers, as summarized by igus. Other studies give different splits.
A separate study of CNC machines found mechanical parts behind about 49% of failures, with electrical parts next. The exact split depends on machine type, age and duty.
A good program covers every subsystem with at least one signal. See a full machine health view in a demo.
Spindle Health: The Costliest Failure
Spindle bearings fail from contamination, imbalance, crashes and poor lubrication more often than from simple age.
- Contamination. Coolant, condensation and fine chips entering the bearings are the leading cause, according to spindle repairers.
- Unbalanced tooling. Imbalance at high speed overloads the bearings.
- Crashes. Even a light collision can dent bearing races.
- Lubrication. Too little or the wrong lubricant shortens bearing life.
- Preload and overload. Wrong preload or heavy cuts speed up fatigue.
| Signal | What it shows | Where it comes from |
|---|---|---|
| Vibration at bearing frequencies | Early race, ball or cage damage | Accelerometer on the spindle housing |
| Idle spindle temperature | Friction rising in the bearings | Built-in or added temperature sensor |
| Spindle load at a reference speed | Extra drag or imbalance | CNC drive data |
| Drawbar clamping force | Weak tool clamping | Periodic force gauge check |
| Run-out and surface finish | Loss of accuracy | Test cut or in-process gauging |
A new spindle can take this long to arrive. Repair or reconditioning usually takes under two weeks.
Sealing matters as much as monitoring. One remanufacturing case raised spindle life from weeks to 18 months by improving seals. Our specialists can review your worst spindles.
Automatic Tool Changer and Magazine
Tool changers fail often and give clear warning in their own timing.
Because the machine controls every tool change, each one is a free health test. No extra sensor is needed.
Trending change time per machine is one of the quickest wins. We set it up in every rollout.
Ball Screws and Linear Guides
Axis wear shows up as lost accuracy first and breakdown later.
- How they wear. Contamination in the nut and breakdown of the lubricant film cause wear and loss of preload, according to ball screw makers.
- Backlash grows. Lost preload means the axis no longer reverses cleanly.
- Servo works harder. Drive load and following error rise on the affected axis.
- Parts drift. Round features go out of round; positions shift after reversals.
A quick circular test that measures how accurately two axes move together. It reveals backlash, servo mismatch and geometry errors, and is covered by ISO 230-4.
A ballbar test every few months, plus servo load trends in between, gives a clear picture of axis health without stopping production for long.
Ask our team how ballbar results and drive data are combined.
Which Signals to Use for CNC Predictive Maintenance
Start with what the control already knows, then add sensors only where needed.
Drive current or torque for each axis and the spindle, read every cycle.
Alarm history, tool-change time, cycle time and feed overrides.
Cuts or minutes per tool against its limit.
An accelerometer for bearing defect frequencies.
Spindle, ball screw supports and coolant.
Geometry and accuracy checks on a schedule.
Vibration analysis looks for bearing defect frequencies and for statistics such as kurtosis and crest factor, which research shows rise as a spindle degrades.
Using one reference routine at a fixed speed makes readings comparable week to week. Our engineers help define it.
Tool Wear, Tool Life and Cycle Time
Machine health and tool life are linked: a healthy spindle cuts cleanly and tools last longer.
- Worn tools load the spindle. Rising spindle load on the same cut is a simple wear signal.
- Fixed counts waste tools. Changing by count alone replaces good tools and misses bad ones.
- Broken tools cause crashes. Detecting a break within one cycle protects the spindle and fixture.
- Cycle time follows. Stable tools and axes let programs run at full feed rates.
Monitoring load per tool and per operation turns tool changes from a schedule into a decision. See it in a session.
Getting Data Out of the Machine
Most modern controls can share health data over standard interfaces.
| Interface | What it is | Typical data |
|---|---|---|
| FANUC FOCAS | Library for reading FANUC controls over Ethernet | Axis and spindle data, servo data, tool life, alarms |
| OPC UA and umati | Open standard with a machine tool companion specification | Machine state, program, alarms, key values |
| MTConnect | Open read-only standard for shop floor equipment | Status, loads, feeds, speeds, alarms |
| Added sensors | Vibration and temperature through an edge device | High-frequency vibration, temperatures |
Mixed fleets are normal. A plant may have three control brands and machines from four decades. An edge device per machine or cell brings them to one format.
We can check which of your controls already expose the data needed in a working session.
From Warning to Planned Repair
A warning only has value if it leads to a repair at a convenient time.
A signal moves away from its normal range.
A second signal or test supports the finding.
How long before it affects parts or stops the machine.
Order the part; book the technician.
Do the work in a planned window.
Check that signals are back to normal.
Illustrative. The value of the warning is mostly lead time.
False alarms matter too. McKinsey has warned that a 10% false-positive rate wiped out the savings in one program, so alerts need a second confirming signal.
Discuss how alerts are confirmed before they reach your planners with our advisors.
Preventive Schedules Versus Predictive Maintenance
Preventive maintenance stays. Predictive maintenance tells you where it is not enough and where it is too much.
- Same intervals for every machine
- Healthy parts replaced early
- Failures between services missed
- Spindles replaced after they fail
- Tools changed by count
- Quality drift found at inspection
- Attention goes to machines that need it
- Parts replaced when condition says so
- Weeks of warning before failure
- Spindle swaps planned
- Tools changed by measured wear
- Accuracy loss seen in machine signals
Published studies put typical predictive maintenance gains at 30–50% less downtime (McKinsey) and 5–10% lower maintenance cost (Deloitte). These are cross-industry figures, not promises.
Your own baseline is the only fair test. We measure it first in every pilot.
CNC Predictive Maintenance Checklist
A quick readiness check for a machining area.
Most shops have the data and lack the trending. A machine review shows what you can read today.
How iFactory Delivers CNC Predictive Maintenance
iFactory reads health signals from every CNC, learns each machine’s normal pattern and warns when a subsystem starts to change.
Loads, alarms and timings from FANUC, Siemens and other controls.
Vibration, temperature and load trends.
Servo load, following error and ballbar history.
Load per tool and operation; break detection.
Two signals before a warning is raised.
Work orders with lead time for parts.
It runs on an on-premise iFactory server next to your machines. Share data from three machines and we will build their health view in a trial.
See What Your CNC Data Already Says
Share control data from a few machines. We trend spindle load, servo load, alarms and tool-change time and show which machine needs attention first.
Bearing defect energy has doubled in three weeks and idle spindle temperature is up 4 °C. Drawbar force is normal. The pattern points to front bearing wear.
A Spindle Swap Planned Three Weeks Ahead
This is how a maintenance lead might use the warning.
iFactory ships as a pre-configured NVIDIA AI server, racked and ready with the machine tool health models loaded. Rack it, plug in power and Ethernet, and the AI is live. Scope covers data connections across press, body, paint, assembly and machining areas, PLC/SCADA, MES, CMMS and ERP integration, cabling and network setup, team training and 24×7 remote monitoring.
Server installed, PLC, MES and CMMS links live, history loaded.
Models tuned on your own lines, then piloted in one area with your team reviewing every output.
Rollout to the agreed lines, team training done, 24×7 remote monitoring in place.
Software, server and integration come as one package. For pricing, contact our sales team.
Frequently Asked Questions
Using data from the machine, such as spindle load, vibration, servo load and alarm history, to detect wear early and plan repairs before a failure stops production.
One five-year field study found hydraulics, tool magazines, electrical systems, clamping accessories, guards and spindles were the leading sources, in that order. Results vary by machine type.
By trending vibration at bearing frequencies, idle temperature and spindle load at a fixed reference speed, plus periodic drawbar force checks.
Not to start. Spindle load, servo load, alarms and tool-change time come from the control. Vibration sensors are usually added on critical spindles.
Reconditioning usually takes under two weeks, while a new spindle can take as long as 24 weeks, according to American Machinist.
A first group of machines is typically monitored within 6–12 weeks. Plan it with our specialists.
Know About the Next Failure Weeks Ahead
iFactory trends spindle, tool changer and axis health on every CNC, confirms each warning and gives your team time to plan the repair.
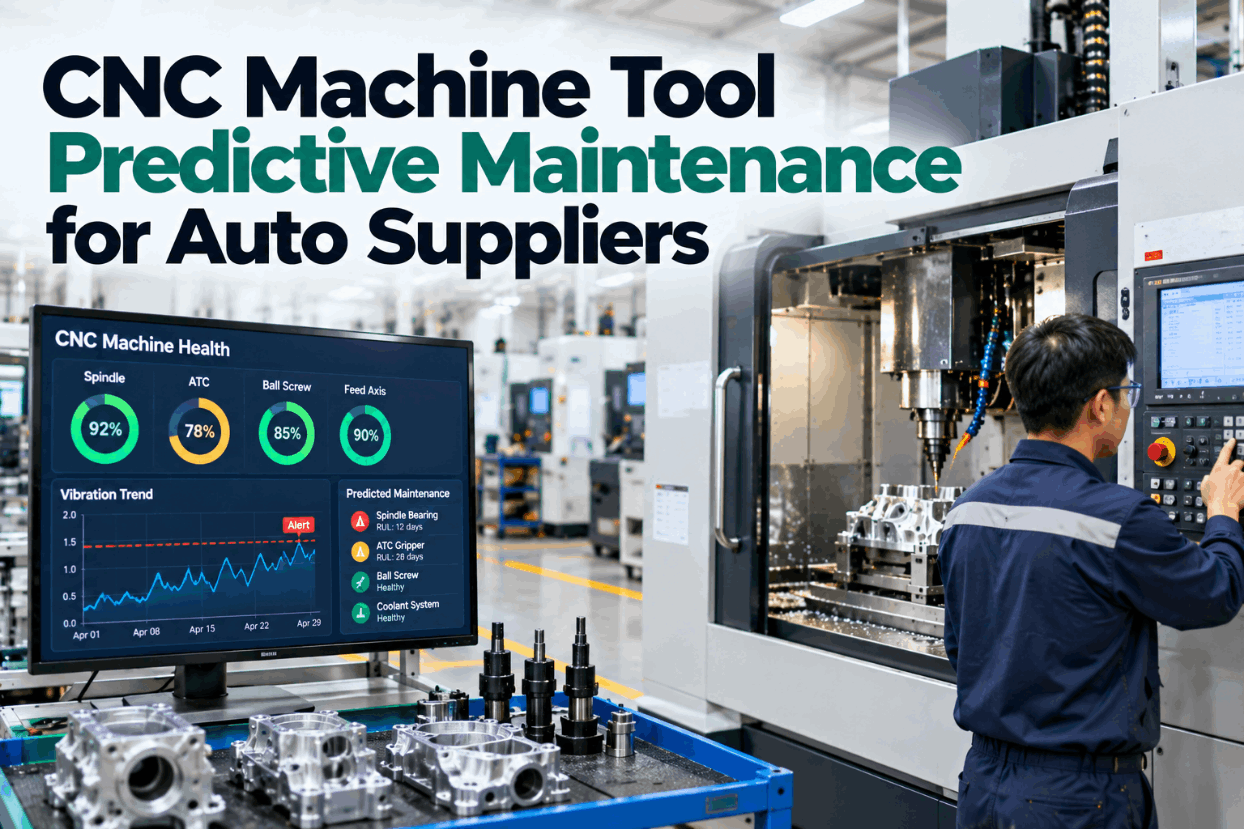
Illustrative. One score per subsystem shows where the next stop is most likely to come from.