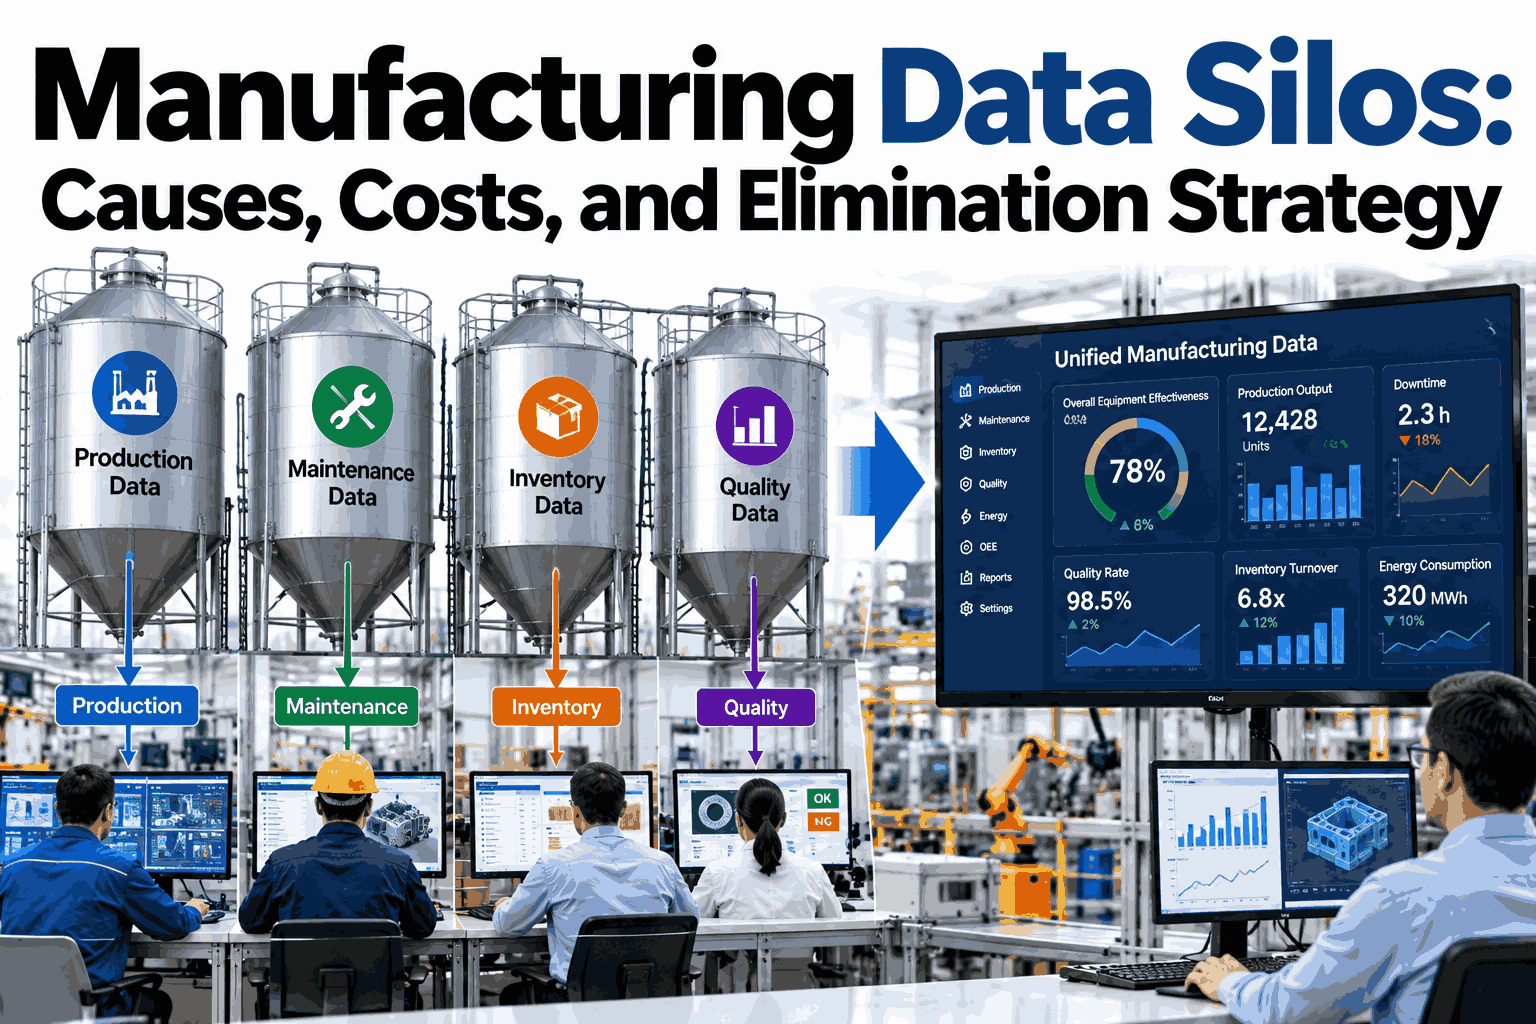
Ask three people on one shop floor why a line ran slow last night and you will often get three different answers. Maintenance has the downtime log, quality has the defect sheet, and planning has the schedule, each in its own system. Nobody can see the whole story, so problems are argued over instead of fixed. This guide explains why silos form, what they cost, and how to remove them, starting with a connected data walkthrough.
Manufacturing Data Silos: Causes, Costs and How to Eliminate Them
Bring machine, quality, maintenance and planning data into one view, so every team works from the same facts.
Six systems, six owners, no shared view.
Why Silos Form on the Shop Floor
Almost never by design. They grow one purchase at a time.
Systems bought for one job
Each tool solves a local problem and speaks only its own language.
Mixed machine ages
New and old equipment use different protocols, so data stays trapped in the controller.
Team ownership
Each department guards its own data and defines its own terms.
Spreadsheets as glue
Manual exports fill the gaps, and go stale the moment they are saved.
If a simple question such as "which product causes the most downtime?" needs three exports and a meeting, you have silos.
What Silos Really Cost
The invoice shows a fraction. The rest sits below the surface.
Easy to see
- Duplicate software licences
- Hours spent building reports
- Rework from wrong data entry
Hidden below the line
- Slow root cause hunts
- Repeat breakdowns nobody links
- Planning built on old numbers
- Decisions based on opinion, not data
- Audit preparation done by hand
Where the Silos Usually Hide
Each system holds one piece of the answer.
Find Where Your Data Is Stuck
Bring a list of your systems. We map them with you and show which cross-team questions a connected view could answer first.
An Elimination Strategy in Four Steps
Climb one step at a time. Do not rebuild everything.
Map
List every system, owner and data type.
Connect
Read data from machines and systems without changing them.
Align
Agree on shared names, units and definitions.
Act
Use the joined data for alerts, analysis and decisions.
Start with a single painful question, such as repeat downtime. Prove value there before widening.
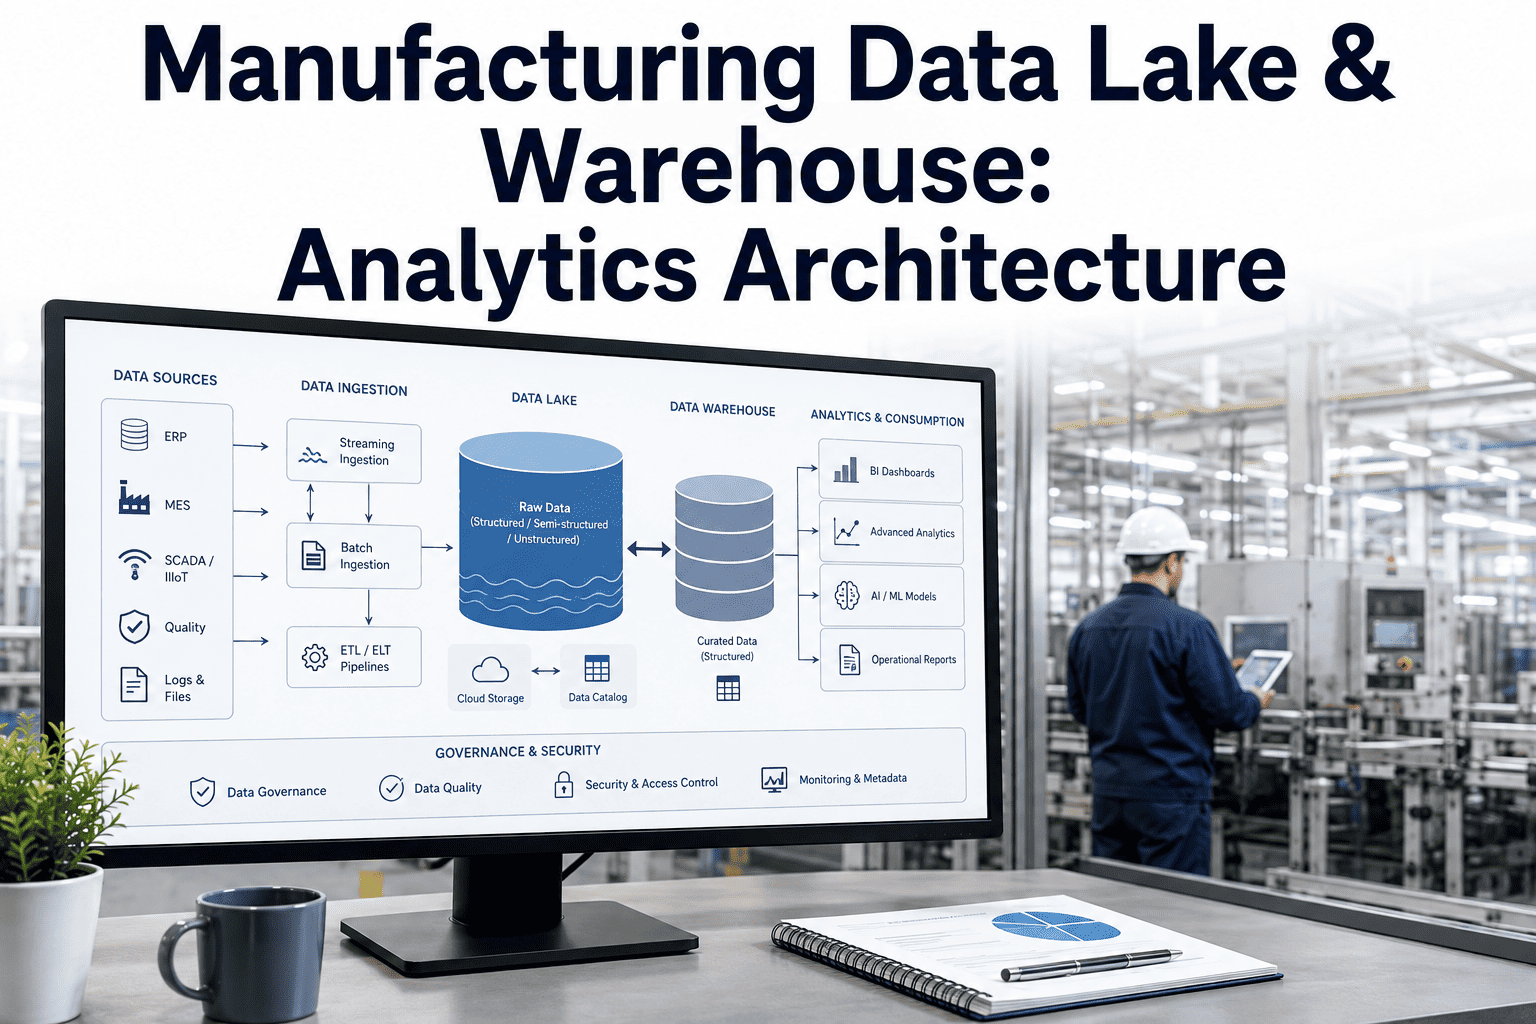
How Connected Data Flows
Many sources in, one layer in the middle, useful answers out.
Sources
PLCs and sensorsMES and ERPCMMS and QMSUnified layer
Clean and alignLink by asset and batchStore historyOutcomes
Root cause answersEarly warningsShared dashboardsStart with read-only connections. Your control systems stay untouched until your team decides otherwise.
Signs the Silos Are Breaking Down
Track these four measures.
Example figures only. Results depend on how fragmented your data is today.
How iFactory AI Connects the Plant
Delivered ready, live in 6 to 12 weeks.
Install and link
Server installed. PLCs, SCADA and plant systems connected.
Align and test
Data cleaned, definitions agreed, first use case piloted.
Go live
Teams trained and remote monitoring begins.
The server sits inside your network. To scope your systems, contact our integration team.
Frequently Asked Questions
What is a data silo in manufacturing?
It is data held in one system or team that others cannot easily reach. A downtime log in a CMMS that quality cannot see is one example. The result is that each team sees only part of any problem.
Do we need to replace our existing systems?
No. Most plants keep their MES, ERP and CMMS and add a layer that reads from them. This avoids a costly rip-and-replace. Our team can review what you have.
How long does it take to connect our data?
A first useful use case is often live within weeks, not years. Full coverage takes longer and depends on the age of your equipment. Starting with one question keeps the first phase short and clear.
Is it safe to connect production systems?
Yes, when connections are read-only and run inside your own network. Your control systems keep running as before. Security and access rules are agreed with your IT team before anything goes live.
How do we prove the value?
Pick one measurable question, such as time to find a root cause, and compare before and after. A demo session shows how we set this baseline.
Give Every Team the Same Facts
In thirty minutes we review your systems, your biggest data gaps and the first question worth answering. You keep the notes either way.