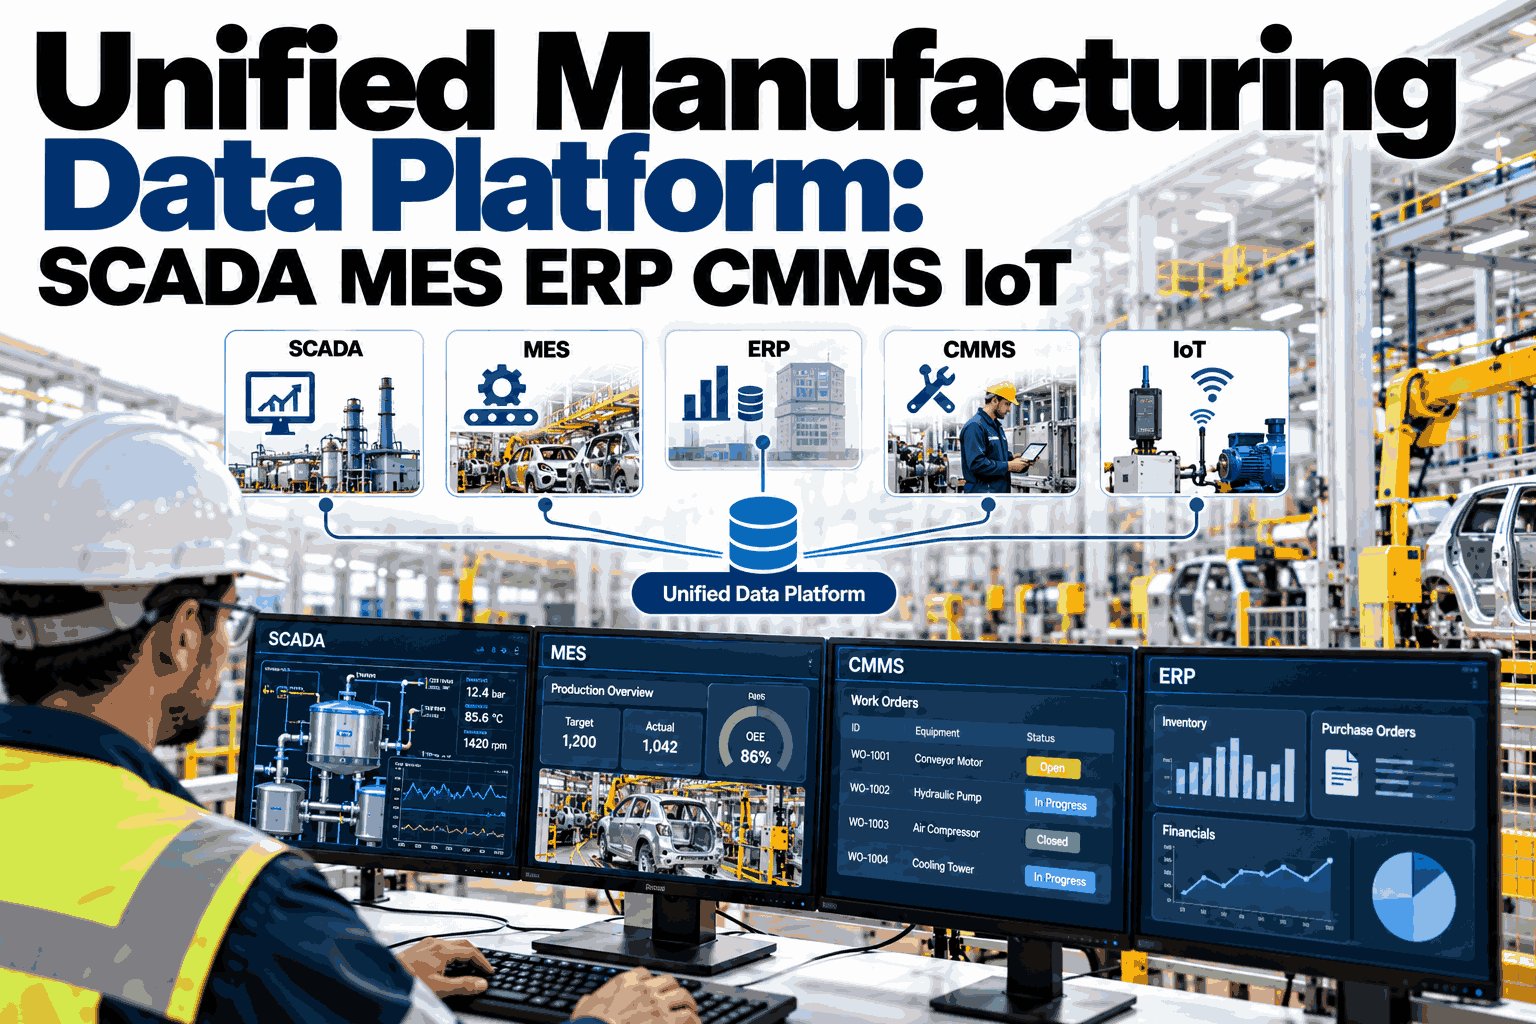
Unified Manufacturing Data Platform: SCADA MES ERP CMMS IoT

By James Smith on October 12, 2026

unified-manufacturing-data-platform-scada-mes-erp-cmms-iot

A bearing starts running hot on a Tuesday night. SCADA logs the temperature rise, the CMMS has no idea, the MES keeps scheduling the line at full rate, and the ERP only learns about it when a delivery slips on Friday. Every system did its own job correctly, yet the plant still lost the shift, because none of them could see what the others knew. That gap between systems is where most avoidable downtime, rework and late orders actually live. This article explains how a unified manufacturing data platform closes it, and if you want to see it mapped to your own stack, you can review your plant data architecture with our team.

Industrial data integration

Unified Manufacturing Data Platform: Connecting SCADA, MES, ERP, CMMS and IoT

How one connected data layer turns five separate systems into a single, trusted view of production, maintenance and cost.

Decisions: dashboards, alerts, AI insights
Unified data platform: one model, one timeline
SCADA | MES | ERP | CMMS | IoT sensors
The problem

Why Plant Data Stays Trapped in Silos

Each system was bought to solve one problem at a different time, by a different team, with its own tags, IDs and time stamps.

5+
systems holding parts of the same story
3
different names for the same machine
24h
typical delay before a report is trusted

These figures are typical patterns seen in mixed-vendor plants, not a survey result. The point is that people end up stitching data together by hand.

The five sources

What Each System Knows and What It Cannot See

Every source is accurate in its own lane. The platform adds the missing context between lanes.

SCADA
Knows: live process values and alarms.
Blind to: orders, work history, cost.
MES
Knows: what is running, batch and yield.
Blind to: asset health and spare parts.
ERP
Knows: orders, materials and finance.
Blind to: what the line did this hour.
CMMS
Knows: work orders and repair history.
Blind to: live condition of the machine.
IoT sensors
Knows: vibration, heat, energy, flow.
Blind to: what the reading means for output.
How it connects

One Hub, Five Streams, a Single Asset Model

Instead of building point-to-point links between every pair of systems, each source connects once to the hub and shares a common asset model.

Unified platform
SCADA
MES
ERP
CMMS
IoT

Five connections replace what would otherwise be ten separate integrations, and adding a sixth system means one new connection, not five.

Inside the platform

Four Layers That Turn Raw Signals Into Decisions

A good platform is built in layers, so each one can improve without breaking the others.

Layer 1
Connect
Read data from PLCs, historians, databases and sensors without changing control logic.
Layer 2
Contextualize
Map every tag to an asset, line, product and order using one naming model.
Layer 3
Analyze
Run rules and AI models on clean, time-aligned data across all five sources.
Layer 4
Act
Raise alerts, create work orders and update schedules back in the source systems.
See it with your own systems

Map Your Plant Data Sources in One Session

Tell us which SCADA, MES, ERP and CMMS you run, and we will show how they would connect into one view.

Same event, two outcomes

The Overheating Bearing: Before and After Unification

Here is the opening story replayed, so you can see where the minutes and the money change.

Siloed plant
Tue 22:10, SCADA logs rising heat
Tue 23:30, operator notices alarm
Wed 07:00, work order raised by hand
Thu 02:15, bearing fails, line stops
Fri, ERP shows delivery slip
Unified plant
Tue 22:10, heat trend flagged
Tue 22:12, work order auto created
Tue 22:15, spare checked in stock
Wed 06:00, repair in planned window
Order date protected, no slip

The timings are illustrative, but the pattern is real: the sooner context reaches the right person, the smaller the loss.

Where are you now

Data Maturity Staircase: Find Your Step

Most plants sit between steps two and three. Knowing your step makes the next move clear.

1Isolated systems and manual spreadsheets
2Some point-to-point links between two systems
3Central historian with limited context
4Unified platform with a shared asset model
5Closed loop with automated actions
What you can do with it

Use Cases That Only Work With Connected Data

Use caseSources combinedResult
Predictive maintenanceIoT, SCADA, CMMSRepairs planned before failure
True OEE by orderMES, SCADA, ERPLosses tied to product and customer
Energy per unitIoT, MES, ERPCost per batch, not per month
Spare parts planningCMMS, ERP, IoTRight parts in stock, less capital tied up
Traceability and auditMES, SCADA, ERPFull batch history in minutes

Each row needs at least two systems talking, which is exactly what a unified layer provides. You can ask our team which use case fits your plant first.

Avoid these

Four Integration Mistakes That Slow Projects Down

Boiling the ocean
Connecting every tag first. Start with one line and one problem.
No naming standard
Without one asset model, data joins fail quietly.
Ignoring OT security
Read-only access and network zones should be agreed on day one.
Dashboards without action
Insight that never reaches a work order changes nothing.
Frequently asked questions

What Plant Teams Ask About Unified Data

Do we need to replace our existing SCADA, MES or ERP?
No. A unified platform sits alongside your current systems and reads from them, so your investments stay in place. The goal is connection, not replacement. See how it fits your current stack on a short call.
Is it safe to connect production systems to a data platform?
Yes, when access is read-only, segmented and agreed with your OT and IT teams in advance. Control logic is not changed. Ask support about security approaches used in industrial plants.
How long before we see useful results?
A focused first use case on one line often shows value within weeks, since the data already exists and only needs connecting. Scope matters more than size. Plan a realistic first phase with our specialists.
Can it work with older machines and mixed vendors?
Usually yes. Older equipment can be read through gateways or add-on sensors, and mixed protocols are normalized into one model. Check support for your equipment before planning.
Who owns the data model once it is built?
Your plant does. The asset model and mappings should be documented and reusable so teams can extend them without starting over. Discuss data ownership and governance with our team.
Stop stitching data by hand

See Your SCADA, MES, ERP, CMMS and IoT Data in One Place

Book a session with iFactory AI to walk through your systems and see how a unified data platform can cut downtime and speed up decisions.

Share This Story, Choose Your Platform!