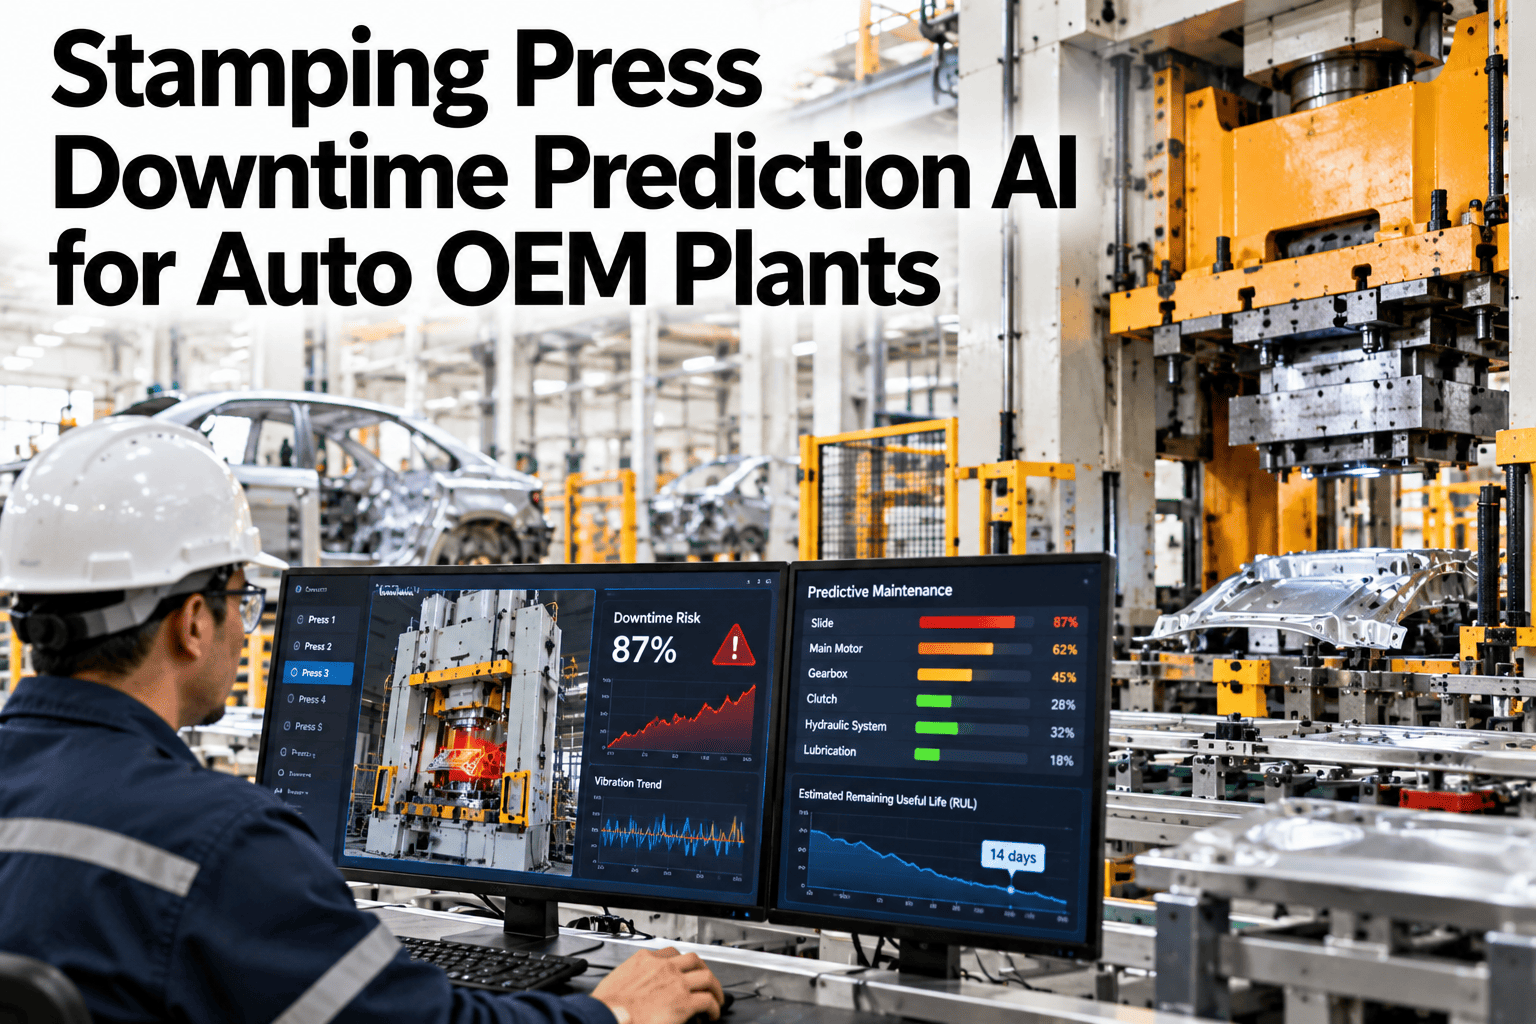
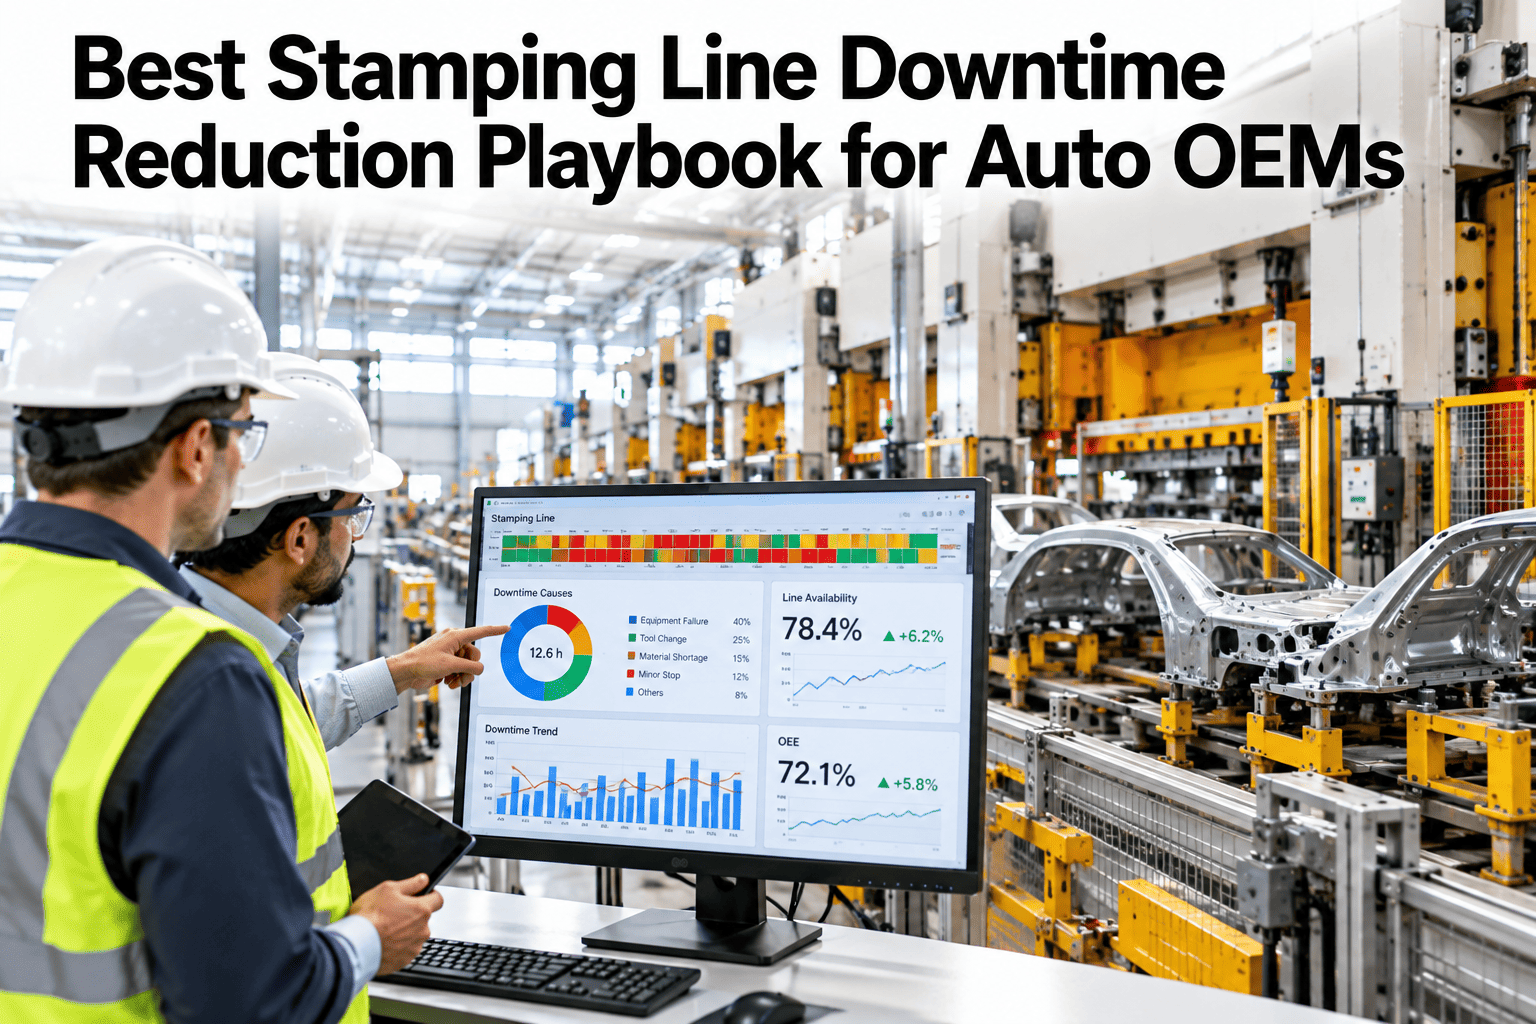
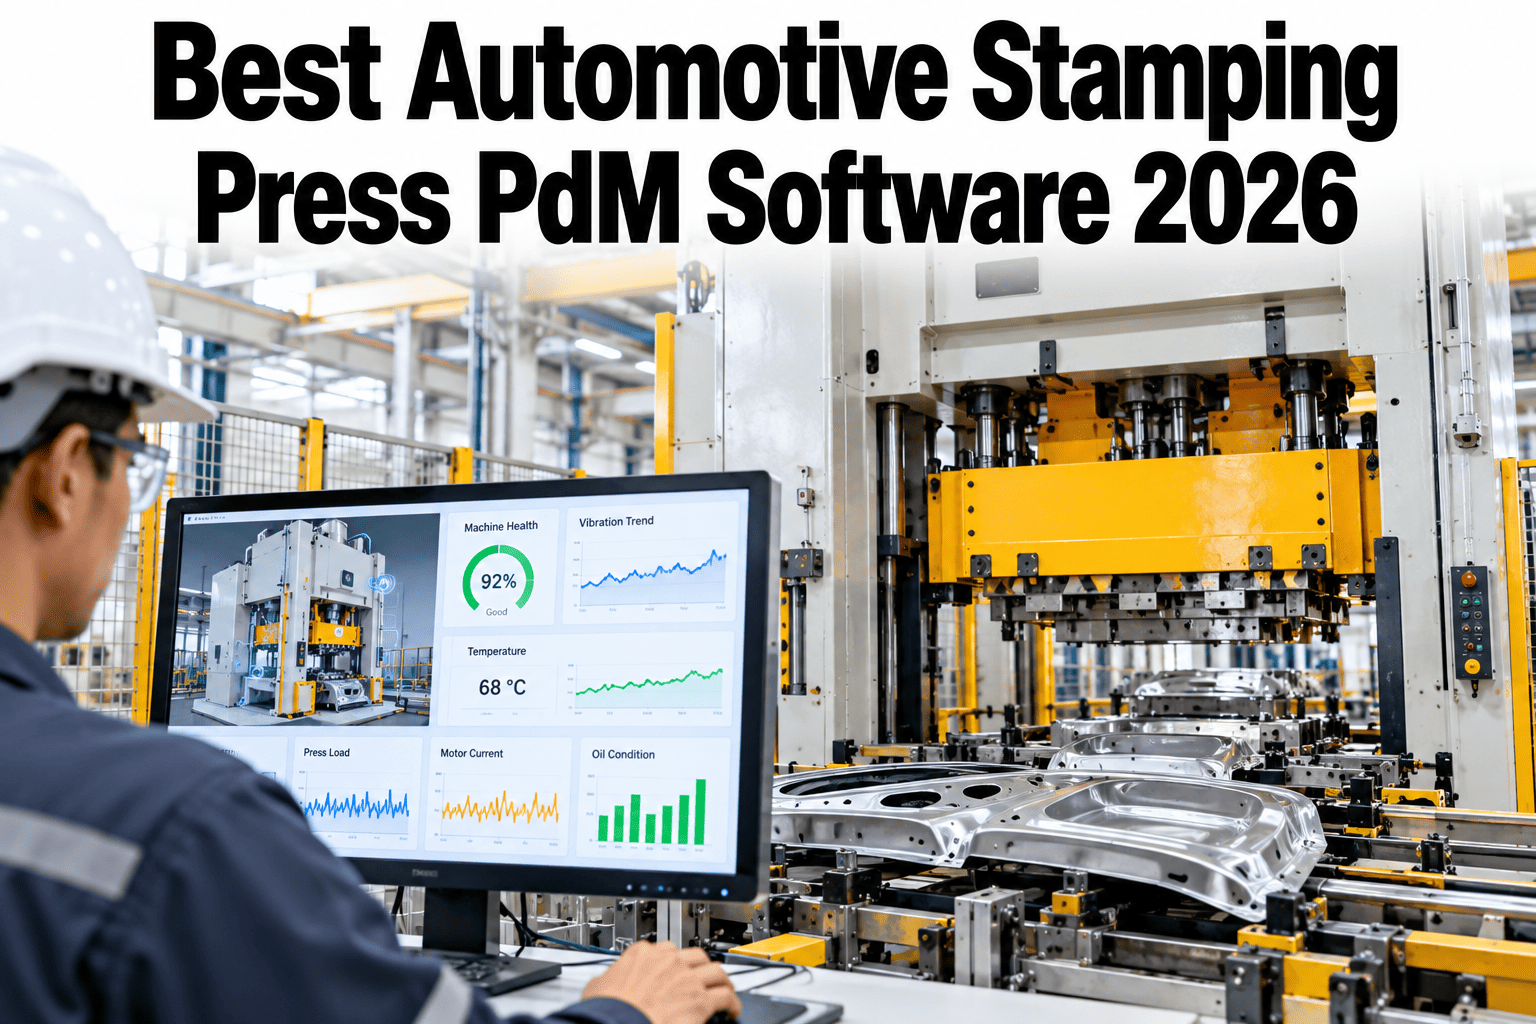
Roughly 40 percent of downtime events in a typical automotive stamping plant last under three minutes, and most MES systems never log them individually (automotive stamping downtime research, 2026). iFactory, an on-premise AI platform with production monitoring and OEE analytics built in, clusters these sub-minute events by station and shift to find the hot spot hiding inside hundreds of tiny stops. Press-shop operations teams who want this on their own lines can request a demo with our team.
Stamping Micro-Stop Analytics · OEM Press Shop, 2026
A Thousand Tiny Stops, One Repeating Pattern — If Something Is Clustering Them
iFactory AI clusters sub-minute stamping stops by station, shift, and time of day, turning scattered seconds of lost time into one actionable hot spot.
Shift 1Shift 2Shift 3Weekend
Why these stops hide
The MES Sees a Stroke Count, Not a Pattern
A stamping press that pauses for eight seconds on a missed feed and resumes rarely generates a logged downtime event — it just shows up as a slightly lower hourly stroke count, indistinguishable from normal cycle-time variation. Multiply that by dozens of stations across a shift, and a real, addressable pattern disappears into statistical noise.
What clustering reveals
Three Patterns That Only Show Up Once Events Are Clustered
Station hot spots
One station on the line accounts for a disproportionate share of all micro-stops, pointing to a specific feed, die, or sensor issue.
Time-of-shift patterns
Stops clustering in the final hour of a shift often point to coil changes, fatigue-driven adjustments, or material running low.
Material-linked spikes
A coil or batch change that correlates with a spike in feed faults flags a material quality issue rather than a machine fault.
What a clustered event record contains
The Data Behind Each Micro-Stop
| Field | Why it's captured |
|---|
| Station and press ID | Pinpoints exactly where the stop occurred on the line |
| Duration | Separates a true micro-stop from a longer, separately-tracked breakdown |
| Shift and time of day | Surfaces time-based patterns tied to shift handover or fatigue |
| Coil or die ID | Links a stop to the specific material batch or tooling in use |
See What's Hiding in Your Press Line's Stroke-Count Data
Share your current press sensor and PLC data, and iFactory AI will show what micro-stop clustering reveals on your specific stations.
From pattern to fix
Four Steps From a Clustered Pattern to a Closed Loss
1
Cluster the events
Sub-minute stops are grouped by station, shift, and material to surface a pattern instead of noise.
2
Rank the hot spots
Stations are ranked by total lost time contributed, not just event count.
3
Investigate the top pattern
Engineering focuses on the station and condition driving the largest share of lost time.
4
Confirm the fix in the data
The same clustering view shows whether the fix actually reduced that station's event rate.
Aggregate OEE vs clustered view
Why a Single OEE Number Hides This Entirely
Shift-level OEE report
One Performance percentage for the whole line
No visibility into which station drives the loss
Looks stable shift to shift, hiding a real pattern underneath
Clustered micro-stop view
Loss broken down by station, shift, and material
A single hot-spot station is immediately visible
Engineering effort goes to the station actually costing the most
Expert review
What a Press-Shop Operations Manager Checks First
Micro-stop analytics earns its place when the clustering actually points engineering to one station, not a vague plant-wide trend nobody can act on.
Verdict
Strong when ranked by total lost time, not event count — a station with fewer, longer micro-stops can cost more than one with many brief ones.
Watch for
Treating a time-of-shift pattern as purely a people issue when it's often a material or changeover timing issue underneath.
Do next
Pull your last month of stroke-count data and check which station shows the widest swing in average rate, shift to shift.
Frequently asked questions
What Press-Shop Teams Ask About Micro-Stop Analytics
How much downtime is actually hiding in sub-minute stops?
Roughly 40 percent of downtime events in a typical automotive stamping plant last under three minutes, and most of these go unlogged individually by standard MES systems (automotive stamping downtime research, 2026).
See what this means for your line.
Does this require new sensors on every press station?
Can this distinguish a feed fault from a die issue?
Clustered events carry fault-code and duration context that generally separates a feed-related stop from a die or tooling-related one, though the specific fault taxonomy depends on what your press controllers report.
Discuss fault classification for your presses.
How often should we review the clustered hot-spot report?
Does this connect to our coil and die tracking systems?
Find the pattern hiding in the seconds
Cluster Your Press Line's Micro-Stops Into an Actionable Hot Spot
Book a demo to see how iFactory AI turns sub-minute stops into a clear station-level priority for your press shop.
{"@context":"https://schema.org","@type":"FAQPage","mainEntity":[
{"@type":"Question","name":"How much downtime is actually hiding in sub-minute stops?","acceptedAnswer":{"@type":"Answer","text":"Roughly 40 percent of downtime events in a typical automotive stamping plant last under three minutes, and most go unlogged individually."}},
{"@type":"Question","name":"Does this require new sensors on every press station?","acceptedAnswer":{"@type":"Answer","text":"Most stamping lines already generate stroke-count and fault data at the press controller level, so connecting existing data is usually the first step."}},
{"@type":"Question","name":"Can this distinguish a feed fault from a die issue?","acceptedAnswer":{"@type":"Answer","text":"Clustered events carry fault-code and duration context that generally separates feed-related stops from die or tooling-related ones."}},
{"@type":"Question","name":"How often should we review the clustered hot-spot report?","acceptedAnswer":{"@type":"Answer","text":"Most press shops review it weekly for operational decisions and monthly for engineering investment decisions."}},
{"@type":"Question","name":"Does this connect to our coil and die tracking systems?","acceptedAnswer":{"@type":"Answer","text":"Yes, linking a micro-stop cluster to the specific coil or die in use separates a material-driven pattern from a machine-driven one."}}
]}