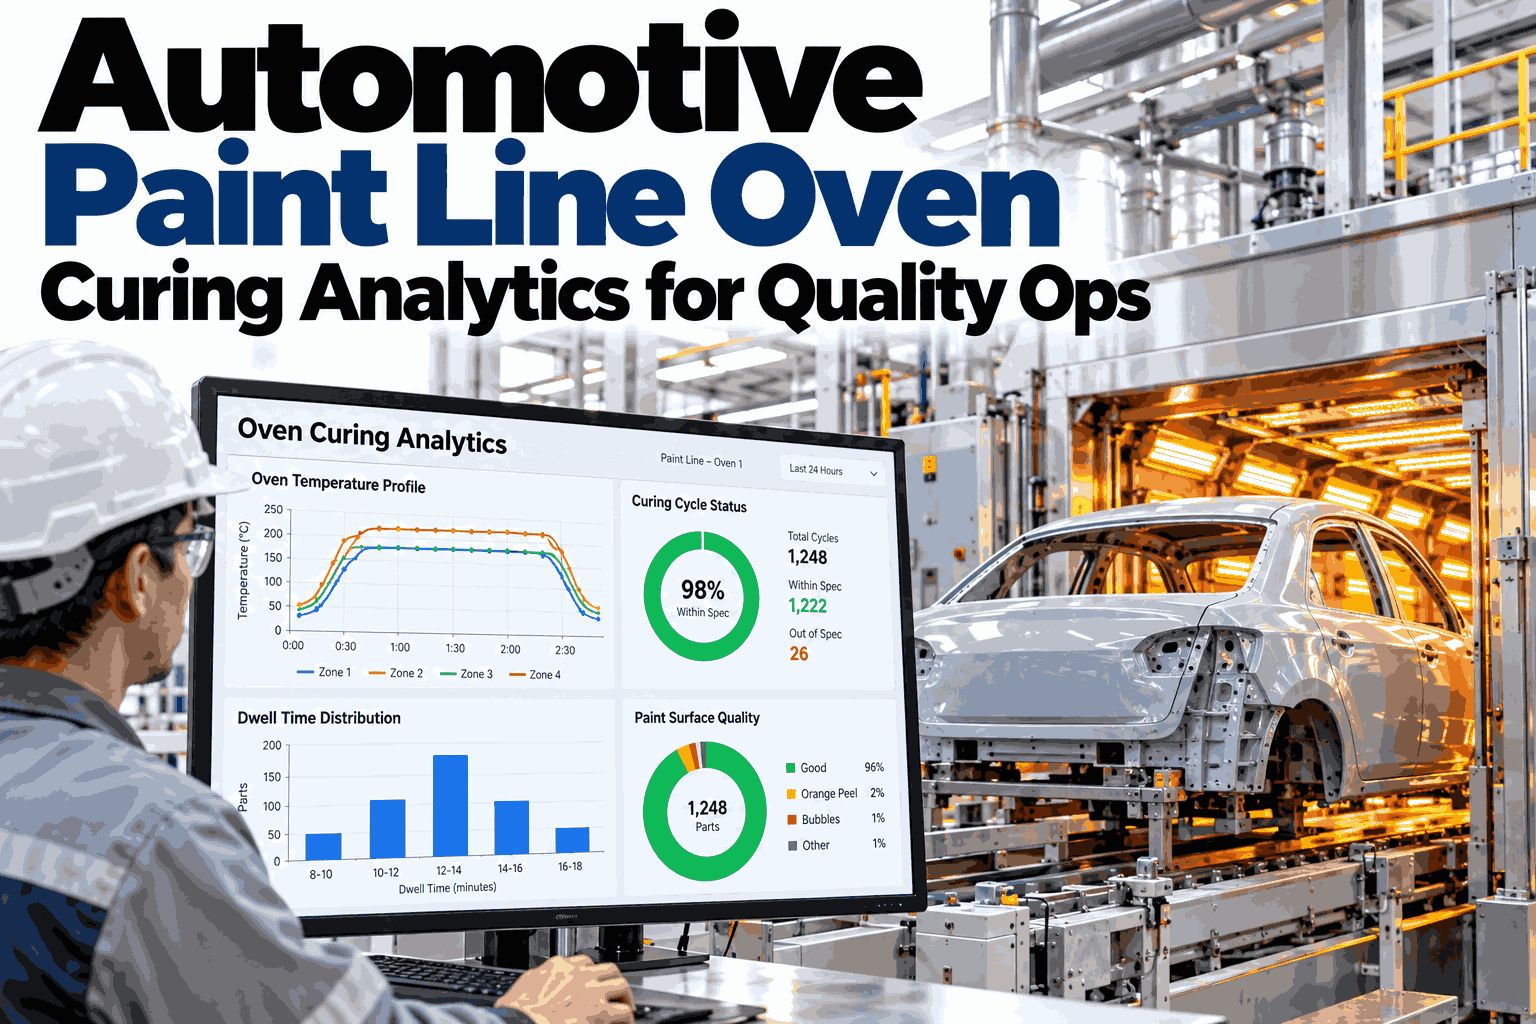
A car body can leave the paint shop looking flawless and still carry a weak finish, because curing happens inside the oven where nobody can see it and the defects it causes often appear weeks later as soft clearcoat, gloss loss or peeling. Quality teams usually rely on a few spot checks and the oven setpoints, which describe what the oven was told to do rather than what each body actually experienced. Curing analytics closes that gap by tracking the real temperature history, time at temperature and air moisture conditions for every body that passes through. To see how this works on a live paint line, review an oven curing walkthrough built around your own process.
Know Exactly How Every Body Cured Before It Leaves the Oven
iFactory AI links oven temperature profiles, time at temperature and dew point conditions to each vehicle body, so quality operations can stabilise paint properties instead of discovering problems downstream.
Curing Is the Quiet Step That Decides How Long the Finish Lasts
Paint becomes a durable film only when its chemistry completes inside the oven. If the coating receives too little heat or too little time, cross-linking stays incomplete and the film remains softer, less chemical resistant and more prone to marring. If it receives too much, the film can yellow, lose gloss or turn brittle, and the colour can drift away from the approved standard.
The difficulty is that both extremes can look acceptable at the end of the line. The body passes visual inspection, the paint thickness is correct and the shipment leaves on schedule, while the real problem waits in the film. This delayed visibility is exactly why quality operations teams need evidence from inside the oven.
Warranty claims tied to paint are expensive, public and slow to trace. When a claim arrives, the plant needs to answer a simple question, which is how that specific body was cured on that specific day, and most plants cannot answer it from memory or paper.
Metal Temperature and Time Above Threshold Define the Real Cure
Air temperature in the oven is not the temperature of the coating. Heavy sections of a body warm more slowly than thin panels, so the same oven air can leave one area fully cured and another barely at threshold. What matters is the temperature of the substrate and the minutes spent above the minimum cure temperature required by the paint supplier.
The slowest area sets the real limit. If the pillar joint reaches temperature last, the oven profile must leave enough remaining hold time for that area to complete its cure, even when the roof has been ready for ten minutes. A good analytic view therefore tracks the coldest critical point, not the average.
This also explains why a profile that was perfect in a commissioning trial can drift into trouble later. Body mix changes, new models add heavier sections and seasonal conditions shift the heat load, so the profile needs ongoing measurement rather than a once-a-year check. Continuous tracking also gives maintenance an early warning, because a slow rise in the time needed to reach temperature often points to fan wear, fouled filters or burner decline long before the oven fails an audit.
Scoring One Body Against Its Time-at-Temperature Requirement
Suppose a clearcoat specification requires the substrate to stay above its minimum cure temperature for at least twenty minutes. Probes placed at four critical points on one body produce the results below, with the required time marked on every track.
The roof and door pass comfortably, which is why a surface check on those panels would suggest a healthy cure. The pillar joint and sill fall short, and these are exactly the areas that tend to hide problems. An automatic view flags the body, records the result and lets quality decide whether to hold, test or release.
See Which Bodies on Your Line Are Closest to the Edge
Share your oven profile and body mix, and see how automatic time-at-temperature scoring would highlight weak spots before paint leaves the plant.
Why Dew Point Belongs in the Same Conversation as Oven Temperature
Dew point measures how much moisture the air holds, and it matters because a body that is colder than the dew point of the surrounding air collects condensation. That moisture can become craters, pinholes, water marks or poor adhesion between layers. Tracking the margin between body surface temperature and dew point shows when conditions are quietly turning risky.
The surface temperature barely changed across the three cases, yet the humid evening shows a margin of only two degrees. A plant that watches temperature alone would miss it. Combining the two signals lets the system warn the team before moisture appears on the film, not after defects have been counted.
Dew point also affects flash-off and the way solvents leave the wet film before the oven. Consistent air conditions upstream make the oven profile easier to hold, which is why many quality teams review both zones together. A shared view of booth, flash-off and oven data also ends the familiar argument over whether a defect started in application or in curing, because the timeline shows where conditions first moved outside their normal range.
Five Families of Cure Drift and Where They Start
Cure problems seldom appear as a sudden failure. They creep in as small drifts in heat, airflow, conveyor speed or air conditions, each too small to trigger an alarm. Grouping the causes by family helps the team look in the right place when the analytics shows a trend.
Film build deserves special mention. A thicker coat needs more time to cure all the way through, so a spray booth drift that adds a few microns can quietly push the oven requirement beyond what the profile provides.
| Visible symptom | Likely cure or moisture link | What analytics should show |
|---|---|---|
| Solvent pop or pinholes | Heat ramp too fast or insufficient flash-off | Steep early ramp and short flash-off time on affected bodies |
| Soft or marring film | Under-cure at cold spots | Short time at temperature on sills and pillars |
| Yellowing or colour shift | Over-bake after a stop or hot zone drift | Extended hold time or excess peak temperature |
| Craters or water marks | Condensation on cold bodies | Small margin between surface temperature and dew point |
| Gloss loss | Uneven or excessive heat exposure | Zone deviation and rising peak temperature trend |
| Adhesion problems between layers | Moisture trapped between coats or incomplete cure of the lower layer | Humidity spikes and short cure of the earlier coat |
What Happens to the Bodies Inside the Oven When the Conveyor Stops
A conveyor stop is one of the hardest events for paint quality. Bodies that are in the hold zone keep absorbing heat while the line waits, and bodies in the ramp zone may sit in partial heat. Without a record, the team often guesses which bodies were affected and releases or scraps them on judgement alone.
The value lies in precision. Instead of treating a whole oven load as suspect, the plant identifies the exact bodies at risk, which protects both quality and throughput. The decision limits for each category are set with your paint supplier and quality leadership, not by the software.
From Oven Sensors to a Cure Decision for Every Body
The analytics follows each body from the entry of the oven to the exit and builds a record that quality can read in seconds. The chain below shows how raw sensor signals become a decision, with every step recorded for later review.
Because the record is built automatically, quality engineers spend their time reviewing exceptions instead of collecting data. The same record supports audits, supplier conversations and customer questions with facts rather than recollection. It also builds a library of known good bodies, so when a new model, colour or paint batch is introduced, the team can compare its first runs against proven history instead of starting from guesswork. Over time this library becomes one of the most useful quality assets in the paint shop.
A Control Board That Quality Teams Can Read at a Glance
A good dashboard answers three questions quickly: is the oven within its window now, is it drifting, and which bodies need attention. The board below shows the kind of overview a quality operations lead could check at the start and end of every shift.
Values on the board are examples only. In practice each number links to the bodies behind it, so a quality lead can move from a drop in compliance to the exact shift, zone and carrier in a few clicks.
Every Coat Has Its Own Cure Concern and Its Own Data to Watch
A painted body is a stack of layers, and each layer is cured on its own schedule. Treating all ovens as one problem hides important differences, because a weakness in an early layer can undermine every coat above it. The table below summarises what quality teams usually watch for at each stage.
| Coating layer | Main cure concern | Data worth tracking | Typical consequence of drift |
|---|---|---|---|
| Electrocoat | Full cure on heavy and enclosed sections | Substrate temperature at cavities and joints | Weak corrosion protection that appears late |
| Primer or surfacer | Even cure that supports good adhesion above it | Time at temperature and film build | Intercoat adhesion problems and chip sensitivity |
| Basecoat | Controlled flash-off and moisture release | Humidity, surface temperature and ramp rate | Solvent pop, colour variation and mottling |
| Clearcoat | Complete cross-linking for gloss and durability | Peak temperature, hold time and zone deviation | Soft film, gloss loss and early wear |
| Repair and touch-up | Lower temperature limits for parts already assembled | Local heating records and exposure time | Mismatch in gloss or durability on repaired areas |
This layered view also helps with root cause work. When a clearcoat defect appears, the investigation should look at the basecoat flash-off and the primer cure, because the visible problem often begins one or two layers below the surface.
Where Curing Analytics Returns Value to Quality Operations
The benefit of tracking cure is not limited to fewer visible defects. The same data shortens investigations, supports supplier discussions and reduces the energy spent on unnecessary overbaking. Four areas usually deliver the clearest return, and each can be measured from the first pilot.
Any energy saving must be approached carefully. The first goal is always a complete cure, and a reduction in heat should only follow once the data shows consistent margin across the coldest points of every body type and every season.
Seasonal change is a good example of where this discipline pays off. Winter air brings colder bodies into the shop, and summer brings humidity, so a profile that was ideal in one season can drift in another. Trend views by month let the team adjust early rather than react to a rise in defects.
A Practical Rollout Path and a Readiness Checklist
Most paint shops begin with one oven and one coat, usually the clearcoat, because it shows cure problems most visibly and carries the highest warranty exposure. After the first oven is trusted, the same approach extends to primer, basecoat and other lines.
A short readiness check keeps the first pilot focused. Most items can be completed within a few days, and several only need a single meeting between paint shop, quality and maintenance.
What Quality Teams Ask Before Adding Curing Analytics
See Paint Oven Curing Analytics Working on Your Own Line
Book a session with iFactory AI to review your oven profile, dew point conditions and body tracking, and see how every body can leave the oven with a cure record.