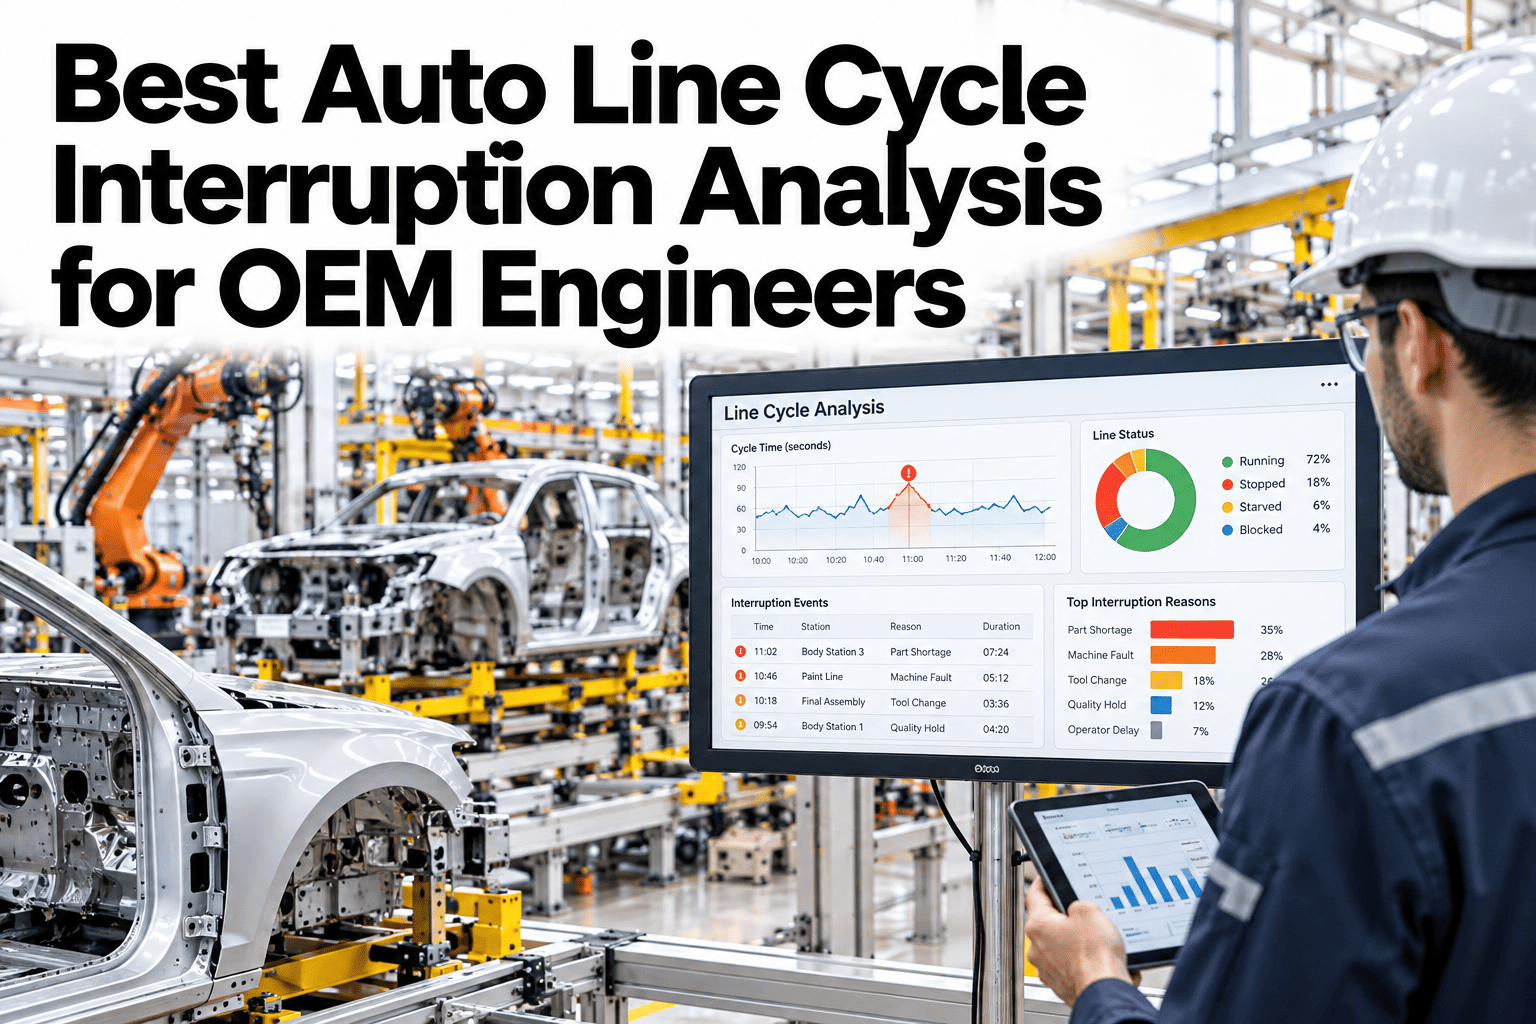
A thirty-second stop on an assembly line rarely gets its own investigation, yet a hundred of them in a shift can cost more than one hour-long breakdown. Most OEM lines track the big stoppages closely and let micro-stops blur into a vague "line efficiency" number nobody can act on. Cycle interruption analysis separates every short stop into a category, locates it as in-station or between-station, and groups the patterns that repeat. Process and reliability engineers can walk a shift's worth of cycle breaks through iFactory AI's categorization to see which pattern is actually costing the most time.
Every Thirty-Second Stop Has a Category. Find It.
iFactory AI tags each cycle interruption as in-station or between-station, then groups the recurring patterns so engineers fix the cause, not the symptom.
Inside the cycle time budget
In the handoff or conveyance gap
Where a Thirty-Second Stop Actually Happens
Not every interruption has the same root. Splitting by location is the first cut that makes a pattern visible.
A fastener misfeed, a torque retry, a sensor recheck inside the station's own cycle.
A component that needs a second attempt to seat or align correctly.
A carrier, skid or AGV that arrives late or stalls in transit.
A starved or blocked buffer upstream or downstream of the station.
A manual station waiting on an operator action outside the standard time.
The same category repeating at the same station, shift after shift.
Categorization in Four Steps
Location, duration and station at the moment it occurs.
Was the delay inside the cycle budget or in the handoff?
Cluster stops that share a station, shift or cause.
Not by count alone, since duration varies by category.
Turn Your Shift Log Into a Ranked Pattern List
Bring a day of cycle data to a 30-minute session and see which station's pattern is costing the most time.
Count vs Total Time Lost
| Station | Stop Count | Avg Duration | Total Time Lost |
|---|---|---|---|
| Station 12, fastening | 140 | 18 sec | Highest when ranked by total |
| Station 7, conveyance | 35 | 90 sec | High despite low count |
| Station 22, part fit | 60 | 25 sec | Moderate |
| Station 4, operator paced | 200 | 8 sec | Lower than count alone suggests |
Illustrative figures. Ranking by count alone would have pointed to the wrong station first in this example.
Pattern-Based vs Event-Based Response
A Composite Scenario: The Station Everyone Thought Was Fine
Picture a line where Station 4 logs the most stop events on the daily report and draws constant attention, while Station 7 sits quietly further down the count list.
Ranked by total time lost instead of count, Station 7's longer, less frequent conveyance stalls turn out to cost more shift time than Station 4's short, frequent operator-paced pauses. The investigation moves to where the time is actually going.
Where iFactory AI Fits
Tags automatically
Captures location, duration and station for every cycle interruption without manual logging.
Splits in vs between
Separates station-internal delay from conveyance and buffer delay.
Groups the repeats
Surfaces recurring patterns across shifts instead of isolated events.
Ranks by real impact
Orders patterns by total time lost, not raw stop count.
Expert Review
A manufacturing process engineer's perspective, reviewed for accuracy before publication: micro-stop analysis fails most often not from lack of data but from treating every stop as a one-off event. The moment a team starts asking "has this exact pattern happened before, at this station, on this shift," the investigation gets dramatically shorter. Seeing a week of pattern-grouped data usually changes which station gets attention first.
Frequently Asked Questions
What counts as a cycle interruption versus a normal stop?
A cycle interruption is any delay that pushes a station or segment beyond its standard cycle time, whether that is a few seconds of retry inside a station or a longer gap waiting on conveyance. The threshold and definition can be tuned to your line's own standard times rather than a fixed universal number. See how interruption thresholds would be set for your specific stations in a short session.
Why separate in-station from between-station interruptions?
The two have different owners and different fixes. An in-station delay usually points to tooling, part fit or operator timing at that specific station, while a between-station delay points to conveyance, buffer sizing or line balance. Mixing them into one generic downtime number hides which team should actually investigate. Ask for a breakdown of your own line split this way.
Should we prioritize stations by stop count or total time lost?
Total time lost is usually the more useful ranking, since a station with fewer but longer stops can cost more shift time than one with many brief pauses. Stop count still matters for operator fatigue and process stability, so both are worth tracking, but the investigation priority should follow the time, not just the frequency. Explore a ranked view of your stations by both measures.
How much historical data is needed to see a real pattern?
It depends on how frequently the interruption occurs and how much the process varies by shift or product mix, but a few weeks of data is often enough to separate a genuine recurring pattern from normal day-to-day noise. Comparing across shifts and product changeovers specifically helps confirm whether a pattern is structural or coincidental. Try a pattern check against your own recent production history.
Can this integrate with our existing line PLC and MES data?
In most cases, yes, since cycle timing and station status are typically already available from PLC or MES systems and can be read without major new hardware. The specifics depend on what your current systems expose and how cleanly station boundaries are defined in the data. Join a review of your current PLC and MES data for this fit.
Stop Letting Micro-Stops Hide in an Efficiency Number
iFactory AI categorizes and ranks every cycle interruption so engineers fix the pattern, not the symptom. Book a walkthrough on your own line data.