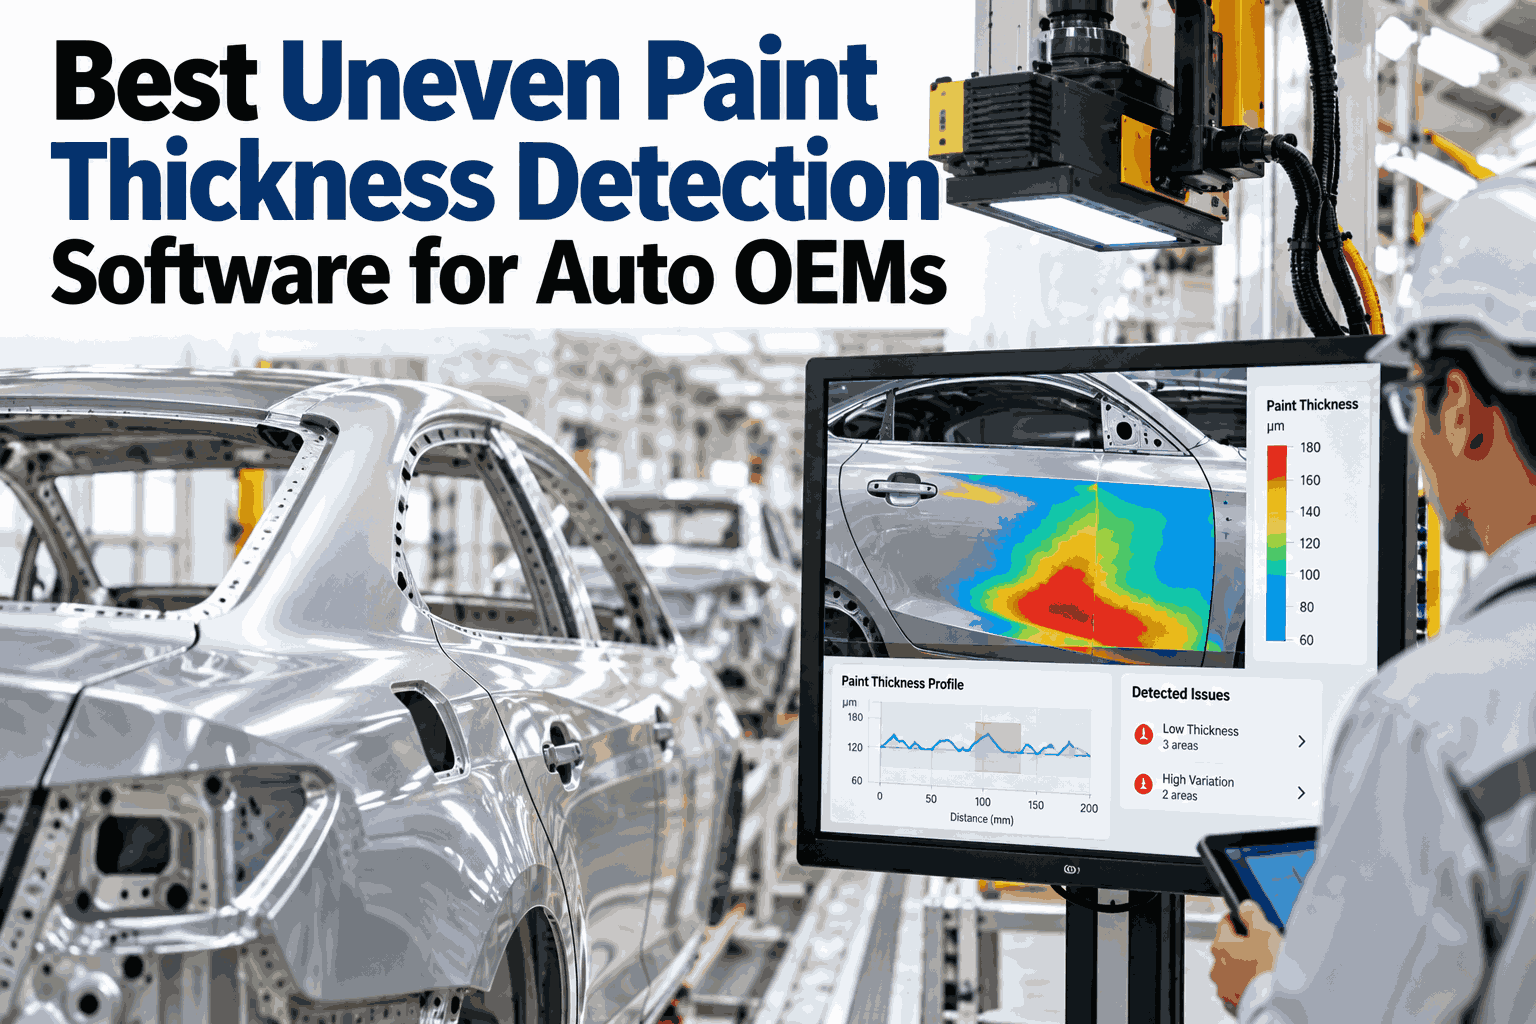
Paint thickness is a quiet specification. Too thin, and a panel loses hiding power, gloss and long-term protection. Too thick, and it invites runs, cracking, extra material cost and longer cure. The trouble is that a body is never uniform: recesses, edges and flat areas all take paint differently, and a handful of gauge readings cannot show the full picture. Software that combines gauge data with spray behavior can show where the film really sits across the panel. Paint shop teams can see how their own gauge readings would look as a full thickness map and where the spread is widest.
Find Uneven Film Build Before It Becomes a Defect or a Cost
iFactory Automotive Paint AI integrates coating gauges, correlates spray patterns and visualizes thickness as heat maps across every body.
The Cost Sits on Both Sides of the Window
Most plants worry about thin film. Thick film is equally expensive, just quieter.
Narrowing the spread lets you aim closer to the target, which is where both quality and material savings come from.
A Cross-Section of Uneven Build
Zoom into a panel edge and the problem is obvious. The same spray pass leaves different film depth depending on geometry.
Why a Few Gauge Readings Are Not Enough
Gauges are accurate where they touch. The challenge is that touched points are a tiny fraction of the surface.
See Your Spread on One Real Panel
Bring a set of gauge readings from a single body. We will show the thickness map and the zones with the widest variation.
How the Software Builds the Map
Gauges give the truth at specific points. Spray data explains the rest. Together they fill in the panel.
Reading the Thickness Heat Map
Darker cells mean heavier film. A good map makes patterns visible at a glance, such as a heavy stripe from one overlapping pass.
Tracking Drift Across Shifts
Average thickness often creeps before anyone sees a defect. A control view shows when the process is moving.
Linking Thickness Back to the Spray
A map only matters if it points to a cause. Each pattern suggests where to look in the application process.
| Map Pattern | Likely Cause | First Check |
|---|---|---|
| Heavy stripes between passes | Overlap too generous | Robot path spacing |
| Thin recessed areas | Poor reach into concave zones | Gun angle and bell positioning |
| Heavy edges | Charge or flow concentrating | Voltage and fluid settings |
| Whole body trending up | Flow or solids shift | Material and flow-rate records |
| One panel type outlier | Program mismatch | That panel's robot program |
A Practical Rollout
Start with the data you already have, then widen coverage where the map shows the biggest gaps.
Frequently Asked Questions
Does this replace our coating gauges?
No. Gauges remain the measurement truth, and the software builds on their readings. It fills in the areas between points and tracks trends. Review which gauges you already have and what they can feed with our team.
How accurate are the between-point estimates?
Accuracy depends on how many points you measure and how well spray data explains the pattern. Estimates should be checked against fresh readings at intervals, and confidence is shown with each map.
Which substrates and coatings are supported?
That depends on the gauge technology used for each layer and material. Steel, aluminum and composites often need different methods. Talk through your substrate and coating mix with our engineers before setup.
Can it help reduce paint consumption?
Narrowing the spread lets teams aim nearer to the lower limit with confidence. That can reduce material used per body. The size of the saving depends on your current variation and target.
How quickly can we see a first map?
If gauge data is already logged with body IDs, a first map can come quickly. Otherwise data capture comes first. Find out how soon your data could produce a first map in a short call.
Aim Closer to Target With Confidence
Bring gauge readings from one model. We will show the thickness map, the spread and the spray settings behind it.