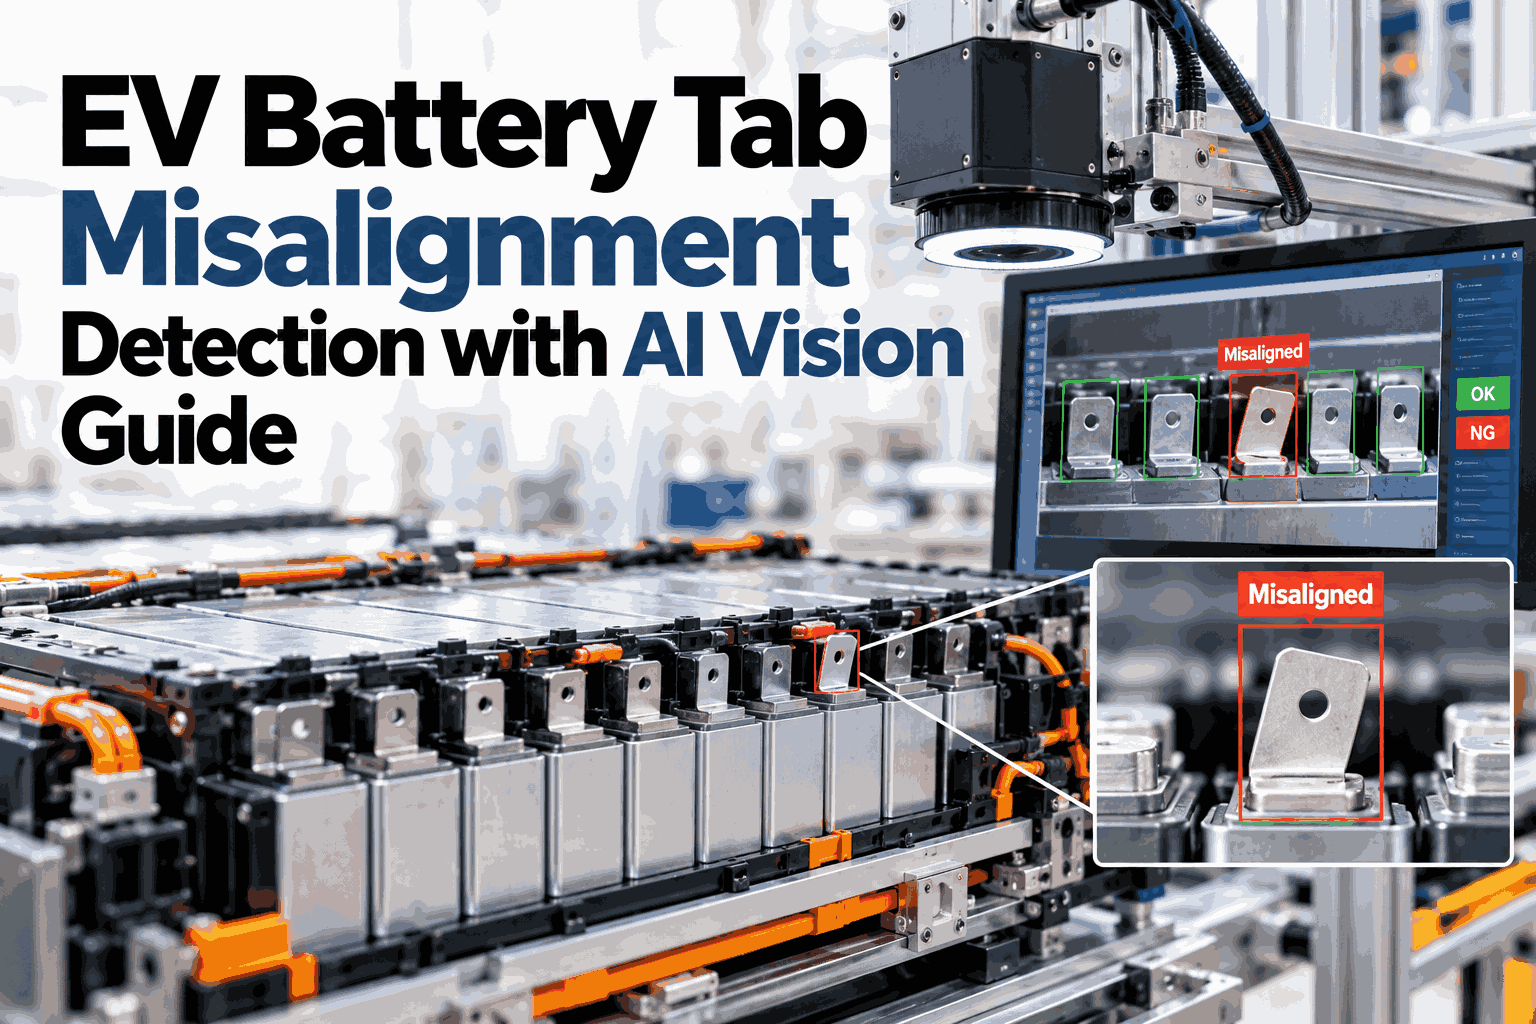
A tab weld can look perfect under a microscope and still sit in the wrong place. Weld quality asks whether the joint fused correctly. Position asks whether the tab is where the design says it should be, relative to the electrode edge and the opposite-polarity tab across the stack. Those are two different checks, and a line built to catch cold welds and spatter is not automatically built to catch a tab that drifted a few tenths of a millimeter out of place. Plants that want to see position checked as its own discipline can walk through a tab-position verification pipeline on real cell data in a short session.
Weld Quality Asks If It Fused. Position Asks If It Belongs There.
iFactory AI measures tab position against a tolerance band at line speed, independent of weld inspection, and diverts the cell before misalignment becomes a safety question.
Why Position Is Its Own Defect Category
A tab in the wrong position can still weld cleanly. The fusion can be sound, the joint strong, and the cell still carries a geometric defect that weld inspection was never built to see.
Position matters because of what sits near the tab, not because of how the tab was joined. A tab that has drifted toward the opposite-polarity side of the stack brings the anode and cathode closer together than the design allows, and that closing distance is where a safety risk lives, independent of weld quality entirely.
This is also why a position defect can slip past a quality system built mainly around weld inspection. Weld inspection is usually tuned to look at the joint itself: fusion depth, spatter, porosity, crack lines. None of those checks has any reason to look at where the tab started relative to the electrode edge, because that question sits one step upstream of the weld entirely. A plant can run a mature, well-tuned weld inspection program for years and never once measure tab position as its own number.
The gap shows up most clearly in failure investigations. When a field issue traces back to a tab that was too close to the opposite polarity, the weld inspection records for that cell often look clean, because the weld itself was fine. The defect lived in a measurement nobody was taking, not in a measurement somebody took and missed.
What Actually Moves a Tab Out of Position
Misalignment is rarely one dramatic failure. It usually accumulates from a handful of upstream steps that each nudge the tab a little, none of them obviously wrong on their own.
Die-Cutting Drift
A slightly worn die or a web-tension change shifts where the tab is cut relative to the electrode edge, before winding even begins.
Winding Tension Variation
Uneven tension during winding can carry a correctly cut tab into a slightly rotated or offset final position in the jelly roll.
Stacking Misregistration
In a stacked-cell format, each layer's tab has to land in registration with the ones above and below it, and small per-layer offsets compound across the stack.
Material Batch Variation
A foil or tab-material batch with slightly different stiffness can behave differently through the same equipment settings that handled the last batch without issue.
None of these causes announces itself. A die that is a few cycles into wear still cuts a tab that looks fine to a quick visual check, which is exactly why position has to be measured against a number, not judged by eye.
The practical consequence is that these causes rarely show up as a single bad cell surrounded by good ones. A worn die degrades gradually, so the cells it produces tend to drift together, a slow walk away from the design position rather than a sudden jump. A tension excursion during winding behaves differently, often producing a short run of affected cells before the process settles back. Recognizing which pattern a given run of rejects follows is itself diagnostic information, and it only becomes visible once position is being measured and logged cell by cell, not sampled occasionally by hand.
What "Measured Against a Tolerance Band" Actually Means
A tolerance band turns a judgment call into a measurement. Position verification compares the tab's actual coordinates against the design's allowed range, and the cell passes or fails on that comparison alone.
| What Is Measured | Compared Against | Why It Matters |
|---|---|---|
| Tab start position | Design-specified coordinate, found from the electrode's height profile | Confirms the tab sits where winding or stacking expects it to be |
| Edge-to-tab distance | Minimum clearance from the electrode edge | A tab too close to the edge risks folding or damage during winding |
| Opposite-tab clearance | Minimum separation from the opposite-polarity tab | Closing this distance is the condition a cited patent calls a direct safety concern |
| Tab geometry | Folding, end-face damage, and material-line deviation thresholds | A tab can be positioned correctly and still be damaged in a way that matters |
That last row matters more than it looks. Position and shape are related but separate checks, and a tab can pass a position check while carrying a fold or an end-face defect that a pure coordinate comparison would never catch on its own.
The opposite-tab clearance row deserves a second look, because it is the one most often missing from a setup that otherwise seems thorough. A plant that measures tab-to-edge distance has covered the winding-damage risk, but that measurement alone says nothing about how close the tab has come to the opposite polarity's tab across the stack. Those two distances can move independently of each other, since a tab can sit safely away from its own electrode's edge while still having drifted toward the opposing tab. Verifying both distances, not just one, is what closes the specific risk a tab inspection program exists to catch.
See Tab Position Measured Against Your Own Design Tolerance
Book a 30-minute session and iFactory AI will show position, edge clearance, and opposite-tab distance measured on your own cell data.
How the Measurement Actually Happens
Finding a tab's true start position is not as simple as looking for the tab shape in an image. The published patent approach is worth walking through because it shows how much engineering sits behind a number that sounds simple.
This two-source comparison, a measured position and an expected position, is what makes the check meaningful. A system that only looked for "a tab somewhere near where it should be" could not distinguish a correctly placed tab from one that drifted just inside a loose visual impression of correct.
The encoder step is easy to underrate, but it is what turns a height reading into a position measurement in the first place. Without a reliable running-length reference, a height jump only tells you a tab edge passed the sensor at some point; it says nothing about whether that point was where the design expected it. Pairing the optical height reading with the encoder's running-length count is what lets the system state a position in millimeters along the web, rather than just confirming that a tab-shaped feature went by.
Sensor placement also shapes what the measurement can tell you. A sensor mounted at the die-cutting stage reports position right where the tab is first created, which is the earliest and cheapest point to catch a problem. A sensor mounted later, after winding or stacking, reports position after handling has already had a chance to shift the tab further, which is a different and complementary signal rather than a redundant one.
Shape Defects That Ride Alongside Position
A position check answers one question. A complete tab inspection needs a few more, because a tab can be perfectly placed and still be the wrong shape.
Folding
A tab folded over on itself changes its effective geometry even if its base position is correct, checked by comparing height readings across a small margin around the tab.
End-Face Damage
Tearing or deformation at the tab's cut edge, checked within a narrow band just beyond where the tab ends.
Material-Line Deviation
A finer threshold, in the fractional-millimeter range, catches a tab edge that wanders from a straight cut line even when the start position itself is correct.
Running position and shape as separate, named checks rather than one blended "tab looks okay" verdict is what lets a plant tell, after a reject, exactly which of these actually failed, and the operator who has to intervene on the line.
The practical payoff of separating these checks shows up at the moment a reject happens. An operator looking at a single combined pass/fail code has to guess at what actually went wrong before deciding how to respond. An operator looking at a named position deviation, or a named folding flag, or a named end-face-damage flag, knows immediately whether the fix belongs at a die, a winding head, or a handling step, without needing to pull the physical cell and inspect it by hand first.
Where in the Process Position Should Be Checked
Tab position can drift at more than one stage, which is why checking only at the end of the line leaves earlier stages unaccountable for their own contribution to the problem.
Die-Cutting Stage
The earliest point to catch a drifting die before it cuts hundreds of tabs out of position, with the lowest cost to correct.
Winding or Stacking Stage
Confirms the tab survived handling into its final jelly-roll or stacked-layer position, catching tension and registration issues die-cutting could not see.
Pre-Weld Stage
The last checkpoint before the tab is joined permanently, where a caught misalignment can still be corrected rather than scrapped.
A gigafactory line running at full speed usually cannot afford a manual stop-and-check at every one of these stages, which is exactly the gap an inline position check closes without adding a cycle-time penalty the plant cannot absorb.
There is also a cost-of-correction argument for checking early rather than only at the end. A tab caught out of position at die-cutting can often still be adjusted or the affected material diverted before it absorbs the cost of winding, stacking, and electrolyte filling. The same defect caught only at final inspection, after the cell is fully built, has already consumed every downstream process step, which makes the scrap considerably more expensive than it needed to be. Checking position at more than one stage is as much a cost decision as a quality decision.
What a Reject Lane Actually Needs to Do
Finding a misaligned tab is only useful if the cell it belongs to is reliably separated from the ones that passed. The reject-lane logic matters as much as the measurement itself.
Divert, Not Just Flag
A measured failure should move the cell physically off the line, not only log a warning an operator may not see in time.
Carry the Measurement, Not Just Pass or Fail
A rejected cell's record should include the actual deviation value, so engineering can tell a borderline miss from a gross one.
Tie Back to the Upstream Stage
A cluster of rejects from one die-cutting station or one winding head points maintenance at the actual cause rather than the symptom.
A reject lane that only diverts the cell and discards the measurement throws away the most useful part of the event. The pass or fail decision protects the cell that would have shipped with a defect. The deviation value and stage attached to that decision are what prevent the next hundred cells from needing the same decision made about them, by pointing someone at the die or winding head before it produces another run of marginal cells.
Where iFactory AI Fits
iFactory AI runs tab-position and shape verification as their own measured checks, independent of weld inspection, and ties every reject back to its stage of origin.
Position Measurement
Tab start position is measured against the design-specified coordinate at line speed, not estimated from a visual impression.
Shape Verification
Folding, end-face damage, and edge-line deviation run as their own checks alongside position, not folded into one blended verdict.
Multi-Stage Coverage
Position can be verified at die-cutting, winding or stacking, and pre-weld, so a drift is caught at the earliest stage it appears.
Traced Reject Lane
Every diverted cell carries its measured deviation and originating stage, so a cluster of rejects points straight at its cause.
A Short Self-Check Before Your Next Ramp
Run these against your current tab inspection setup. A no points directly at the gap worth closing first.
Frequently Asked Questions
Isn't tab position already covered by weld inspection?
Weld inspection checks whether the joint fused correctly, which is a different question from whether the tab sits in the right place. A tab can weld perfectly while still being positioned too close to the opposite-polarity tab, which a cited patent on tab inspection names directly as a safety concern independent of weld quality. Treating position as its own measured check catches a failure mode weld inspection was never built to see.
What actually causes a tab to drift out of position?
Die-cutting wear, winding tension variation, stacking misregistration, and material batch changes each nudge tab position a little, usually without any single step looking obviously wrong on its own. See which stage is driving drift on your own line in a short review.
How is the tab's "true" position actually measured?
One published method reads a height profile as the electrode moves past an optical sensor, finds the tab's actual start from a sudden height change, and compares it against the expected start calculated from an encoder tracking how much material has run through. The distance between those two points is the position error the system scores.
Do we need to check position at every stage, or just once at the end?
Checking only at the end catches the problem late and tells you nothing about which upstream stage caused it. Position can drift at die-cutting, again during winding or stacking, and the earlier a drift is caught, the cheaper it is to correct rather than scrap. Ask support how multi-stage checking is typically staged for a line like yours.
What data do we need before setting up position verification?
The core is the design-specified tab position and allowed tolerance, line encoder data to track material position, and sensor access at whichever stages you want checked. Most gigafactory lines already have the encoder and control infrastructure in place. The early weeks of a rollout focus on calibrating the tolerance band against your actual design specification rather than building the measurement approach from scratch.
Measure Tab Position as Its Own Discipline
iFactory AI checks tab position, edge clearance, and shape against your design tolerance, independent of weld inspection, and traces every reject to its cause. Book a walkthrough on your own line.