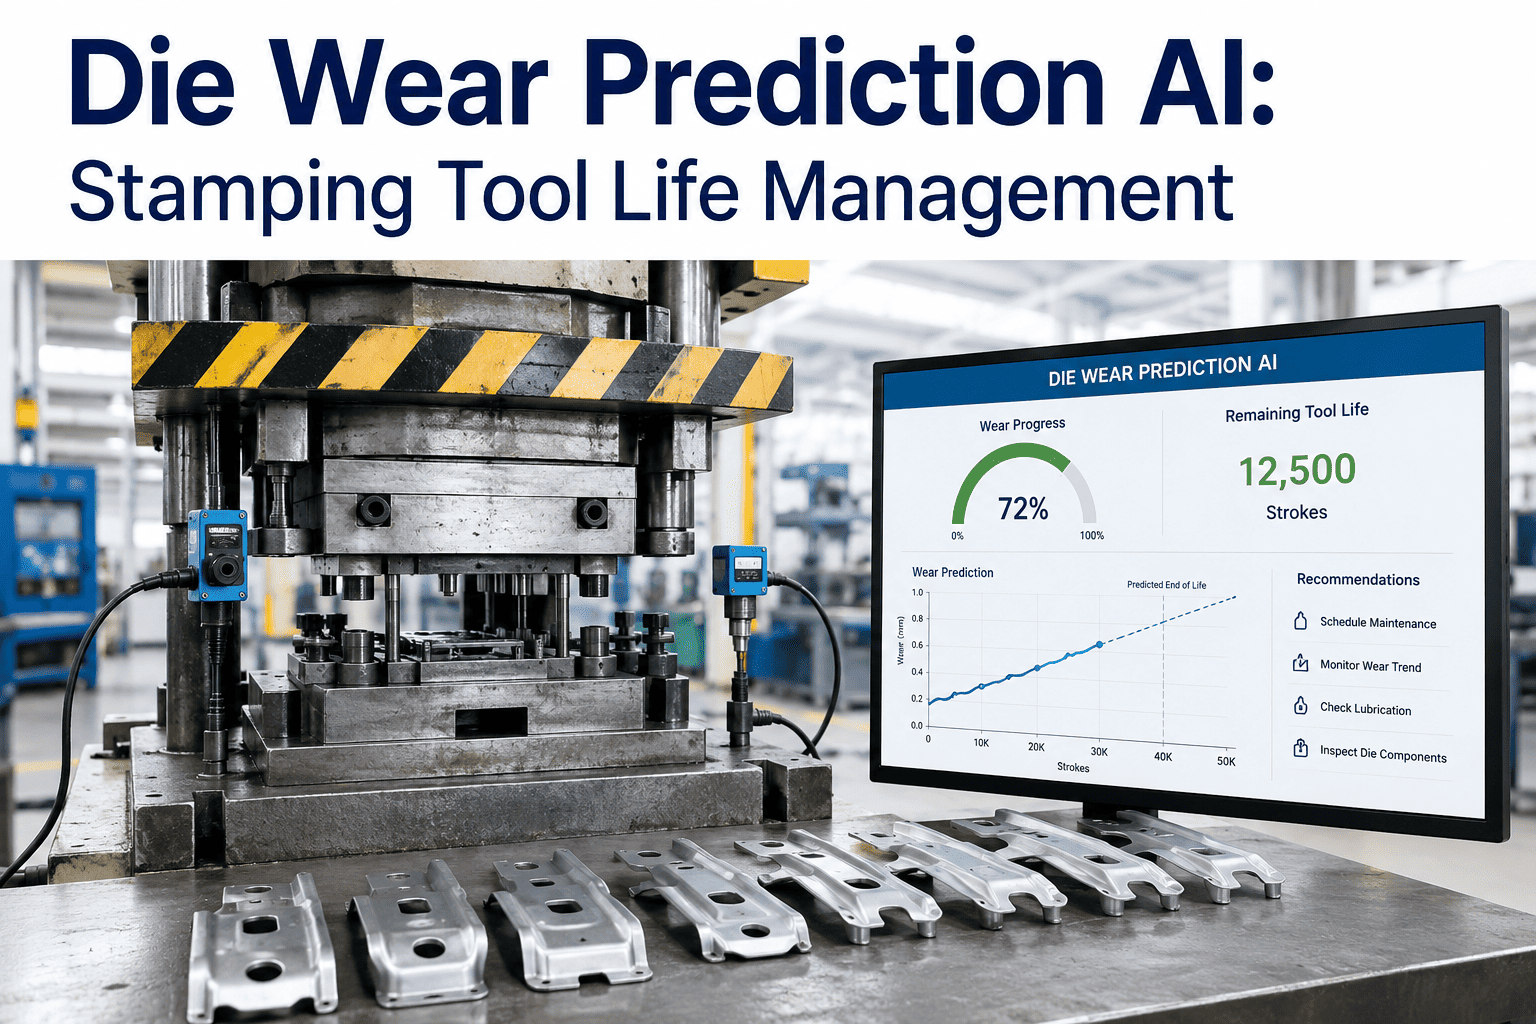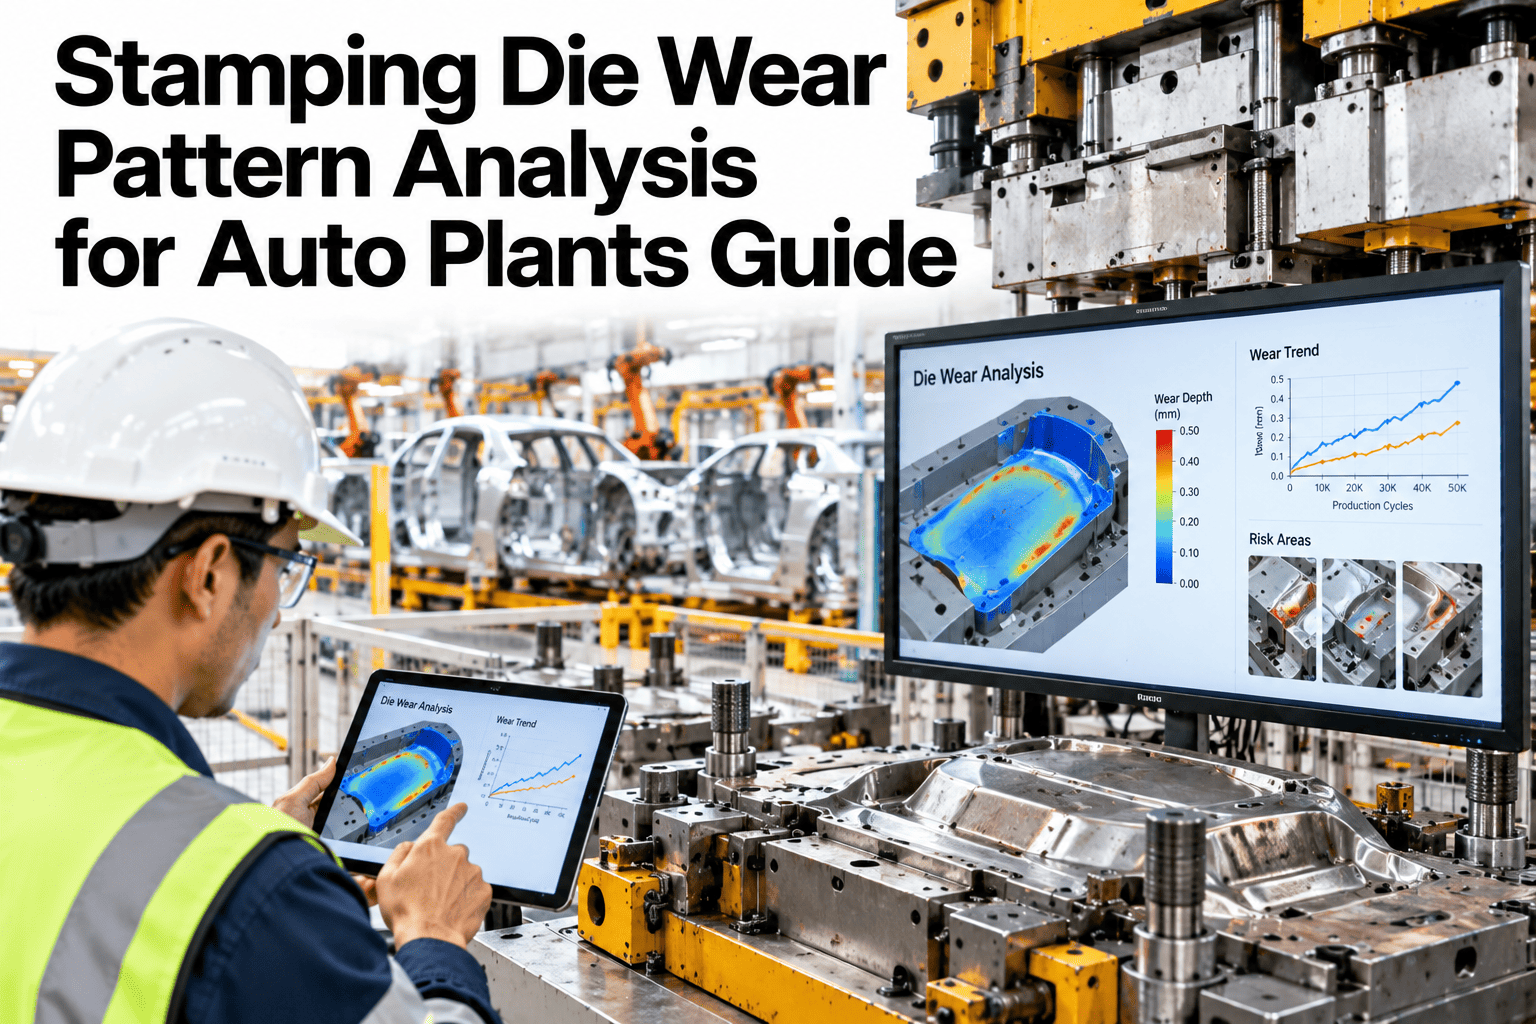
A stamping die rarely fails all at once. It wears in a few small places, edges soften, radii polish and surfaces start to gall, and the parts it makes drift slowly out of tolerance until a burr or a split gives it away. Most plants sharpen and repair by hit count or by habit, which treats every die as if it wore the same way. Wear pattern analysis shows where each die wears and how fast. Plants who want to see it can ask iFactory AI how die wear patterns are mapped and tracked.
Read Die Wear Patterns Before They Show Up as Scrap
iFactory AI maps wear hot spots, correlates hit counts with part quality and tunes lubrication, so dies are serviced when condition says so and life is extended cleanly.
Where a Stamping Die Actually Wears
Wear is not uniform. The bar shows an illustrative split of where it tends to concentrate on a typical die.
How Each Wear Mechanism Shows Up
Different wear types leave different clues. The matrix, shown as an illustration, links mechanism to evidence.
| Wear Mechanism | Burr Height | Press Tonnage | Surface Marks |
|---|---|---|---|
| Edge dulling on trim steels | High | Moderate | Low |
| Galling on draw surfaces | Low | Moderate | High |
| Radius wear and polishing | Moderate | Moderate | Moderate |
| Guide and clearance wear | Moderate | High | Moderate |
| Coating failure | Low | Moderate | High |
How Part Quality Drifts With Hit Count
Wear builds with every stroke, and quality follows it. The chart shows an illustrative view of burr growth over a die's life between services.
Lubrication Regime and Its Effect
Lubrication is the cheapest way to slow wear. This table shows the main variables and what to watch.
| Variable | Why It Matters | What to Watch |
|---|---|---|
| Lubricant type and grade | Matches the material and forming severity | Galling or scoring on draw surfaces |
| Application rate | Too little wears, too much causes slugs and slip | Coverage consistency across the blank |
| Application timing | Must be present before the stroke | Dry strokes after interruptions |
| Cleanliness and condition | Contaminated lube scores the die | Particles and degradation over time |
Find Out Where Your Dies Are Wearing Fastest
Book a 30-minute session and iFactory AI will review your die records, hit counts and part quality to show where service intervals can be set by condition.
Servicing by Hit Count Alone or by Condition
Hit count is a good start, but dies of the same design can wear at different speeds.
A Five-Step Die Wear Study
A study does not need special equipment. These steps work with data most plants already have.
Log hit counts, services and repairs for each die.
Capture burr height and tonnage at regular intervals.
Mark where wear and repairs occur on the die.
Compare wear growth with hit count and lubrication.
Set service points by condition and verify the result.
Die Wear Inspection Checklist
Use this list at every die change and service. Each box should be answerable from records.
A Composite Scenario: The Die That Wore Unevenly
This is a composite example, not a named plant. It shows how mapping changes a repair.
Mistakes That Shorten Die Life
These habits quietly cut die life.
Servicing by calendar
Wear follows strokes and material, not dates.
Ignoring lubrication drift
Small changes in coverage can double wear in the wrong place.
Not recording repairs
Without history, patterns stay invisible.
Replacing instead of studying
A new component may wear in the same spot for the same reason.
What iFactory AI Adds to Die Health
iFactory AI is smart manufacturing and industrial software for automotive stamping plants. Explore die health monitoring in a live product tour on realistic press data.
A 30-Day Plan to Start
A month is enough to build a first wear study on a handful of dies.
Review of Stamping Die Wear Analysis
A practical review of what makes die wear studies useful, written as editorial guidance rather than a named expert quote.
Map before you repair
Knowing where a die wears prevents repeat repairs in the wrong place.
Let condition adjust the count
Hit count sets the first estimate and condition refines it.
Treat lubrication as a lever
It is the cheapest and fastest change in most wear studies.
Frequently Asked Questions
Why do dies of the same design wear differently?
Material batches, lubrication, press condition and part mix all change wear. See wear differences between similar dies on live data in a short demo. That is why a single service interval rarely fits every die.
Can hit count alone predict die service?
It is a useful starting point, but condition data such as burr height and tonnage improves accuracy. Using both reduces early service and late surprises. The mix depends on your parts.
How does lubrication affect die life?
The right type, rate and timing reduce friction and galling, which slows wear. Ask support how lubrication settings are logged against wear on your presses. Often it is the first and cheapest improvement.
What data do we need to start?
Hit counts, service and repair records, and a regular measure of part quality such as burr height. Press tonnage helps if it is available. Many plants already hold most of this.
How quickly can we see results?
Many plants find a clear wear pattern on their first dies within weeks. Book time to scope a die wear pilot with your tooling team. One extended die interval proves the value.
Extend Die Life by Reading the Wear, Not the Calendar
iFactory AI maps wear, correlates hit counts with quality and tunes lubrication so dies are serviced at the right moment. Book a walkthrough to see it on your own dies.