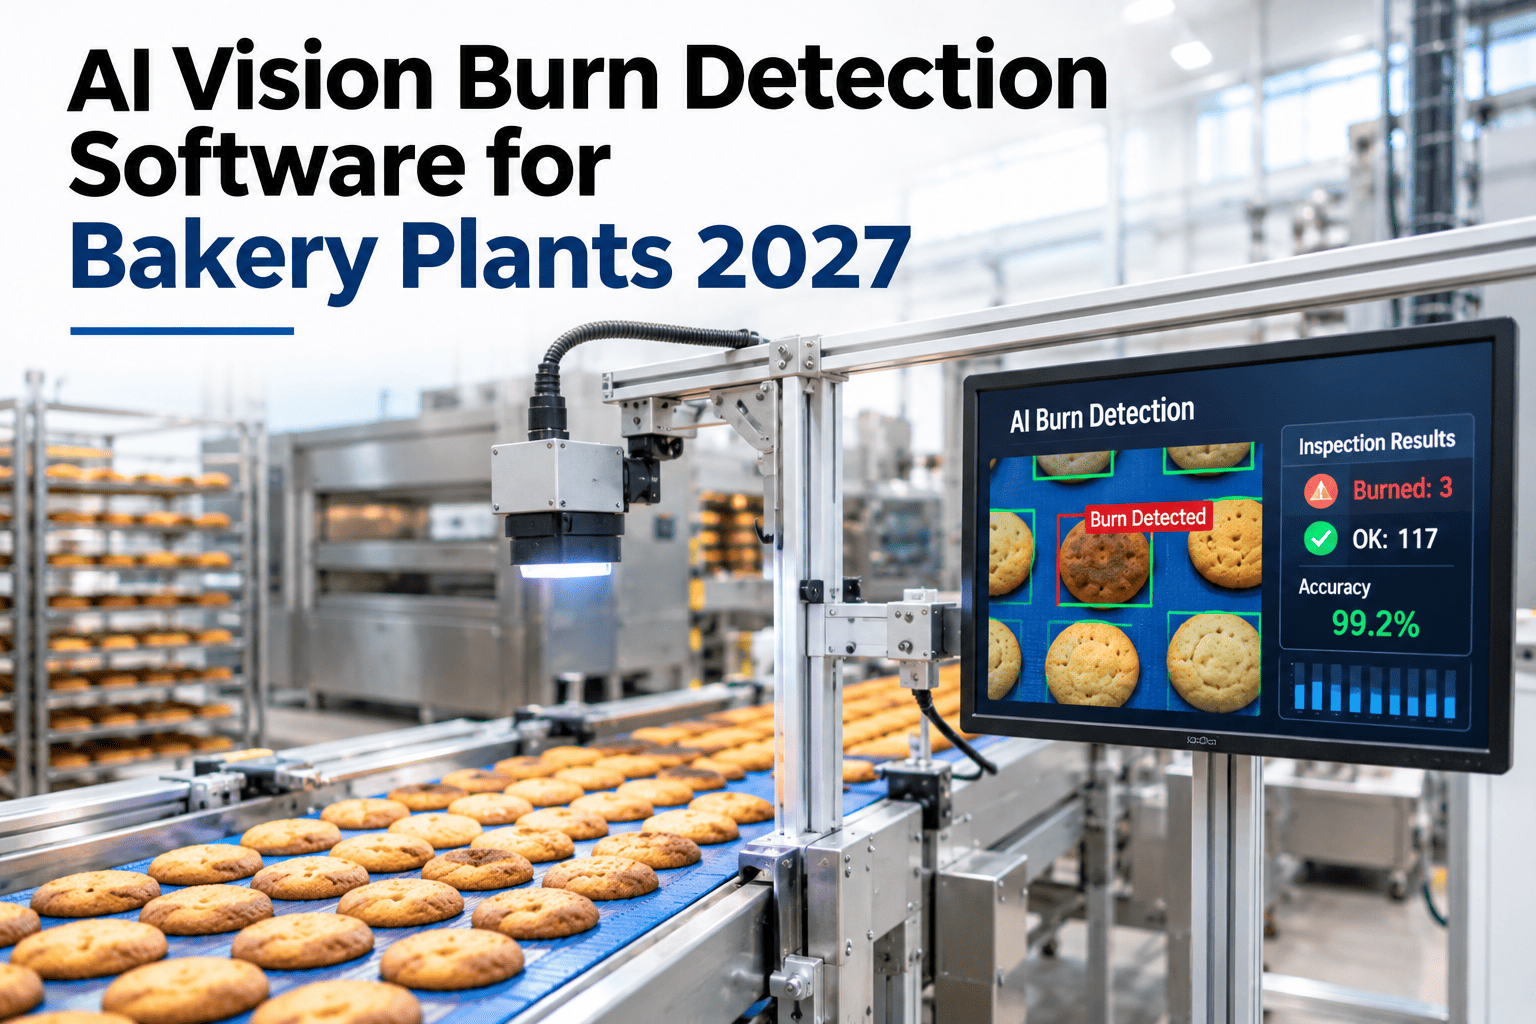
A burn grade that just says "reject" tells a bakery operator nothing about where to look, and on a line with a dozen burner zones across multiple lanes, that's the difference between fixing the problem in minutes and chasing it for a shift. Per-unit grading paired with per-zone attribution — tying a burn pattern back to the specific lane, band or burner that produced it — is what turns a reject count into a maintenance work order instead of a mystery. iFactory AI's food vision team can map your own oven's burn patterns back to specific zones before your next burner service.
A Reject Count Without a Zone Attached Is a Mystery, Not a Work Order
Grading every cookie, chip and pretzel per unit, then attributing the burn pattern back to the specific lane, band or burner responsible, turns a rising reject rate into a targeted fix instead of a guessing game.
Why a Plant-Wide Reject Rate Hides the Actual Problem
A tunnel oven running multiple lanes with independently controlled burner zones can have one zone running hot while the rest run perfectly normal, and a single plant-wide burn reject percentage blends that one hot zone into an average that looks only mildly elevated. The operator ends up adjusting the whole oven's settings in response to a problem that was actually isolated to one burner, over-correcting everywhere except where the real issue was.
Independently controlled lanes can drift differently from each other.
Within one lane, different heating bands can run hot or cool unevenly.
A single burner element aging or fouling affects only its own zone.
A plant-wide reject percentage can hide a severe but localized problem.
How Per-Zone Attribution Actually Works
Attribution depends on knowing exactly which lane, band and burner each unit passed through, tied to its burn grade at the end of the line. Our team can review your current oven zone layout before building the attribution model.
Vision inspection assigns a burn grade to every cookie, chip or pretzel, not a sample.
Lane, band and approximate burner exposure logged as each unit moves through.
Burn severity mapped back to exactly which lane, band or burner produced it.
Maintenance gets a specific burner to check, not an instruction to inspect the whole oven.
Plant-Wide Average vs Per-Zone Attribution
| Approach | What It Shows | Time to Fix |
|---|---|---|
| Plant-wide reject rate | An overall percentage, blended across all zones | Hours to days of manual inspection to isolate |
| Lane-level grading | Which lane is contributing most rejects | Hours — still need to check every burner in that lane |
| Per-zone attribution | The specific lane, band and burner responsible | Minutes — the work order names the exact zone |
Find Out Which Burner Is Actually Driving Your Reject Rate
Share recent burn reject data and your oven's zone layout, and see which specific zone the pattern traces back to.
A Composite Scenario: The Oven Adjustment That Fixed Nothing
Picture a snack plant responding to a rising plant-wide burn reject rate by lowering the overall oven temperature setpoint across all four lanes, a broad fix aimed at a problem that was actually isolated.
Per-zone attribution traced the burn pattern to a single aging burner element in one band of Lane 2, while the other three lanes had been running correctly the entire time. The broad temperature reduction meant to fix the burn problem had actually under-baked product on three healthy lanes while barely touching the real cause. Replacing the one burner element resolved the issue without affecting the rest of the oven. The scenario illustrates the risk of treating a blended average as the whole picture; actual causes vary by oven design.
Where iFactory AI Fits
iFactory AI grades every unit's burn severity individually and correlates it against lane, band and burner position, so a rising reject rate routes directly to the specific zone responsible instead of prompting a plant-wide guess.
Every piece graded, not a sample, so no burn pattern goes unseen.
Burn severity tied to the exact lane, band and burner responsible.
Maintenance gets a named zone, not an instruction to search the whole oven.
Frequently Asked Questions
Attribution accuracy depends on how granular the oven's own zone control is — a line with individually controlled burner elements per band gives the tightest attribution, while coarser zone control still narrows the problem to a band or lane rather than the whole oven. Review attribution granularity for your oven's zone layout.
Attribution relies primarily on tracking unit position through the oven and grading at the exit, so it typically doesn't require new sensors inside the oven, though it does depend on knowing the oven's own zone control layout. Confirm what your current oven data provides.
A burn pattern isolated to one consistent zone across different product batches points to the burner or that zone's heat source, while a pattern that shifts with loading density or belt speed changes points elsewhere, and correlating both signals helps separate the two. Discuss how causes are distinguished for your line.
Grading models are trained on a representative range of acceptable natural variation for each product, so normal browning differences between pieces aren't flagged as burns — only genuine deviation outside that trained range triggers a grade. Review how natural variation is handled for your products.
Yes, a confirmed zone-level pattern can generate a maintenance work order naming the specific burner or zone, rather than requiring a quality team to manually report the finding to maintenance separately. See the work order generation flow in a walkthrough.
Stop Guessing Which Burner Is Causing Your Rejects
iFactory AI grades every unit and attributes burn patterns back to the specific lane, band or burner, so maintenance gets a work order, not a mystery.