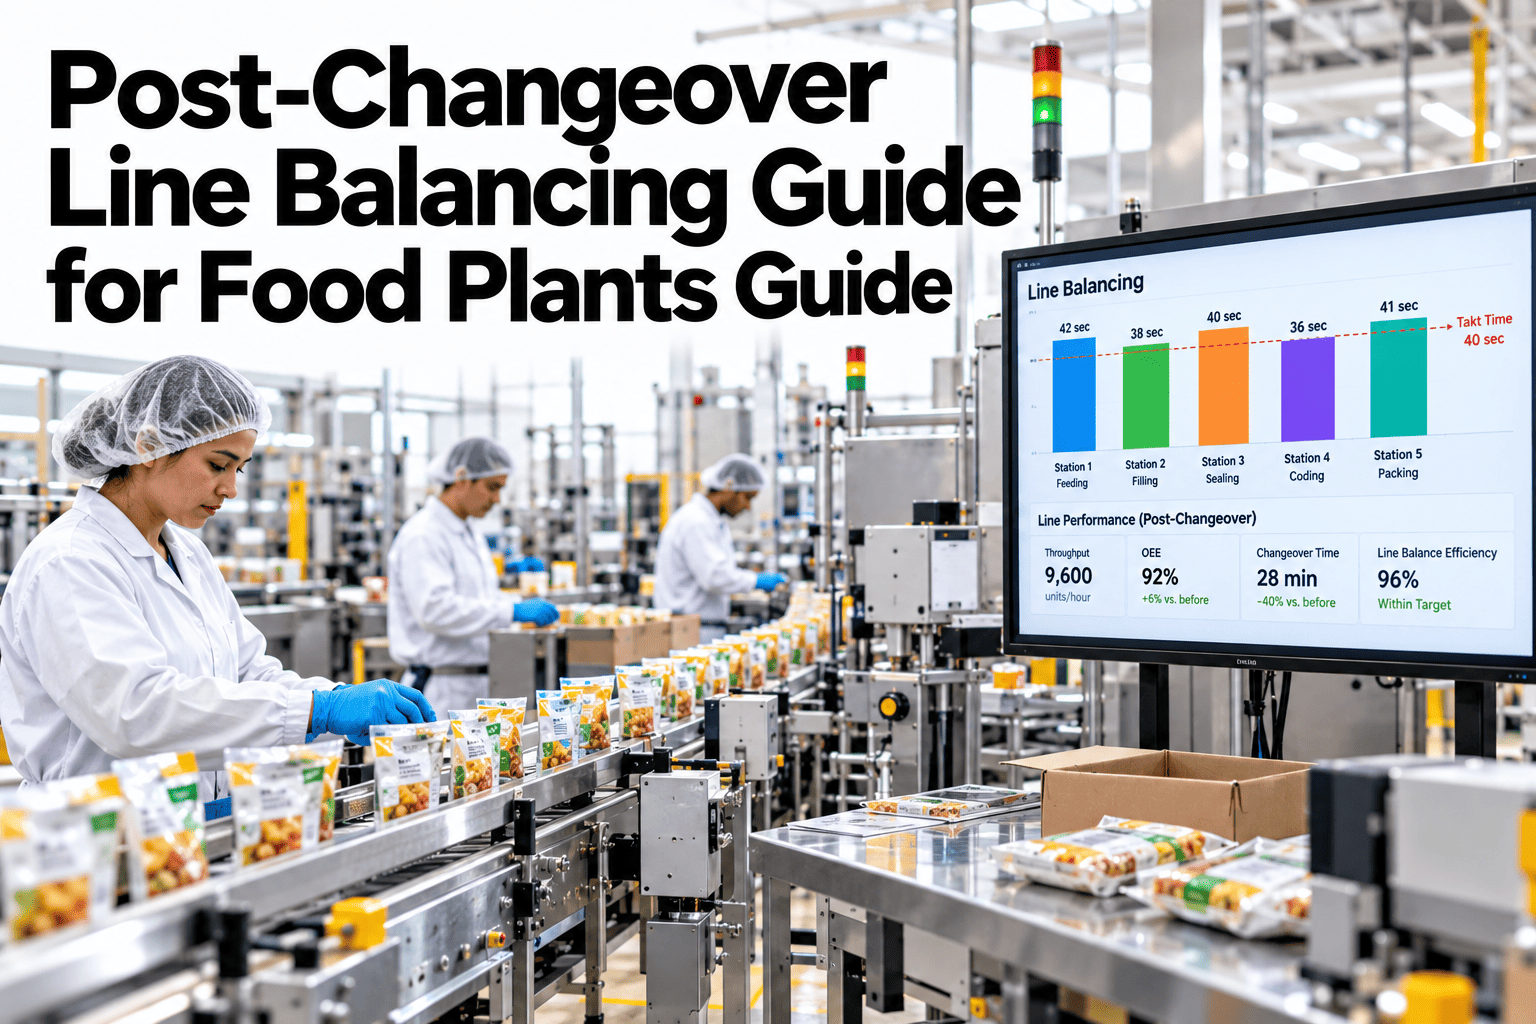
The changeover itself often isn't the biggest loss around a SKU switch, the slow first hour afterward is. A line balanced for one product's fill speed, pack rate and buffer needs isn't automatically balanced for the next one, and running it at the old settings produces exactly the kind of slow ramp-up that quietly eats more time than the changeover did. Presetting speeds, buffer levels and staffing for the incoming SKU before the line restarts closes most of that gap. Plants can review their own post-changeover ramp data in a short session.
The First Hour After Changeover Is Where Balance Actually Matters
iFactory presets speed, buffer and staffing targets per SKU, so the line ramps to full rate in minutes, not an hour.
Why Line Balance Changes With Every SKU
Fill speed, pack pattern, carton size and buffer dwell time all shift when the product changes, which means a line balanced for the previous SKU is, almost by definition, out of balance for the next one until someone adjusts it.
| Factor | Why It Changes With SKU | Fix |
|---|---|---|
| Fill or form speed | Different product viscosity, weight or size changes optimal fill rate | Preset speed target per SKU before restart |
| Buffer levels | Downstream dwell time varies by pack configuration | Preset buffer targets to match the new product's flow |
| Staffing allocation | Some SKUs need more manual intervention at specific stations | Adjust staffing plan to match the incoming SKU's demands |
| Reject and inspection rate | New product variation affects quality check throughput | Plan inspection capacity for the specific SKU's needs |
Measure Your Own First-Hour Ramp Time
Book a 30-minute session and iFactory will measure how long your line actually takes to reach full rate after a changeover.
Three Levers to Preset Before Changeover
SKU-Specific Speed Presets
Each SKU's optimal line speed is stored and applied automatically at changeover, rather than relying on an operator to adjust from the prior setting.
Buffer Sizing Per SKU
Buffer levels are preset to the new product's flow characteristics, avoiding the starve-and-block cycles a mismatched buffer causes.
Staffing Plan Alignment
Staffing is matched to where the incoming SKU actually needs attention, instead of carrying over the prior SKU's allocation by default.
Before and After Presetting
One line compared time to reach full rate after changeover, before and after SKU-specific presets were implemented.
Signals Your Ramp-Up Needs Attention
Where iFactory Fits
iFactory builds SKU-specific presets for speed, buffer and staffing, applied automatically the moment a changeover completes.
Automated Speed Presets
Each SKU's optimal speed profile is stored and applied automatically rather than left to operator judgment.
SKU-Matched Buffer Targets
Buffer levels are preset to match the incoming product's flow, avoiding starve-and-block cycles.
Staffing Guidance by SKU
Staffing plans recommend allocation based on where the specific incoming SKU actually needs attention.
Ramp-Up Tracking
Time to reach full rate is tracked per changeover, confirming presets are actually closing the gap.
Reviewed by iFactory's Lean Manufacturing team for alignment with standard line balancing practice. The ramp-up figures shown are illustrative; actual improvement depends on how varied your SKU mix is and how well current settings are already matched per product.
Frequently Asked Questions
How are SKU-specific presets initially built?
They're typically derived from historical production data showing the optimal settings each SKU has run at previously, refined through a short validation period to confirm accuracy. Support can review what historical data you already have.
Does this work for SKUs we run infrequently?
Yes, once a preset is built for a SKU it remains available for future runs regardless of frequency, which is particularly valuable for infrequent SKUs where operators are less likely to remember the right settings.
Can presets be adjusted if line conditions change over time?
Yes, presets should be periodically reviewed against actual performance and adjusted as equipment wear, material changes or other factors shift the optimal settings. See how preset review works in a short session.
Does this require new line hardware?
Usually not. Most presets apply through existing PLC and HMI settings already capable of storing SKU-specific recipes, rather than requiring new equipment.
How does this interact with a SMED changeover program?
They address different parts of the same timeline, SMED shortens the changeover itself while line balancing shortens the ramp-up after it, and the two together typically produce the largest combined gain. Ask support how these combine for your line.
Start Every New SKU Already Balanced
iFactory presets speed, buffer and staffing per SKU so your line ramps to full rate in minutes. Book a walkthrough on your own data.