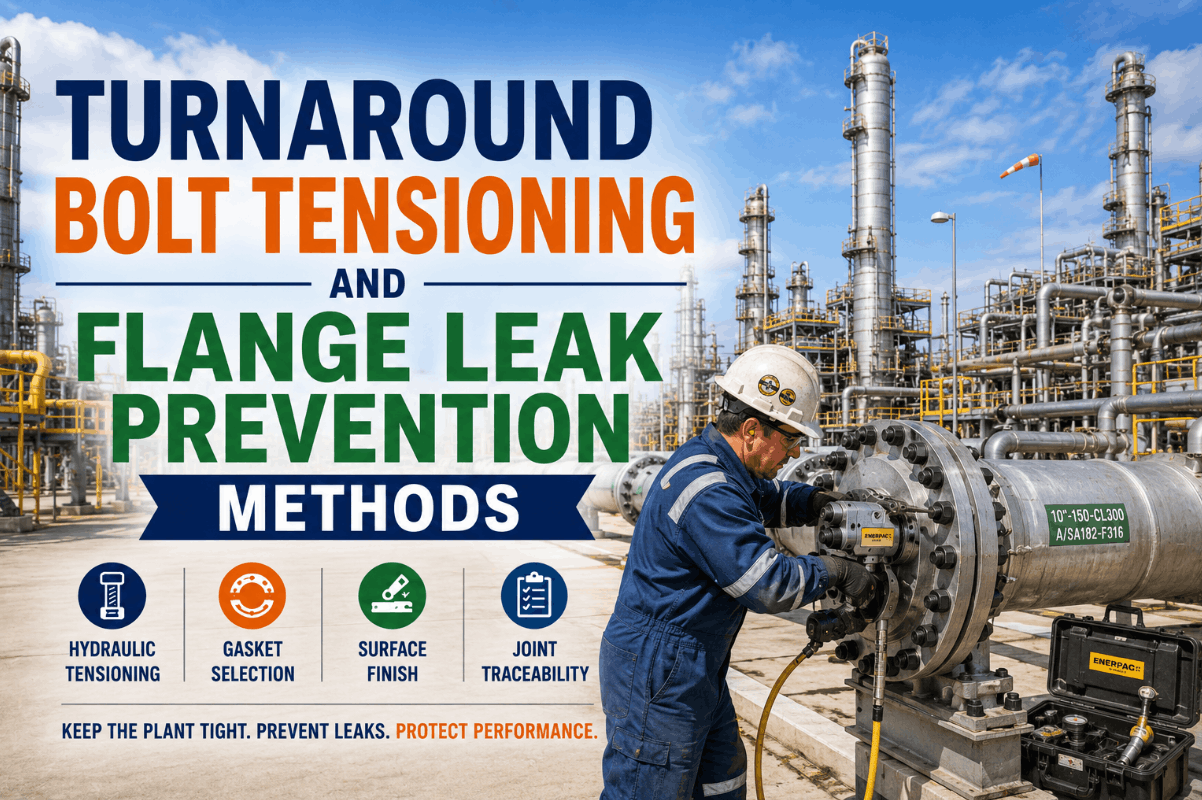
Half of all leaks discovered in the first weeks after a turnaround trace back to one source: bolted flange joints that were torqued, not tensioned, and never verified against a documented joint trace. A flange that looks correctly assembled on the outside can still be carrying uneven bolt load, a gasket seated against the wrong surface finish, or a tightening sequence that was never actually followed in the field. The cost of that gap shows up during startup — when a unit under full pressure and temperature reveals every joint that was assembled on assumption rather than verified preload. Closing that gap during the turnaround itself, before the unit is repressurized, is the difference between a clean startup and a flange leak punch list that follows the plant for weeks. iFactory's turnaround joint integrity platform gives bolting crews and QA teams a connected system for hydraulic tensioning records, gasket selection traceability, surface finish verification, and a live joint trace that follows every flange from breakout to final torque check. Facilities that have Book a Demo with iFactory consistently report fewer post-startup leak repairs and faster turnaround close-out on critical bolted joints.
Is Your Flange Joint Data Working for You During Turnaround?
Connect hydraulic tensioning records, gasket selection, surface finish checks, and joint trace documentation into one verified system before the unit is repressurized.
Why Flange Joints Are the Most Common Source of Post-Turnaround Leaks
Flanges are designed to be leak-free. When a joint leaks after startup, the cause is almost never a defective flange or gasket — it is a process failure somewhere in the assembly sequence. Uneven bolt load from manual torquing, a gasket selected for the wrong service, a flange face with surface imperfections the gasket can't conform to, or a tightening pattern that skipped the gradual multi-pass sequence — any one of these is enough to produce a joint that holds at ambient conditions and weeps the moment the unit comes up to temperature and pressure. With thousands of bolted joints broken and remade during a major turnaround, the traditional approach of paper torque sheets and visual sign-off simply cannot catch every deviation before the unit is closed up.
iFactory's joint integrity platform addresses this by digitizing every step of the bolting process — from joint identification through final verified preload — so that QA teams can confirm, joint by joint, that the documented procedure was actually the procedure followed in the field.
Hydraulic Tensioning Records
Capture stretch, pressure, and sequence data for every bolt tensioned hydraulically, giving QA a verified preload record instead of a torque wrench estimate.
Gasket Selection Traceability
Match gasket type, material, and rating against the joint's specified service condition before installation, flagging any mismatch before the flange is closed.
Surface Finish Verification
Log flange face condition checks — scoring, pitting, flatness — at breakout and again before gasket installation, so a damaged face is caught before reassembly.
Live Joint Trace
Follow every flange from breakout to final torque check with a QR-tagged joint record, eliminating the paper trail gaps that leave joints unaccounted for at close-out.
Building a Connected Joint Integrity Program for Turnaround Bolting
A purpose-built joint integrity platform has to address four practical requirements that paper torque sheets were never designed to handle: precise preload application on critical joints, service-correct gasket selection, surface condition control, and a traceable record that ties every joint back to the crew, tooling, and procedure used. Bolting supervisors who have Book a Demo with iFactory consistently point to the joint trace as the single feature that changes how close-out is verified.
| Joint Element | Primary Function | Turnaround Application | Integrity Benefit | Priority Level |
|---|---|---|---|---|
| Hydraulic Tensioning | Precise bolt preload application | Critical & High-Pressure Joints | Uniform clamp load, no over-torque | Critical |
| Gasket Selection Check | Service-rated gasket matching | All Reinstated Flanges | Prevents wrong-gasket leaks | Critical |
| Surface Finish Inspection | Flange face condition logging | Breakout & Reassembly | Catches damaged faces early | High |
| Joint Trace & QR Tagging | Full joint history tracking | Plant-Wide Bolted Joints | Audit-ready close-out record | High |
| Startup Leak Trend Analysis | Post-TAR leak rate modeling | Repressurization & Startup | Faster startup, fewer call-backs | Standard |
How iFactory Supports a Disciplined Flange Assembly and Verification Sequence
Leak-free flange assembly depends on controlling every variable in sequence, not just hitting a final torque number. Most mills and refineries still verify joints through paper sign-off and a supervisor's spot check at the cooling-off period before startup — an approach that misses the gradual, multi-pass tightening sequence and surface preparation steps that actually determine whether a joint holds under service conditions. iFactory's platform digitizes each step in that sequence so it can be verified, not assumed.
Joint Identification and Criticality Classification
Tag every flange scheduled for breakout with a joint ID, service rating, and criticality class that determines whether torque wrenches or hydraulic tensioning is required.
Surface Finish and Face Condition Check
Log flange face condition at breakout — scoring, pitting, flatness — and flag any face requiring rework before a new gasket can be seated against it.
Gasket Selection and Service Match Verification
Confirm gasket type, material, and pressure-temperature rating against the joint's specified service before installation, blocking mismatched gaskets at the point of use.
Multi-Pass Hydraulic Tensioning or Calibrated Torque
Apply preload in progressive passes using calibrated hydraulic tensioners or torque wrenches, with stretch or torque values logged against the joint record at every pass.
Final Verification and Startup Leak Monitoring
Confirm final preload against the joint's target value, close the joint record, and track any leak indications during repressurization back to the original assembly data.
"Before connecting our bolting records into iFactory, we'd close out a turnaround with a stack of paper torque sheets and find out which joints actually held once the unit was back at pressure. Since tracking hydraulic tensioning data and gasket selection against every joint ID, our post-startup flange leak call-backs have dropped sharply, and close-out audits take a fraction of the time."
Top Operational Gaps Behind Post-Turnaround Flange Leaks
Most plants pursuing improvements to their turnaround flange management programs encounter a predictable set of recurring gaps. Recognizing these before the next major TAR helps bolting supervisors and QA teams direct limited crew hours toward the joints most likely to leak on startup.
Manual torque wrenches applied without a progressive multi-pass sequence produce uneven bolt load, leaving some bolts under-tensioned and others over-stressed on the same flange.
A flange face with scoring or pitting from the last breakout is reassembled without inspection, leaving the gasket unable to conform to the imperfection and seal properly.
A gasket rated for the wrong pressure class or chemical service is installed because the correct specification wasn't checked against the joint at the point of assembly.
Joint assembly data recorded on paper is difficult to reconcile at close-out, leaving QA teams unable to confirm which joints received hydraulic tensioning versus manual torque.
Without a joint ID system, a leak discovered during startup can't be traced back to the crew, tooling, or procedure used during assembly — making root cause analysis slow and incomplete.
Thousands of joints broken and remade on a tight TAR schedule create pressure to skip verification steps, increasing the odds that a critical joint is closed without final preload confirmation.
Closing these gaps takes more than a stricter procedure document — it requires a platform that makes every assembly step verifiable in real time. Bolting supervisors regularly Book a Demo to see how joint trace data applies to their unit's critical flange population.
Connecting Joint Integrity Data Into Your Existing Turnaround Workflow
Joint integrity tracking only works if it fits inside the bolting crew's existing field workflow rather than adding a separate documentation burden on top of it. iFactory's platform is built to log tensioning, gasket, and surface finish data at the point of work — on a tablet at the flange — and tie that record automatically to the joint's QR tag, work order, and turnaround schedule, without requiring crews to re-enter data into a separate system after the fact.
Key Joint Integrity Capabilities for Turnaround Bolting Crews
Log every pass of a multi-stage hydraulic tensioning or torque sequence, with stretch or torque values recorded against the joint at each stage.
Cross-check installed gasket specifications against the joint's pressure-temperature rating and process service before sign-off is allowed.
Scan a joint's QR tag in the field to pull up its full history — breakout condition, gasket used, tensioning data, and final verification status.
Link any leak indication found during repressurization directly back to the original joint record to identify whether the cause was preload, gasket, or surface condition.
Close Out Your Next Turnaround With Verified Joints, Not Paper Sign-Offs
Deploy a unified platform that connects hydraulic tensioning data, gasket selection, surface finish checks, and joint trace records for every critical flange in your turnaround scope.
Turnaround Flange Management — Common Questions Answered
Why is hydraulic tensioning preferred over torque wrenches for critical joints?
Hydraulic tensioning applies a direct, measurable stretch to the bolt, giving a precise preload reading independent of thread friction — a variable that makes torque-based tightening less consistent on critical, high-pressure joints.
What is a multi-pass tightening sequence, and why does it matter?
A multi-pass sequence applies bolt load gradually in stages, often 30%, 60%, then 100% of target, in a star pattern. This lets the gasket relax evenly and prevents flange distortion that uneven, single-pass tightening can cause.
How does surface finish affect whether a flange leaks?
A gasket can only seal if it conforms to the flange face. Scoring, pitting, or an uneven surface from a prior breakout prevents proper seating, so face condition should be checked and reworked before every reassembly.
Can iFactory's joint trace integrate with our existing work order system?
Yes. iFactory ties each QR-tagged joint record to its work order and turnaround schedule, so tensioning, gasket, and inspection data are captured at the point of work without a separate manual data entry step.
How does joint trace data help during a startup leak investigation?
If a leak appears during repressurization, the joint's full record — breakout condition, gasket used, and tensioning values — is available immediately, letting teams identify the likely cause without reconstructing paper records.