Coke rate has fallen from around 500 kilograms per ton of hot metal in older blast furnace practice down to a range of 286 to 320 kilograms per ton in most modern furnaces today, and pulverized coal injection has done most of that work by taking over a share of the reducing and heating role coke used to carry alone. That drop did not happen through a single breakthrough, it happened through years of incremental gains in burden distribution, hot blast temperature, and injection rate tuning that most furnace crews never see summarized in one place. Every additional kilogram of coke saved per ton is a direct fuel cost reduction that compounds across every ton the furnace produces for the rest of its campaign, and finding where your own furnace still has room to close that gap starts with comparing your actual coke rate against what your burden and injection setup should be capable of.
The Best Blast Furnaces Run At Roughly Half The Coke Rate Of Older Practice
Modern blast furnaces commonly operate in the 286 to 320 kilogram per ton hot metal coke rate range, down from around 500 kg/tHM in older practice, largely through pulverized coal injection and better burden control. The gap between your furnace and that range is a direct, ongoing fuel cost.
Coke Rate Isn't One Number To Chase, It's The Output Of Four Separate Systems
Treating coke rate as a single target to push down often leads to isolated fixes that fight against each other, since coke rate is really the combined result of burden distribution, hot blast conditions, injection rate, and coke quality all interacting simultaneously. A furnace that improves one of these in isolation without checking the others frequently finds the gain smaller than expected, or offset entirely by a side effect elsewhere in the process.
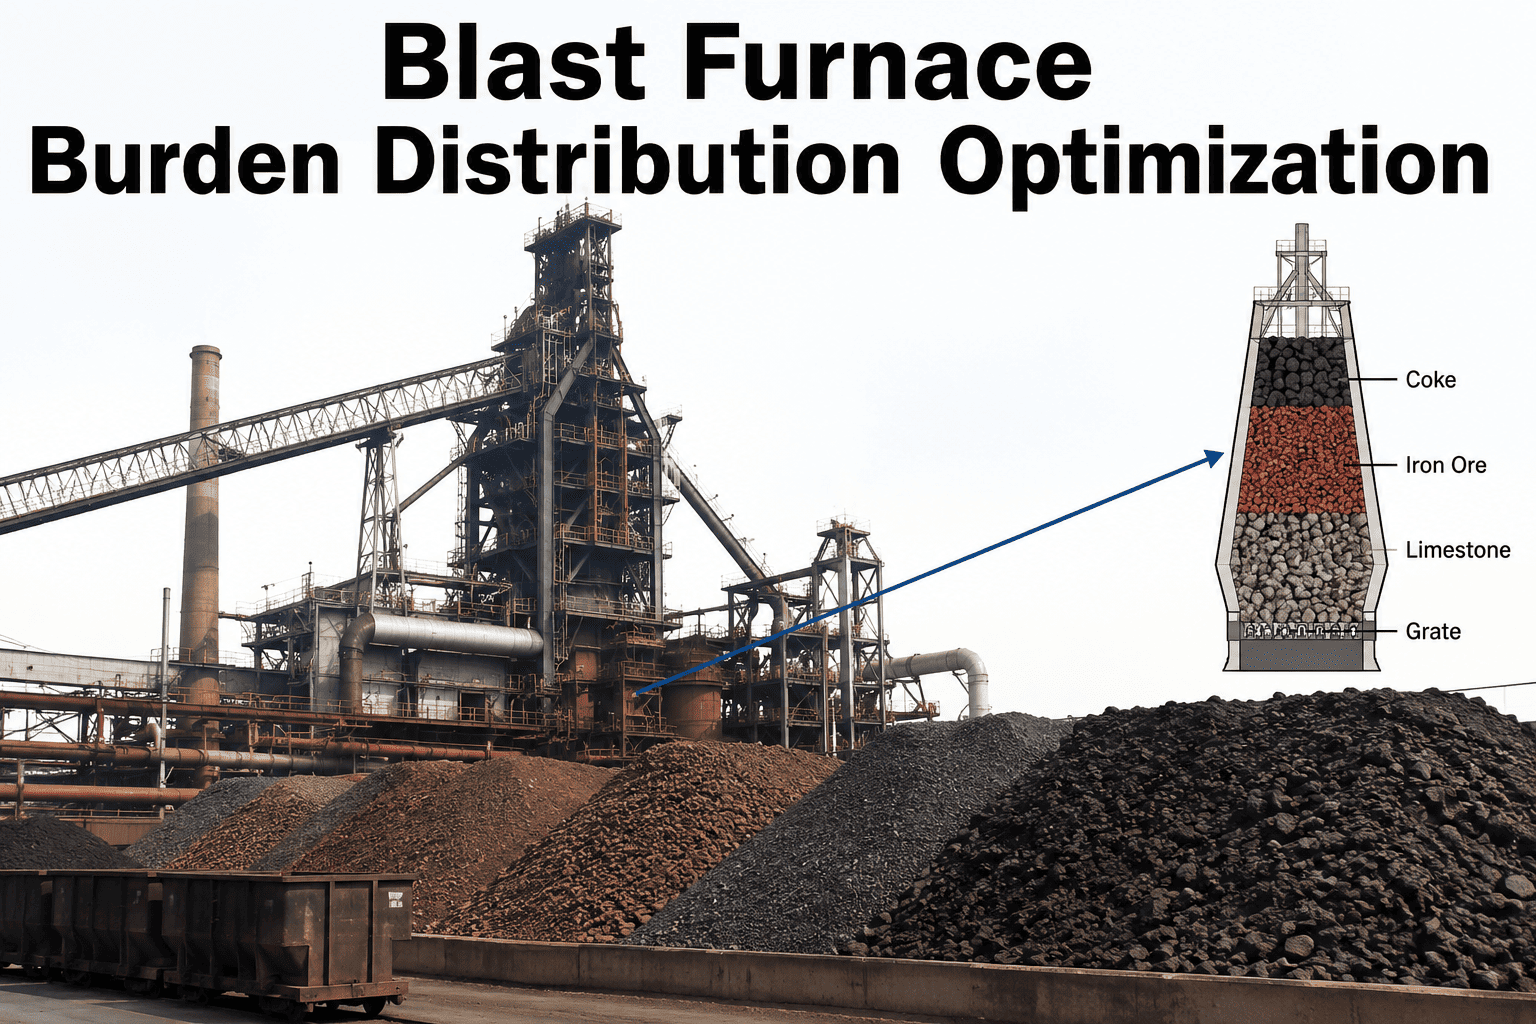
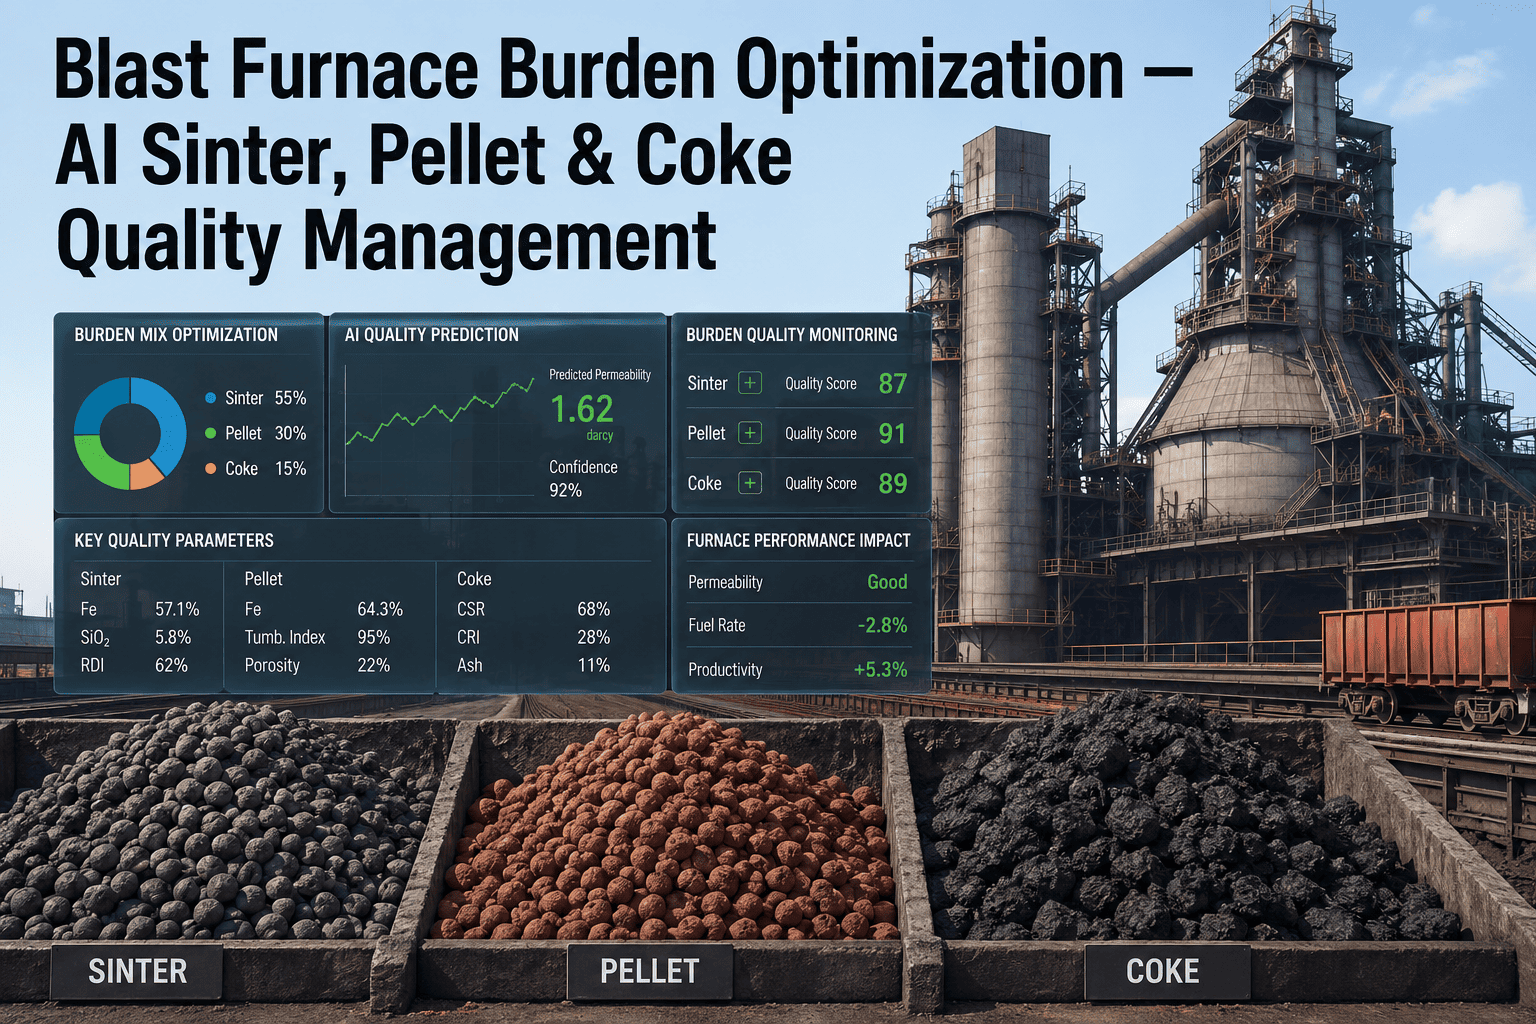
Burden Distribution
A better-controlled burden distribution, supported by improvements like top pressure and charging sequence control, directly improves gas utilization and has been a major contributor to historical productivity gains and coke rate reduction.
Hot Blast Temperature
Hot blast temperatures in the 1200 to 1300°C range have become standard in modern practice, and higher blast temperature reduces the coke needed to generate equivalent thermal energy inside the furnace.
Pulverized Coal Injection Rate
PCI rates commonly run in the 170 to 220 kilogram per ton range in current practice, with some furnaces pushing toward 250 kg/tHM, directly substituting for coke as both a reducing agent and heat source.
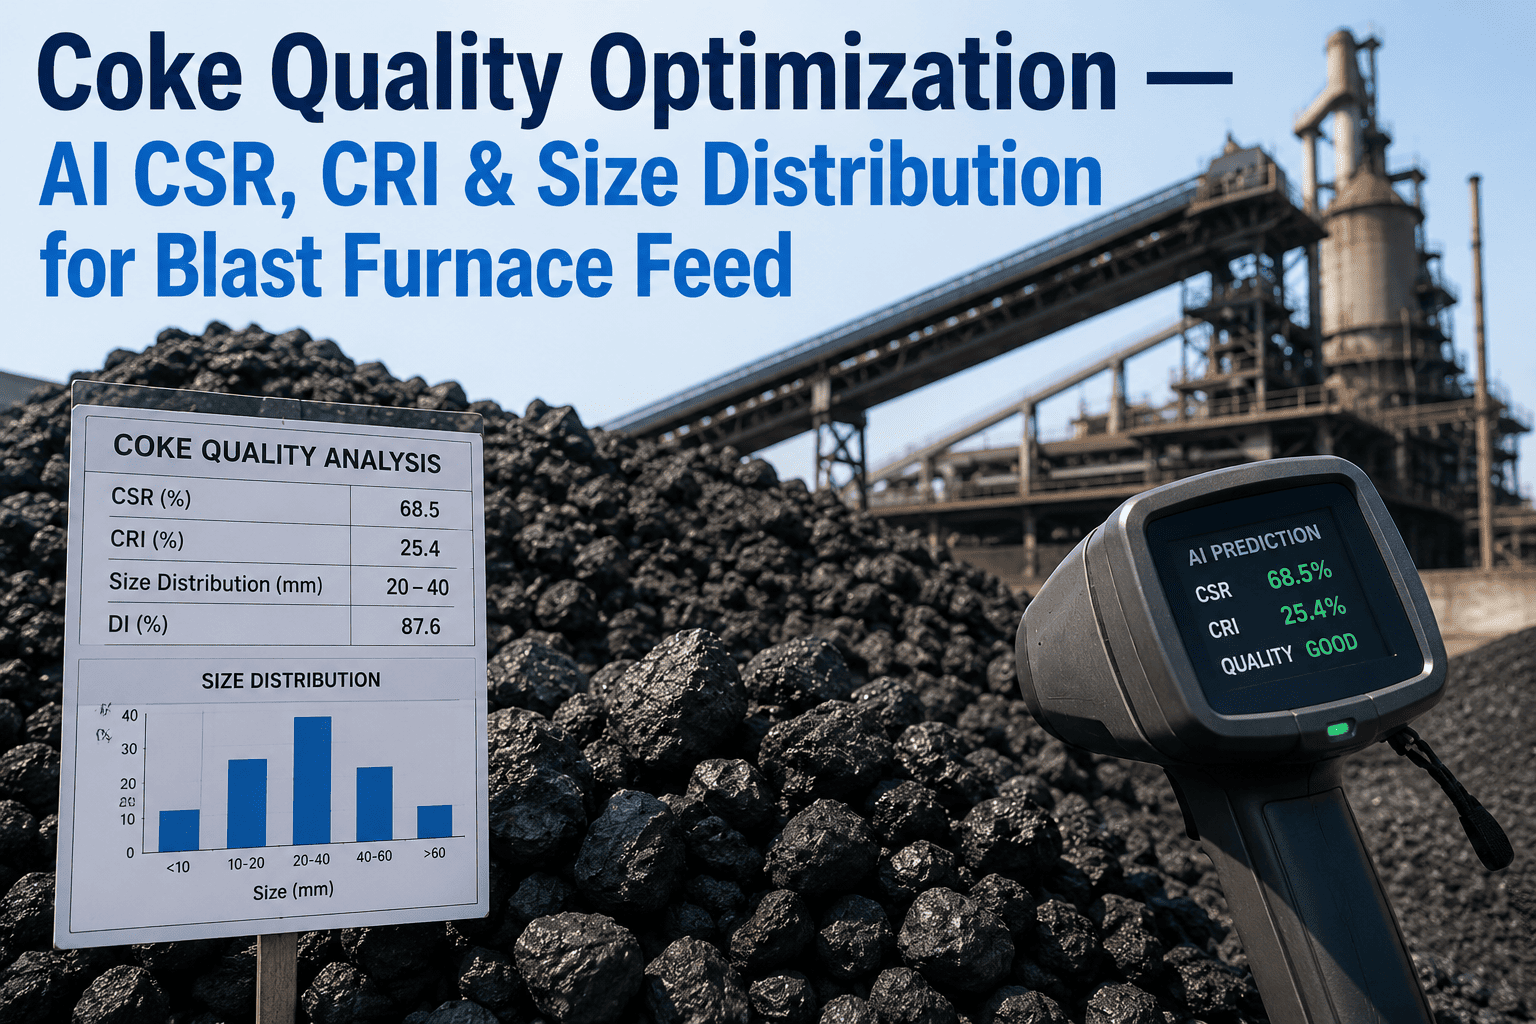
Coke Quality
Lower sulphur content in coke has been shown to improve blast furnace productivity meaningfully, since impurities like sulphur, ash, and moisture reduce the effective fuel and structural value of every kilogram of coke charged.
Coke Rate Has Been Falling For Decades — Here's What Actually Drove It
The decline from roughly 500 kilograms of coke per ton of hot metal down toward today's 286 to 320 kilogram range did not happen at a single point in time. It happened through a sequence of overlapping improvements, and understanding that sequence is useful because it shows which levers still have room to move further on a given furnace and which ones have largely reached their practical limit.
Burden And Distribution Control
Better sinter and pellet quality combined with improved burden distribution and top pressure control drove the earliest major gains in furnace productivity and coke consumption.
Hot Blast Temperature Increases
Pushing hot blast temperature toward the 1200 to 1300°C range further reduced the coke needed per ton by supplying more thermal energy directly through the blast itself.
Pulverized Coal Injection Adoption
PCI injection allowed coke rate to fall from around 500 down toward 250 kilograms per ton hot metal in demonstrated practice, becoming the single largest lever in modern coke rate reduction.
Auxiliary Fuel And Alternative Reducing Agents
Natural gas, coke oven gas, and increasingly hydrogen-based reducing agents are being explored to push coke rate even lower, though coke retains an irreplaceable structural role as the permeable support layer inside the furnace.
Your Coke Rate Trend Deserves The Same Scrutiny As Your Production Numbers
iFactory tracks coke rate, PCI rate, hot blast conditions, and burden data together heat by heat, so a drifting fuel rate gets caught early instead of surfacing only in the monthly cost report.
More PCI Doesn't Always Mean Proportionally Less Coke
It is tempting to assume that increasing pulverized coal injection produces a straight-line reduction in coke consumption, but the relationship is not linear across the full injection range. The replacement ratio, how many kilograms of coke are saved per kilogram of coal injected, tends to decline at higher injection rates, meaning the easy gains come first and the marginal gains get progressively smaller as PCI rate climbs.
This has a direct practical implication for furnace operators chasing coke rate targets: pushing PCI rate aggressively past the point where the replacement ratio has already flattened produces diminishing fuel savings while introducing operational complications, including gas permeability changes and raceway conditions that need to be actively managed. The furnaces getting the most value from PCI are generally the ones tracking replacement ratio as its own metric rather than simply maximizing injection volume and assuming coke savings will follow proportionally.
Coke Rate And PCI Benchmarks Worth Comparing Your Furnace Against
The figures below reflect commonly cited ranges from blast furnace operating literature and technical reviews, giving a reference point for where a modern, well-run furnace typically sits on coke rate and injection metrics.
| Metric | Typical Modern Range | Older Practice Comparison |
|---|---|---|
| Coke rate | 286-320 kg/tHM | ~500 kg/tHM |
| PCI rate | 170-220 kg/tHM | Minimal to none |
| Hot blast temperature | 1200-1300°C | Lower, furnace-specific |
| Demonstrated coke rate floor with high PCI | As low as ~250 kg/tHM | Not achievable without PCI |
A Practical Sequence For Reviewing Coke Rate Improvement Opportunities
Rather than attempting to optimize burden distribution, hot blast temperature, and PCI rate simultaneously, a sequential review tends to produce clearer, more attributable results. Start by comparing your furnace's current coke rate and PCI rate against the modern practice ranges above to identify the largest gap. If PCI rate is well below 170 kg/tHM, injection capacity is often the first lever worth reviewing, since it typically offers the largest single opportunity. If PCI rate is already in range but coke rate remains elevated, burden distribution and coke quality become the more likely areas to investigate, since injection alone cannot compensate for poor gas utilization or high-impurity coke. Reviewing hot blast temperature capability comes last in most cases, since it usually requires the most significant capital consideration relative to the other three levers.
Common Questions On Blast Furnace Coke Rate Optimization
Find The Specific Lever Still Costing You Coke
iFactory connects burden, injection, hot blast, and coke rate data into one view, so you can see exactly which lever is holding your furnace back from modern practice benchmarks. Book a demo to see your own furnace's fuel rate breakdown.