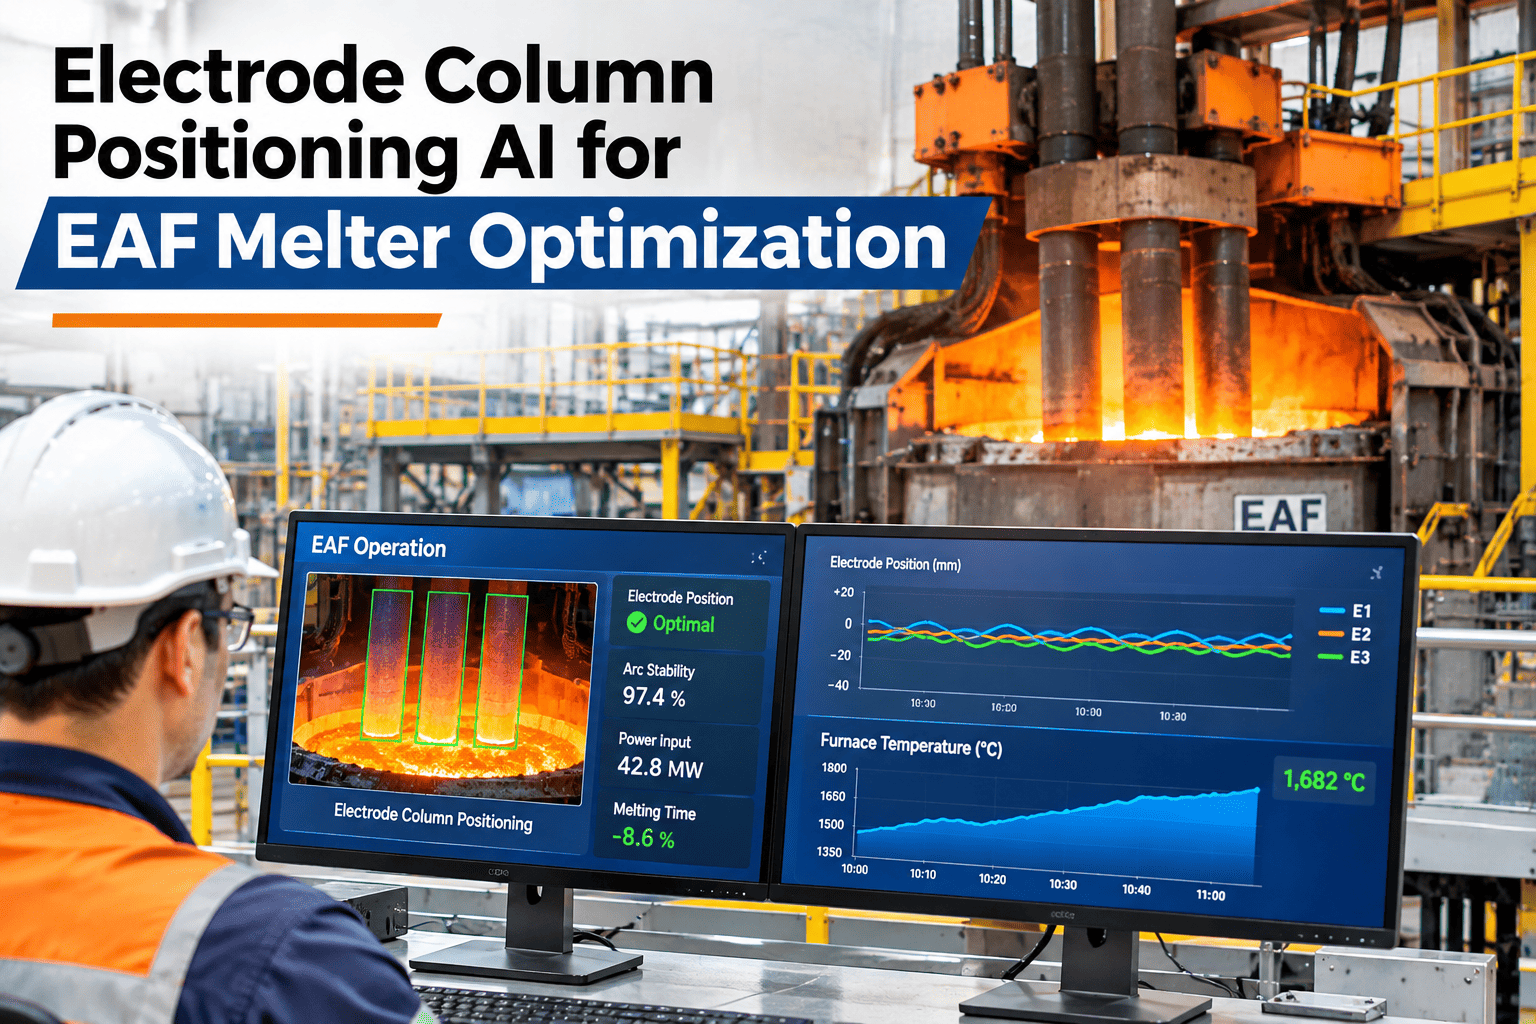
Electrode position inside an EAF affects far more than just arc stability. A column riding too close to the side wall accelerates refractory wear, a tip sitting at the wrong proximity to the bath wastes energy, and a column that drifts out of vertical alignment stresses the entire electrode holding system. Most of these effects build up slowly enough that operators do not notice until the melter is already paying for it in electrode consumption and refractory life, and our team can walk you through how continuous position analytics catches this earlier.
Electric arc furnace, melter optimization
Track Electrode Column Position Before It Costs You Consumption and Refractory Life
iFactory AI tracks column-tip proximity, side-wall exposure and vertical alignment continuously, surfacing the drift that quietly drives up electrode and refractory cost.
Why position drift is missed
Small Position Errors Compound Before Anyone Notices
A few degrees of tilt or a few inches of lateral drift do not trigger an alarm on their own, but sustained across thousands of heats, they translate directly into higher electrode consumption and faster refractory wear.
Small deviation
A few degrees of tilt look harmless on any single heat
No alarm triggers
Position stays within normal operating range
Cost compounds silently
Wear and consumption rise heat after heat
Discovered at budget review
The cost only becomes visible months later
Three position metrics
What Column Positioning Analytics Actually Tracks
Column-tip proximity
How close the electrode tip sits to the bath, affecting arc efficiency and energy use.
Side-wall exposure
How close the column runs to refractory walls, a direct driver of localized wear.
Vertical alignment
How straight the column runs, affecting mechanical stress on the holding system.
See Your Own Column Position Data
Share your current electrode consumption and refractory wear trends and see what position analytics would reveal.
Position-to-cost table
How Each Position Metric Connects to Cost
| Position issue | Direct effect | Cost driver |
|---|
| Tip too close to bath | Reduced arc stability | Higher energy use per heat |
| Tip too far from bath | Weaker, less efficient arc | Longer melt time |
| Column near side wall | Localized refractory heat load | Accelerated refractory wear |
| Vertical misalignment | Uneven mechanical load | Faster wear on holding arms and electrode |
Monitoring pipeline
Four Steps From Position Data to Operator Action
1
Track continuously
Column position is monitored throughout every heat, not sampled periodically.
2
Compare against optimal range
Position is checked against the proximity and alignment targets for the furnace.
3
Flag sustained drift
A trend outside the optimal range over multiple heats is surfaced, not just a one-off reading.
4
Guide correction
Operators get a clear signal of what to adjust and by how much.
Where drift concentrates
Position Drift Risk Across the Heat Cycle
Column position is not equally stable throughout a heat. Certain phases carry more risk of drift than others.
Bore-in phaseElevated
Flat bath meltingLow
Refining phaseModerate
Electrode changeoutHigh
Electrode changeout and bore-in are the phases most likely to introduce alignment error, since both involve physical adjustment of the column. To track this against your own heat cycle, ask our team about phase-level position tracking.
Common pitfalls
Three Problems With Manual Position Checks
1
Checked only during scheduled maintenance
Drift that develops between checks goes unnoticed for weeks.
2
No baseline for "optimal" position
Without a defined target range, a drift has nothing to be measured against.
3
Consumption and wear tracked separately from position
The link between a cost trend and its position cause is never made.
Expert review
Electrode and refractory cost trends are often blamed on material quality when the real driver is a slow position drift nobody was tracking. Before changing suppliers or specs, confirm the column has actually been running in its optimal range.
Watch for
Rising electrode consumption with no corresponding change in material batch or supplier.
Do next
Pilot continuous position tracking on one furnace and compare against current consumption trends.
— iFactory steel specialists
Frequently asked questions
What Melt Shops Ask About Column Positioning AI
How is column position actually measured?
Position is typically derived from existing regulator and control system data combined with additional sensing where needed, rather than requiring an entirely new measurement system from scratch.
Ask about your current control data.
Can this reduce electrode consumption measurably?
Keeping column position within its optimal range addresses one of several drivers of electrode consumption, so the measurable impact depends on how much drift was previously going uncorrected on your furnace.
Discuss your consumption trends.
Does this help extend refractory life too?
Reducing sustained side-wall exposure addresses one source of localized refractory wear, which can contribute to longer refractory life alongside other wear factors already in play.
Talk through your refractory wear patterns.
What counts as "sustained" drift versus normal variation?
A single heat with position outside the target range is usually normal variation, while a trend holding outside that range across multiple consecutive heats is what the system is designed to flag as worth investigating.
Ask about drift thresholds.
Does this work across multiple furnaces with different configurations?
Yes, optimal position ranges are typically set per furnace based on its specific geometry and operating parameters, so each furnace gets its own baseline rather than a shared generic target.
Discuss your furnace fleet.
From silent drift to tracked position
Stop Paying for Electrode Drift You Cannot See
Book a session with iFactory AI to review your furnace data and see how column positioning analytics fits your melt shop.