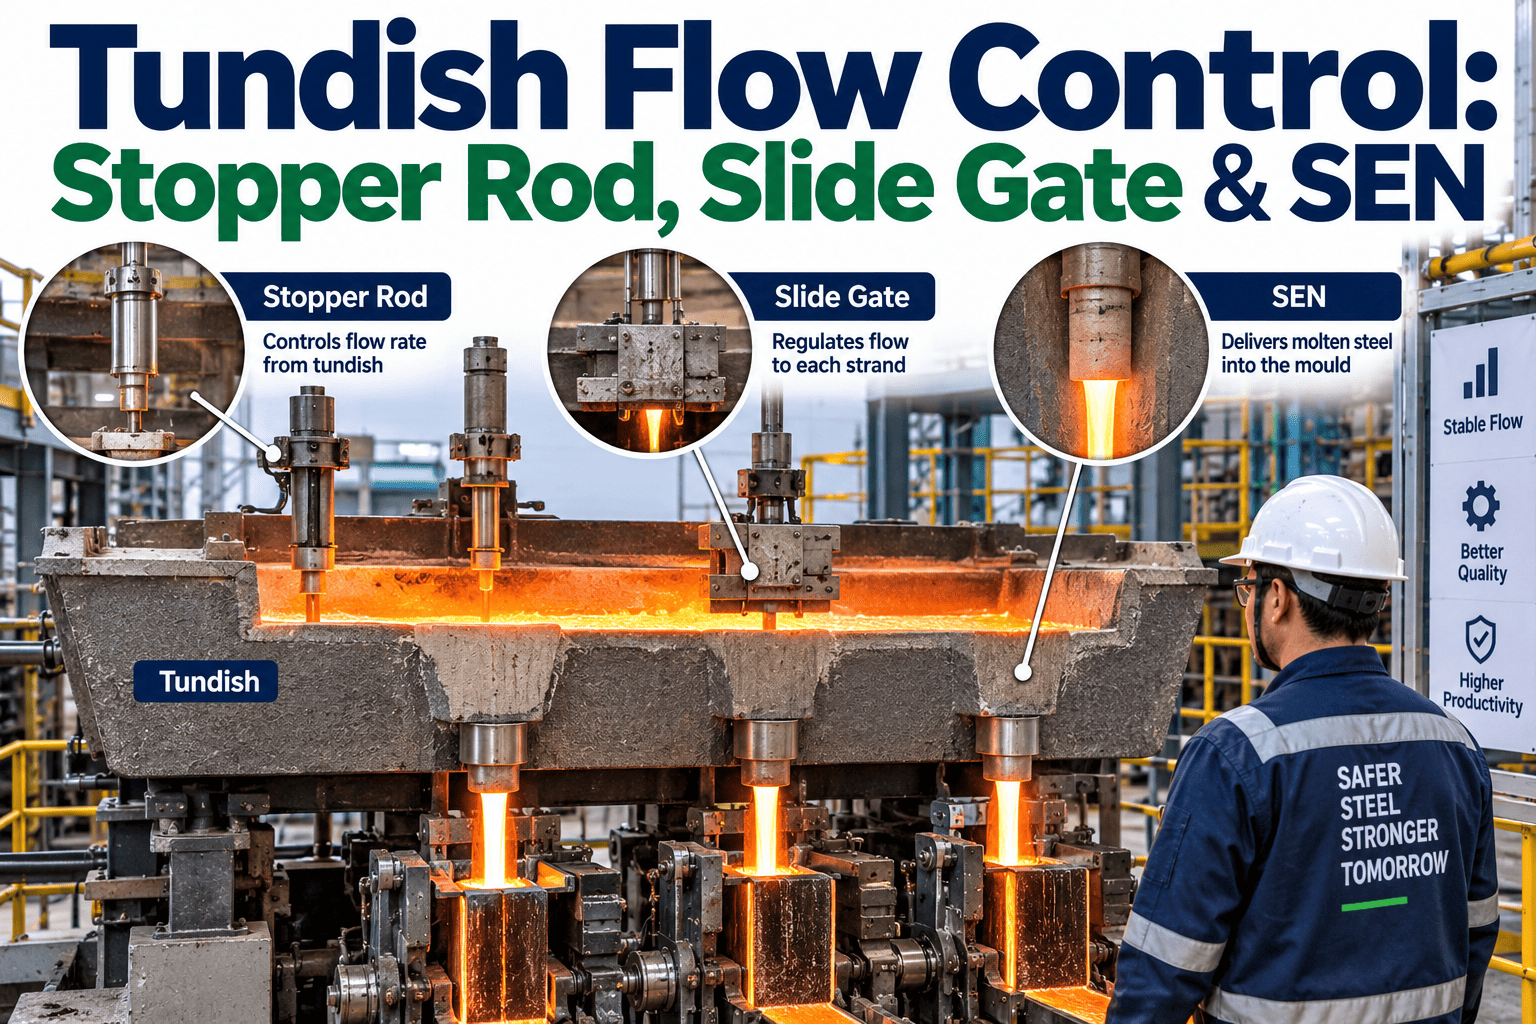
A slide gate failure during teeming is one of the few events on a steel plant floor that turns a routine heat into an emergency in seconds, because there is no pause button on a ladle full of liquid steel. Most gate failures are not sudden at all, they are the visible end point of a plate refractory or hydraulic issue that had been building for days or weeks and simply went unnoticed until the gate could no longer hold or control flow. A maintenance approach built around scheduled inspection points and known wear signs catches that build-up long before it becomes a floor incident, which is a far cheaper place to catch it than at the moment of tap. If your current gate maintenance still relies mainly on catching problems after they show up in a heat, it is worth comparing that against a condition-based schedule — see how that comparison looks for your ladle fleet.
SECONDARY METALLURGY · LADLE SLIDE GATE · MAINTENANCE
Keep Flow Control Reliable Before the Gate Becomes the Incident
A ladle slide gate is only as reliable as its plate refractory condition and hydraulic mechanism on the day it is asked to perform, and both degrade in ways that a scheduled inspection catches well before an operator ever sees a problem at tap.
The Slide Gate System, Part by Part
01
Upper Plate
Fixed against the collector nozzle, taking the direct thermal and erosive load from the first contact with liquid steel.
02
Lower Plate
Slides against the upper plate to open, throttle, or close the flow path, and carries most of the mechanical wear from repeated movement.
03
Hydraulic Cylinder and Actuator
Drives the lower plate's position with enough force and precision to hold a partial-open throttle setting steadily, not just fully open or closed.
04
Frame and Spring Package
Holds plate-to-plate contact pressure consistent as the plates heat, cool, and wear, which is easy to overlook until contact pressure is already uneven.
05
Collector Nozzle and Well Block
Sits above the upper plate and directs flow into the gate assembly, wearing on its own timeline that does not always match the plates beneath it.
WHY IT MATTERS
What a Gate Problem Actually Costs When It Shows Up Mid-Heat
A slide gate issue rarely stays contained to the gate itself once it shows up during teeming, because everything downstream of the ladle is timed against a flow rate that gate reliably controls.
Uncontrolled Flow Rate
A gate that cannot throttle precisely sends steel to the mold or tundish faster or slower than the process was set up to handle.
Emergency Ladle Change
A gate that cannot close reliably can force an unplanned ladle swap, disrupting the entire sequence behind it.
Safety Exposure on the Floor
Any loss of flow control near a ladle full of liquid steel is a direct safety event, not just a production one.
Refractory and Plate Cost
A plate pushed past its safe wear point is often damaged badly enough that it cannot be reused, turning a maintenance item into a scrap cost.
None of these outcomes require a dramatic failure to happen, a gate that is simply a little less precise than it should be is enough to start showing up as inconsistent casting speed long before anyone calls it a maintenance issue.
PLATE WEAR STAGES
Reading Plate Condition Before It Becomes a Flow Problem
Plate refractory wears in a fairly predictable progression, and knowing which stage a plate is in is what separates a planned changeout from a surprise one.
| Wear Stage |
What to Look For |
Recommended Action |
| Stage 1 — Early Surface Wear |
Light surface erosion visible at the contact face, flow control still precise |
Log condition, continue on standard rotation |
| Stage 2 — Moderate Groove Formation |
Visible grooving along the flow path, minor throttle drift under partial-open settings |
Schedule changeout within the next planned window |
| Stage 3 — Advanced Erosion |
Deep grooving, noticeable flow inconsistency, contact pressure harder to hold evenly |
Prioritize changeout before the next heat on this ladle |
| Stage 4 — Critical Wear |
Near breakthrough risk, flow control unreliable at any throttle position |
Remove from service immediately, do not tap |
Most plants catch stage 3 and stage 4 conditions today because they are hard to miss, the real value in a structured inspection cadence is catching stage 2 consistently, since that is where a changeout is still fully planned rather than reactive.
Get a gate reliability review before your next scheduled reline
iFactory can walk your maintenance team through condition-based inspection points mapped to your current plate rotation and gate fleet.
HYDRAULIC MECHANISM
The Mechanism Fails Quietly Long Before It Fails Visibly
Plate condition gets most of the attention because it is easier to inspect visually, but a hydraulic mechanism issue is just as likely to cause a flow control failure and considerably easier to miss during a routine walk-down.
CHK
Cylinder Response Time
A cylinder that responds slower than its baseline is often the earliest sign of internal seal wear, well before any visible leak appears.
CHK
Throttle Position Accuracy
The actual plate position should match the commanded position within a tight tolerance, and drift here signals mechanical wear even when the plate itself looks fine.
CHK
Spring Package Tension
Contact pressure between plates depends on spring tension holding steady, and a package that has relaxed over time reduces sealing pressure without any obvious visual cue.
CHK
Hydraulic Fluid Condition
Contaminated or degraded fluid accelerates wear across the entire actuation system, making fluid condition one of the highest-leverage checks on the list.
The common thread across all four of these is that none of them announce themselves the way a cracked plate does, which is exactly why a mechanism-specific inspection point belongs on the same schedule as the refractory check rather than being treated as a separate, lower-priority task.
INSPECTION CADENCE
Building an Inspection Schedule That Actually Gets Followed
An inspection schedule only works if it is specific enough that a crew can follow it consistently, rather than a general reminder to "check the gate" that gets interpreted differently by every shift.
EVERY HEAT
Visual Flow Check During Teeming
Operator watches for flow inconsistency or throttle lag during actual use, the earliest possible signal available.
DAILY
Cylinder Response and Fluid Level Check
A quick mechanical check that catches early hydraulic drift before it affects flow control during a heat.
WEEKLY
Plate Wear Stage Assessment
A closer inspection against the wear stage reference to plan changeouts before they become urgent.
CAMPAIGN END
Full Mechanism Teardown Check
Spring package tension, seal condition, and frame alignment reviewed together at a natural maintenance window.
RECORDKEEPING
Why the Same Gate Failure Keeps Coming Back on Some Plants
A surprising number of repeat gate failures trace back not to a maintenance gap but to a recordkeeping gap, where the inspection happened but the result never made it into a record anyone could check before the next heat on that ladle.
Plate Serial Tied to Ladle History
Each plate's wear record follows the specific ladle and gate it was installed on, not a generic plant-wide log.
Inspection Result, Not Just Inspection Done
A record that shows what the wear stage actually was, not just a checkbox confirming someone looked.
Visible Across Shifts
The next crew can see what the previous shift found, closing the handoff gap where a known issue quietly falls through.
Failure Root Cause Logged
When a gate does fail, the record captures whether it was plate wear, mechanism drift, or something else, so the same root cause does not repeat unnoticed.
None of this requires a complex system to start, it requires the inspection result to land somewhere the next shift and the next maintenance planner can both actually see, which is where a surprising number of plants still fall short today.
DATA-DRIVEN MONITORING
What Condition Monitoring Adds on Top of the Manual Checklist
A well-run manual checklist catches most gate issues, but it depends entirely on the checklist being followed exactly the same way by every crew, every time, which is a hard standard to hold across a full year of shifts.
24/7
Continuous cylinder response tracking instead of once-a-shift spot checks
Trend
Wear stage progression tracked plate by plate instead of judged fresh at each inspection
Alert
Flagged automatically the moment a reading drifts outside its normal range for that gate
iFactory's monitoring layer sits alongside the existing manual checklist rather than replacing it, giving the maintenance team a continuous record to check the manual inspection against instead of relying on the checklist alone to catch everything between scheduled checks.
FREQUENTLY ASKED QUESTIONS
What Maintenance Teams Ask About Slide Gate Reliability
How often should plates actually be changed if they still look usable?
Plate life depends on grade mix, steel cleanliness, and number of heats rather than a single fixed number that applies everywhere, which is why a wear-stage assessment matters more than a calendar date. A plate that reaches stage 2 grooving should be scheduled for changeout on the next planned window rather than pushed further just because it has not yet failed.
Set up a wear-based rotation schedule for your specific plate grades.
Can a hydraulic mechanism issue cause problems even with a brand new plate installed?
Yes, and this is one of the more common troubleshooting mistakes, since a fresh plate with a worn mechanism underneath it can still produce inconsistent throttle control that looks like a plate problem at first glance. Checking cylinder response and spring tension alongside any plate changeout avoids chasing the wrong root cause.
Have our team review your current mechanism inspection points.
What is the earliest reliable sign that a gate is heading toward a mid-heat failure?
Throttle position drift, where the actual plate position no longer matches the commanded position within tolerance, tends to show up before any visible refractory damage and before an operator would notice a flow change by eye. Continuous monitoring of that specific signal is one of the highest-value early warnings available on a gate system.
See how that signal gets tracked in practice.
Does condition monitoring require replacing our current manual inspection checklist?
No, monitoring is designed to run alongside the manual checklist rather than replace it, since the checklist still captures things a sensor does not, such as visible refractory condition during a physical walk-down. The two work best together, with monitoring catching drift between inspections and the checklist confirming physical condition at each scheduled check.
Ask our team how the two are typically combined.
Is this approach practical for a plant with an older gate fleet rather than newer equipment?
Yes, condition monitoring is added onto existing gate hardware rather than requiring newer equipment, since the sensors track cylinder response, position, and related signals that are present on most standard slide gate systems already in service. Older fleets are frequently where the earliest warning value matters most, given the accumulated wear already present.
Check compatibility with your current gate fleet.
CATCH GATE WEAR BEFORE IT REACHES THE FLOOR
Build a Slide Gate Maintenance Program That Catches Stage 2, Not Just Stage 4
iFactory helps maintenance teams combine wear-stage tracking, mechanism monitoring, and a realistic inspection cadence so gate issues get caught on a planned schedule instead of mid-heat.