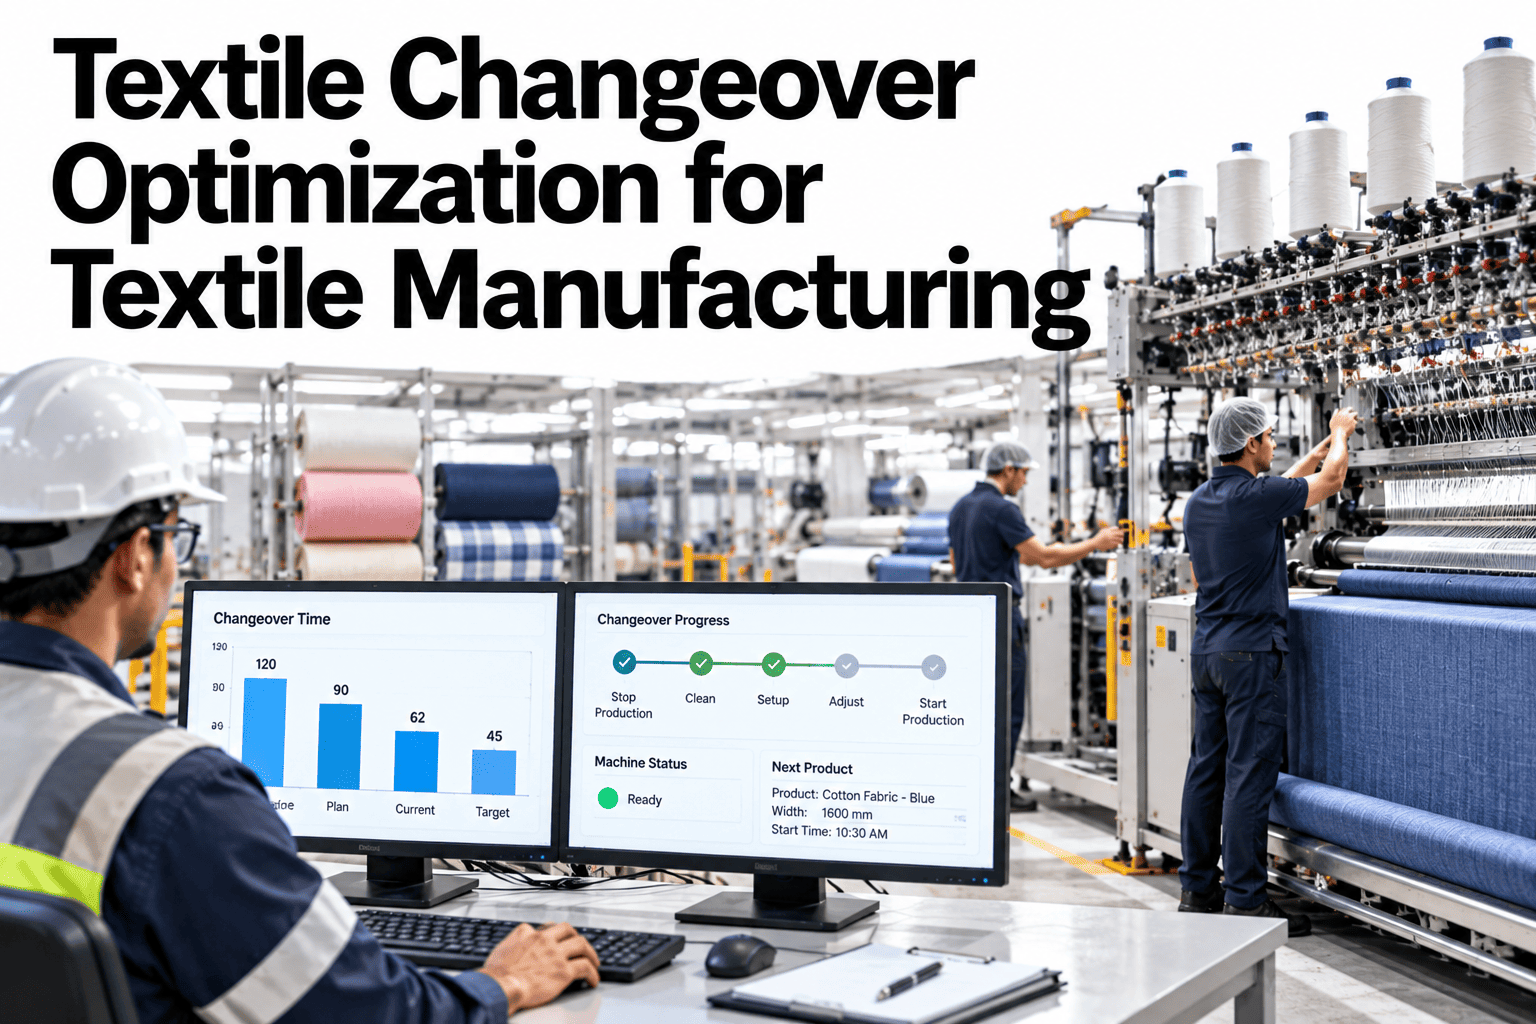
In a mill with many short runs, the machines spend a surprising share of the day not producing. Style changes on looms, count changes in spinning, colour changes in dyeing and screen changes in printing all stop output, and each one tends to take longer than its standard. Changeover optimisation does not ask people to work faster. It reorganises the work so more of it happens while the machine is still running. Mills that want to measure and shrink setup time can ask iFactory AI how changeovers are timed and analysed by style.
Shrink Setup Time Between Styles Without Rushing Anyone
iFactory AI times every changeover by machine and style, separates the work that must stop the machine from the work that does not, and shows which changes to attack first.
Where Changeovers Hurt Across a Textile Plant
Every department has its own changeover. The table shows typical examples and what usually makes them slow.
| Department | Typical Changeover | What Usually Makes It Slow |
|---|---|---|
| Spinning | Count or blend change on a frame | Gear and setting changes, cleaning, waiting for material |
| Weaving | Style change and warp tie-in or drawing-in | Beam handling, searching for parts, setup trials |
| Knitting | Pattern or yarn change on a machine | Needle and cam changes, yarn preparation |
| Dyeing | Colour or recipe change | Cleaning between colours, waiting for chemicals |
| Printing | Design and screen change | Screen preparation, colour matching, registration setup |
The Core Idea: Internal and External Work
Changeover work falls into two groups. Moving work from the first group to the second is the heart of the method.
Where the Changeover Minutes Go
Time disappears in a few places. The chart shows an illustrative breakdown for a typical style change.
Find Out How Many Hours Your Style Changes Really Take
Book a 30-minute session and iFactory AI will review your changeover records and schedules to show where setup time hides and which styles cost the most.
A Five-Step Path to Faster Changeovers
The method works in textiles as in any other industry. These steps keep it simple.
Sequencing: The Free Gain Before Any Tooling
The order of styles changes how much setup is needed. Good sequencing reduces work before anyone touches a tool.
Light to dark in dyeing
Running lighter shades before darker ones reduces cleaning between lots.
Group similar counts
Running similar counts together reduces gear and setting changes.
Group similar widths and constructions
Looms and knitting machines change less when neighbouring styles are alike.
Cluster by customer or finish
Shared finishes and recipes cut preparation and cleaning.
Sequence and Setup Cost: An Illustration
Sequencing can change total setup time significantly. The matrix, shown as an illustration, ranks typical sequence effects by department.
| Department | Sequencing Benefit | Effort to Plan |
|---|---|---|
| Dyeing | High | Moderate |
| Spinning | High | Moderate |
| Weaving | Moderate | Moderate |
| Knitting | Moderate | Low |
| Printing | Moderate | High |
Changeover Preparation Checklist
Use this list before every changeover. Each box moves work from inside the stop to outside it.
A Composite Scenario: The Style Change That Lost an Hour
This is a composite example, not a named mill. It shows how recording and sorting tasks shortens a changeover.
Mistakes That Stall Changeover Improvement
These habits keep changeovers long.
Rushing the crew
Speed without redesign causes errors and rework.
Improving without timing
Without a baseline, nobody can show a gain.
Ignoring sequencing
Setup that never needed to happen is the cheapest to remove.
Not recording the new standard
Gains fade when the old habits return.
What iFactory AI Adds to Changeover Optimisation
iFactory AI is smart manufacturing and industrial software for textile operations. Explore changeover analytics in a live product tour on realistic data.
A 30-Day Plan to Start
A month is enough to improve one changeover and prove the method.
Review of Textile Changeover Optimisation
A practical review of what makes changeover improvement last, written as editorial guidance rather than a named expert quote.
Time before you improve
Without a baseline, an improvement cannot be shown or defended.
Move work outside the stop
Preparing in advance is the biggest single gain.
Sequence first
Removing a changeover is better than shortening it.
Frequently Asked Questions
What is changeover optimisation in textile manufacturing?
It is reducing the machine stopped time between styles by moving preparation outside the stop and standardising the rest. See a changeover timed and broken down in a live demo with realistic data. It does not rely on working faster.
Which changeovers should we improve first?
Start with the most frequent change on the most expensive machine, since small savings repeat many times. Ranking by total stopped time per month finds it quickly. One clear win builds momentum.
Is sequencing really that important?
Often yes, because the order of styles changes how much cleaning and setting is needed. Ask support how schedule sequences are compared for setup time in your plan. Sequencing must still respect delivery dates.
Do we need new equipment?
Usually not at first. Kitting, staging and standard work deliver much of the gain. Equipment changes can follow where timing shows a clear need.
How soon can we see results?
Many mills shorten a first changeover within a month. Book time to scope a changeover pilot with your production team. Timing data makes the saving visible.
Give Your Machines Back the Hours Lost Between Styles
iFactory AI times every changeover and shows which tasks to move outside the stop. Book a walkthrough to see it on your own styles and machines.