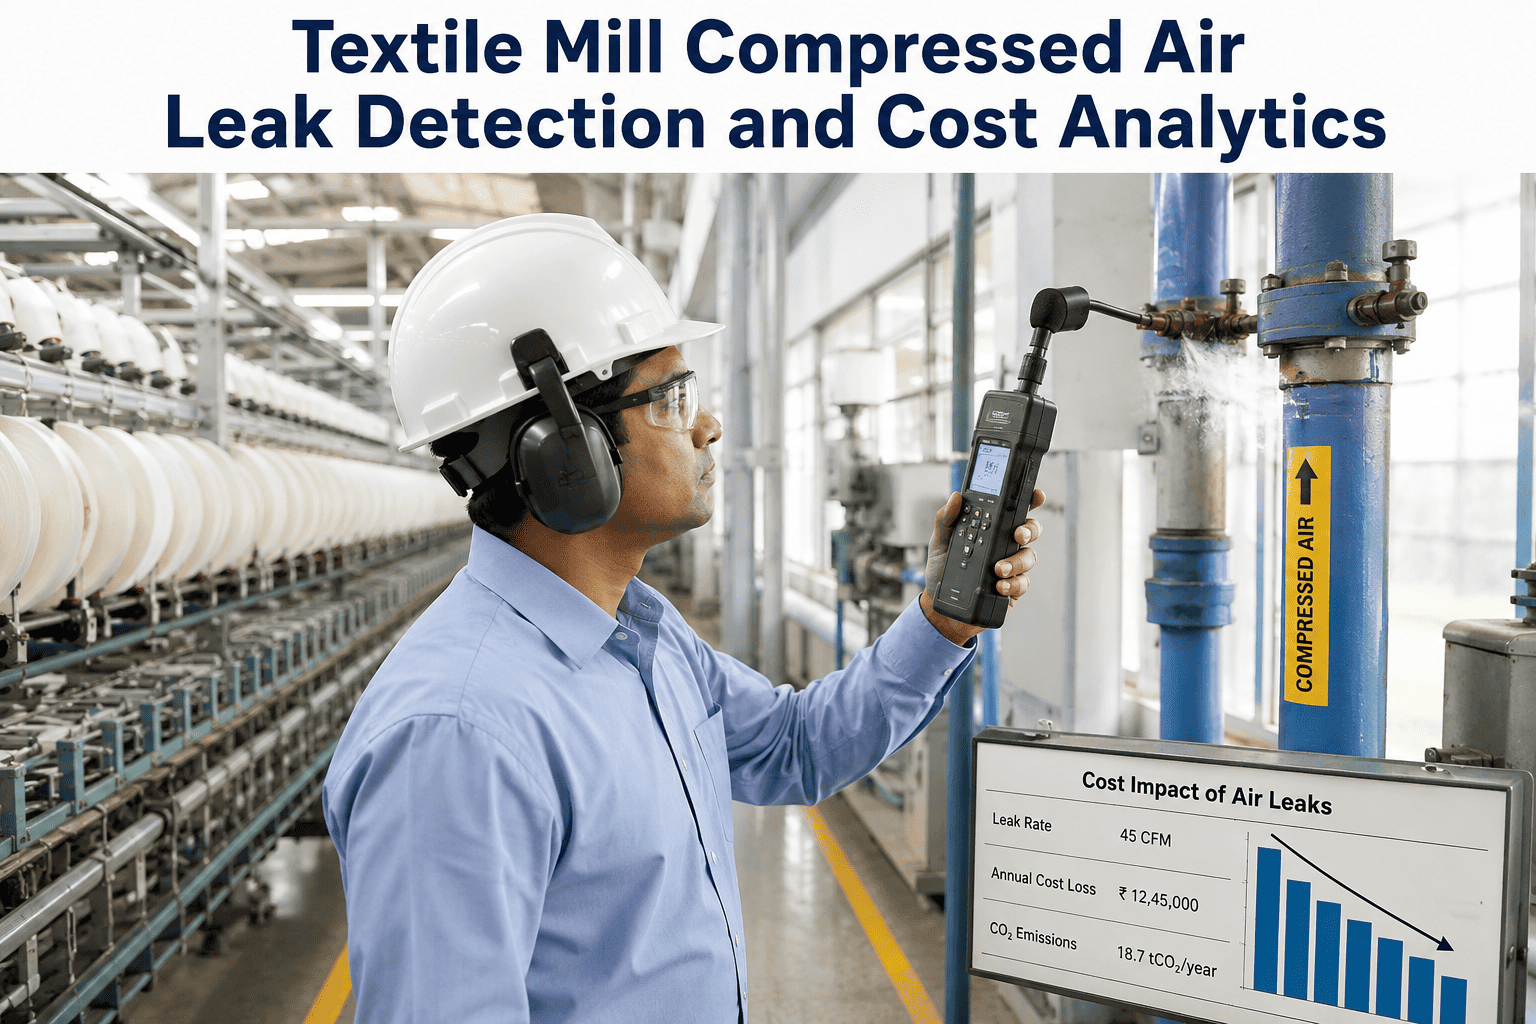
Compressed air is the most expensive utility in a textile mill that nobody reads a meter for. Looms, winders, cleaners and blow-off guns all run on it, and every hissing joint on the floor is paid for by a compressor motor. Finding those leaks is easier when flow and pressure are logged against production. Plants setting up that discipline can ask iFactory AI how leak tracking fits a mill.
Textile Compressed Air Leak Detection: Flow, Pressure and Cost per Leak
Measure what your compressors really deliver, find where it goes and rank repairs by rupee or dollar value. iFactory AI keeps the flow, pressure and energy picture in one place for textile plants.
Why Textile Mills Leak More Than They Think
Few industries use compressed air in as many places as textiles. Air-jet looms carry weft across the shed with it, spinning and winding lines clean with it, and operators blow lint off machines with it all shift. More points of use means more joints, hoses and couplings that can slowly fail.
Many small points
Each loom has its own feed, filter and regulator. A worn coupling on one is minor, but a hall of looms multiplies it.
Cleaners and blowers
Suction and blow-off points run through the shift, and hoses get dragged, bent and cut.
Headers and dryers
Long pipe runs, condensate traps and dryer purge lines leak quietly, often far from anyone's attention.
Fibre2Fashion, in a 2016 article by Ashok Sethuraman, goes further. The author says mills are losing more than 30 percent of their compressed air to leakage, and that some record more than 50 percent. These are one practitioner's observations rather than a survey, but they match what energy audits often find: the leak share is higher than the plant assumes.
What a Single Leak Costs
Leaks are measured by the size of the hole. The US Department of Energy figures, as reproduced by Reliable Plant, assume a hole at 100 psig running all year at 5 cents a kWh. Annual cost grows fast with size.
Doubling the hole width multiplies the cost about four times. A quarter-inch leak costs as much as sixteen of the smallest. That is why a repair list should be ranked by size and not worked in the order the leaks were found.
Scale to your tariff
The source rate is 5 cents. If your tariff is higher, the cost rises in proportion, so use your own rate.
Pressure matters too
A higher header pressure pushes more air through the same hole, so leaks cost more at 8 bar than at 6.
Hours matter
Mills that run around the clock pay for every leak around the clock, including nights and holidays.
Flow, Pressure and Power: The Three Readings
Leak detection starts with measurement, not with a hunt. Three readings tell you how much air is made, how hard it is pushed and what it costs. Together they show whether leaks are the main problem.
| Reading | Where to Measure | What It Tells You | Common Gap |
|---|---|---|---|
| Flow | Compressor outlet and main branches | Air produced and where it goes | No flow meter on branches |
| Pressure | Compressor house, header, far ends of lines | Loss between supply and use | Only a gauge at the compressor |
| Power | Each compressor motor | kWh and kWh per cubic metre | Shared meter for all units |
| Dew point | Dryer outlet | Whether air is dry enough for looms | Checked rarely |
| Run state | Loaded, unloaded, off | Hours wasted at no load | Not logged |
The mill described by Air Best Practices followed this pattern. It fitted energy meters on each compressor and vortex flow meters on the air output, then calculated compressor efficiency in kWh per normal cubic metre. Compressed air there was about 61 percent of the facility's annual electricity, around 26 GWh costing 2.2 million dollars a year, according to the article.
Find Out How Much Air You Lose
Book a 30-minute session and iFactory AI will show how flow, pressure and power readings turn into a leak share and a ranked repair list for a textile mill.
The Baseline Test: Measure Leaks Without Finding One
You can estimate total leakage before locating a single leak. When looms and winders are stopped, any air still being produced is going to leaks, or to a few continuous uses. Compare that flow with the average flow during production.
At 29 percent this mill sits inside the 20 to 30 percent band that the DOE rule of thumb describes for neglected systems. Over 8,000 hours a year, the leak power adds up to 1,276,000 kWh, which at 9 cents a kWh is 114,840 dollars. All figures are illustrative.
Pick a quiet window
A planned stop, a Sunday or a changeover gap works, as long as all machines are truly off.
Subtract known uses
Dryer purge, process blowers or instrument air that must run should be taken off the number.
Repeat monthly
The same test each month shows whether leaks are growing back after repairs.
Ways to Find the Leaks Themselves
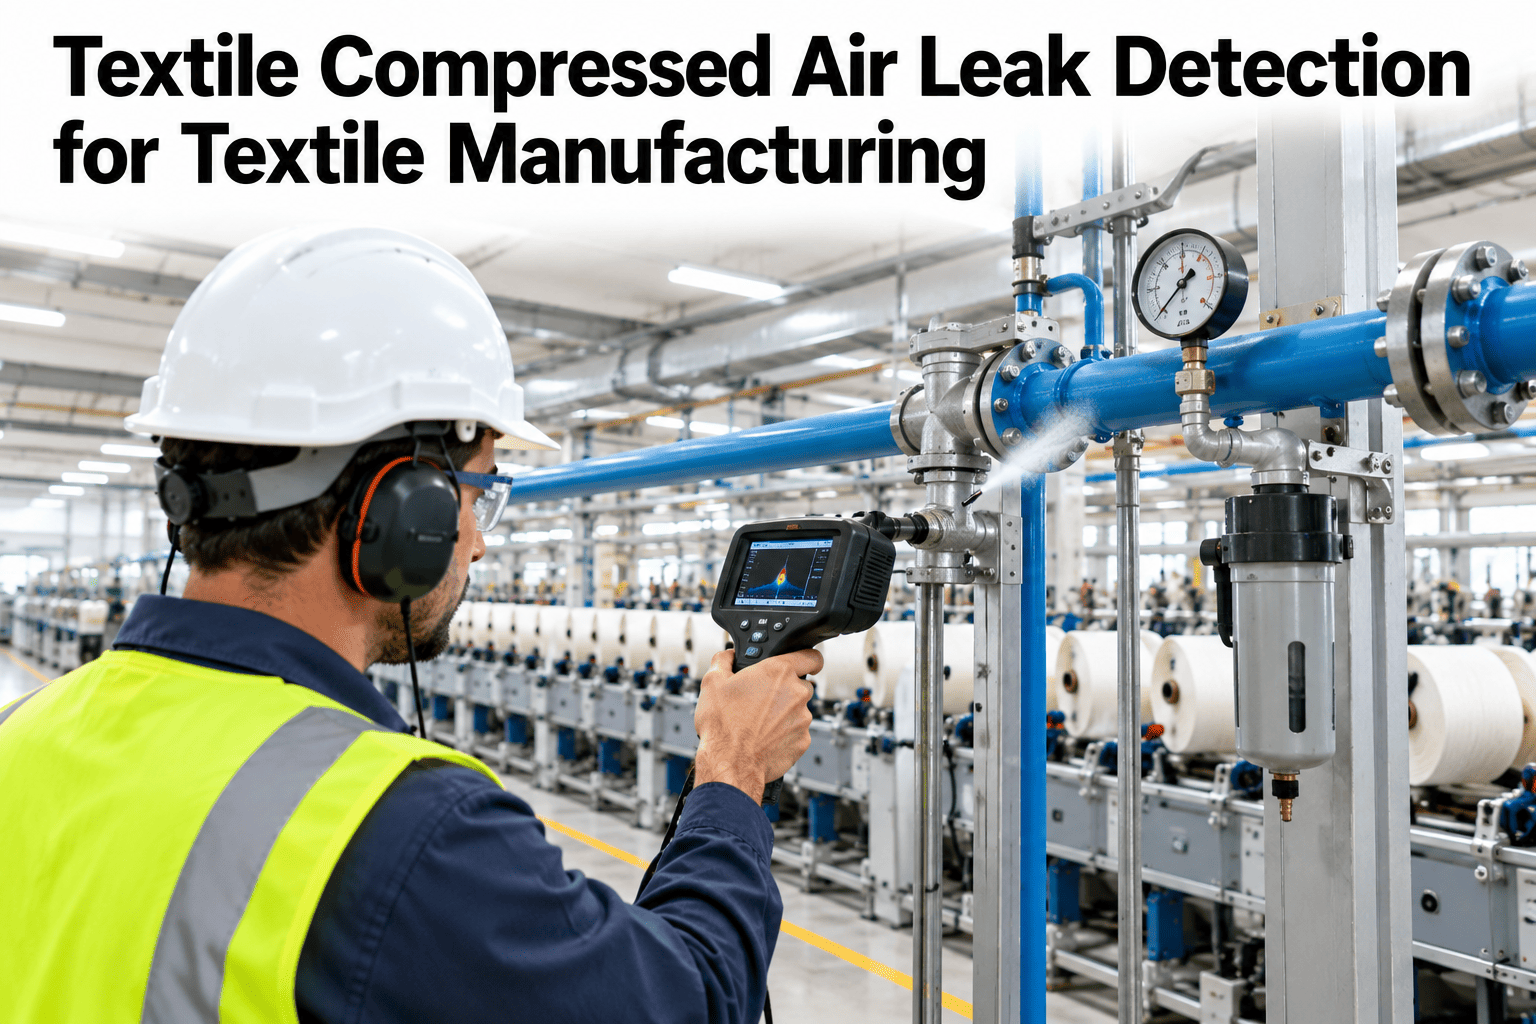
Once you know the size of the problem, you need to locate it. Several methods work, and mills often combine them. Fibre2Fashion advises fixing the audible leaks first, since they are easy to hear and the loud ones can mask quieter ones from a detector.
| Method | How It Works | Best For | Limits |
|---|---|---|---|
| Listening walk | Technicians walk the floor on a quiet shift | Large audible leaks | Misses small and noisy-area leaks |
| Soap solution | Bubbles form at the leaking joint | Confirming a suspected joint | Slow and only for reachable fittings |
| Ultrasonic detector | Picks up the high-pitched sound of escaping air | Finding leaks in noisy halls | Needs a trained operator and a route |
| Acoustic imaging | A camera shows a map of sound sources | Fast surveys across many points | Equipment cost and training |
| Flow trending | Branch meters show a creeping base flow | Spotting new leaks early | Shows the area, not the exact joint |
Reliable Plant notes that cheaper ultrasonic and acoustic-imaging tools have made leak detection more accessible than it was in the 1990s, though it does not give accuracy or cost data. Treat vendor claims about detection speed with care and test a tool in your own hall before buying.
Tag, Rank and Repair: A Leak Register
Every leak found should get a tag, a location, an estimated size and a cost. The register then becomes the repair list, ordered by value. Here is an illustrative census of 36 leaks using the size costs quoted earlier.
| Size Class | Count | Cost Each | Annual Cost | Share of Total |
|---|---|---|---|---|
| 1/4 inch | 2 | $8,382 | $16,764 | 33% |
| 1/8 inch | 10 | $2,095 | $20,950 | 42% |
| 1/16 inch | 24 | $523 | $12,552 | 25% |
| Total | 36 | $50,266 | 100% |
Twelve leaks, a third of the count, carry 75 percent of the cost. Repairing those first captures most of the value with a fraction of the work. The register mirrors the DOE worked example cited by Reliable Plant, where the ten largest of 160 leaks accounted for most of a 57,069 dollar annual loss.
Tag it
Hang a numbered tag at the leak and log the location, size and photo.
Rank it
Order by annual cost and by ease of repair, so quick wins go first.
Close it
Record the fix, retest and confirm the flow fell.
Pressure: The Lever That Shrinks Every Leak
Leaks flow harder at higher pressure, and compressors burn more power to make it. Lowering the setpoint, where the process allows, reduces both effects. The ladder shows where pressure is typically lost between the compressor and the loom.
The Air Best Practices case lowered its main header from 80 psi to 73 psi, about 7 psi. On the DOE rule of 1 percent per 2 psi, that is roughly 3.5 percent of compressor energy. In the illustrative mill above, with 550 kW of compressor power over 8,000 hours at 9 cents, 3.5 percent is about 13,860 dollars a year.
The Value of Repairing: A Worked Example
Back to the illustrative mill with a 29 percent leak share. Suppose repairs bring the leak flow from 1,450 to 500 Nm3 per hour, a leak share of 10 percent, the level Reliable Plant associates with a well-maintained system.
| Item | Before Repairs | After Repairs | Change |
|---|---|---|---|
| Leak flow, Nm3 per hour | 1,450 | 500 | -950 |
| Leak share of 5,000 | 29% | 10% | -19 points |
| Leak power, kW | 159.5 | 55.0 | -104.5 |
| Leak energy over 8,000 h, kWh | 1,276,000 | 440,000 | -836,000 |
| Annual leak cost at 9 cents | $114,840 | $39,600 | -$75,240 |
The saving of 75,240 dollars a year would come from repairs that mostly cost fittings, hoses and labour. Fibre2Fashion says a good leak program can pay back in around six months, though the author gives no audit to support it. Test the claim against your own repair cost.
What a Whole-System Program Can Deliver
Leak repair is one part of a wider compressed air program. The fabric mill in the Air Best Practices article combined several measures, and the result is a useful reference for how the pieces add up. The numbers below are as reported there.
| Measure | Reported Result |
|---|---|
| Header pressure cut from 80 to 73 psi | Lower power draw and smaller leak flows |
| Energy-saving reeds on 130 air-jet looms | About 680 cfm less flow, 20 percent saving projected |
| Overhaul of two underperforming compressors | About 10 percent better efficiency, 69,000 kWh a month saved |
| Booster replacing a separate electric compressor | About 1,500 dollars a month saved |
| Whole program | Air use down 64,800 m3 a day, 5,532,800 kWh and 468,000 dollars a year, 21 percent |
That mill was large and used compressed air for a major share of its power, so your scale will differ. The lesson is the order of work: measure, cut waste on the demand side, then match supply, and only then consider new compressors.
KPIs That Keep Leaks Under Control
Leaks come back. Hoses are moved, couplings wear and new machines are tapped in. A short set of KPIs, tracked every week, shows when it is time to survey again.
| KPI | Formula | Good Direction | Warning Sign |
|---|---|---|---|
| Leak share | Quiet-window flow divided by average flow | Below 10 percent | Rising month on month |
| Specific power | kWh per Nm3 delivered | Stable or falling | Creeping up with no load change |
| Pressure loss | Compressor outlet minus far-end pressure | Below 0.7 bar to the header | Growing during busy shifts |
| Air per kg of fabric | Nm3 per kg produced | Falling | Rising with the same product mix |
| Leaks open | Tagged and not yet closed | Shrinking | Backlog older than 30 days |
| Unloaded hours | Compressor hours running at no load | Low | Many hours at no load |
From kWh to Sustainability Reporting
Leak repairs also show up in sustainability reports. Energy per kilogram of fabric and the carbon that goes with it are easy to compute from the same meters. The figures below are illustrative.
After repairs, compressed air energy would fall to 10,692 kWh a day, or about 0.594 kWh per kg. Multiply the saved kWh by your own grid emission factor to get the carbon figure, since factors differ by country, year and supplier. Do not borrow one from a different plant or period.
Common Leak Program Mistakes
Most leak programs fade, not because the method is wrong but because habits slip. Each mistake below has a plain fix.
A 90-Day Path to Leak Control
iFactory AI is built as a turnkey server that racks in, plugs in and goes live in roughly 6 to 12 weeks, so a leak program with live metering fits inside a quarter.
What iFactory AI Adds
iFactory AI is smart manufacturing and industrial software. For compressed air it brings meter data, production and maintenance into one view.
Plain-Language Glossary
Shared words keep engineers, operators and finance on the same page.
Frequently Asked Questions
How much compressed air do textile mills lose to leaks?
The DOE rule of thumb is 20 to 30 percent in poorly maintained systems, and below 10 percent in well-kept ones. Measure your own mill with a quiet-window test, since sites vary widely.
How do we measure leaks without finding each one?
Stop all machines and read the air flow still being produced, then divide by the average production flow. Ask support how this test runs automatically from live meters.
Which leaks should we fix first?
The largest by annual cost, since cost grows roughly with the square of hole size. A small number of big leaks usually carries most of the loss.
Can we lower the pressure setpoint?
Often, after repairs and filter clean-up. DOE guidance puts the saving at about 1 percent per 2 psi. Lower in small steps and watch loom stops.
How often should we repeat the survey?
Run the quiet-window test monthly and survey the halls at least yearly, or sooner when the leak share starts to climb.
Stop Paying to Make Air You Lose
iFactory AI brings flow, pressure and energy data together so your team can size the leak problem, rank repairs and prove the savings. Book a walkthrough on your own mill data.