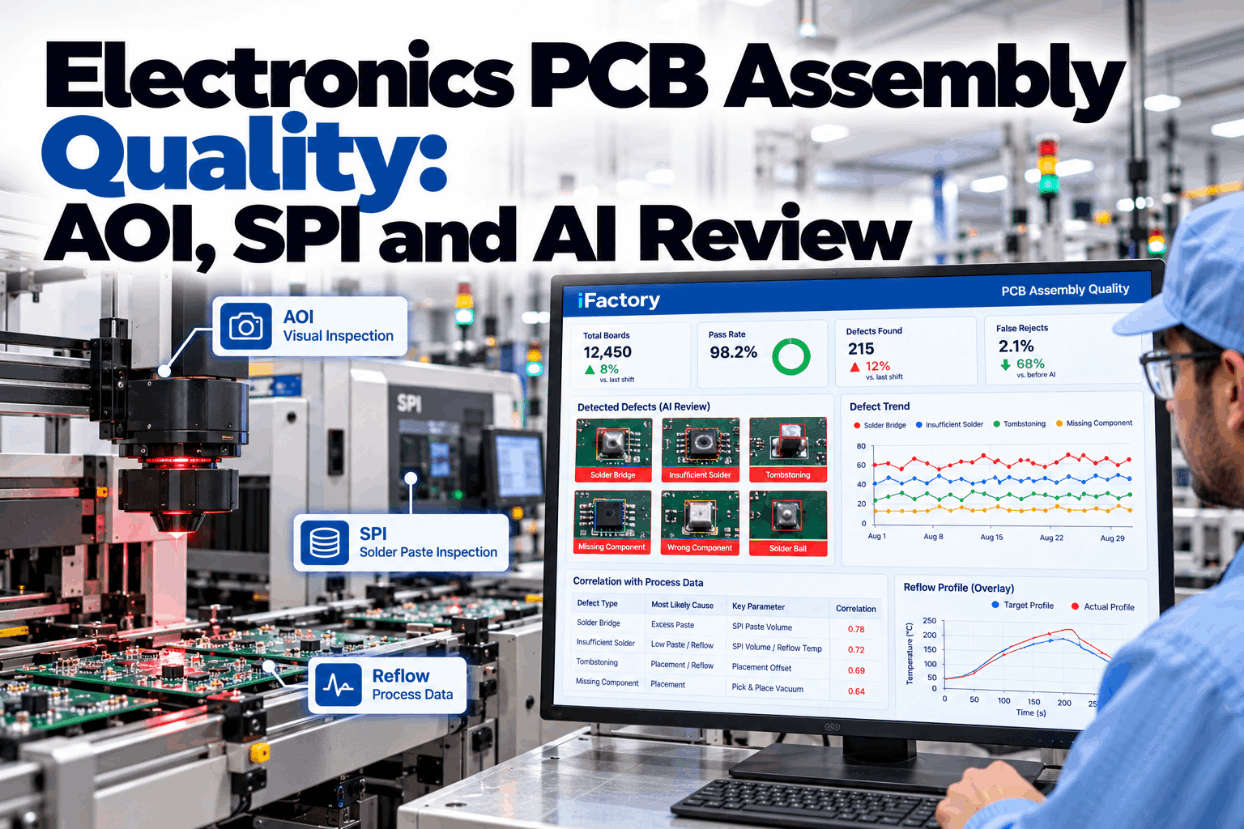
Electronics PCB Assembly Quality: AOI, SPI and AI Review

By Jackson T on October 21, 2026

electronics-pcb-assembly-quality-aoi-spi-ai-review

On most SMT lines, the AOI is not short of calls. It is short of trust. Operators clear call after call at the review station, a real insufficient joint slips through with the false ones, and nobody connects it back to the stencil aperture that started it. Good PCB assembly quality comes from treating SPI, AOI and X-ray as one chain of evidence for each board, not three separate machines. See that chain on real board data in a short SMT review demo.

AI VISION · ELECTRONICS ASSEMBLY

Fewer False Calls, Real Defects Traced to Paste, Placement or Reflow

The iFactory AI Review Layer re-classifies every AOI call before it reaches the operator. It checks each confirmed defect against SPI and reflow data for that pad and opens an NCR against the board serial.

SN 2410-0336 · SMT Line 24 AOI calls
AI review after AOI · Class 2 product
C112Lifted lead?False call · reflection
U7 pin 14Bridge?False call · flux residue
R47Insufficient solderConfirmed
C9Tombstone?Unsure · to operator
NCR opened on SN 2410-0336 · stencil aperture check requested
THE SMT LINE AS A CHAIN

Seven Stations From Bare Board to Tested Assembly

A typical surface mount line prints solder paste through a stencil, inspects the paste, places parts, reflows the board and then inspects the joints. Each inspection gate sees something the others can't. SPI measures paste before parts hide it. AOI sees visible joints and part position. X-ray sees under BGAs and bottom-terminated parts. In-circuit test checks the electrical result. Map your own line with our electronics team.

1Stencil printPaste deposited on every pad
2SPIVolume, area, height and offset per pad
3PlacementParts picked and placed onto wet paste
4ReflowPaste melts, wets and forms joints
5AOIVisible joints, presence, polarity, position
6X-ray / AXIHidden joints, voids, BGA balls
7ICTOpens, shorts, values on the finished board
Inspection and test gates · each one writes a result against the board serial
SMT DEFECTS

Common Solder Defects, Where They Are Caught and What Starts Them

Most SMT defects have more than one possible cause, which is why the joint image alone rarely settles the argument. The matrix below links each defect to the gate that usually catches it and the upstream step to check first. Head-in-pillow is the hard one. The BGA ball sits on the paste without fusing, can pass electrical test and is not visible to AOI. Walk through your own defect pareto in a defect review.

Defect
What it looks like
Usually caught at
Check first
Insufficient solder
Thin or incomplete fillet, part of the pad dry
SPI (low volume), then AOI
Paste: aperture, release, blocked stencil
Bridging
Solder joining two leads or pads
SPI (excess or smeared paste), AOI
Paste: volume, offset, slump, stencil wipe
Tombstoning
Small chip part standing on one end
AOI
Uneven paste, placement offset, uneven heating
Misalignment
Part shifted or rotated off its pads
AOI
Placement: nozzle, feeder, vision, program
Voids
Gas pockets inside the joint
X-ray / AXI
Reflow profile, paste flux, pad design
Head-in-pillow
BGA ball resting on paste, not fused
Angled or 3D X-ray, sometimes only in the field
Warpage, oxidation, low paste, profile
Solder balls
Small spheres of solder beside the joint
AOI
Paste under stencil, moisture, fast ramp
IPC-A-610 ACCEPTABILITY

Which Class You Build To Changes What Counts as a Defect

IPC-A-610 is the common workmanship standard for electronic assemblies. It sets criteria for three product classes and judges each condition as Acceptable, Process Indicator or Defect. The classes stack: a defect for Class 1 is also a defect for Classes 2 and 3, and a Class 2 defect is a Class 3 defect. An AI review layer must be trained and set up for the class each product is built to. Confirm your class mapping with our quality team.

Class 1
General electronic productsFunction is the main requirement. Cosmetic flaws allowed if it works. Toys, simple consumer goods.
Class 2
Dedicated service productsLong, reliable service life expected. Industrial controls, telecom and commercial equipment.
Class 3
High performance productsFailure is not an option. Medical, aerospace, defence and safety-critical systems.
Process indicators are not defects, but they are signals

A process indicator does not reject the board, yet a rising count of them on one part or pad is often the earliest sign that the print, placement or profile is drifting.

AOI FALSE CALLS

Why AOI Flags Good Joints, and What an AI Review Layer Adds

Rule-based AOI is tuned to miss nothing, so its limits are set tight. Shiny fillets, flux residue, silkscreen, part colour changes between reels and board warp all trip those limits. The result is a stream of calls that operators must clear, and a review habit that can wave real defects through. An AI review layer looks again at each call and sorts it before a person sees it. Your own false call rate is the baseline to measure against. See it on your images in a false call review.

AOI ALONE
  • Every call goes to the operator to accept or reject
  • Limits widened to calm the line, which risks escapes
  • Reel or board changes trigger fresh waves of calls
  • Verdicts rarely linked to SPI or reflow data
AOI + AI REVIEW LAYER
  • Calls sorted into confirmed, false or unsure
  • Operators review the unsure group and spot-check the rest
  • AOI limits stay tight because noise is handled after
  • Confirmed defects carry SPI and profile data with them
Confirmed defectGoes to repair with an NCR on the board serial
UnsureShown to the operator first, with the reason
False callCleared and sampled for audit, always kept in the log

Let the Review Station See Only What Needs a Person

iFactory re-classifies AOI calls, ties each confirmed defect to SPI and reflow data for that pad and opens the NCR against the board serial. Operators keep the final say on unsure calls.

SMT Line 2 · Process engineer and iFactory
EngineerWhy are we seeing insufficient solder on R47 again?
iFactoryFive confirmed on R47 pad 2 this shift. SPI volume on that pad has been under 70% on all five boards, other pads are normal.
EngineerSo it's the print, not the oven.
iFactoryThe profile for those boards is in window. I suggest checking that aperture for paste build-up. NCRs are open on all five serials.
REFLOW PROFILE

Four Zones, and the Defects Each One Can Cause

A reflow profile is the temperature path the board follows through the oven. For lead-free SAC305 paste, typical guidance is a gentle ramp, a soak to even out the board, a peak above the alloy's liquidus of about 217°C and a controlled cool. The ranges below are typical published figures. Your paste maker's datasheet and your thermocouple runs set the real window. Check your profile data with our process specialists.

PreheatRamp about 1–3°C/sToo fast: solder balls, spatter, part cracking
SoakAbout 150–200°C, 60–120 sToo short: uneven heating and tombstones
ReflowPeak about 235–250°C, 40–70 s above liquidusToo cool: poor wetting, voids. Too hot: damage, warp
CoolingAbout 2–4°C/sToo slow or uneven: coarse joint structure
FROM DEFECT TO CAUSE

Three Questions That Point a Defect at Paste, Placement or Reflow

When AOI or X-ray confirms a defect, the fastest route to the cause is to look at what the earlier gates recorded for that exact pad on that exact board. That only works if every result carries the board serial and pad reference. iFactory runs these checks automatically and attaches the answer to the NCR. Try it on your own escapes in a root cause walkthrough.

Defect confirmed on a pad, with board serial
Q1Was SPI volume, area or offset out on that pad?
Yes → Print · aperture, stencil wipe, squeegee, paste age
Q2If not, did AOI or the placer log offset or rotation?
Yes → Placement · nozzle, feeder, part data, vision
Q3If not, was the profile out of window for that board?
Yes → Reflow · zone setpoints, conveyor speed, loading
All three normal → check the part and board: coplanarity, solderability, moisture, warpage
PCB ASSEMBLY QUALITY TEMPLATE

A Per-Board Record That Follows the Serial

Per-board serial traceability is what turns inspection data into answers. When a field return arrives, you should be able to pull up exactly how that board was printed, placed, reflowed and inspected. Use these fields as a template, whether or not AI writes them. Ask our support team for a sample record.

Board SN 2410-0336Assembly 74-118 rev C · Class 2
PrintStencil ID, paste lot, print time
SPIPass, with any pads near limits
PlacementMachine, feeder and reel per part
ReflowOven recipe, setpoints, conveyor speed
AOICalls, AI verdicts, operator decisions
X-ray and ICTResults for BGAs and hidden joints
RepairWhat was reworked, by whom, re-inspected
NCRNumber, cause, linked boards
PCB ASSEMBLY QUALITY EXAMPLES

Three Typical Situations on an SMT Line

These are illustrations of how the review layer usually responds, not case studies. Each one shows how linking the gates changes the next action. Bring your own recent escapes to a line review.

Tombstones on one 0402
SeenAOI confirms tombstones on C9 only
LinkedSPI shows uneven paste between the two pads
ActionAperture checked and stencil cleaned
Bridges after a reel change
SeenBridges on a fine-pitch IC from one feeder
LinkedPaste normal, placement offset in Y on that part
ActionPart data and nozzle checked on the placer
BGA voids rising
SeenX-ray void area trending up on one BGA
LinkedNew paste lot and a shorter soak recipe
ActionProfile re-run with thermocouples
PCB ASSEMBLY QUALITY FOR PLANT MANAGERS

PCB Assembly Quality Best Practices for the Whole Line

The tools matter less than the habits around them. These practices keep inspection honest and make root cause work fast. Most of them cost nothing but discipline. Review them against your line with our electronics team.

01Serialise every boardEvery gate writes against the same serial and pad reference.
02Track false calls as a KPICalls per board and false share, by product and by AOI program.
03Keep AOI limits tightFix noise with review, not by widening limits that guard escapes.
04Act on SPI trendsA pad drifting toward its limit is cheaper to fix than a defect.
05Profile with thermocouplesRe-run when the board, paste, oven or loading changes.
06Audit cleared callsSample false calls weekly so trust is earned, not assumed.
TURNKEY AI DEPLOYMENT

AI Review Layer, Line Connectors and NVIDIA Server in One Package

iFactory delivers the AI Review Layer as a turnkey bundle. A pre-configured NVIDIA AI server ships racked and ready with the review models and line connectors pre-loaded, so AOI images are re-classified on site at line speed. You rack it, plug in power and Ethernet, and the AI is live. To scope it for your SMT lines, request a turnkey quote.

What's Included
  • Pre-configured NVIDIA AI edge server, racked and ready
  • Connectors for your AOI, SPI and AXI result files
  • Review models trained on your own call images
  • Reflow oven and profile data linked per board
  • Per-board serial record and NCR workflow
  • Operator review screen for unsure calls
  • 24×7 remote monitoring of models and hardware
Live in 6–12 weeks
Wk 1–4
Connect and Collect

Server installed, AOI, SPI and oven data linked, past calls and verdicts gathered.

Wk 5–8
Train and Shadow

Review models trained and run in shadow, compared with operator verdicts.

Wk 9–12
Go-Live and Training

Call sorting, NCRs and board records switched on, operators trained.

HOW iFACTORY FITS

A Review Layer That Works With the AOI You Already Own

iFactory does not replace your SPI, AOI or X-ray. It reads their results, connects them per board and puts better decisions in front of people. Our support team can outline a pilot on one line.

1
Re-classifies AOI calls. Each call is sorted into confirmed, false or unsure before it reaches the review station.
2
Links defects to SPI. Paste volume, area and offset for the same pad travel with every confirmed defect.
3
Brings in reflow data. Oven recipe and profile for that board help separate print, placement and heat causes.
4
Opens NCRs per serial. Every board keeps a full record from print to test.
1000+
Industrial clients running iFactory
99.9%
Platform uptime for multi-shift SMT lines
6-12 wks
From racked server to live call review
FREQUENTLY ASKED QUESTIONS

What Plant Managers Ask About PCB Assembly Quality

What is an AOI false call?
A false call is a joint or part that AOI flags as defective but that meets your acceptance criteria when a person or a second check reviews it. Common triggers are reflections from shiny fillets, flux residue, silkscreen, part colour changes between reels and slight board warp.
Does the AI review layer replace our AOI?
No. It works after your existing AOI, reading its images and calls. That lets you keep AOI limits tight while the review layer handles the noise. Your AOI programs and hardware stay as they are.
How does it link a defect to solder paste inspection?
Every result is stored against the board serial and pad reference. When a defect is confirmed, iFactory pulls the SPI volume, area, height and offset for that pad, plus placement and oven data for that board, so the NCR shows which step most likely caused it.
Can it find head-in-pillow defects?
Not from AOI images, because BGA joints sit under the package. Head-in-pillow needs angled or 3D X-ray and sometimes destructive analysis to confirm. iFactory can read AXI results and connect them to paste, warpage-related and profile data for that board.
How is IPC-A-610 class handled?
Each product is mapped to the class it is built to. Review models and rules follow that class, so a condition that is acceptable on a Class 2 board can still be flagged as a defect on a Class 3 board.
What do we need to get started?
Access to your AOI, SPI and oven result data, a few weeks of past calls with operator verdicts and one line to pilot on. The review layer runs in shadow before it sorts calls live. Our support team can scope the pilot with you.

Trust Every Call That Reaches the Review Station

Sort AOI calls with AI, link each defect to paste, placement and reflow data, and keep a full record for every board serial. The system is delivered turnkey and goes live in 6 to 12 weeks.
Example shift summary · SMT Line 2
Boards inspectedSPI, AOI and AXI per serial
AOI callsSorted before the review station
Confirmed defectsLinked to paste, placement or reflow
NCRsOpened per board serial
Every board traceable from print to test

Share This Story, Choose Your Platform!