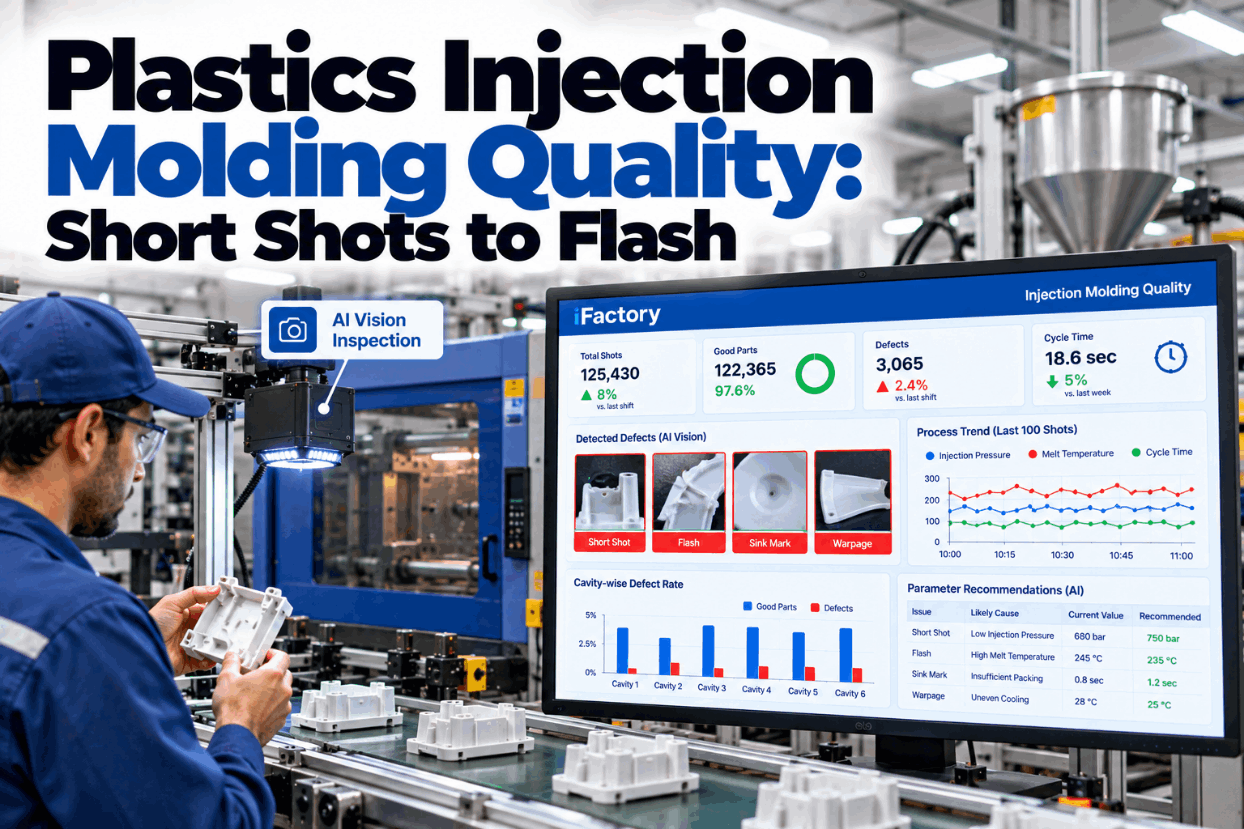
Most molding defects are not mysteries. A short shot, a flash line or a sink over a boss is the part telling you that pressure, temperature or time was wrong in one cavity on one shot. The trouble is that the press records those numbers and nobody reads them until the parts are already in the box. Injection molding quality improves fastest when every shot is checked against the window that made good parts and the setup tech hears about drift before it becomes scrap. Hear how that sounds on a real press in a short molding floor demo.
Catch Short Shots, Flash and Sink by Cavity, Shot by Shot
iFactory Shot-Level Analytics reads press and cavity pressure data for every shot, predicts defects by cavity and confirms them with vision checks. Setup techs get the recommended change by voice and confirm what they did.
Most Defects Sit at One End of the Pressure Scale
Cavity pressure tracks part quality closely. Too little pressure in the cavity gives small parts, short shots and sinks. Too much gives oversize parts and flash. That simple idea is why a sensor near the last place to fill is so useful: most quality defects can be linked to the pressure at that spot. A few defects, such as burn marks and flow lines, depend more on speed, venting and temperature. Check where your own defects sit with our molding team.
Seven Molding Defects, Their Usual Causes and the First Move
Every defect has a list of possible causes in the material, the machine, the mold and the process. The matrix pairs each one with the signal that usually shows up in shot data first and the change a setup tech would normally check before anything else. Your validated process sheet always comes first. Review your own defect list in a defect session.
Decoupled Molding Splits the Shot Into Stages You Can Control
Scientific molding sets the process from data rather than habit. In decoupled molding, the first stage fills the cavity by speed to about 95–98% full, then switches to a separate pack and hold stage. Stopping short of full lets melt momentum settle and helps prevent flash. Hold continues until the gate freezes, which you find with a gate freeze study: weigh parts at rising hold times and note where weight stops increasing. The study below is illustrative. Plan your own studies with our process engineers.
Where the Sensor Goes Decides What It Can Tell You
Press data such as injection pressure and screw position tells you what the machine did. Cavity pressure tells you what the plastic did. The usual starting point is a sensor at the end of fill, the last place the cavity fills, often found with a short shot. A second sensor near the gate helps separate gate and runner problems from the rest. Cold runner tools can often share one sensor across several cavities, while hot runner tools usually need more, because flow balance shifts over time. Size your sensor plan in a sensor planning call.
Recommendations Spoken to the Setup Tech, Not Buried in a Report
iFactory watches every shot by cavity, predicts which cavity is heading for a defect and tells the setup tech what to check. The tech makes the change at the press and confirms it by voice, so every adjustment is logged with the shot number.
A Window, Not a Single Setpoint
A robust process makes good parts across a range of settings, not just at one. A molding area diagram maps that range by running a grid of two settings, often melt temperature and hold pressure, and marking which combinations made good parts. The wider the good area, the more room the process has to absorb normal variation. iFactory compares every shot against that window, not just the setpoint. The grid below is illustrative. Get help building yours from our support team.
A Quick Clamp Tonnage Estimate Before You Chase Flash
Flash often starts with the clamp. A common rule of thumb multiplies the projected area of all cavities, plus any cold runner, by a factor in tons per square inch. Published guidance puts that factor anywhere from 2 to 10 depending on the material and flow length, with 3 as a common starting point. More is not better: excess tonnage can crush vents, which brings burns and short shots, and can damage the mold. The example uses assumed inputs. Check your own tools in a tonnage review.
Two Shot-by-Shot Stories: Flash on One Cavity, Sink on a Boss
These are illustrations of how shot-level data usually plays out, not case studies. Both show a small change upstream turning into a defect, and how the shot record points straight at it. Walk through your own recent defects with our molding team.
A Process Sheet That Says Who May Change What
A process sheet is only useful if it shows the window as well as the setpoint, and who is allowed to move each value. That turns AI recommendations into safe, bounded actions. Use the layout below as a template for each tool and press. Ask our specialists for a blank version.
Injection Molding Quality Best Practices, in the Order That Works
Plants that get the most from shot data tend to follow the same order. They fix the process first, then add sensors and analytics, then hand recommendations to the people at the press. Skipping the first steps means the AI learns a process that was never stable. Plan your roll-out with our support team.
Injection Molding Quality Software, Connectors and NVIDIA Server in One Package
iFactory delivers Shot-Level Analytics as a turnkey bundle. A pre-configured NVIDIA AI server ships racked and ready with press connectors, defect models and vision checks pre-loaded, so every shot is scored on site in real time. You rack it, plug in power and Ethernet, and the AI is live. To scope it for your molding floor, request a turnkey quote.
- Pre-configured NVIDIA AI edge server, racked and ready
- Press and hot runner controller data connectors
- Cavity pressure sensor data integration
- Vision checks for shorts, flash and sink at the take-out
- Per-cavity defect prediction models for each tool
- Voice recommendations and confirm-back for setup techs
- 24×7 remote monitoring of models and hardware
Server installed, press, sensor and vision data linked, process sheets loaded.
Per-cavity models trained and run in shadow against quality results.
Voice alerts switched on, setup techs trained, weekly defect review started.
Shot Data Put to Work at the Press
iFactory turns the data your presses already produce into per-cavity warnings and clear actions for the people running them. Our support team can outline a pilot on one press.
What Plant Managers Ask About Injection Molding Quality
Know Which Cavity Is Drifting Before It Fills a Box
Score every shot by cavity, confirm with vision and give setup techs clear, bounded recommendations by voice. The full system is delivered turnkey and goes live in 6 to 12 weeks.