SPC was developed for discrete parts, where every piece gives a fresh reading. Batch processes don't work that way. A reactor, a paint tank or a cooking kettle produces one result per batch, consecutive batches share raw material lots and equipment condition, and the same vessel runs several products. Copying textbook charts onto batch data produces false alarms and missed shifts in roughly equal measure. This guide covers SPC that suits how chemicals, coatings and food plants actually run, and you can see it in a short live demo.
Batch SPC That Separates Raw Material Effects From Real Process Drift
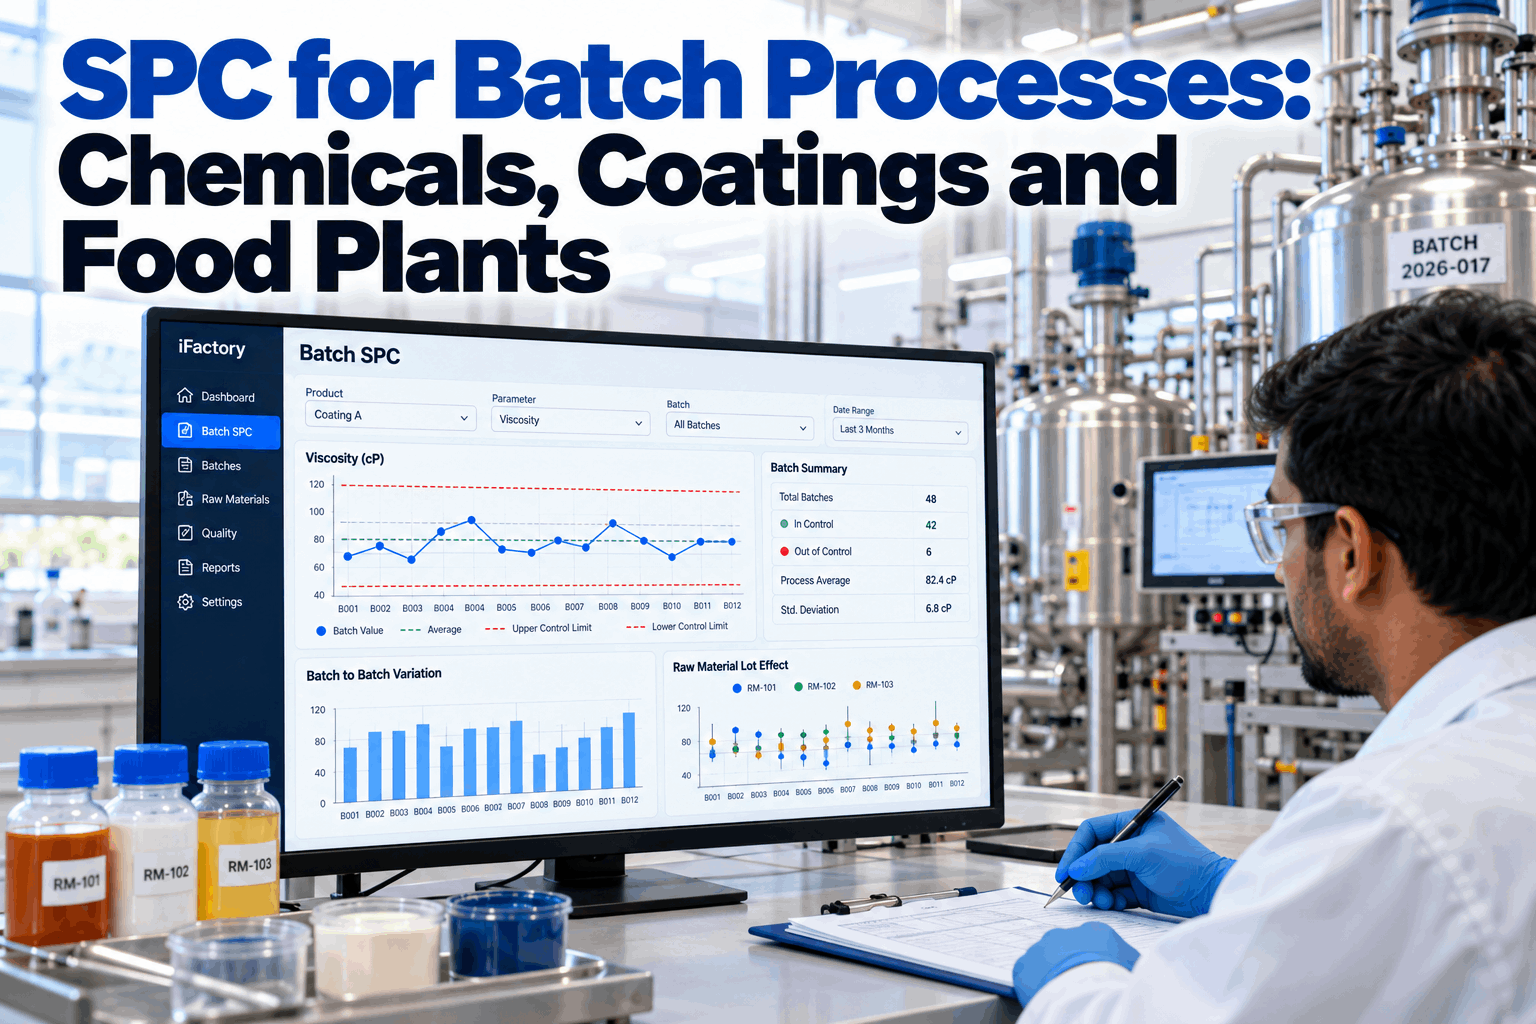
iFactory's Batch SPC charts every product and batch parameter, overlays raw material lots so lot-driven shifts are obvious, and suggests adjustments for the next batch, with operators approving each change.
Four Ways Batch Data Breaks the Textbook Assumptions
Classic Shewhart charts assume a steady stream of independent readings from one stable process, grouped into rational subgroups. Those assumptions hold well on a machining line producing thousands of identical parts. Batch processes rarely give you that. Recognizing which assumption your data breaks is the first step toward charts that alarm on real problems and stay quiet otherwise. Most batch plants break at least two of the four below, which is why a parts-industry SPC package often disappoints when it is pointed at a reactor or a mixing tank. If you'd like a review of your current batch charts, our SPC specialists can help.
Each batch gives a single final result, so there are no natural subgroups and data arrives slowly, sometimes only a few points a week.
Consecutive batches share raw material lots, vessel fouling and catalyst age, so readings depend on the ones before and aren't independent.
The same reactor or kettle runs different products and recipes, each with its own target and variation.
Variation within a batch, from sampling and mixing, is often far smaller than variation between batches, from lots and conditions.
Which Control Chart Fits Which Batch Situation
There is no single "batch chart", and choosing one by habit is a common source of trouble. The right choice depends on how many samples you take per batch, how many products share the equipment and whether you are watching for sudden shifts or slow drift. The matrix below is a practical starting guide. Many plants use two charts on the same parameter, an I-MR for sudden shifts and an EWMA for slow drift, because each catches what the other misses. You can see each chart running on batch data in a working session.
When Consecutive Batches Aren't Independent
Autocorrelation is the quiet reason many batch charts misbehave. If each batch is more like the one before than a random batch would be, because of a shared raw material lot, gradual vessel fouling or a slowly ageing catalyst, then the moving range underestimates true variation. Limits come out too tight, and the chart alarms constantly on normal behavior. Teams then learn to ignore it, and when a real shift does happen it is lost among the false alarms. Autocorrelation is common in batch plants, so it is worth testing for before any limits are set. Our support team can test your batch data for autocorrelation and show which of the four steps below your process needs.
Check the lag-1 correlation of batch results. A clearly positive value means neighboring batches move together.
Raw material lots, cleaning cycles and equipment age are the usual causes. Link them to each batch record.
Chart the residuals after accounting for the known effect, such as the lot mean or time since cleaning, so the chart watches what's left.
For real slow drift, use EWMA or CUSUM with defined resets after cleaning or catalyst change.
Ask Why a Run of Batches Went High
iFactory links each batch to its raw material lots, equipment and recipe, so when a chart moves the reason is a question away. It also suggests a next-batch correction for operators to approve.
Overlay Raw Material Lots on Every Batch Chart
In many batch processes, the biggest single source of batch-to-batch variation is raw material. Different lots of resin, flour, solvent or active ingredient behave slightly differently even within specification. A supplier's certificate may show every lot passing, yet the spread between lots can still be wide enough to move your batch results noticeably. Overlaying lot changes on the chart turns a confusing pattern into an obvious explanation and points to the right fix: the recipe, the supplier or the incoming specification. It also stops wasted investigations into process causes that were never there. We can show overlays on your own batch history in a short demo.
What to Chart in Chemicals, Coatings and Food
The principles are the same across process industries, but the critical parameters differ. The parameters worth charting are the ones that predict customer complaints or downstream problems, not simply everything the lab measures. These are typical starting points. Your specifications and quality risks decide the final list. Start with three to five per product and add more once those are working. Our support team can help prioritize parameters for your products.
- Assay or purity
- Viscosity and density
- pH and acid or amine value
- Moisture content
- Reaction end-point time
- Viscosity at shipping temperature
- Color difference (ΔE) to standard
- Solids content
- Gloss and fineness of grind
- Density and drying time
- Brix or total solids
- Moisture and water activity
- pH and salt content
- Fill weight
- Cook temperature and time
Adjust on Signals, Not on Noise
Feeding batch results back into the next recipe can reduce variation, but only if adjustments respond to real signals. Adjusting after every batch to chase random variation, which Deming demonstrated with his funnel experiment, makes the process worse. The safe approach is to adjust only when a chart shows a signal or a known lot effect, by a bounded amount, with operator approval. Each adjustment should also be recorded against the batch, so its effect can be seen on the chart and judged before the next one is made. You can see guarded suggestions in a guided demo.
- A chart signal confirms a real shift
- A new raw material lot has a known offset
- Equipment state has changed, such as after cleaning or a new catalyst
- A single batch is high or low within limits
- The cause hasn't been identified
- The last adjustment hasn't had time to show its effect
- Maximum change per step
- Recipe limits never exceeded
- Operator approval and a logged reason
Four Batch SPC Mistakes That Erode Trust in the Charts
When operators stop believing a chart, they stop reacting to it, and the investment in SPC quietly disappears. These four mistakes are the most common reasons batch charts lose credibility. Each one is easy to spot once you know what to look for. Our SPC specialists can audit your current charts against them.
Specs say what the customer accepts, while control limits say what the process normally does. Mixing them hides shifts until product is already out of spec.
Plotting different products on one raw chart makes product changes look like shifts. Use standardized charts or separate charts.
Limits set years ago after a recipe or equipment change no longer describe the process and either alarm constantly or not at all.
A signal with no defined response becomes a dot on a screen. Each chart needs a written first action for each type of signal.
Batch SPC, Data Connections and AI Server in One Package
iFactory delivers Batch SPC as a turnkey bundle. A pre-configured NVIDIA AI server ships racked and ready with the SPC engine and adjustment models pre-loaded, so process data stays on site. You rack it, plug in power and Ethernet, and the AI is live. To scope it for your plant, request a turnkey quote.
- Pre-configured NVIDIA AI edge server, racked and ready
- Connectors for batch records, LIMS, ERP lots and certificates
- Chart library per product and parameter
- Cabling and plant network setup
- PLC/SCADA and batch system integration
- Training for process engineers and operators
- 24×7 remote monitoring
Server installed, batch history and raw material lots linked, parameters prioritized.
Charts and lot effects reviewed on one product family, with suggestions in advisory mode.
All products live, approval flow on, engineers and operators trained.
Batch SPC Built for Process Industries
iFactory handles the realities of batch data, including one value per batch, many products, lot effects and drift, and turns charts into decisions. Process engineers spend their time on causes rather than on rebuilding charts in spreadsheets. Our support team can review your current batch SPC before a pilot.
What Process Engineers Ask About Batch SPC
Make Batch SPC Alarm Only on Real Problems
Chart every product and parameter correctly, see raw material lot effects at a glance and get bounded next-batch suggestions that operators approve. The full system is delivered turnkey and goes live in 6 to 12 weeks.