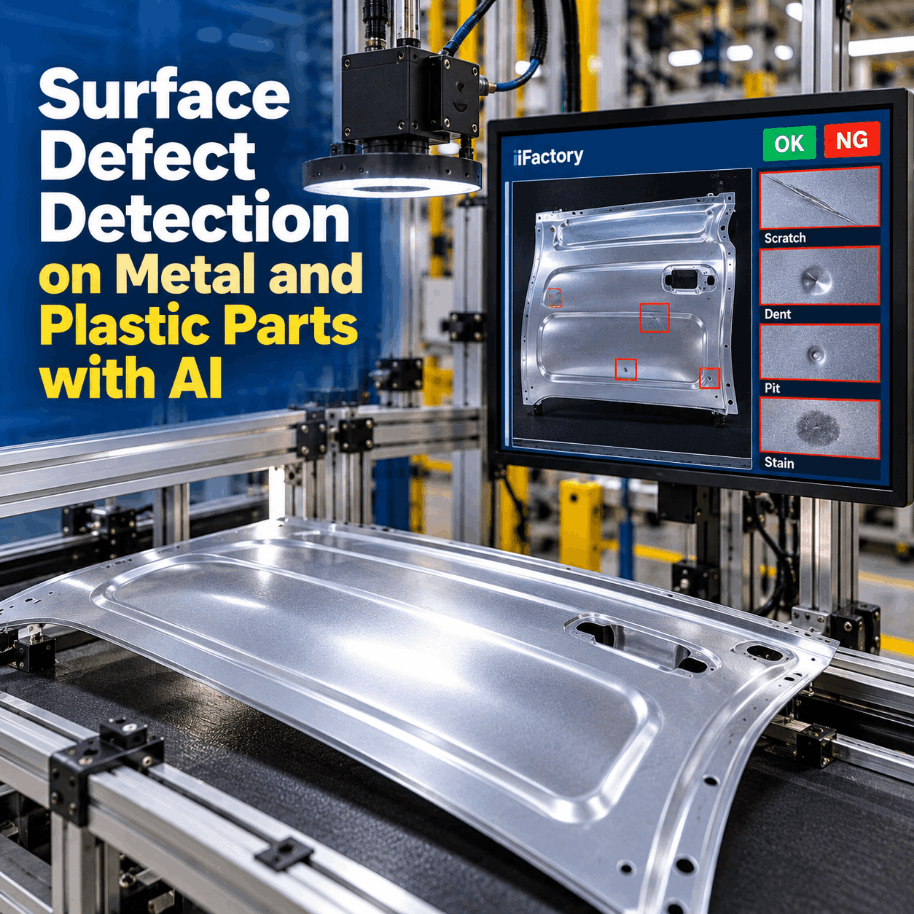
A scratch a customer can see on a machined cover or a glossy moulded bezel is a defect, even when the part works perfectly. The difficulty is that the same scratch can vanish under one light and flare under another, and a textured plastic can look like a field of defects to a camera set up for polished metal. Surface defect detection works when the lighting, the resolution and the model are matched to each material and finish, and when borderline calls go to a person instead of a guess. See it on your own parts in a short surface AI demo.
Find Scratches, Dents and Stains Without Rejecting Good Parts
iFactory Surface AI trains a model for each material and finish, runs every station under controlled lighting and sends borderline calls to an AI review queue. Clear defects are rejected at once. Unclear ones get a second look.
Six Surface Defects and What Makes Each One Show
Cosmetic defects differ in how they change the light, which is why one camera setup rarely finds them all. A scratch is a narrow groove that scatters light. A dent changes the slope of the surface without breaking it. A stain changes colour or gloss but not shape. Knowing what each defect does to light is the first step in choosing how to light it. Map your own defect list with our vision support team.
Match the Light to the Defect, Then Choose the Camera
Lighting decides contrast before the camera or the AI gets a say. Dark field puts light at shallow angles, so smooth surfaces stay dark while scratches, dents and particles show bright. A dome surrounds the part with diffuse light and calms hotspots on curved, shiny parts. Coaxial light comes down the lens axis through a beam splitter and suits flat, reflective faces. Photometric stereo takes several images from one viewpoint, each lit from a different direction. It needs at least three light directions, and four or more are used in practice. Test the options on real parts in a lighting trial.
Polarisers Tame Glare, Up to a Point
Put one polariser on the light and a second on the lens, turned at right angles, and light that keeps its polarisation when it reflects is blocked while scattered light passes. Shiny surfaces such as bare metal and paint keep much of that polarisation, so their mirror glare is cut and the diffuse light from the material shows through. On glossy plastic that can reveal stains hidden under the shine. On polished metal, nearly all the light is mirror glare, so crossed polarisers can leave a very dark image, and each filter costs light as well. Ask our optics team how your parts behave.
- Glossy moulded plastic with stains or colour defects
- Painted or coated parts with bright hotspots
- Clear film or a window over the surface
- Plastic parts where moulded-in stress matters
- Bright turned or polished metal: dark field
- Curved chrome or plated parts: dome
- Flat machined faces: coaxial
- Dents on shiny parts: photometric stereo
Why the Model Is Trained per Material and Finish
Every finish has its own normal texture, and the model has to learn it before it can spot what is abnormal. Machined metal carries tool marks in one direction. Cast skin is rough and varies from part to part. Moulded plastic copies the mould finish, which is graded: SPI runs from A-1, a diamond-buffed high polish, through paper and stone grades to D-3, a coarse dry-blasted dull finish. VDI 3400 numbers rise with roughness, and those textures are mostly made by EDM. A model trained on one grade will misread another. See per-finish models in a model walkthrough.
Borderline Calls Get a Second Look, Not a Guess
Surface AI rejects clear defects at the station and sends unclear ones to a review queue with the image, the score and the closest library examples. Every review decision becomes a new labelled sample.
Worked Example: Can One 5 MP Camera See a 0.1 mm Scratch?
A common machine vision rule says a feature needs at least two pixels across it with excellent contrast, and three to four pixels for reliable results. The example checks a 100 × 80 mm moulded cover against a spec that says scratches 0.1 mm wide must be caught. The figures are illustrative, so run your own part through the same steps with our vision engineers.
A higher-resolution sensor with one view is the other route, but the lens must resolve pixels that small. Four views mean four images per part, so check the cycle time. A fine scratch still needs dark field to give it contrast.
Boundary Samples Decide Where a Pass Ends
A defect library is more than a folder of bad parts. It holds clear passes, clear fails and, most important, boundary samples: parts right at the edge of the cosmetic standard, agreed by quality and, where needed, the customer. Train on them, test on them and use them to check that reviewers agree with each other. AIAG suggests a kappa of at least 0.75 indicates good agreement, with values near 0.90 preferred. Build your first library in a library setup session.
How the AI Review Queue Handles Borderline Calls
Every inspection makes two kinds of error. A false reject scraps or re-checks a good part, which costs yield and labour. An escape ships a defective part, which costs a complaint or a claim. Moving a single threshold only trades one error for the other. A review band between two thresholds lets clear calls run automatically while uncertain ones go to a person. Tune your bands with our quality support team.
Six Numbers That Show Whether Surface AI Is Working
Track these from the first week of shadow running so you have a baseline. Keep false rejects and escapes side by side, because improving one while hiding the other is easy. Ask for a sample weekly report in a reporting demo.
Price Your False Rejects First
Escapes are hard to price honestly, so start with false rejects, which you can count. The worksheet uses assumed inputs to show the arithmetic only. Use your own shift counts, and our support team can help build the fuller case.
Add scrapped good parts at your own part cost. Keep escape savings out of the sum until shadow results show what the model really catches.
Cameras, Lighting and an NVIDIA Server Set Up for Your Finishes
iFactory delivers Surface AI as one package. Cameras and lights are chosen per station from trials on your parts, and a pre-configured NVIDIA AI server ships racked and ready with the review queue and defect library pre-loaded. You rack it, plug in power and Ethernet, and the AI is live. Price your stations in a turnkey quote call.
- Pre-configured NVIDIA AI server, racked and ready
- Cameras and lighting chosen from trials on your parts
- Models trained per material and finish
- Defect library with signed boundary samples
- AI review queue for borderline calls
- PLC link to each reject gate
- 24×7 remote monitoring of models and hardware
Defects listed, lighting tried on real parts, stations and server installed.
Per-finish models run silently and are compared with inspector calls.
Gate switched on, review band set, reviewers and operators trained.
Surface Defect Detection Software Built Around the Finish
Surface AI treats each material and finish as its own inspection job, which is what keeps good parts moving. Our support team can walk you through a pilot plan.
What Quality Teams Ask About Surface Defect Detection
Catch Real Defects and Keep Good Parts Moving
Train per finish, light each station for its defects and send borderline calls to review. The full system is delivered turnkey and goes live in 6 to 12 weeks.