Paint and Coating Defect Detection with AI Vision Systems

By Josh Brook on October 21, 2026

paint-coating-defect-detection-ai-vision-systems

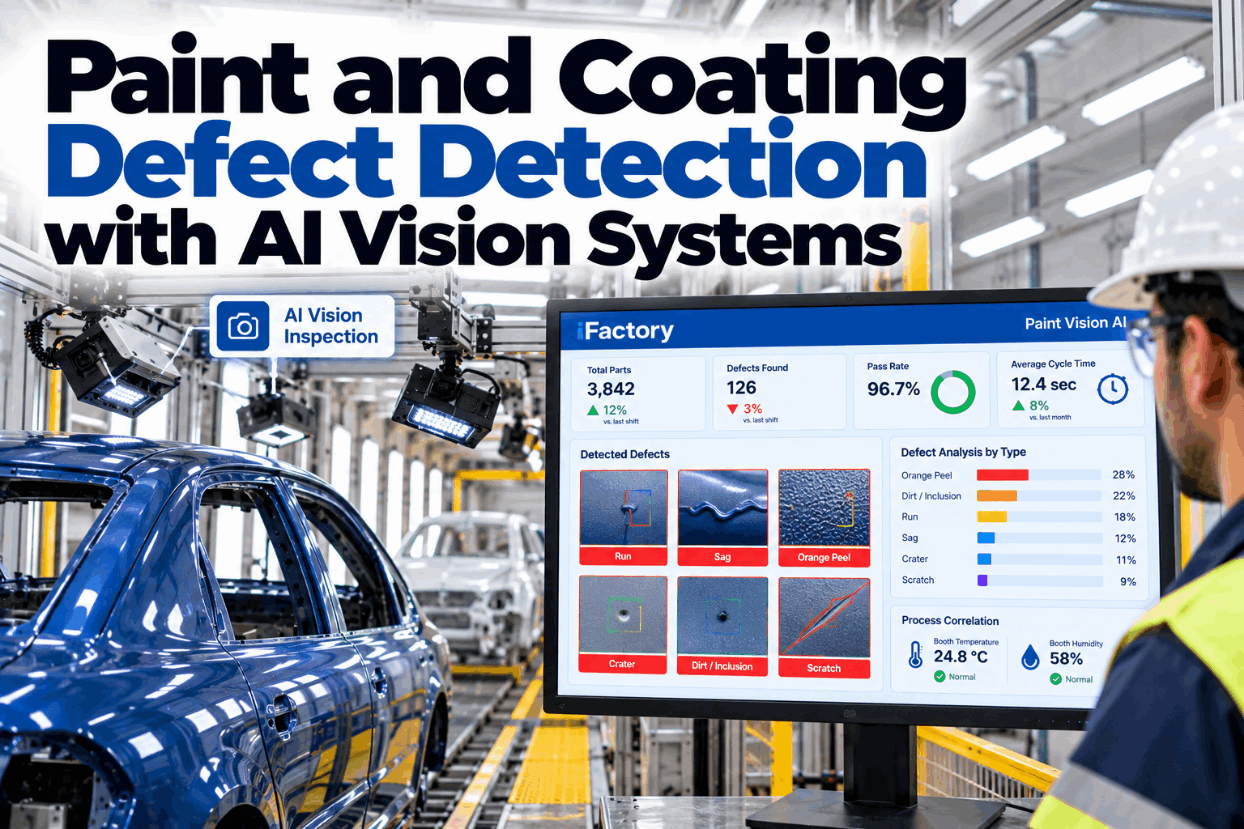
Finding a paint defect is only half the job. A crater, a sag and a dirt nib can sit side by side on one panel, yet each was born somewhere different in the booth and each needs a different repair. If the inspection line only says "defect", the cause keeps producing more of them and the repair deck guesses at the fix. Paint defect detection with AI vision names the defect, points to its likely root cause in the booth and sends the body to the right repair. See it on real panels in a short paint vision demo.

AI VISION · PAINT SHOP QUALITY

Name the Defect, Find Its Cause in the Booth, Route the Repair

iFactory Paint Vision AI uses tunnel cameras to classify every defect, checks it against booth humidity and temperature and routes each body to the right repair by defect type.

Body 8841 · Tunnel 23 defects
Clearcoat inspection · after oven
Crater 2 mmHood · contamination, booth 2 baseSpot repair
Sag 40 mmLeft door · high film build, booth at 19 °CPanel repaint
Dirt nibRoof · clearcoat inclusionSand and polish
Booth 2 now19 °C · 71% RHOutside setpoint
Body routed to repair deck B · booth lead alerted
PAINT DEFECT DETECTION

Six Defects That Fill Most Repair Decks

Most paint shop rework comes from a short list of defects. Each one has a typical look and a typical birthplace, which is why classifying them correctly is the first step to fixing the process, not just the panel. Coatings makers list causes such as excess film build and low temperature for runs, high temperature and high viscosity for orange peel, and silicone or oil contamination for craters. Review your own top defects with our paint quality team.

Clearcoat or base
Runs and sagsPaint flows down before it sets, leaving a curtain or drip
Clearcoat
Orange peelUneven, dimpled texture like the skin of an orange
Any layer
Craters and fish-eyesRound pits where paint pulled away from a contaminated spot
Any layer
Dirt and inclusionsFibres, dust or overspray trapped in the film as nibs
Clearcoat
Solvent popTiny blisters or pinholes from solvent escaping in the oven
Lower layers
MappingOutlines of earlier repairs or filler showing through
PAINT BOOTH DEFECTS

From Defect Type to Likely Root Cause

Classification becomes useful when every defect class is linked to the process data that can confirm or rule out a cause. iFactory stores booth, robot and material data against each body, so the likely cause comes with evidence instead of a guess. The matrix shows typical links. Confirm them on your own line in a root cause session.

Defect
Common causes
Data that confirms it
Who acts
Runs and sags
Excess film build, slow gun speed, low temperature, short flash time
Film build, robot speed, booth temperature
Robot programmer
Orange peel
High temperature, high viscosity, poor atomisation
Booth temperature, paint viscosity, bell speed or air pressure
Paint process engineer
Craters
Silicone or oil on the part, in the air supply or in the booth
Location pattern, air supply checks, pretreatment results
Booth and maintenance
Dirt and inclusions
Fibres from clothing, dust from filters, sanding or the conveyor
Booth pressure, filter age, location on the body
Booth cleanliness team
Solvent pop
Short flash-off, high film build, fast-evaporating solvent, hot part
Flash zone time and temperature, film build, oven ramp
Oven and process
Mapping
Thick filler or primer, poor drying of earlier coats, incompatible products
Repair history, primer film build, material batches
Repair and materials
BOOTH HUMIDITY AND TEMPERATURE

How Booth Conditions Shift the Defect Mix

Booth temperature and humidity change how fast solvents and water evaporate, and that changes which defects appear. Cold, damp air slows evaporation, so paint stays wet longer and is more likely to sag. Hot, dry air speeds it up, so paint has less time to level and orange peel and solvent pop become more likely. The grid shows general tendencies, not limits, since every paint system has its own window. Find your own window with our process specialists.

Temperature ↓ · Humidity →
Low RH
In window
High RH
Hot
Orange peel, solvent popFast evaporation, poor levelling
Orange peel riskWatch viscosity
Mixed effectsWaterborne flash slows
In window
Dry spray, peelEdges dry too fast
StableLowest defect rate
Sag riskSlower flash-off
Cold
Slower flashCold slows solvent release
Runs and sagsPaint stays fluid
Sags, slow flashHighest wet-film risk
DIRT IN PAINT

Where the Dirt Comes From, Read From Where It Lands

Dirt and inclusions are often among the most frequent defects on a paint line, and the hardest to blame on one source. Position on the body is a strong clue. Fibres on horizontal surfaces suggest something falling from above, nibs low on the sides point to the conveyor or floor, and dirt in one zone on every body points to one robot or one booth section. iFactory maps every nib by panel and zone, so patterns show up within a shift. Trace your dirt sources in a dirt mapping session.

Roof and hood
Falling from aboveBooth ceiling filters, plenum, overhead structures
Lower doors and sills
Rising from belowConveyor, skids, floor grating and booth pressure
Same zone, every body
One stationA robot cover, bell cup or tack-off step on that zone
Random, after breaks
People and doorsClothing fibres, door openings, sanding dust
SURFACE FINISH VISION

Light Tunnels and Deflectometry, Side by Side

Classic inspection uses light tunnels, where trained inspectors look for defects under bright stripes of light. Deflectometry automates the same idea: a known stripe pattern is reflected off the body and cameras measure how the reflection bends, which reveals small bumps and dents in the surface. iFactory tunnel cameras feed classification models that label each defect and record its position on the body. Plan your tunnel setup with our vision engineers.

Manual light tunnel
  • Inspectors judge reflected light by eye
  • Results depend on skill, fatigue and line speed
  • Defects marked by hand, often without a record
Automated deflectometry and AI
  • Bent stripes show bumps and dents as data
  • Every body checked the same way
  • Each defect logged with class, size and position

Every Defect Arrives With a Cause and a Route

iFactory tunnel cameras classify each defect, correlate it with booth humidity and temperature at the time the body was painted and route the body to the right repair by defect type. Booth leads see the pattern while it is still forming.

Paint shop · Booth lead and iFactory
Booth leadWhy are we seeing more sags this shift?
iFactorySags are up on doors from booth 2 since 14:00. Booth 2 has been at 19 °C and 71% RH, both outside setpoint.
Booth leadAnything else changed?
iFactoryFilm build on doors is also at the top of its range. Bodies with door sags are going to repair deck B.
FILM BUILD MEASUREMENT

Dry Film Thickness: The Number Behind Runs and Pops

Too much film build drives runs, sags and solvent pop, and too little causes poor hiding and weak protection. Dry film thickness is usually measured with magnetic or eddy current gauges, as described in ASTM D7091, and ISO 2808 sets out the wider range of methods. Wet film readings help catch problems before the oven, because dry film thickness is roughly wet film thickness multiplied by the paint's volume solids. Link your gauges to iFactory in a data connection review.

ClearcoatGloss and protection
BasecoatColour
PrimerSmoothing and chip resistance
E-coatCorrosion protection
Steel or aluminium
Wet to dry check · illustration
Wet film thickness100 µm
Volume solids45%
Expected dry film100 × 0.45 = 45 µm
If wet film rises to 130 µm130 × 0.45 = 58.5 µm
Compare with your own target range for that layer.
REPAIR ROUTING

Sending Each Body to the Right Repair

Not every defect needs the same fix. A dirt nib in the clearcoat can often be sanded and polished in minutes, while a crater that goes through the colour layer needs a spot repair, and a large sag on a visible panel may need a full panel repaint. iFactory routes each body using defect type, size, layer and zone, following the repair rules your quality team sets. Map your repair rules with our quality specialists.

Defect found and classified
Only in the clearcoat surface, and small?
YesSand and polishDirt nibs, light orange peel, small runs
No
Into the colour layer, but in one small area?
YesSpot repairCraters, small pops, deep nibs
NoPanel repaint or resprayLarge sags, clusters, mapping, adhesion issues
PAINT DEFECT DETECTION TEMPLATE

A Defect Record That Closes the Loop

Every defect record should connect the finished panel to the booth that painted it and the repair that fixed it. Use these fields as a template, with or without AI. Ask our paint vision team for a blank version.

Defect recordD-8841-02Sag · left door
Body and colourBody ID, model, colour code
DefectClass, size, layer, image
PositionPanel and zone on the body
Booth dataTemperature and RH at painting
ApplicationRobot, film build, viscosity, batch
Likely causeRanked, with supporting data
Repair routePolish, spot, panel or respray
Closed byRepair result, who and when
PAINT DEFECT DETECTION EXAMPLES

Found, Traced, Routed: Three Illustrations

These examples show how the system typically responds. They are illustrations, not case studies. Walk through your own recent defects with our paint engineers.

FoundCrater cluster on hoods
TracedSame robot, after a seal change
RoutedSpot repair, booth checked for silicone
FoundOrange peel on roofs
TracedAfternoon booth temperature above setpoint
RoutedSand and polish, air handling adjusted
FoundDirt nibs after a shift change
TracedBooth pressure low, filters overdue
RoutedSand and polish, filters changed
PAINT DEFECT DETECTION COST AND ROI

A Worksheet for Plant Managers

The value comes from two places: fewer defects once causes are fixed, and cheaper repairs when bodies go straight to the right route. Every input below is assumed, so replace each one with your own figures. Build the full case with our ROI specialists.

Bodies per day800assumed
×
Bodies needing repair12%assumed
=
Repairs per day96800 × 0.12
Repairs per day96from above
×
Sent to a heavier repair than needed15%assumed
=
Over-repairs per day14.496 × 0.15

Multiply over-repairs by the cost difference between routes, then add the value of each root cause fixed. Keep the sum to figures your own repair data supports.

TURNKEY AI DEPLOYMENT

Tunnel Cameras, Booth Links and NVIDIA Server in One Package

iFactory delivers Paint Vision AI as a turnkey bundle. Tunnel cameras and lighting are installed after the oven, booth sensors are linked, and a pre-configured NVIDIA AI server ships racked and ready with the defect and root cause models pre-loaded, so every body is classified on site. You rack it, plug in power and Ethernet, and the AI is live. To scope it for your paint shop, request a turnkey quote.

What's Included
  • Pre-configured NVIDIA AI edge server, racked and ready
  • Tunnel cameras and lighting for painted bodies
  • Defect classification models trained on your finishes
  • Booth temperature and humidity correlation
  • Film build and gauge data links
  • Repair routing rules by defect type and zone
  • 24×7 remote monitoring of models and hardware
Live in 6–12 weeks
Wk 1–4
Install and Collect

Tunnel cameras and server installed, booth data linked, images collected.

Wk 5–8
Train and Compare

Defect models trained and checked against inspector calls on the same bodies.

Wk 9–12
Routing and Training

Repair routing and booth alerts switched on, teams trained.

HOW iFACTORY FITS

Paint Defect Detection Software That Fixes the Booth Too

iFactory links what the camera sees on the panel to what happened in the booth. Our support team can walk you through a pilot plan.

1
Classifies every defect. Tunnel cameras label runs, orange peel, craters, dirt and pops by panel and zone.
2
Correlates with the booth. Humidity and temperature at painting are checked against each defect class.
3
Routes the repair. Bodies go to polish, spot repair or repaint by defect type.
4
Alerts booth leads. Rising defect patterns reach the booth while they can still be fixed.
1000+
Industrial clients running iFactory
99.9%
Platform uptime for continuous paint lines
6-12 wks
From racked server to live repair routing
FREQUENTLY ASKED QUESTIONS

What Plant Managers Ask About Paint Defect Detection

Which paint defects can AI vision detect?
Tunnel cameras and deflectometry can find surface defects such as runs and sags, orange peel, craters, dirt nibs, solvent pop and many scratches and dents. Models are trained on your own colours and finishes, since dark, light and metallic paints reflect light differently.
How does it link a defect to a root cause?
Each body carries the booth temperature and humidity, robot, film build and material batch from the time it was painted. The system compares defect classes with that data and ranks likely causes. A process engineer confirms the cause before changes are made.
Who decides the repair route?
Your quality team writes the rules, for example which defect sizes and zones can be sanded and polished and which need a spot repair or repaint. iFactory applies those rules to each body, and repair staff can override a route when they see something different.
Does it measure film thickness?
Cameras do not measure dry film thickness. iFactory links readings from your film build gauges and inline systems to each body, so film build can be compared with defects such as runs, sags and solvent pop.
Does it work on parts other than car bodies?
Yes. The same approach suits painted appliances, machinery panels, plastic parts and other coated products. Coating inspection on smaller parts often uses fixed cameras on the conveyor instead of a full tunnel.
How do we start?
Start with one tunnel and your top three defect classes. Collect images, compare system calls with inspectors, then switch on root cause alerts and repair routing. Our support team can plan that pilot with you.

Fix the Panel and the Booth That Painted It

Classify every paint defect, link it to booth humidity and temperature and send each body to the right repair. The full system is delivered turnkey and goes live in 6 to 12 weeks.
Example shift summary · Paint shop
Bodies inspectedEvery body, every panel
Defects classifiedBy type, size, layer and zone
Root causesLinked to booth and robot data
RepairsRouted by defect type
Every repair traceable to its defect

Share This Story, Choose Your Platform!