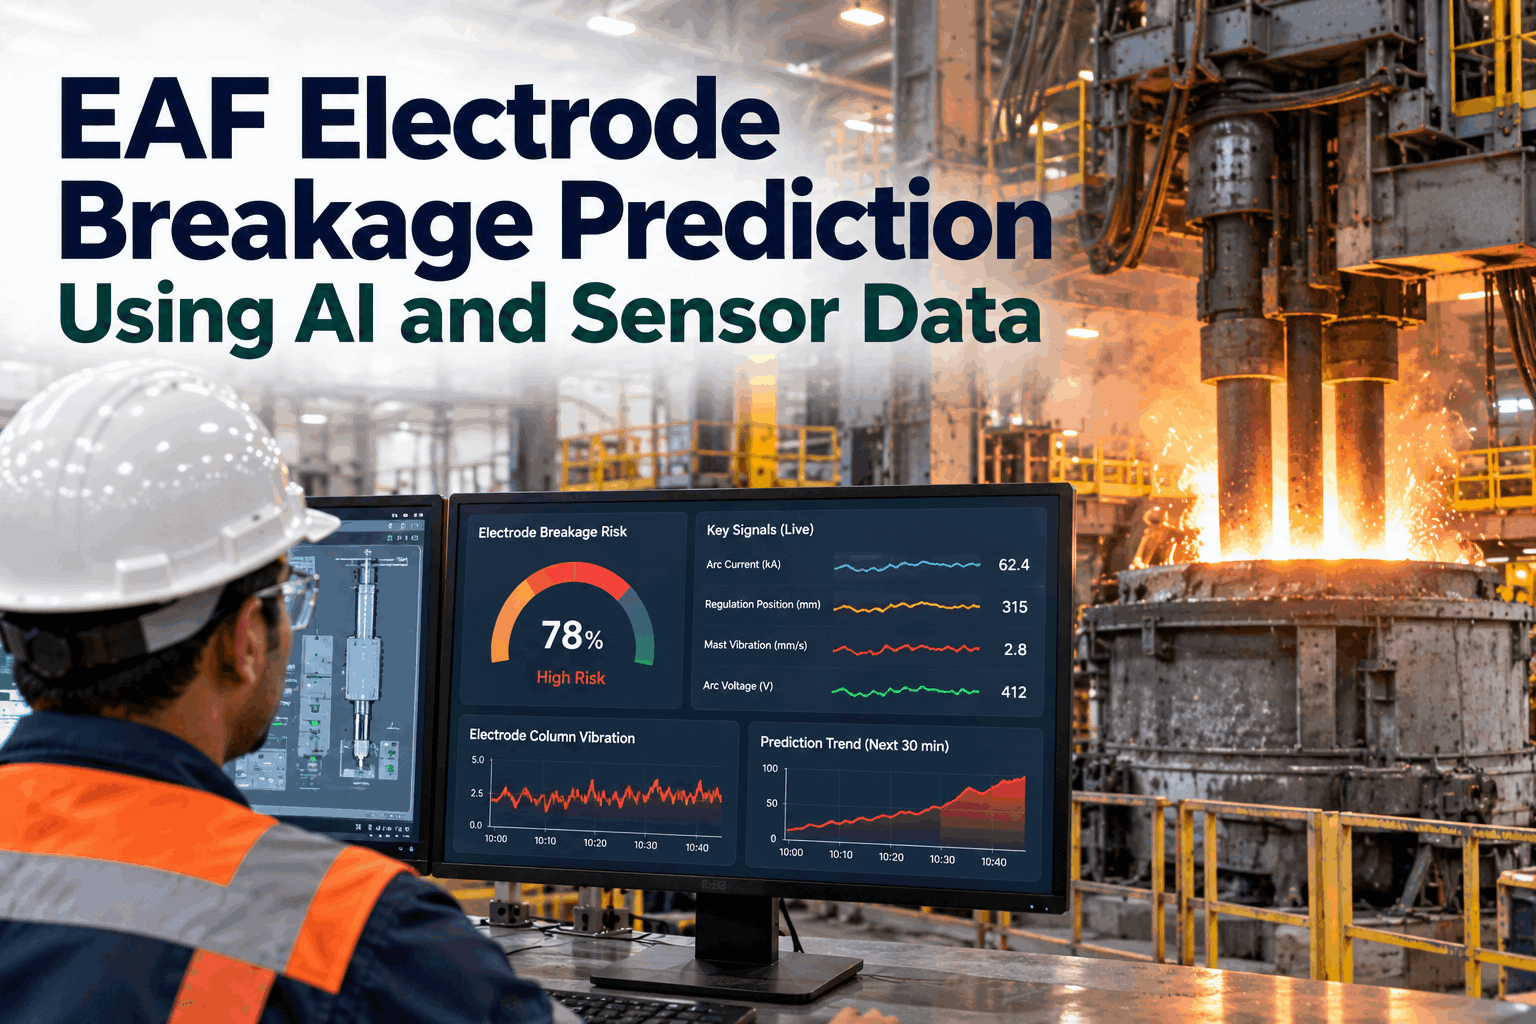
EAF Electrode Breakage Prediction Using AI and Sensor Data

By James C on October 16, 2026

eaf-electrode-breakage-prediction-ai-sensor-data

A graphite electrode that breaks mid-heat stops the furnace, puts crews to work near a hot shell and wastes graphite that was already paid for. Most breaks are not random. They follow additions, heavy charges and columns that have been vibrating harder than usual for several heats. EAF electrode breakage prediction reads those signals and warns the melt shop in time to act at the next tap. See it on furnace data in a short melt shop demo.

PREDICTIVE AI · MELT SHOP

Hear About an Electrode Break Before It Stops the Heat

iFactory models arc stability, regulation behaviour and column vibration for each phase. When breakage risk rises, the voice agent speaks to melt shop headsets and logs a check task for the next tap.

Voice alert · EAF 1Risk high
"Electrode B column risk high."
A0.22
B0.78
C0.31
Column B vibration2.4× baseline
Regulation moves, BUp 35% this charge
Last addition on B3 heats ago
Check task logged: inspect column B joint at next tap
WHERE BREAKAGE FITS

Small Share of Graphite, Large Share of Trouble

In a well-run shop, most electrode consumption is continuous. The tip is used up by the arc and the sides oxidise in the furnace atmosphere. A widely cited industry estimate puts that at about 95% of consumption. The other 5% or so is discontinuous: breaks at the socket, pin or body, butt losses and spalling. That share is small in tonnes of graphite, but each break also costs furnace time, crane time and a risky job near the shell. That is why breakage is worth predicting on its own. Our melt shop team can help you separate the two in your own records.

Continuous, about 95%~5%
Continuous: tip sublimation and sidewall oxidationDiscontinuous: breaks, butt losses and spalling
Body breakThe electrode snaps along its length, often from side impact or bending.
Socket breakCracks start in the threaded socket, where bending stress is highest.
Pin breakThe connecting pin fails, often after poor tightening or thermal stress.
Tip lossA piece of the hot tip falls into the bath after cracking or spalling.
WHY BREAKS HAPPEN

Six Causes, and What Each Looks Like in the Data

Industry experience points to two leading causes: the way electrodes are added, and the way scrap is mixed and loaded, including nonconductive material in the charge. Studies of column joints add thermal stress, over-tightening, vibration and side impact from the charge or furnace tilting. Each cause leaves a different trace in the data, which is what makes prediction possible. Map these causes to your furnace in a breakage review session.

01
Addition techniqueDirty threads, wrong torque or a joint left loose.Data: breaks cluster in the heats after an addition
02
Scrap mix and loadingHeavy pieces near the electrodes or nonconductive material in the arc path.Data: arc outages, current swings, mast load spikes
03
Cave-ins in bore-downScrap shifts and strikes the column as the electrodes bore down.Data: sudden hydraulic pressure changes on the mast
04
Column vibrationLong columns in tall shells can vibrate near their natural frequency.Data: rising vibration energy on the arm or mast
05
Joint thermal stressElectrode and pin expand at different rates, loading the joint.Data: breaks at joints after long, hot heats
06
Unstable regulationHunting or aggressive moves keep the column in motion.Data: frequent, large regulation corrections
THE SIGNALS

Seven Data Streams That Warn of a Break

Most of these signals already exist in a melt shop. The power system measures arc current, the regulator records every electrode move, and the mast cylinders carry pressure transducers. What is usually missing is the step that puts them together per phase and per heat, and compares them with the history of past breaks. Vibration sensors on the arms are the one item some shops need to add. Check what your furnace already records with our support team.

Signal
Source
Pattern before a break
When it matters most
Arc current per phase
Power metering
Erratic current, short circuits and arc outages on one phase
Bore-down
Regulation moves
Regulator and PLC
Hunting, large fast corrections, one phase far busier than others
Whole heat
Mast hydraulic pressure
Cylinder transducers
Sudden load changes from scrap contact or side loads
Bore-down
Arm and column vibration
Accelerometers on arm or mast
Vibration energy rising heat over heat near the column's natural frequency
Main melting
Electrode additions
Operator log or CMMS
Higher risk in the first heats after a new section is joined
After additions
Charge data
Scrap yard and bucket records
Heavy or bulky scrap, poor layering, nonconductive material
Each charge
Tilt and door events
Furnace PLC
Side loads on the column during tapping or deslagging
Tap and slag-off
RISK ACROSS A HEAT

When in the Heat a Break Is Most Likely

Breakage risk is not spread evenly across a heat. It peaks when the electrodes bore down into a fresh charge, with scrap shifting and the arc unstable. It falls once a flat bath forms and the arc is covered by foamy slag. The pattern below is typical for a scrap-based EAF, and the model learns the actual shape for each furnace. Compare it with your own heat logs in a heat profile review.

ChargingMedium
Bore-downHighest
Main meltingHigh
Flat bathLow
RefiningLow
Tap and tiltMedium

Warnings That Reach the Pulpit, Not a Report

A risk score in a dashboard is no use during bore-down. iFactory speaks the alert to melt shop headsets, names the phase and the driver, and lets the melter ask questions without taking their eyes off the furnace.

EAF 1 · Melter and iFactory
MelterWhy is B high? Arc looks normal now.
iFactoryColumn B vibration has been 2.4 times its baseline since the second bucket, and B regulation moves are up 35%. B had a section added three heats ago.
MelterCan we finish the heat?
iFactoryThat is your call. Risk falls once the bath is flat. I have logged a joint check on column B for the next tap.
EAF ELECTRODE BREAKAGE PREDICTION EXAMPLE

One Heat, One Warning, No Break

Here is an illustrative heat on a two-bucket furnace. The times and scores are examples, but the sequence is a common one: a column that was joined recently, a heavy second charge and vibration that builds during bore-down. The point is that the warning arrives while there is still a choice, not after the break. Ask our support team to replay a heat from your own history.

Start
0.30
Heat beginsColumn B was joined three heats ago, so the model starts it at a slightly higher base risk than A and C.
Min 4
0.42
Bucket 1 bore-downB regulation moves rise, but vibration stays near normal. No alert.
Min 23
0.78
Bucket 2 bore-downHeavy scrap shifts, mast pressure spikes on B and vibration reaches 2.4 times baseline. The voice agent announces the risk to the pulpit and crew.
Min 25
0.70
Melter decidesThe melter switches to the shop's gentler bore-down profile, as standard practice allows, and watches B closely.
Min 41
0.35
Flat bathRisk falls as the arc is covered. The heat is tapped without a break.
At tap
Check
Joint inspectedThe crew finds the last joint on B slightly open and re-tightens it to the supplier's torque. The finding is logged against the column.
EAF ELECTRODE BREAKAGE PREDICTION TEMPLATE

An Electrode Event Log Worth Keeping

A model learns from past breaks, so the quality of your break records decides how good the predictions can be. Many shops log a break as a single line in the shift report. The fields below turn each break, and each near miss, into a record the model and your engineers can use. Start logging them now, even before any AI is in place. Get a ready-made version in a setup call.

Heat and furnaceHeat number, furnace, time in heat
Phase and columnA, B or C, and where in the heat
Break typeBody, socket, pin or tip
Break positionWhich joint or distance from the tip
Last additionHeats since, who joined it, torque used
Electrode lotSupplier, grade and batch
ChargeBucket number, scrap mix, anything unusual
DelayFurnace minutes lost and graphite lost
Near missesAlerts acted on, and what was found at the tap
COST AND ROI

How to Size the Value of Fewer Breaks

The cost of a break has four parts: lost furnace time, the graphite left in the bath or scrapped, crane and crew time to recover the column, and the safety exposure of working near the shell. Furnace time is usually the largest, and only you know what a minute of your furnace is worth. The example below uses assumed inputs to show the arithmetic. Replace each one with your own figures, and our team can help you complete the case.

Mid-heat breaks per year10, assumed
Furnace delay per break35 minutes, assumed
Furnace time lost per year10 × 35 = 350 min, about 5.8 hours
Breaks avoided if half are predicted and prevented5
Furnace time recovered5 × 35 = 175 min, about 2.9 hours

Multiply the recovered time by the value of a furnace minute in your shop, then add the graphite and recovery labour saved. Leave the safety benefit out of the sum, but keep it in the case.

BEST PRACTICES

Prediction Works Best Alongside Good Practice

A warning helps most when the basics are in place. These habits reduce breaks on their own and make the remaining ones easier to predict, because the data is cleaner and the causes are fewer. If you want a second opinion on your practices, talk to our melt shop specialists.

On the electrodes
  • Clean threads and pins before every joint
  • Tighten to the supplier's torque, not more
  • Record who joined each section and when
  • Track breaks by supplier, grade and batch
On the charge
  • Keep heavy scrap away from the electrode path
  • Keep nonconductive material out of the buckets
  • Layer buckets the same way every time
  • Record anything unusual in each charge
On the furnace
  • Keep regulation tuned and check for hunting
  • Check column vibration on tall shells
  • Aim oxygen away from the electrodes
  • Inspect arms, clamps and holders on schedule
TURNKEY AI DEPLOYMENT

Models, Voice Alerts and AI Server in One Package

iFactory delivers electrode breakage prediction as a turnkey bundle. A pre-configured NVIDIA AI server ships racked and ready with the models, furnace data connectors and the voice agent pre-loaded, so high-speed furnace data is processed on site. You rack it, plug in power and Ethernet, and the AI is live. To scope it for your melt shop, request a turnkey quote.

What's Included
  • Pre-configured NVIDIA AI edge server, racked and ready
  • Connectors for power metering, regulator and furnace PLC
  • Arm and mast vibration sensors where needed
  • Breakage risk models trained on your heat history
  • Voice alerts to melt shop headsets and the pulpit
  • Check tasks logged to the CMMS for the next tap
  • 24×7 remote monitoring of models and hardware
Live in 6–12 weeks
Wk 1–4
Connect and Collect

Server installed, furnace signals connected, past breaks and additions loaded.

Wk 5–8
Train and Shadow

Models trained per furnace and run silently, with risk scores checked against real events.

Wk 9–12
Go-Live and Training

Voice alerts switched on, thresholds agreed, melters and crews trained.

HOW iFACTORY FITS

Breakage Prediction Built for the Melt Shop

iFactory's Predictive AI and voice agent are designed for the pace of an EAF, where decisions happen in minutes and nobody has time to read a screen. Our support team can walk you through a pilot plan.

1
Scores each column. Risk is calculated per phase, per heat stage, from arc, regulation and vibration data.
2
Names the driver. Every alert says which signal moved and how far from normal.
3
Speaks to the crew. Alerts go to headsets and the pulpit, and the melter can ask why.
4
Closes the loop at tap. A check task is logged for the next tap, and findings feed back into the model.
1000+
Industrial clients running iFactory
99.9%
Platform uptime for continuous melt shops
6-12 wks
From racked server to live breakage alerts
FREQUENTLY ASKED QUESTIONS

What Plant Managers Ask About EAF Electrode Breakage Prediction

Can electrode breakage really be predicted?
Not every break, but many give warning signs. Breaks often follow recent additions, heavy or poorly layered charges, unstable regulation and rising column vibration. A model that watches these signals together, per phase and per heat stage, can flag a rising risk minutes ahead, which is enough time to change the bore-down approach or plan a joint check at the next tap.
What data does the model need?
Arc current per phase, regulation moves and mast hydraulic pressure, which most furnaces already record. Vibration from accelerometers on the arms or masts adds a strong signal where available. The model also needs a record of past breaks, additions and charges, so it can learn what came before each event.
How does it differ from consumption tracking?
Consumption tracking measures how much graphite is used per tonne over time, which is mostly tip and side loss. Breakage prediction looks for the short-term signs that a column is about to fail. The two use some of the same data, but breakage prediction works in minutes and heats, not weeks.
What happens when the voice agent raises an alert?
It names the column, the phase of the heat and the main driver, such as vibration or regulation activity. The melter decides what to do, whether that is a gentler bore-down profile or simply closer watching. The agent logs a check task for the next tap so the column is inspected before the next heat.
Does it work with different electrode suppliers or grades?
Yes. Supplier, grade and batch are recorded as inputs, so the model can tell whether one lot behaves differently. After a change of supplier or grade, the model takes some heats to settle, and the shadow period is the right time to check it.
How do we start?
Begin with your break records. Collect the heats where breaks happened, along with additions and charge data, and connect the furnace signals. The model then runs in shadow mode for several weeks before any alert reaches the crew. Our support team can plan that first phase with you.

Fewer Broken Columns, Fewer Lost Heats

Connect your furnace signals, load your break history and let iFactory warn the melt shop while there is still time to act. The full system is delivered turnkey and goes live in 6 to 12 weeks.
Example shift summary · EAF 1
Heats scoredEvery column, every phase
Voice alertsEach with a named driver
Joint checks at tapLogged to the CMMS
FindingsFed back into the model
Every alert and check traceable

Share This Story, Choose Your Platform!