Most FMEAs are written once, under deadline, and then opened again only when an auditor asks for them. That is backwards. A failure mode and effects analysis is supposed to be a living record of what can go wrong with a design or process and what stops it, updated as the product changes. When it is treated as a one-time document, the next design change, the next supplier switch or the next field issue finds nothing waiting for it. Quality engineers rebuilding that habit can see how iFactory AI keeps DFMEA and PFMEA linked to live production data before the next APQP gate review.
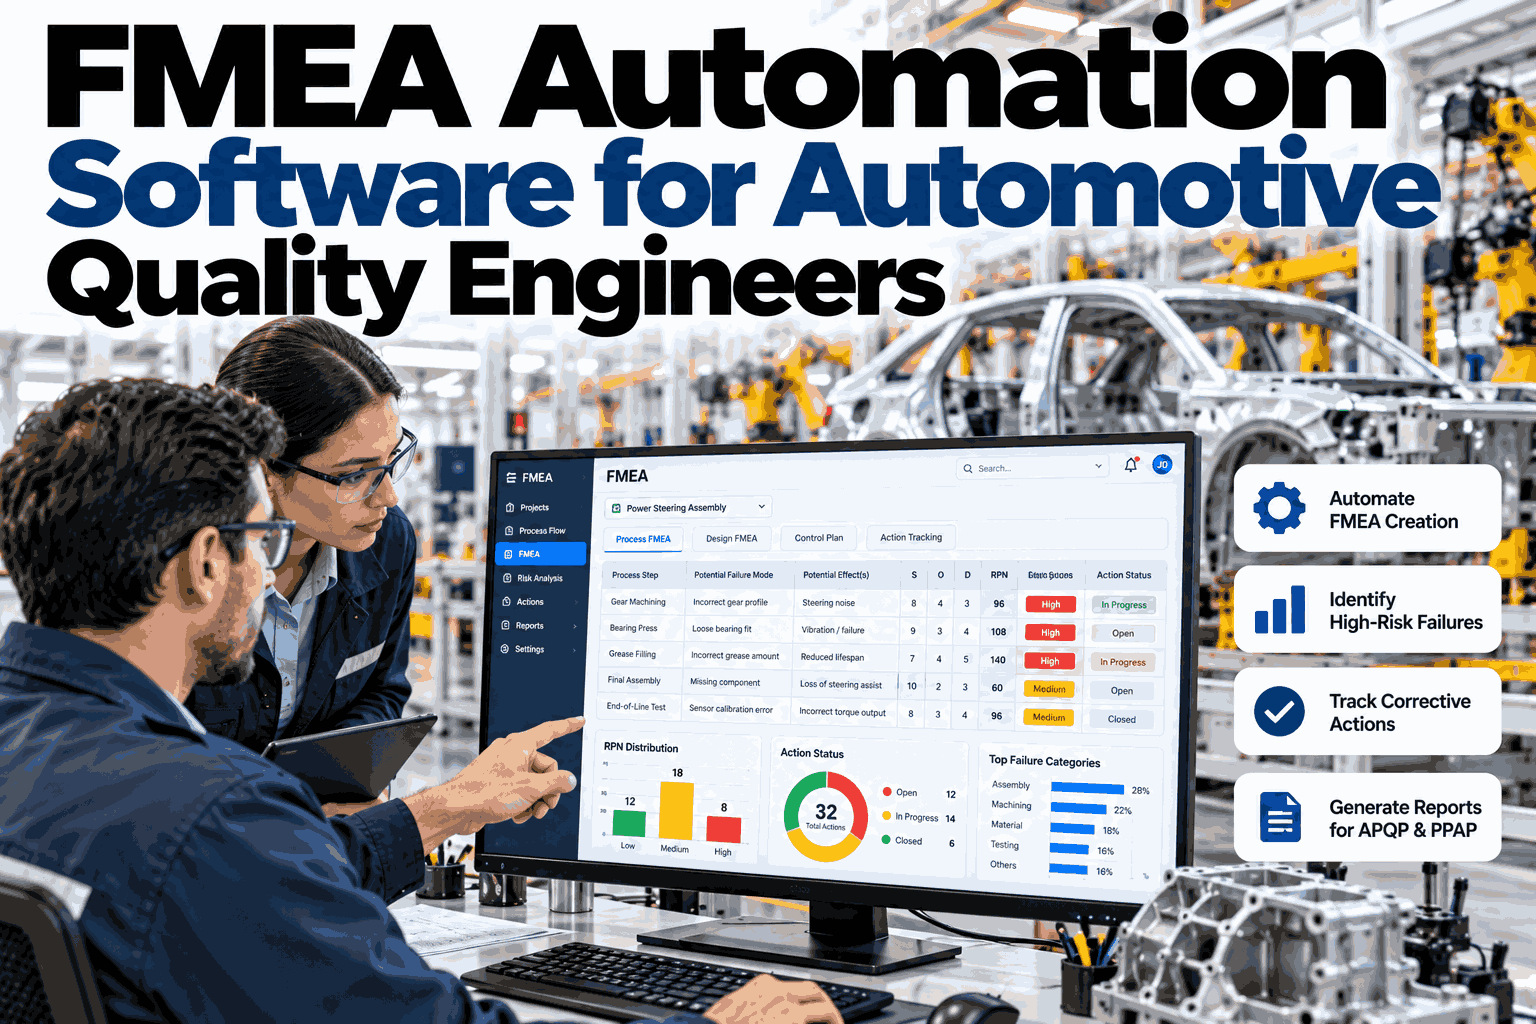
FMEA Automation Software for Automotive Quality Engineers
Keep DFMEA and PFMEA current, scored to AIAG-VDA, and connected to the production data that proves the controls still work.
The Document That Stopped Living
An FMEA built once and filed away loses its purpose quickly. Three patterns show when that has happened.
Severity, occurrence and detection ratings have not changed since launch, even after field issues.
Listed controls do not match what SPC and inspection actually check on the floor today.
The document is opened only when a customer or certification audit requires it.
None of these make the FMEA wrong on day one. They make it stale by month six, which is when it stops protecting anyone.
DFMEA and PFMEA, Side by Side
The two documents ask different questions and feed different stages of the product. Confusing them is a common source of weak analysis.
Reading the AIAG-VDA Action Priority
The current AIAG-VDA handbook replaced the older risk priority number with an action priority of high, medium or low, built from severity, occurrence and detection together rather than a single multiplied score. Confirm the latest edition and tables for your programme, since guidance is revised periodically.
Action is required. Work does not proceed without a defined response.
Action is recommended, or a justification is documented for not acting.
Action is optional, based on engineering judgement.
See Your FMEA Scored and Linked to Production
Book a 30-minute session and iFactory AI will show how action priority, control plans and live SPC data are kept in step with each other.
Where a Library Saves Real Time
Most failure modes repeat across similar parts and processes. A structured library turns a blank page into a starting point.
Standard wording for common part functions, kept consistent across programmes.
Prior failure modes for similar features, with their known effects.
Typical causes and the prevention or detection controls already proven to work.
A library speeds up drafting, but engineers still judge whether each entry truly applies. Copy-paste without review is how an FMEA quietly loses its value.
Tying FMEA to the Control Plan
A control that exists only in the FMEA, and not in the control plan or on the floor, protects nobody. Check the chain runs both ways.
FMEA names a control
A prevention or detection method is identified for a specific failure mode.
Control plan records it
The same control appears with its method, frequency and reaction plan.
The floor executes it
SPC charts, gauges or inspection steps carry out the control as written.
Data proves it works
Process data confirms the control is catching or preventing what it claims to.
Triggers That Should Reopen the FMEA
An FMEA should not wait for a scheduled review to change. These events should reopen it immediately.
| Trigger | What to Reassess |
|---|---|
| Design change | New or changed failure modes from the revised geometry or material |
| Process change | New equipment, tooling or parameters that affect occurrence or detection |
| Supplier change | Incoming quality risk tied to the new source |
| Field issue or warranty claim | Whether the failure mode was anticipated and scored correctly |
| Customer complaint | Detection effectiveness and whether controls caught the issue earlier |
Where iFactory AI Fits
iFactory AI keeps the FMEA, control plan and floor data connected, so the document reflects what is actually happening, not just what was planned at launch.
Linked control plans
Each FMEA control maps to its control plan entry, so gaps between the two are visible.
Live detection evidence
SPC and inspection data show whether a listed detection control is actually catching defects.
Reopen triggers
Design, process and supplier changes flag the affected FMEA lines for review.
Ask in plain language
Ask which high action priority items have no confirmed detection evidence and receive the list.
iFactory AI arrives pre-configured on an NVIDIA server that ships racked and ready with software pre-loaded. Scope covers cabling, network, ERP and MES integration, team training and 24x7 remote monitoring.
Frequently Asked Questions
What is the difference between DFMEA and PFMEA?
DFMEA examines how the design itself could fail and is owned by design engineering, while PFMEA examines how the manufacturing process could fail and is owned by manufacturing and quality engineering. Both feed the APQP process but at different stages. You can watch both document types linked to live data in a demonstration session.
How does AIAG-VDA action priority differ from the old RPN?
Action priority groups severity, occurrence and detection into high, medium or low using defined tables, instead of multiplying the three ratings into a single risk priority number. The aim is to focus attention on severity-driven risk rather than letting a low severity, high occurrence item mask a true safety concern. Confirm the exact tables in the current handbook edition for your programme. To review your scoring approach, request a scoring alignment session with the iFactory AI team, or ask support about supported FMEA formats.
Can an FMEA library really be reused across programmes?
Yes, for function, failure mode and typical causes, but occurrence and detection ratings should be rechecked for the specific process and controls in place. A library speeds up drafting, not the engineering judgement behind the scores. A short product tour of the library structure shows how this balance is kept.
How do we know if a listed control is actually working?
Compare the control plan entry against real inspection or SPC data for that characteristic, and check whether detection events match what the FMEA claims the control catches. A control with no supporting data is a paper control. See how control evidence is tracked against the FMEA in a guided walkthrough.
When should an FMEA be reopened outside the normal review cycle?
Reopen it at a design change, process change, supplier change, field issue or customer complaint, rather than waiting for the next scheduled review. Each of these can introduce or reveal a failure mode the original analysis did not anticipate. Schedule a walkthrough of reopen triggers to see how changes are flagged automatically.
Make the FMEA a Living Document Again
iFactory AI keeps DFMEA and PFMEA connected to control plans and real production data. Book a walkthrough to see it built around your own programme.