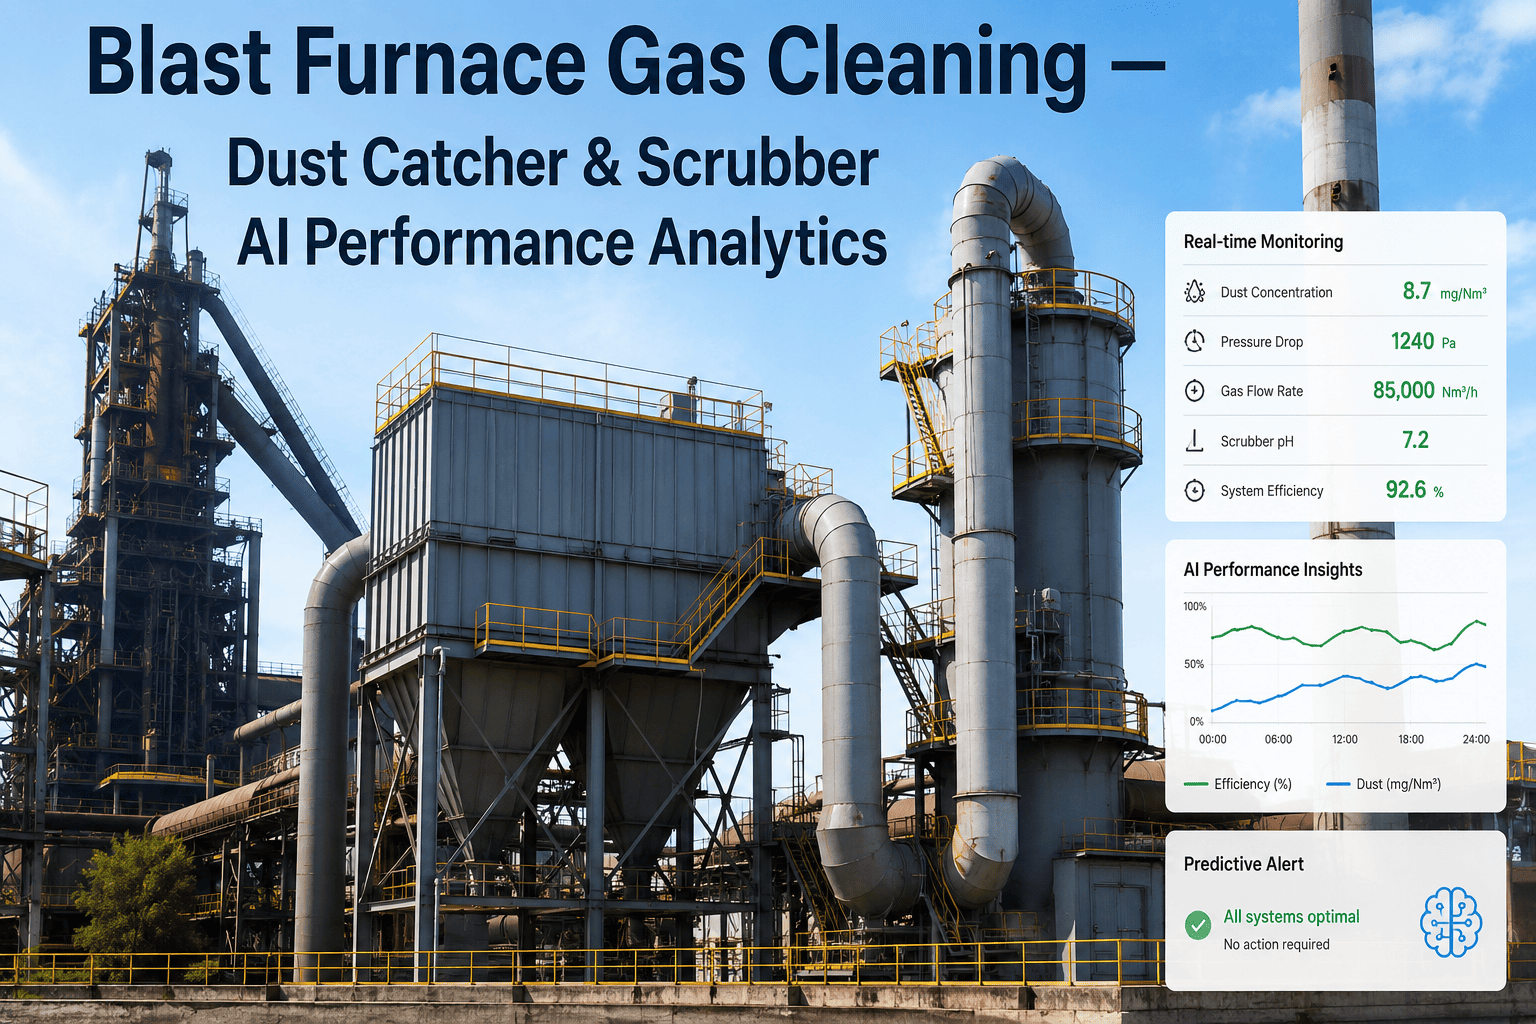
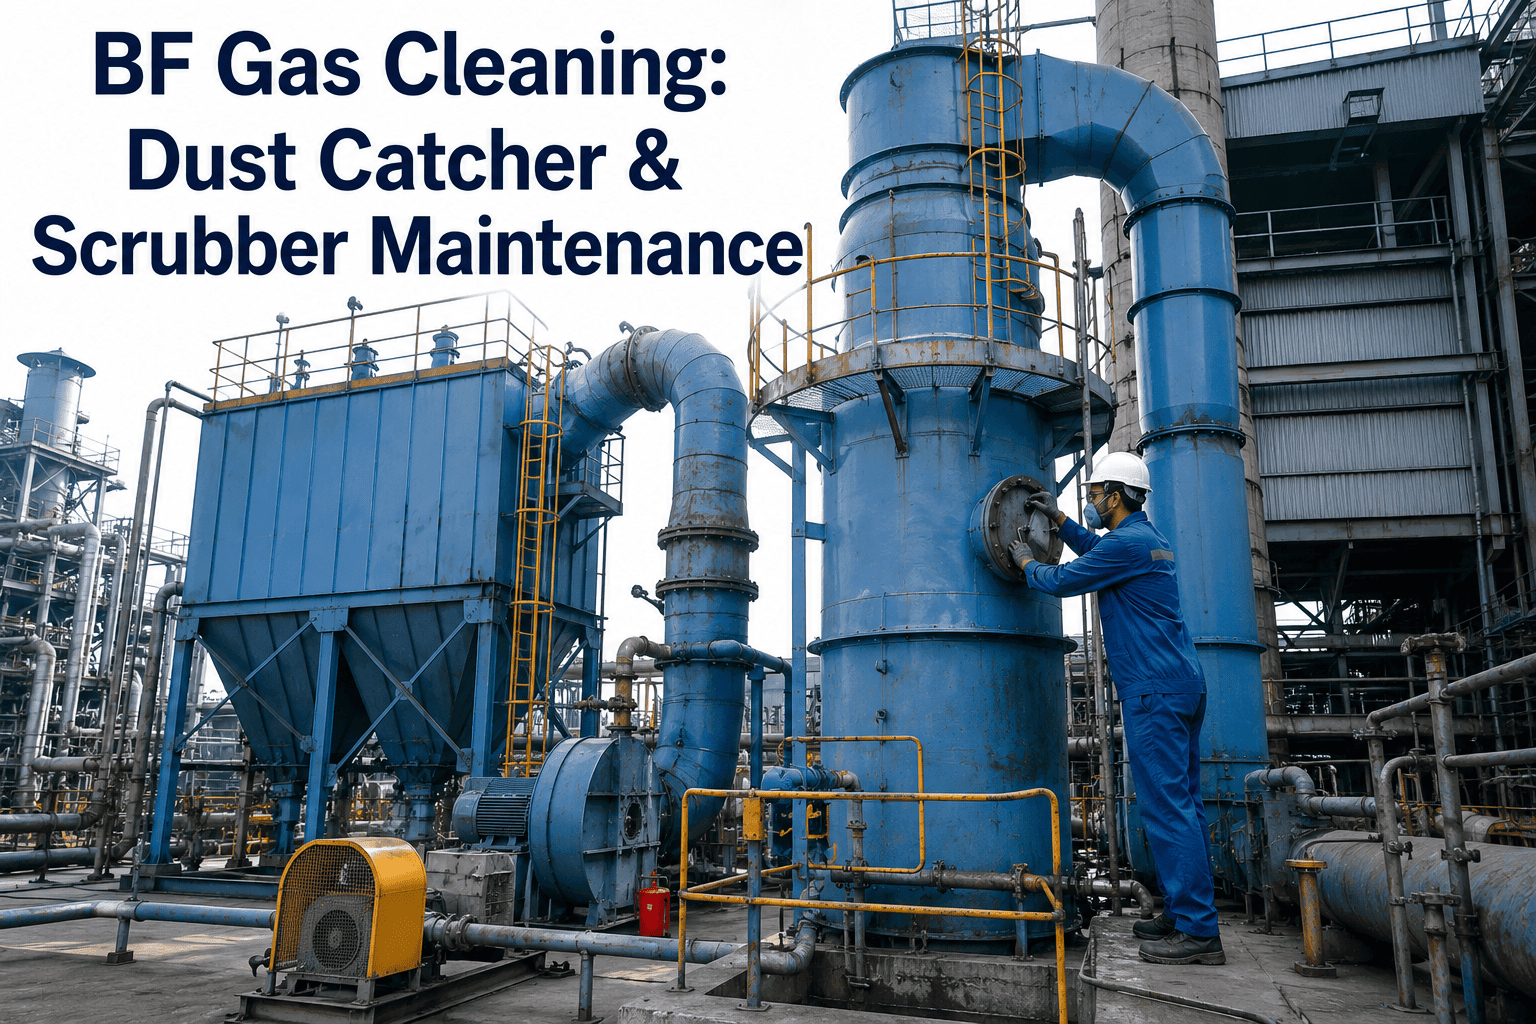
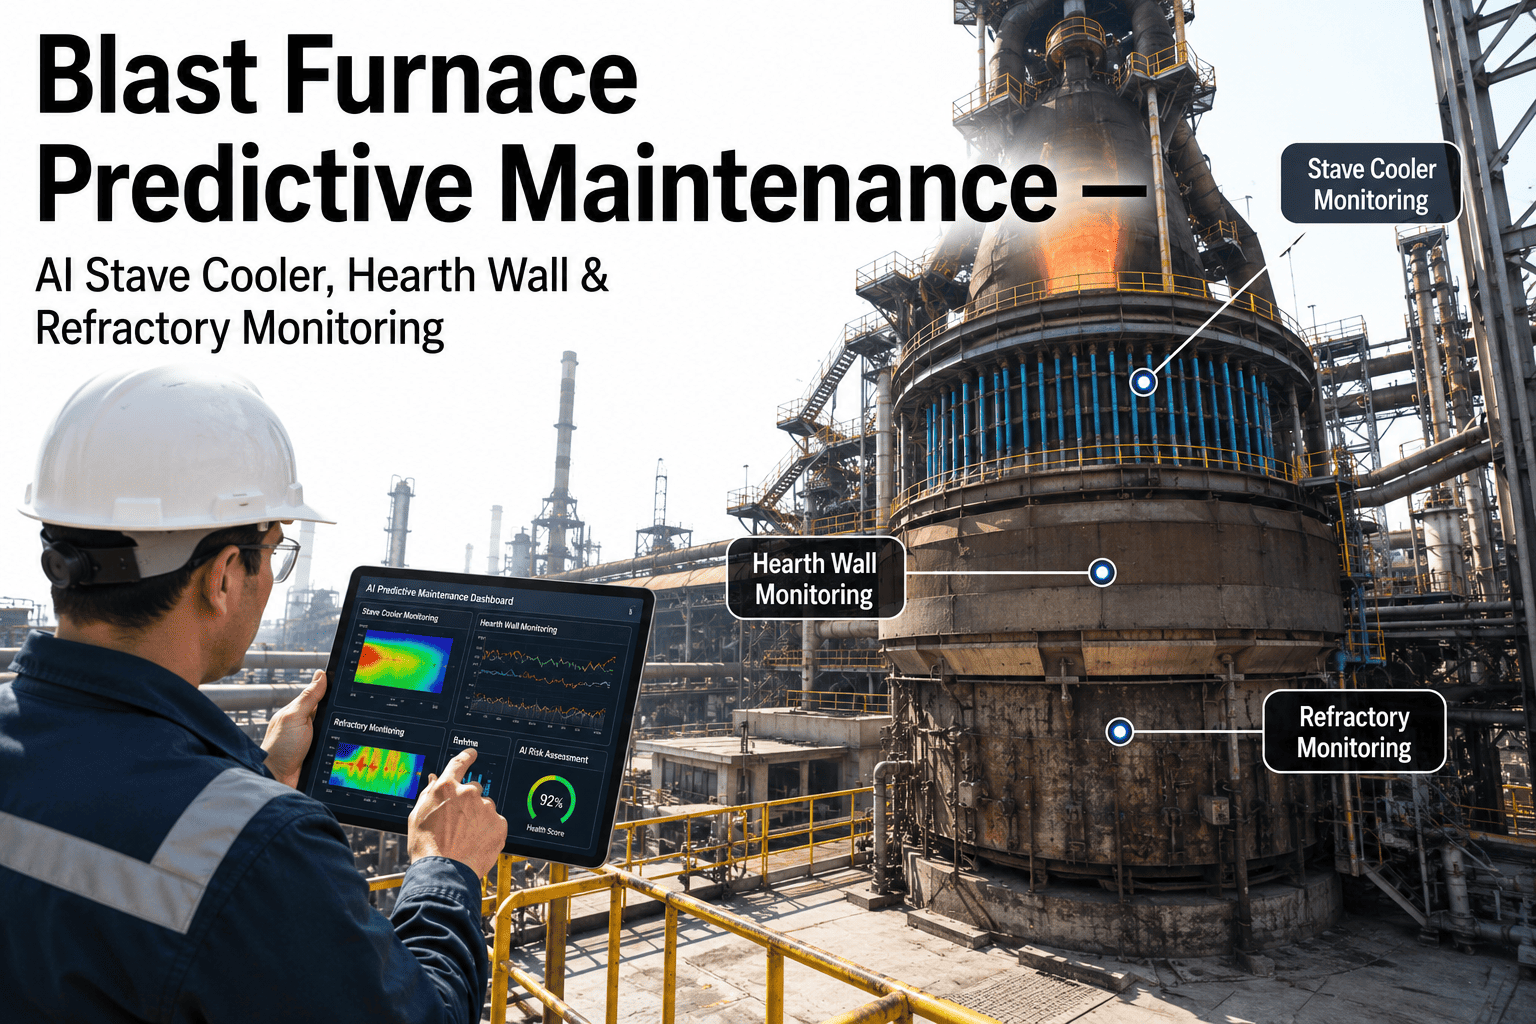
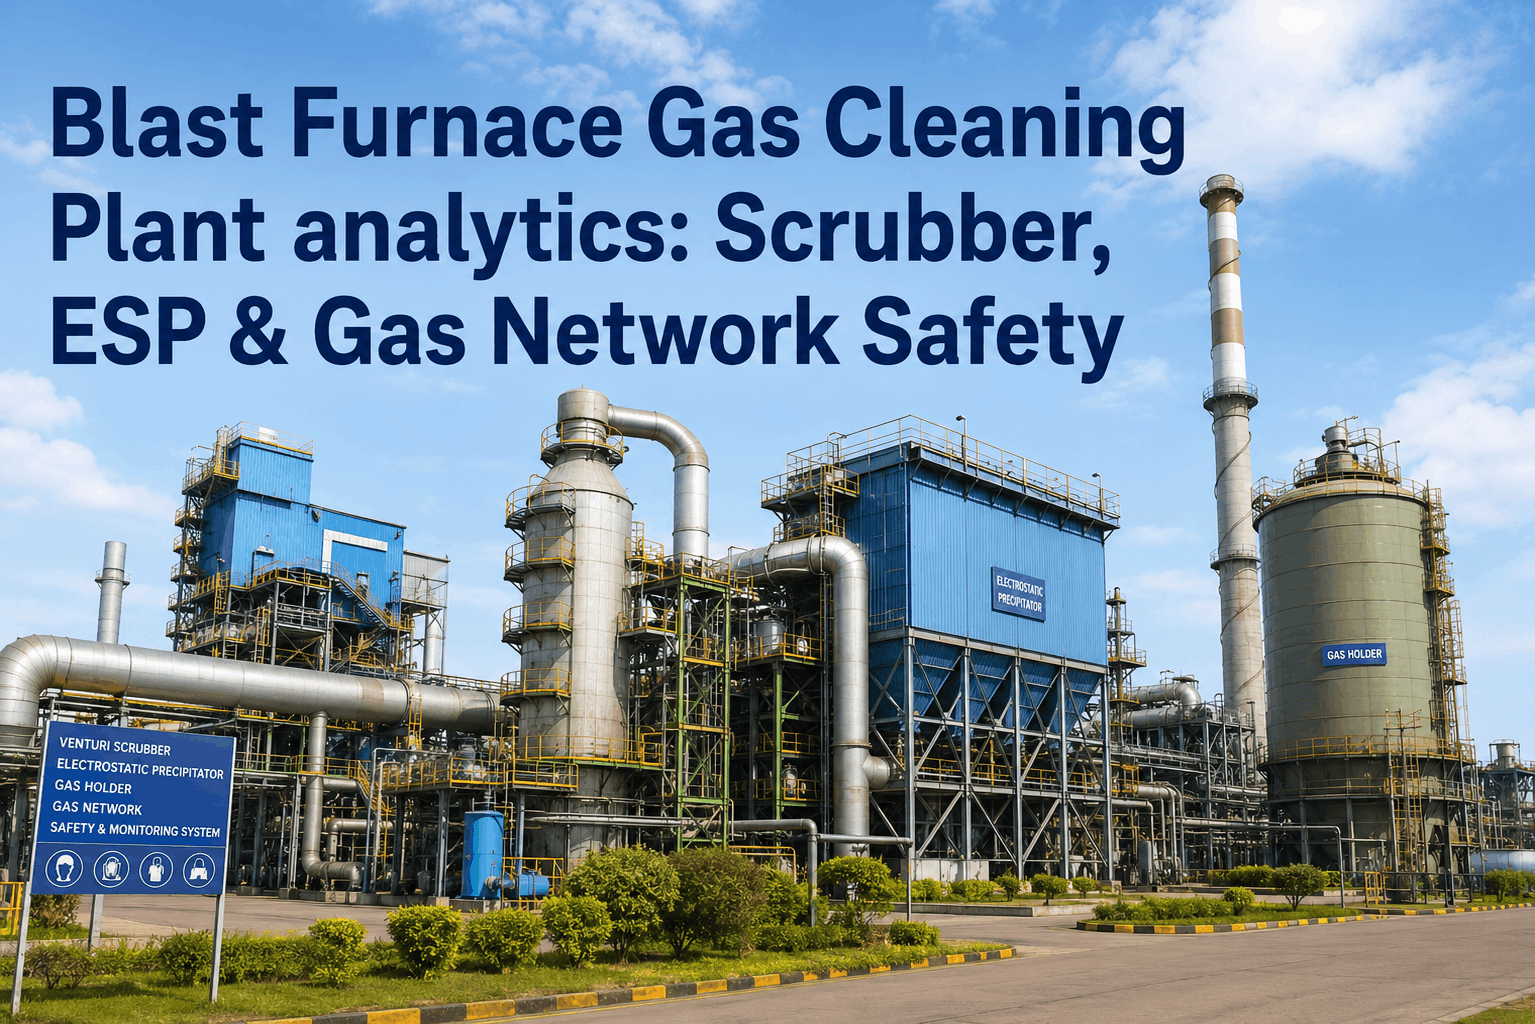
Blast furnace gas cleaning systems fail quietly. A dust catcher losing capture efficiency, a scrubber pressure drop drifting outside range, or a gas main slowly filling with fines rarely trips an alarm before it becomes a hot stove firing problem or a turbo blower trip. Maintenance teams inspecting BF gas systems on fixed weekly rounds routinely miss the early stages of scrubber throat wear, venturi erosion, and dust catcher hopper bridging that eventually force unplanned gas cleaning outages. iFactory's AI Gas Cleaning Analytics Platform continuously reads pressure differential, dust loading, and flow data across your dust catcher, scrubber, and gas main network to catch degradation weeks before it threatens clean gas quality. Book a demo to see live BF gas cleaning analytics running on a working furnace.
21%
Average reduction in unplanned gas cleaning outages within the first two quarters
6–9 wks
Typical lead time gained on scrubber throat and venturi wear before failure
99.5%
Clean gas dust loading compliance maintained across monitored furnaces
$640K
Median annual value from avoided gas main blockages and hot stove trips
A Blocked Gas Main Doesn't Announce Itself Until Hot Stove Firing Is Already Compromised
iFactory tracks dust catcher differential pressure, scrubber water balance, and gas main velocity trends together, so a slow drift toward blockage or scrubber inefficiency is flagged as a pattern — not discovered during a firing upset.
Why Gas Cleaning Systems Are the Most Underwatched Circuit on the Blast Furnace
Gas cleaning sits between the furnace top and everything downstream that depends on clean, cool BF gas: hot stoves, power generation boilers, and the gas main network itself. Because it rarely causes a direct production stoppage on its own, it is often the last system reviewed during daily rounds — until a downstream consequence forces attention.
Zone 1
Dust Catcher
Hopper bridging, uneven dust discharge, and gradual capture efficiency loss increase downstream fines loading before any alarm typically fires.
Venturi Scrubber
Zone 2
Throat erosion and nozzle wear reduce pressure drop efficiency, letting fines pass through into clean gas without a clear single-point failure.
Zone 3
Gas Main Network
Low points and dead legs accumulate fines over months, narrowing effective diameter until velocity and pressure readings finally show the restriction.
Zone 4
Hot Stove Interface
Dirty gas reaching the stove burner accelerates checker fouling and combustion inefficiency, feeding problems back into refractory life.
Each of these four zones is typically instrumented on its own, reviewed on its own schedule, and reported on its own trend screen. A maintenance manager checking dust catcher differential pressure at the start of a shift has little visibility into whether that reading correlates with a slow change happening downstream at the gas main or hot stove interface. That separation is precisely where early degradation signals get lost, and it is the gap iFactory's correlated monitoring model is built to close.
How iFactory Reads the Entire Gas Cleaning Circuit as One System
Instead of monitoring the dust catcher, scrubber, and gas main as separate instruments on separate trend screens, iFactory correlates them into a single gas cleaning health model. This is where early degradation becomes visible — a small scrubber efficiency dip combined with a slow gas main velocity change is a pattern worth investigating long before either reading alone crosses an alarm threshold. See how the correlation model is configured for your specific gas cleaning layout.
1
Continuous Differential Pressure Tracking
Dust catcher and scrubber pressure drop is trended against burden rate and blast volume, isolating true fouling trends from normal operating swings.
2
Scrubber Water Balance Modeling
Inlet and outlet water flow, along with recirculation quality, is modeled to catch nozzle wear and throat erosion before dust carryover rises.
3
Gas Main Velocity & Fines Accumulation Estimate
Velocity profiles across main segments estimate where fines are settling, prioritizing cleaning crew dispatch to the segments that matter.
4
Clean Gas Quality Forecasting
A rolling forecast of dust loading at the clean gas outlet gives maintenance planners a window to schedule intervention around production, not around failure.
5
Maintenance Work Order Sync
Flagged degradation converts directly into prioritized work orders in your CMMS, with the supporting trend data attached automatically.
iFactory vs. Standalone Instrumentation and Manual Trend Review
Most plants already have differential pressure transmitters and flow meters on the gas cleaning circuit. What's missing is the correlation layer that turns isolated readings into an early warning system maintenance teams can actually act on.
Deployment Path: From Gas Cleaning Audit to Live Analytics
iFactory deploys against your existing dust catcher, scrubber, and gas main instrumentation. There is no new hardware requirement for most furnaces already running standard differential pressure and flow transmitters.
Week 1
Instrumentation audit across dust catcher, scrubber, and gas main network; tag mapping to historian.
Week 2–3
Correlation model built against 6–12 months of historical trend data specific to your furnace.
Week 4
Live monitoring goes active; maintenance team trained on alert review and work order workflow.
Week 5–6
Forecasting thresholds tuned against real alerts; first flagged degradation trends confirmed in the field.
What Maintenance Managers Typically Miss Without a Correlated View
Most BF gas cleaning circuits already generate more data than any single maintenance manager can review manually across a full shift rotation. Differential pressure transmitters, water flow meters, and gas main velocity sensors all log continuously, but the review process is usually limited to checking whether each reading individually sits inside an acceptable range. That approach catches sudden failures well. It does not catch the slow, compounding drift that precedes most gas cleaning degradation.
A scrubber losing two or three percent of its pressure drop efficiency over eight weeks will not trip any single alarm. A dust catcher hopper that is discharging unevenly will show up as minor fluctuation in differential pressure readings that a busy maintenance team reasonably attributes to normal burden variation. Individually, each of these signals looks like noise. Together, read against six to twelve months of historical baseline for that specific furnace, they form a recognizable degradation signature — and that signature is exactly what iFactory's correlation model is built to surface.
This matters because the cost of catching gas cleaning degradation late is rarely limited to the gas cleaning circuit itself. Dirty gas reaching the hot stove accelerates checker brick fouling. Reduced scrubber efficiency increases dust loading downstream, which can affect turbo blower and power generation equipment that was never flagged as being at risk. When maintenance teams can see the gas cleaning circuit as a connected system rather than a set of isolated gauges, planning shifts from reactive outage response to scheduled intervention that fits into existing maintenance windows.
Built to Fit Existing Maintenance Workflows, Not Replace Them
iFactory is designed to sit alongside the maintenance processes your team already runs, rather than asking a plant to adopt an entirely new monitoring platform. Trend data, alerts, and work order recommendations are delivered into the systems your maintenance planners, reliability engineers, and shift supervisors already check daily.
Historian Compatibility
Reads directly from OSIsoft PI, AVEVA Historian, and equivalent platforms without requiring a parallel data pipeline or duplicate instrumentation.
CMMS Work Order Sync
Prioritized findings post directly to your existing CMMS as work orders, with trend evidence attached so planners are not re-deriving the case for the work.
Shift Handover Reporting
A rolling summary of gas cleaning circuit health is available for shift handover review, replacing manual trend screen walkthroughs.
Configurable Alert Thresholds
Alert sensitivity is tuned to your furnace's operating history during onboarding, reducing false positives that erode trust in any monitoring system.
Stop Discovering Gas Cleaning Problems During a Hot Stove Upset
Get weeks of advance warning on dust catcher, scrubber, and gas main degradation using the instrumentation you already have.
Results from Furnaces Running iFactory Gas Cleaning Analytics
The following outcomes reflect maintenance teams that deployed iFactory's gas cleaning correlation model against their existing BF gas circuit instrumentation. Request the detailed case data for a furnace comparable to yours.
Integrated Steelworks — 2,800 m³ Furnace
Recurring scrubber throat erosion had been diagnosed only after clean gas dust loading alarms fired, typically requiring emergency outages. iFactory's water balance model flagged the erosion pattern nine weeks before the next expected failure point, allowing the replacement to be scheduled into a planned reline window instead of an emergency stop.
9 wksAdvance warning on scrubber throat erosion
$410KAvoided emergency outage cost
0Clean gas quality violations since deployment
Mini-Mill BF Operation — 1,100 m³ Furnace
Gas main fines accumulation had caused two unplanned velocity-related trips in the prior operating year, both discovered only after downstream pressure anomalies appeared. iFactory's velocity profiling identified the exact main segment accumulating fines, letting the cleaning crew target that section directly instead of a full-network inspection.
70%Reduction in gas main cleaning labor hours
2 → 0Velocity-related trips in following 12 months
$185KAnnual maintenance labor savings
Early Warning Signs Most Rounds Checklists Don't Catch
Standard shift rounds checklists are built to catch out-of-range readings, not gradual drift. The list below reflects the specific patterns iFactory's correlation model is trained to surface across the dust catcher, scrubber, and gas main circuit, based on degradation signatures observed across multiple furnace deployments.
Uneven Hopper Discharge Timing
Dust catcher discharge cycles that slowly lengthen or shorten relative to burden rate often precede hopper bridging by several weeks.
Water Balance Drift
A gradual shift in scrubber inlet-to-outlet water ratio, even within individually acceptable ranges, is a leading indicator of nozzle wear.
Segment-Level Velocity Divergence
One gas main segment trending differently from its neighbors under identical blast conditions typically points to localized fines accumulation.
Slow Pressure Drop Creep
A pressure drop increase of even a few percent sustained over multiple weeks, rather than a single spike, is the pattern most rounds checklists are not designed to flag.
Frequently Asked Questions
Does iFactory require new sensors on our dust catcher or scrubber?
In most cases, no. iFactory connects to existing differential pressure transmitters, flow meters, and water balance instrumentation already installed on the gas cleaning circuit. The instrumentation audit in Week 1 confirms tag availability, and any gaps are identified before the correlation model is built, so there are no surprises during deployment.
How does iFactory tell the difference between normal operating swings and real fouling trends?
The correlation model is trained against 6–12 months of your own historical data, so it learns what normal pressure and flow variation looks like at different burden rates and blast volumes for your specific furnace. This baseline is what allows genuine drift toward fouling or erosion to be separated from expected day-to-day fluctuation, which is the step manual trend review typically skips under time pressure.
Can iFactory pinpoint which section of the gas main is accumulating fines?
Yes. Velocity profiling across gas main segments is used to estimate where fines are most likely settling, which lets the cleaning crew target specific low points or dead legs instead of inspecting the entire network. This is one of the most requested capabilities from maintenance teams looking to reduce unnecessary cleaning labor, and you can
talk to support about how it maps to your gas main layout.
How does this integrate with our CMMS for work order generation?
Flagged degradation converts into a prioritized work order automatically, with the supporting pressure, flow, and trend data attached so maintenance planners don't need to reconstruct the evidence manually. iFactory connects to major CMMS platforms via REST API, and the integration is typically completed during Weeks 2–3 of deployment alongside the correlation model build.
What kind of advance warning should we realistically expect on scrubber or dust catcher issues?
Furnaces running iFactory's correlation model have typically gained 6 to 9 weeks of lead time on scrubber throat and venturi wear compared to waiting for a clean gas quality alarm. Actual warning windows vary by furnace age, instrumentation coverage, and historical failure patterns, which is why the historical data review in Weeks 2–3 is used to calibrate expectations specifically for your equipment.
Turn Your Existing Gas Cleaning Instrumentation Into an Early Warning System
No new hardware in most cases. No isolated trend screens. Just a correlated view of dust catcher, scrubber, and gas main health that gives your maintenance team weeks of lead time instead of a reactive scramble.