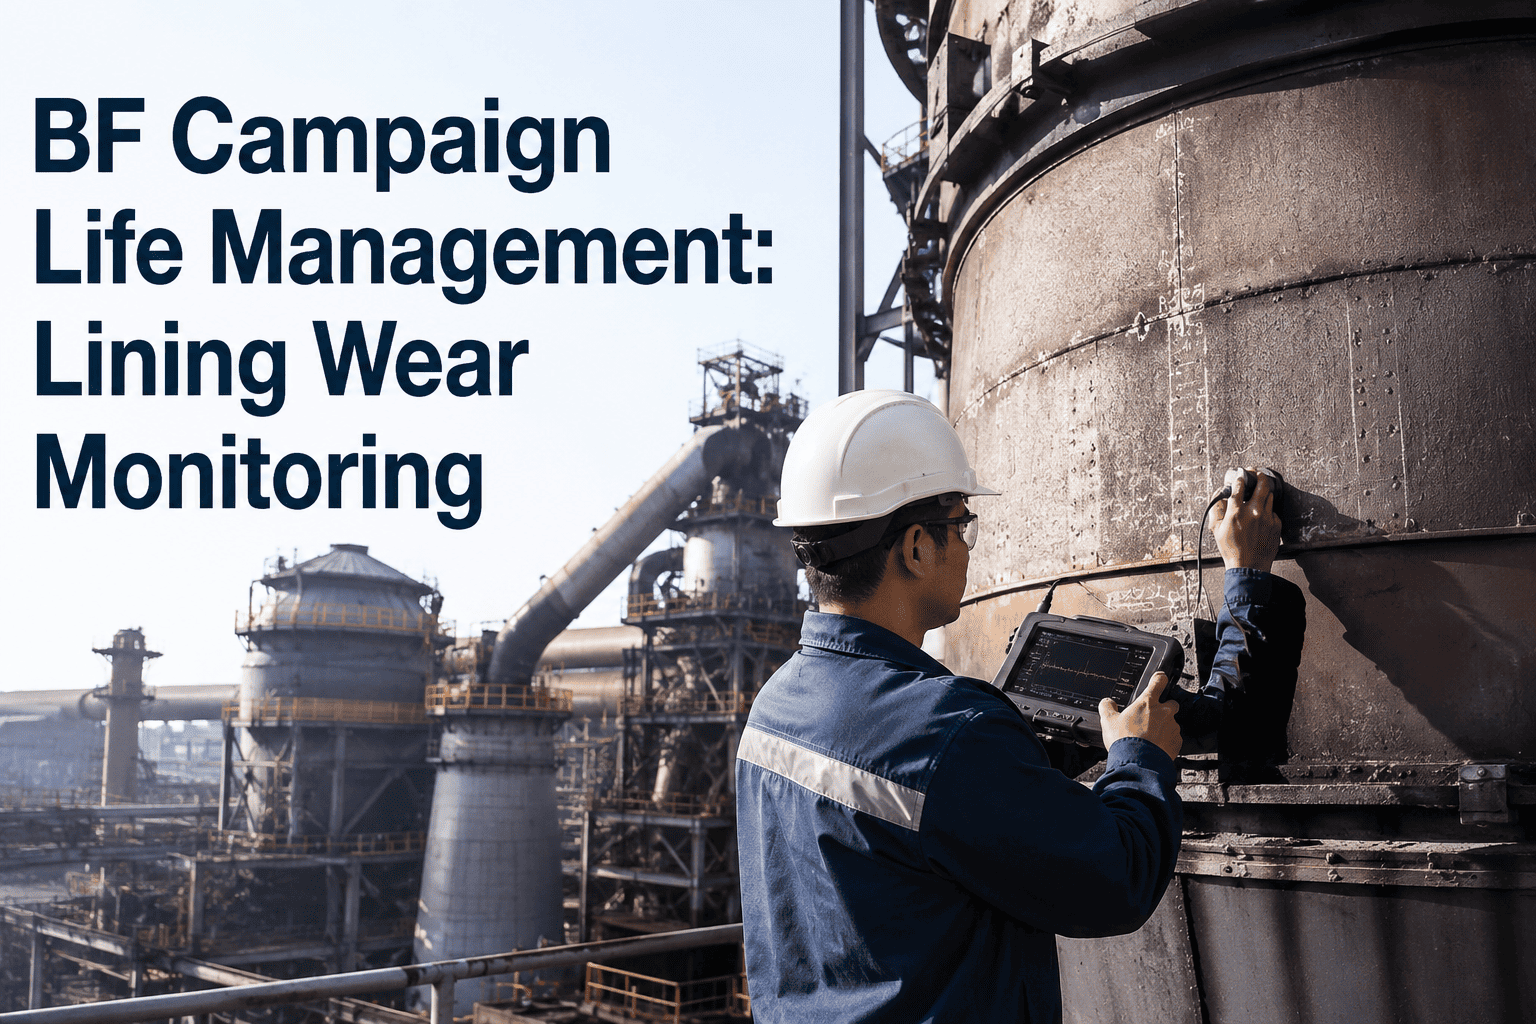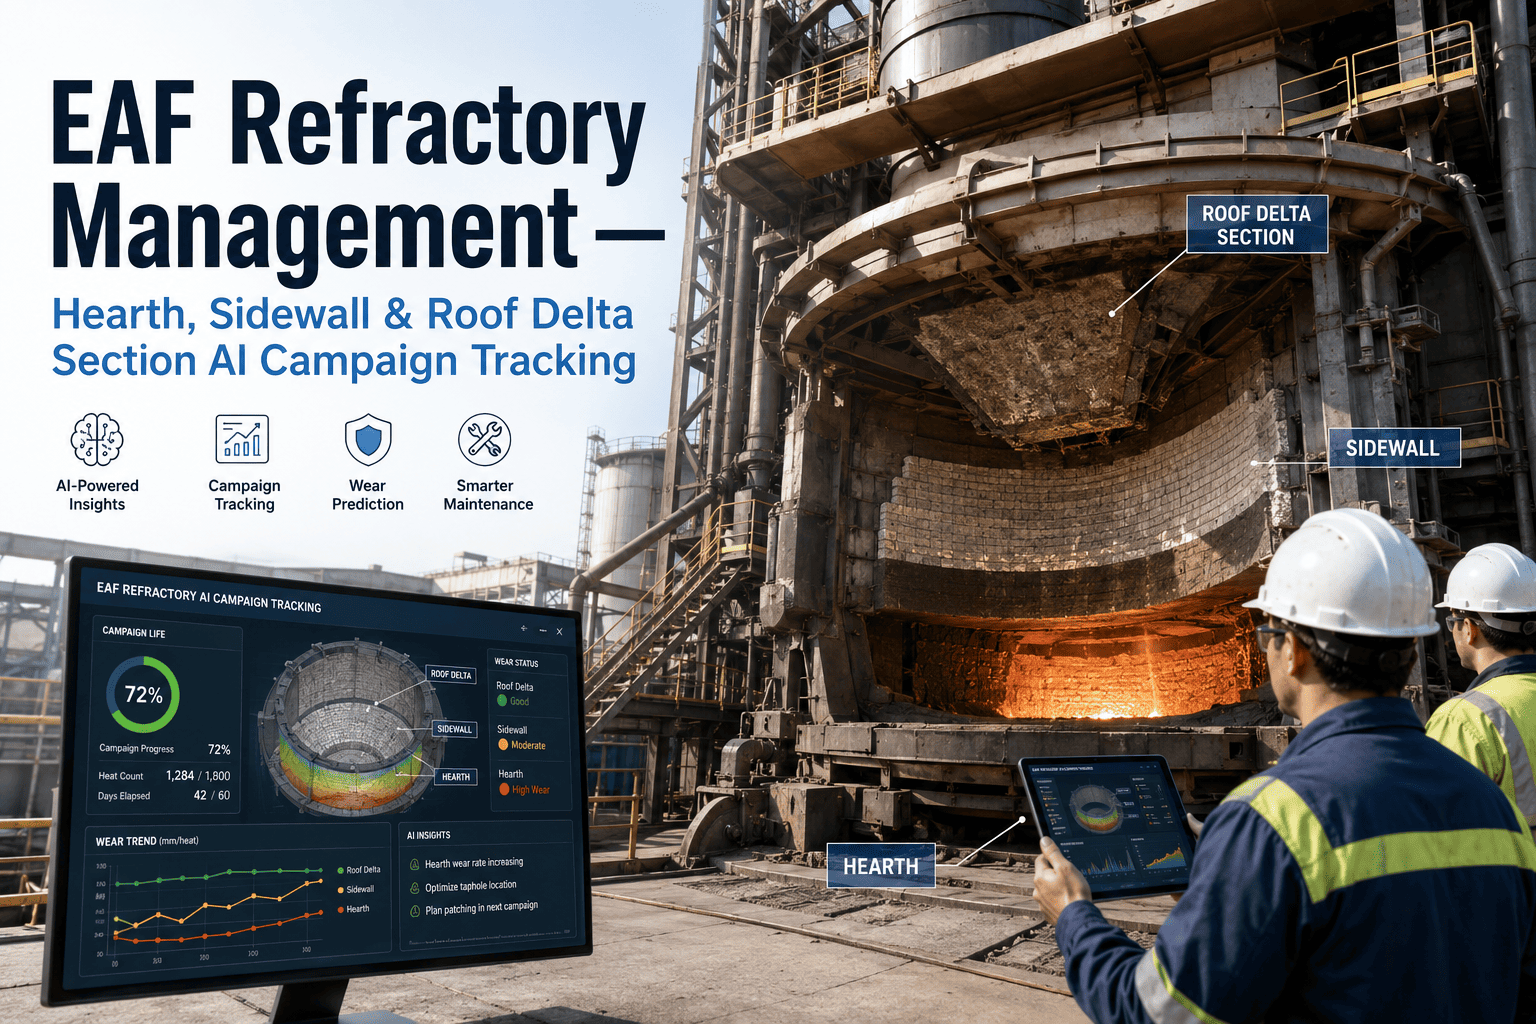
Knowing how thick a refractory lining still is matters more than almost any other single measurement in a steel plant, because it is the number that separates a vessel that is safe to run for another campaign from one that is one heat away from a breakout. Yet a surprising number of plants still rely on visual estimation or infrequent manual checks to make that call, which leaves a wide margin of uncertainty exactly where certainty matters most. Laser and ultrasonic measurement methods close that gap by turning a visual guess into an actual number, and doing it often enough to catch a wear trend before it becomes an emergency. Getting that measurement data organized and trended is where iFactory's refractory monitoring platform fits in.
Refractory Lifecycle · Thickness Measurement
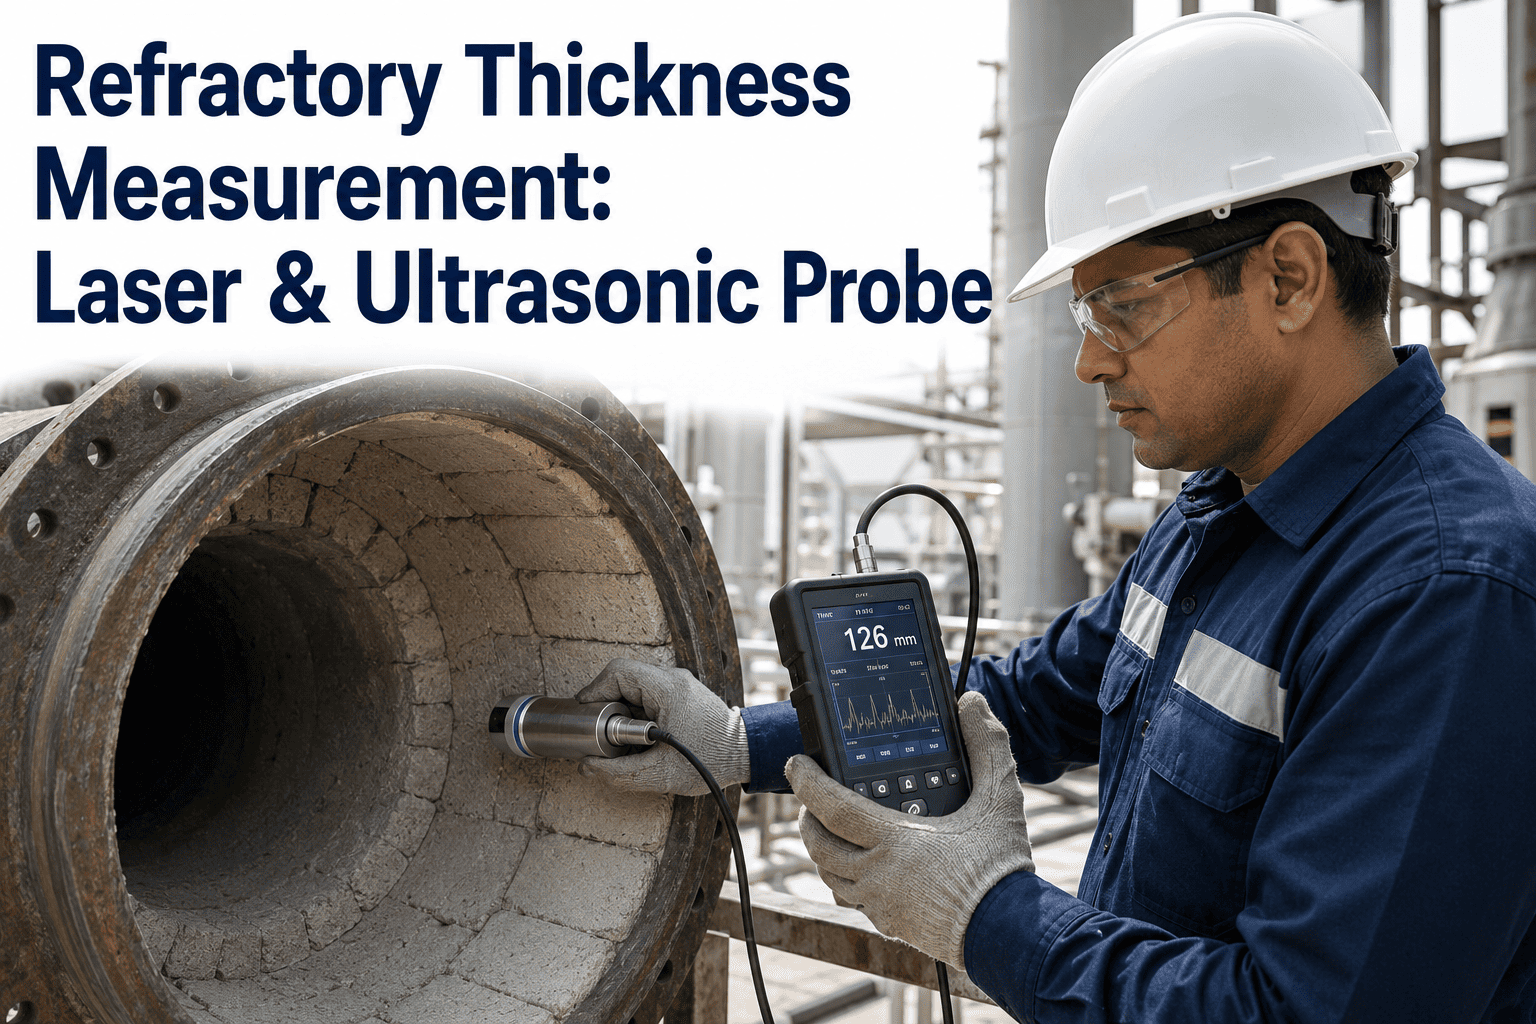
Refractory Thickness Measurement: Laser, Ultrasonic, and Probe Methods Compared
Visual inspection tells you a lining looks worn. Laser and ultrasonic measurement tell you exactly how much material is left, in millimeters, and whether the wear rate is accelerating. That difference is what separates planned replacement from an unplanned breakout.
Three Ways to Measure
Laser, Ultrasonic, and Mechanical Probe Compared
Laser Profiling
Scans the interior surface of a vessel to produce a full profile map, catching localized thin spots and uneven wear patterns that a single-point reading would miss entirely.
Ultrasonic Thickness Gauging
Measures remaining thickness from outside the vessel shell where accessible, well suited to routine spot checks without needing the vessel to be empty or cooled.
Mechanical Probe
A direct physical measurement taken at specific points, simple and low-cost, but limited to the exact spots checked and dependent on consistent operator technique.
Choosing the Right Fit
Online vs. Offline Measurement
| Factor | Online (In-Service) | Offline (Vessel Down) |
|---|---|---|
| Vessel state | Operating or between heats | Empty and accessible |
| Typical method | Ultrasonic from shell exterior | Laser profiling, mechanical probe |
| Measurement frequency | Can be very frequent, low disruption | Limited to scheduled downtime |
| Coverage | Accessible shell points only | Full interior surface possible |
See Your Wear Trend, Not Just a Snapshot
Turn Your Measurement Readings Into a Continuous Wear Curve
Bring your recent thickness measurement data and we will show you what a continuous trend line reveals that individual point-in-time checks don't.
What Affects Reading Accuracy
Variables That Change Measurement Reliability
Surface Condition and Slag Buildup
Residual slag or scale on the hot face can distort readings, particularly for laser methods that rely on a clear line of sight to the actual refractory surface.
Temperature at Time of Measurement
Ultrasonic readings in particular need temperature compensation, since sound velocity through refractory material shifts with temperature and skews raw readings if uncorrected.
Consistency of Measurement Point
Comparing readings over time only works reliably when measurements are taken at the same defined points each time, rather than wherever seems convenient that day.
Equipment Calibration
Both laser and ultrasonic equipment drift out of calibration over time, and uncalibrated readings can create a false sense of confidence in a wear trend that isn't actually accurate.
Getting Consistent Data
A Repeatable Measurement Process
1
Define Fixed Measurement Points
2
Calibrate Equipment Before Use
3
Record Temperature and Conditions
4
Log Readings Against Heat Count
5
Trend, Don't Just Snapshot
What Goes Wrong
Common Mistakes in Thickness Measurement Programs
Measuring Different Points Each Time
Taking readings wherever is convenient rather than at fixed, repeatable points, which makes trend comparison unreliable over successive campaigns.
Skipping Temperature Compensation
Treating raw ultrasonic readings as accurate without correcting for the temperature the measurement was taken at, skewing the trend line.
Measuring Too Infrequently
Checking thickness only at major scheduled outages, missing accelerating wear that develops well before the next planned check.
Not Connecting Readings to Heat Count
Recording thickness without tying it to how many heats or how much production occurred since the last reading, losing the context needed to calculate an actual wear rate.
Before Your Next Measurement Round
Readiness Checklist for Thickness Measurement
Confirm fixed measurement points are defined and documented for each vessel
Verify equipment calibration status before each measurement round
Record temperature and surface condition alongside every reading
Log readings against heat count so wear rate, not just thickness, can be calculated
A Composite Scenario
A BOF Vessel, Two Measurement Approaches
Before
A BOF vessel was measured with a mechanical probe at whatever point looked most worn during each scheduled outage, with no fixed reference points. Successive readings couldn't be compared reliably, and the team relied on visual judgment to time the next relining, erring conservatively and pulling the vessel earlier than needed.
After
Switching to laser profiling at defined reference points during every outage produced a genuine wear trend across campaigns. The trend showed remaining life was better than the conservative estimate, and the team extended the vessel's service by a full campaign with data-backed confidence.
Common Questions
Refractory Thickness Measurement — FAQ
Which method is more accurate, laser or ultrasonic?
Both can be highly accurate when used correctly, but they solve different problems. Laser profiling gives a full surface map that catches localized thinning, while ultrasonic gauging is better suited to frequent spot checks without taking a vessel out of service. Choosing between them depends on whether you need full coverage or frequent monitoring. Our team can help match the method to your specific vessel.
How often should thickness be measured?
It depends on the vessel's wear rate and criticality, but high-turnover vessels like ladles benefit from measurement at nearly every major outage, while less frequently cycled vessels may only need periodic checks. The key is consistency in frequency, since sporadic measurement makes trend analysis unreliable regardless of the method used.
Can measurement data actually predict when a vessel needs relining?
Yes, once enough consistent readings accumulate against heat count, the resulting wear trend can be extrapolated to estimate a remaining-life window with far more confidence than a single point-in-time reading or visual judgment alone provides. Book a demo to see how these predictions are generated from trend data.
Does slag buildup affect measurement accuracy?
Yes, residual slag or scale on the surface can distort readings, particularly with laser methods that need a clear line of sight to the actual refractory surface rather than a layer of buildup sitting on top of it. Surface cleaning before measurement is a standard part of a reliable process.
Is mechanical probing still worth using given laser and ultrasonic options exist?
Mechanical probing remains useful for low-cost, targeted spot checks, especially where laser or ultrasonic equipment isn't readily available, but it depends heavily on consistent operator technique and generally provides less coverage than a full laser scan.
Turn Point-in-Time Readings Into a Real Trend
Track Refractory Thickness Against Heat Count on One Platform
iFactory brings your laser, ultrasonic, and probe measurements together into one continuous wear curve, so relining decisions are based on data, not a conservative guess.