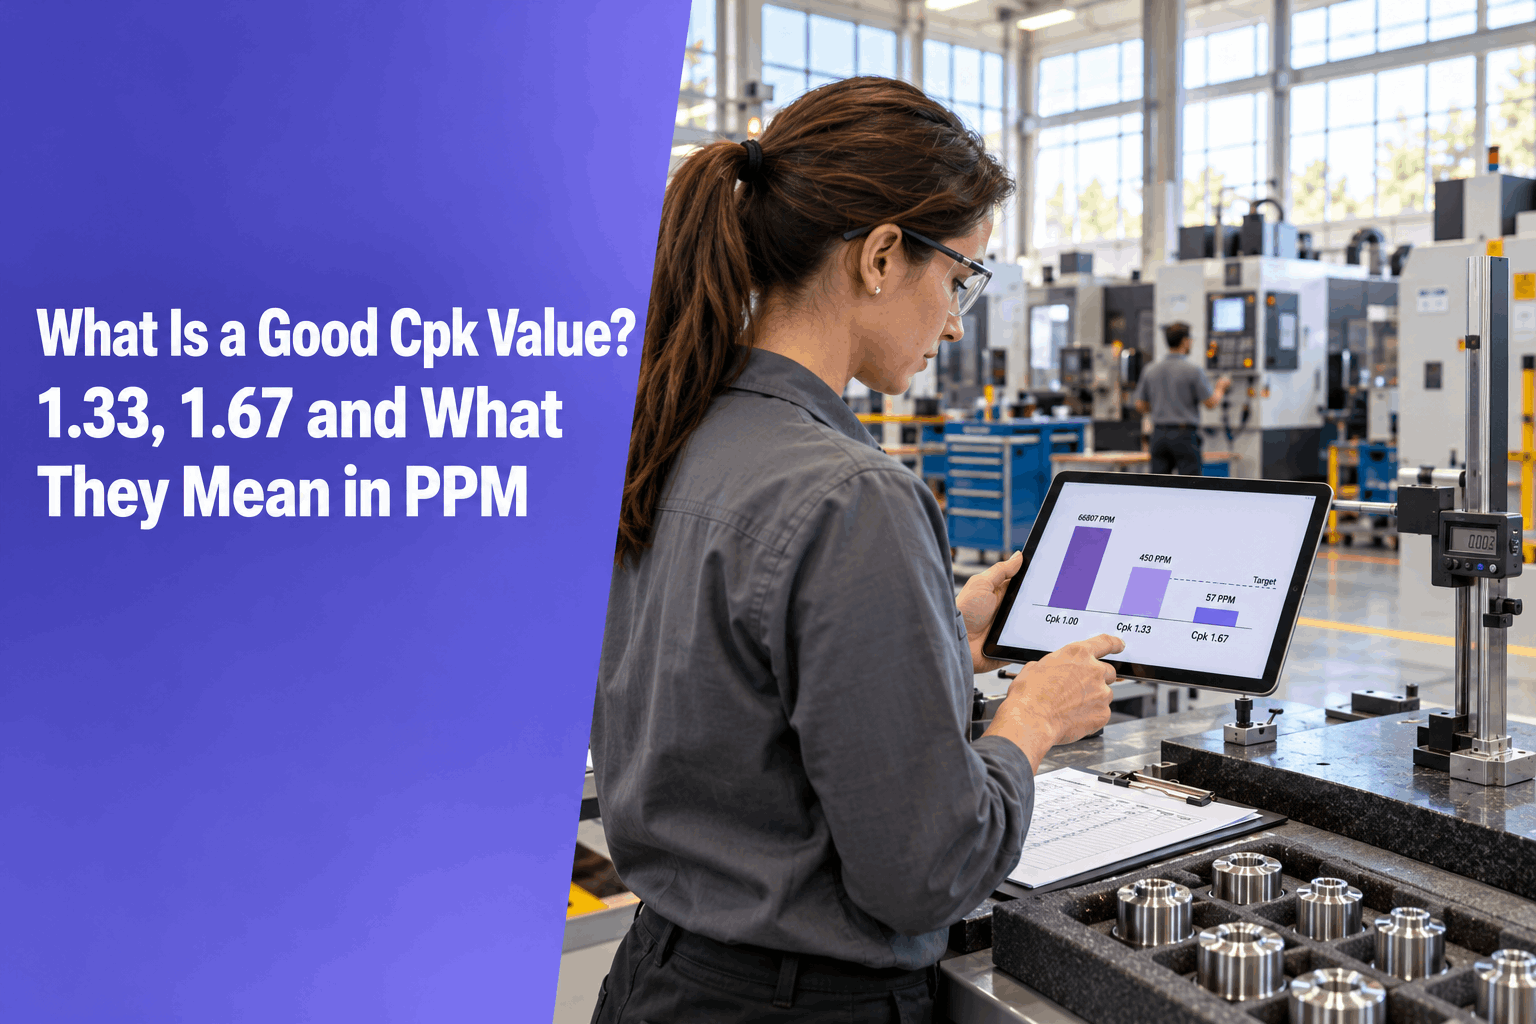
Short answer: a good Cpk value for an ongoing process is at least 1.33. New processes and PPAP initial studies are often held to 1.67. Below 1.00, you should expect parts outside the limits. This page shows what those numbers mean in parts per million and what to do when you fall short. If you still need the number itself, first calculate Cpk.
Three numbers worth remembering
Most capability questions come down to 1.00, 1.33 and 1.67. Know what each one means on the shop floor, and you can read any capability report in seconds.
Cpk benchmarks at a glance
This is how Cpk to PPM works out for a centered process with both limits and normal data. The bar shows expected parts per million on a log scale, so each step down is a big fall.
Why 1.33 is the usual minimum
Cpk times three tells you how many standard deviations sit between the mean and the nearest limit. At 1.00, that distance is three sigma, which is exactly the natural edge of the process. There is no room left. Any drift in the mean pushes parts straight out of spec, on top of the 2,700 PPM you already expect.
At Cpk 1.33, there is four sigma of room: the normal spread plus one extra sigma of buffer. A small shift between setups or tool changes no longer turns straight into rejects, and the expected rate for a centered process is about 63 PPM. That balance of protection and cost is why 1.33 is the usual minimum Cpk for ongoing production.
When 1.67 (or 2.00) is asked for
A higher bar shows up in three common situations.
A new process has little history. A short study cannot show every source of drift yet, so a Cpk 1.67 target leaves room for what has not happened so far.
The AIAG PPAP manual sets three bands for initial process studies:
On characteristics flagged as safety or critical, the customer sets the requirement. It may be 1.67 or 2.00, and it can differ from one feature to the next on the same part.
Get Cp, Cpk, Pp and Ppk from your own data: paste your measurements and get a one-page capability report. 14-day free trial, no card needed.
What a Cpk below 1.33 tells you, and what to do
A low Cpk has two possible causes, and the fix depends on which one you have. Put the number next to Cp first. If you need a refresher on how the two differ, see Cp vs Cpk.
It is a centering problem
The spread fits the tolerance, but the mean sits closer to one limit. This is usually the quickest fix.
It is a spread problem
Even perfectly centered, the process is too wide for the tolerance. Re-aiming will not be enough.
- Re-center the process. Adjust the offset or setup target toward nominal, then confirm with fresh data.
- Reduce variation. Look at fixturing, material, tooling and method for the biggest sources of spread.
- Check the gauge. Run a gauge R&R study. Measurement noise inflates sigma and pulls Cpk down.
- Question the tolerance, last. If the process is stable and well run, ask engineering and the customer whether the tolerance reflects what the part really needs.
Why a good Cpk value can still mislead
A number above 1.33 is only as trustworthy as the study behind it. Three things can make it look better than the process really is.
The process is unstable
Cpk uses within-subgroup sigma, so drift between subgroups does not show up in it. An unstable process can post a strong Cpk while overall output varies far more. Check the control chart, and compare with the overall-sigma index described in Cpk vs Ppk.
The data is not normal
Every PPM figure on this page assumes normal data. Skewed characteristics can have a longer tail on one side, so the real out-of-spec rate can differ a lot from the estimate. Look at a histogram first.
Too few values
A small sample gives a wide range of possible true values. The ranges below are illustrative, approximate 95% ranges for a measured Cpk of 1.33 with normal data.
With 30 values, a reported 1.33 could really be below 1.00. With about 100 values, the range tightens a lot. That is why a capability study needs about 25 subgroups or 100 values before anyone leans on the result.
Check your own number against the target
Once you know which target applies, the Cp/Cpk Report Generator checks your data against it and gives an estimate you can review:
Get Cp, Cpk, Pp and Ppk from your own data: paste your measurements and get a one-page capability report. 14-day free trial, no card needed.
Frequently asked questions
What is a good Cpk value?
For an ongoing process, 1.33 is the usual minimum, which works out to about 63 parts per million outside the limits for a centered, normal process. New processes and PPAP initial studies often need 1.67. Your customer's drawing or quality manual has the final say, so check it before you report a result.
Is a Cpk of 1.00 acceptable?
Usually not. At 1.00, the process spread exactly fills the tolerance, and a centered normal process makes about 2,700 parts per million outside the limits. Any drift in the mean adds more on top. Treat 1.00 as a warning sign and work on centering or variation before you rely on the process.
How do I convert Cpk to PPM?
For a centered process with two limits and normal data, Cpk 1.00 is about 2,700 PPM, 1.33 about 63, 1.67 about 0.57 and 2.00 about 0.002. If only one limit is close to the mean, use roughly half these numbers. Non-normal data can make the real figure quite different.
Why does six sigma mean 3.4 PPM in some places and 0.002 here?
The 3.4 PPM figure assumes the mean drifts by 1.5 sigma over time, so a six sigma process behaves like a 4.5 sigma one. The 0.002 PPM figure assumes the mean stays exactly centered. Both are estimates built on normal data, so state which convention you are using.
What should I do if my Cpk is below 1.33?
Compare it with Cp first. If Cpk is well below Cp, re-center the process. If both are low, work on reducing variation and check your gauge with a gauge R&R study. Only after that should you ask whether the tolerance itself is right, and that question goes to engineering and the customer.